Featured High-Performance Titanium Fasteners & Hardware
Engineered for extreme motorsport, aerospace-grade assemblies, marine engineering, and custom precision tooling. Fully customizable according to DIN, GB, and custom CAD blueprints.
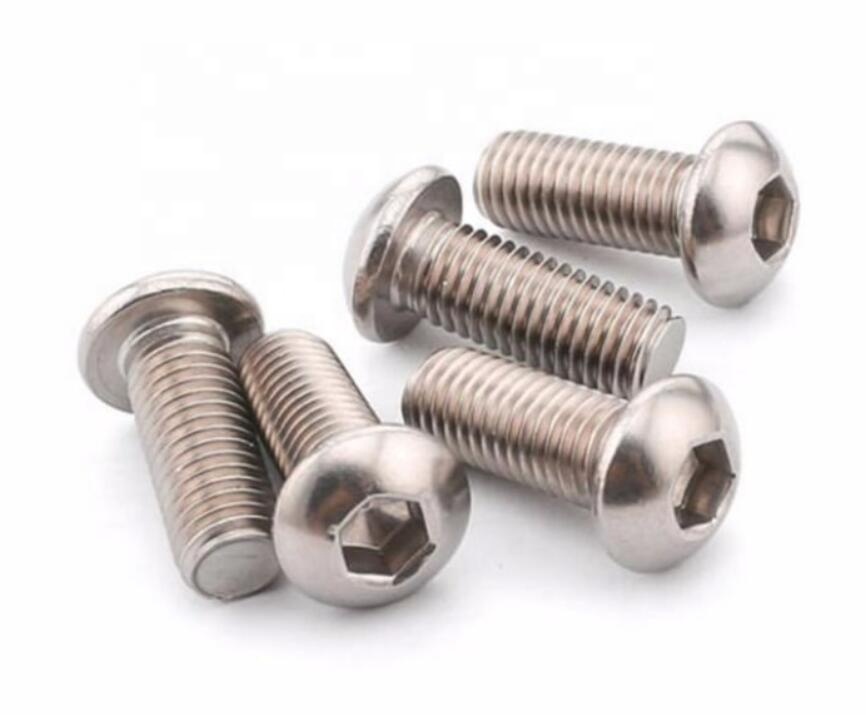
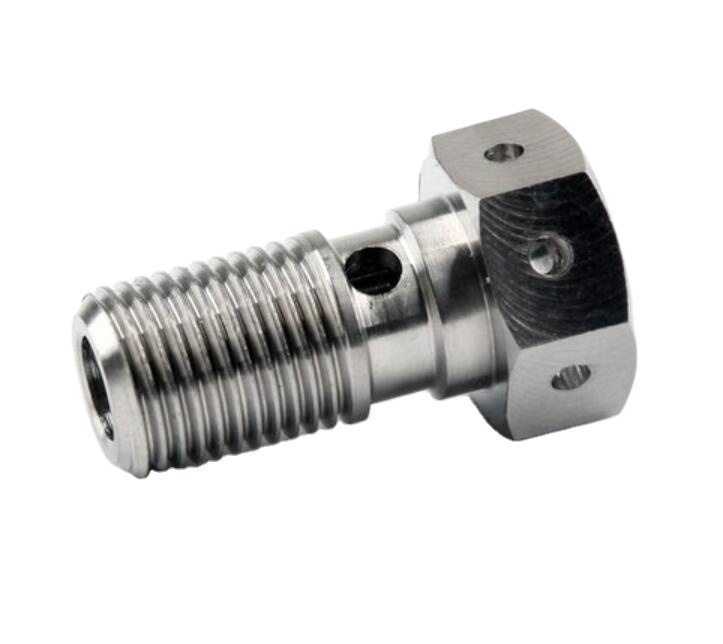
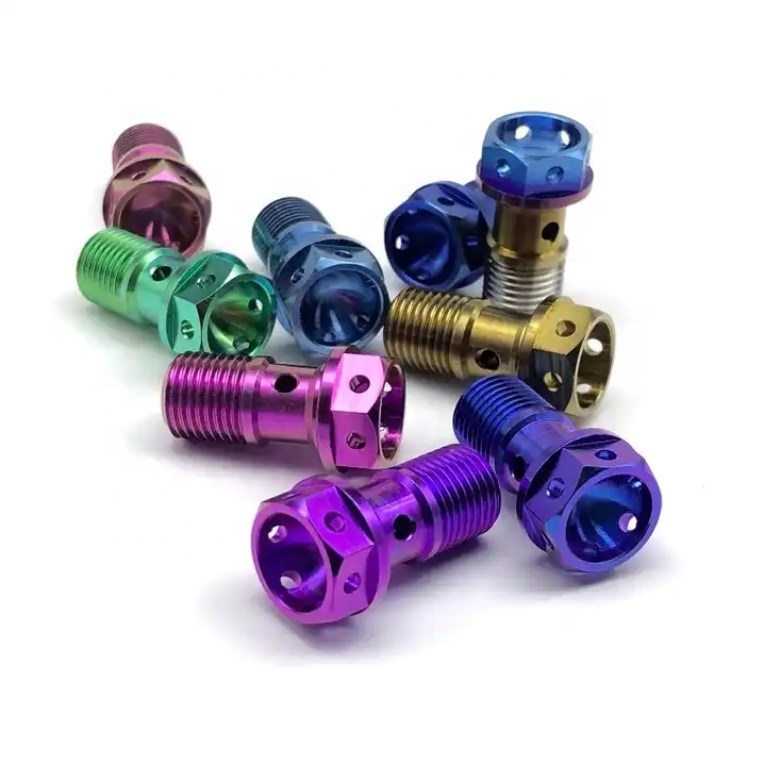
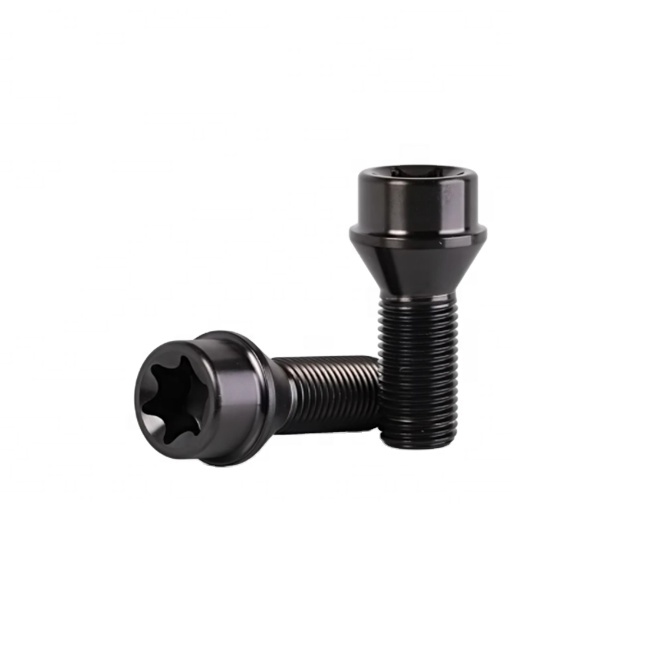
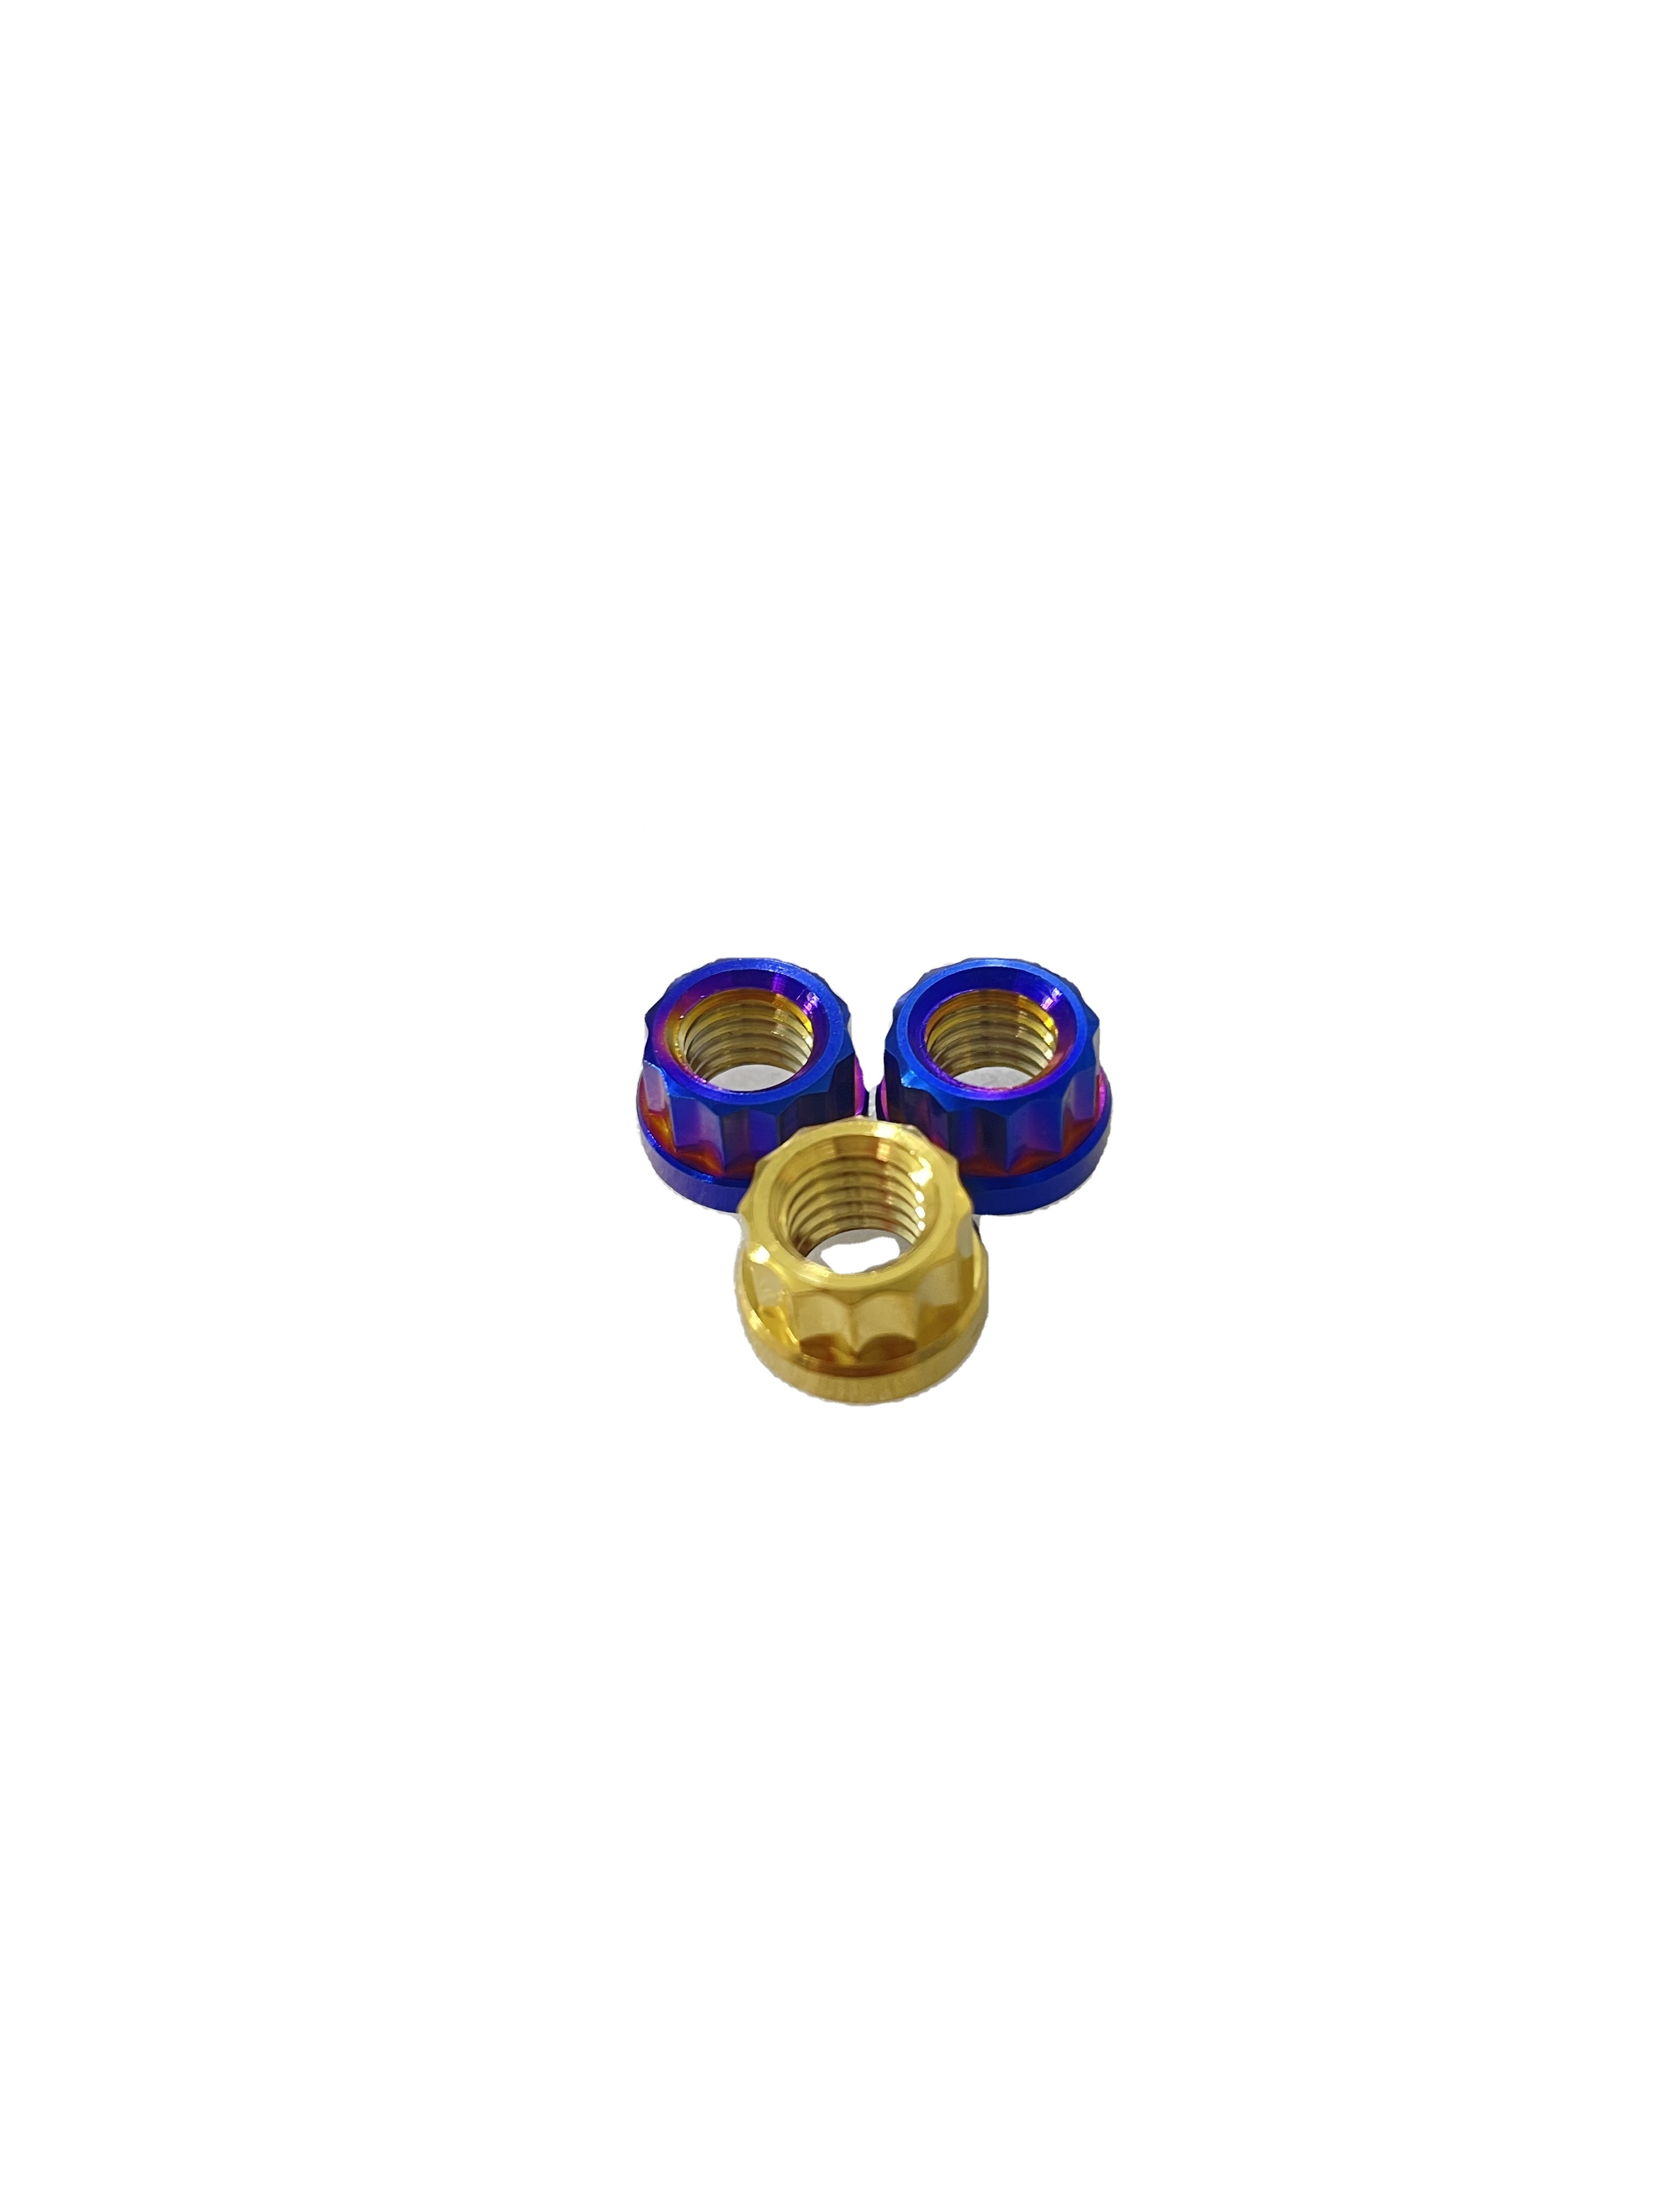
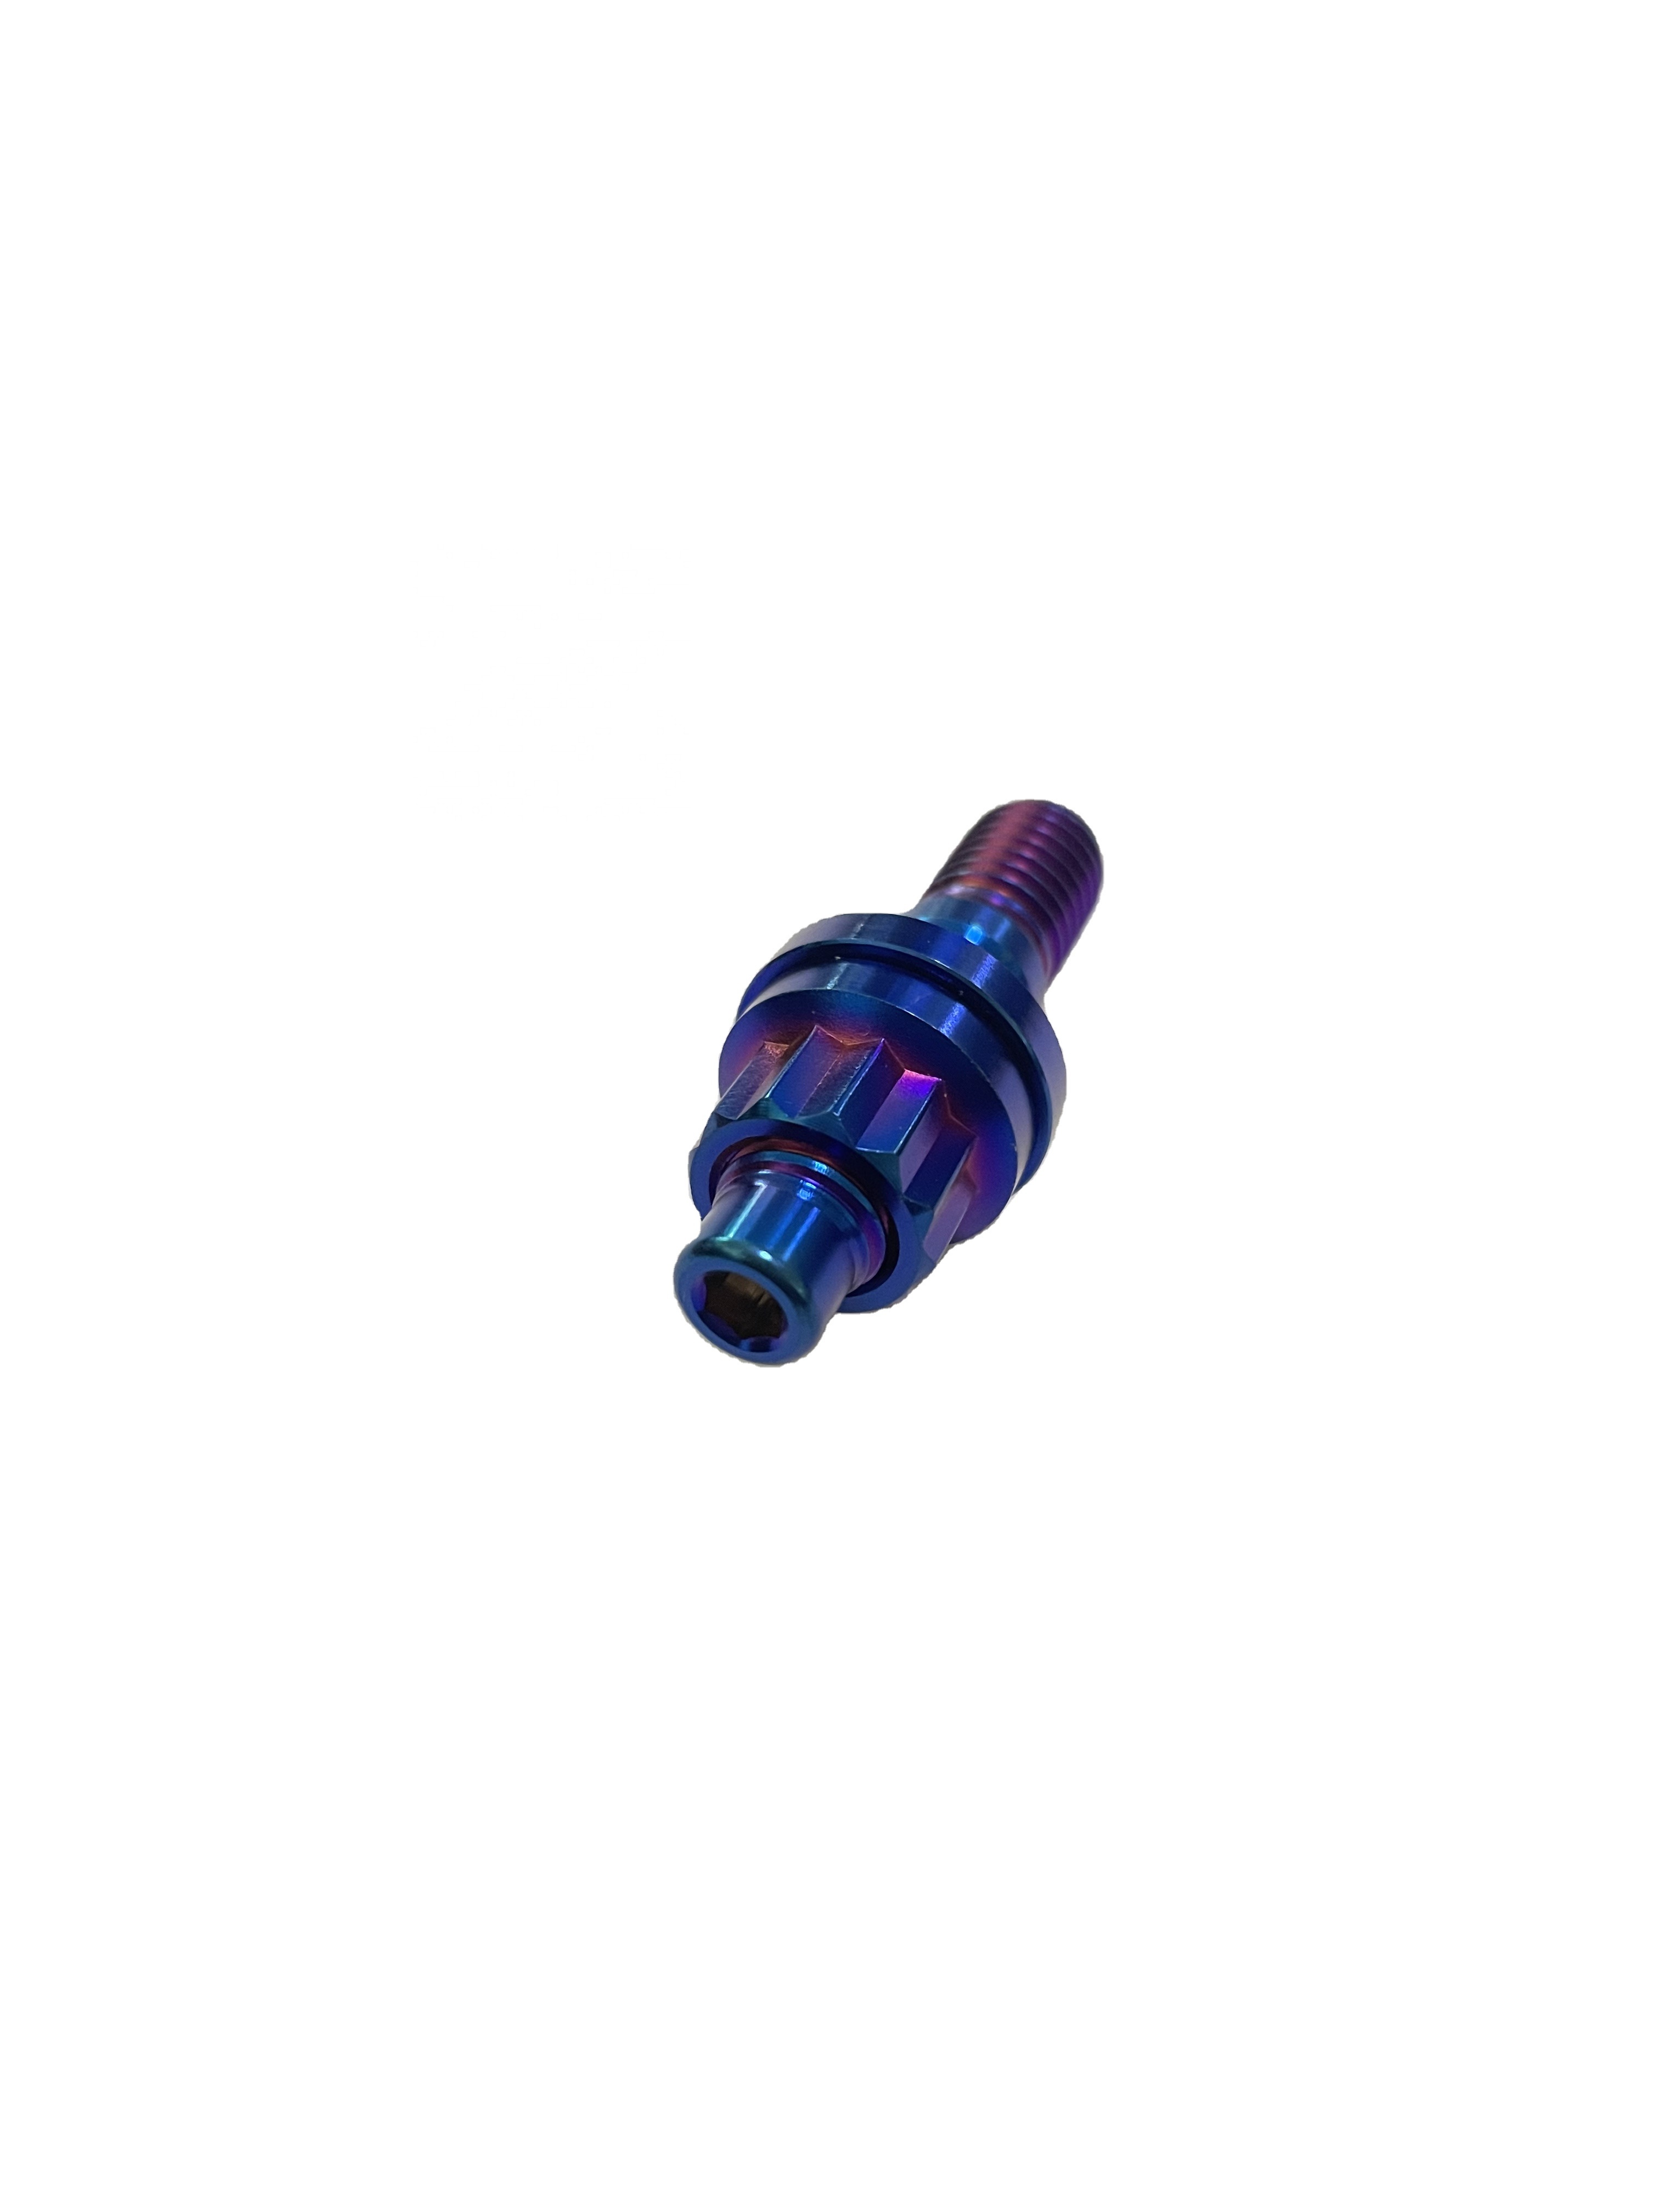
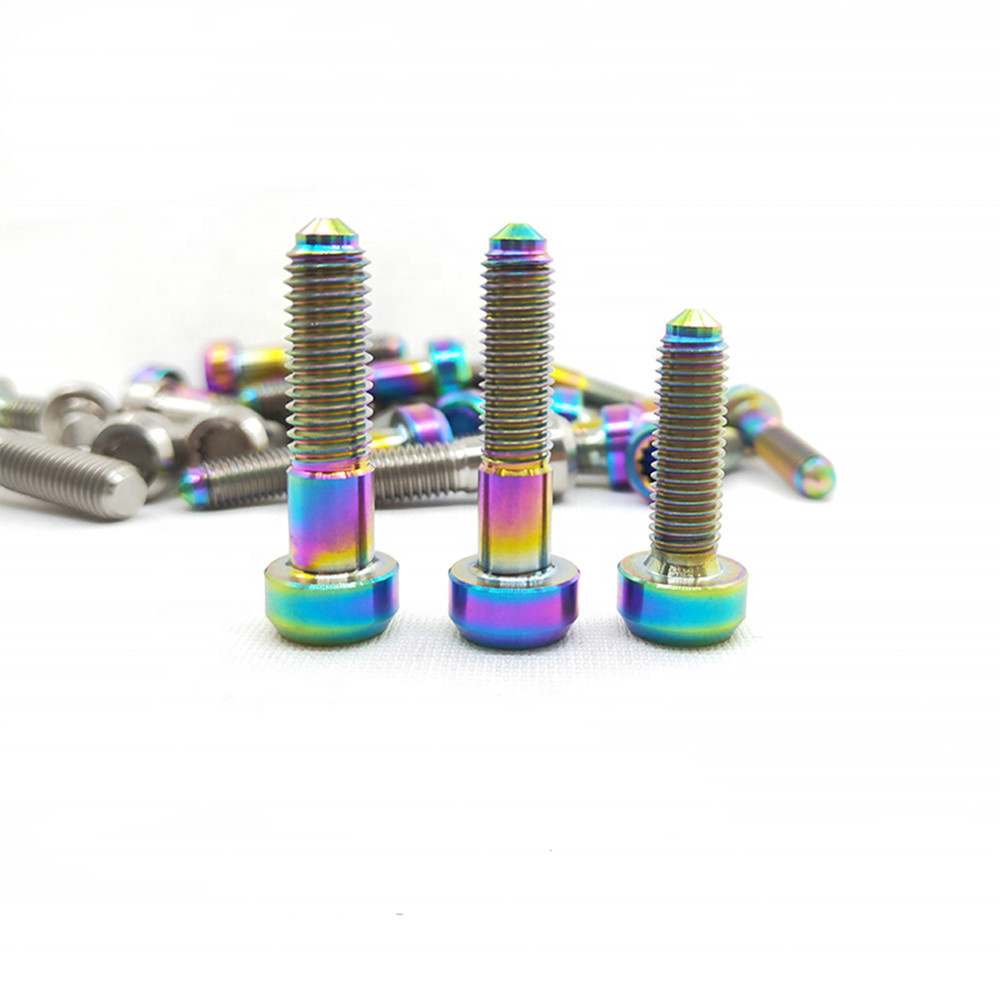
Industrial Engineering Whitepaper: Metallurgical Excellence in Titanium Fastening
Why leading aerospace, hypercar manufacturers, and offshore petrochemical systems rely on Baoji's cold-rolled and CNC precision-turned Grade 5 titanium stud bolts.
In high-stress mechanical engineering, fastener failure is rarely an isolated event—it is catastrophic. Traditional steel studs suffer from corrosive pit degradation, excessive thermal mass expansion, and shear fatigue under high-frequency vibratory loads. As premier manufacturers and direct exporters situated in Baoji (universally recognized as China's Titanium Valley), Vunza Titanium Industry Co., Ltd. addresses these engineering pain points through microstructural optimization of Ti6Al4V (Grade 5 / TC4) alloys.
Titanium boasts an exceptional strength-to-density ratio: at an ultra-light 4.43 g/cm³, Grade 5 titanium delivers a minimum tensile strength exceeding 895 to 1050 MPa, effectively matching Class 10.9 and Class 12.9 alloy steels while yielding a 44% to 47% unsprung weight reduction. For powertrain and racing suspension engineers, cutting rotatory and unsprung reciprocating mass translates directly into reduced rotational inertia, lightning-fast throttle response, optimized suspension damping cycles, and elevated thermodynamic efficiency.
| Mechanical / Physical Property | Grade 5 Titanium (Ti6Al4V) | AISI 4140 Alloy Steel | 316L Marine Stainless | Engineering Advantage |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 g/cm³ | 7.85 g/cm³ | 8.00 g/cm³ | ~45% Massive Weight Reduction |
| Yield Strength (Rp0.2 MPa) | 828 - 920 MPa | 650 - 850 MPa | 220 - 300 MPa | Superb Elastic Deflection Limit |
| Tensile Strength (Rm MPa) | 895 - 1050 MPa | 950 - 1100 MPa | 520 - 680 MPa | High Clamping Force Resistance |
| Corrosion Resistance | Impervious to Chlorides/Salt | Prone to Oxidation/Rust | Moderate (Pitting Vulnerable) | Zero Galling Rust Over Decades |
| Operating Thermal Window | -250°C to +450°C | -20°C to +300°C | -196°C to +400°C | Ideal for Exhaust & Turbo Manifolds |
Unlike standard generic fasteners produced by third-party cutting workshops, Vunza's manufacturing protocol mandates cold thread rolling rather than thread turning or grinding whenever fatigue resistance is critical. Cold thread rolling reorients the natural metallic grain flow along the pitch radius and root radii of the thread profile, completely eliminating stress concentration micro-notches. Consequently, our stud bolts demonstrate up to 300% higher cycle fatigue endurance under high-boost manifold boost pressure, cyclic heat cycles, and severe track harmonic vibration.
Future Procurement Trend
Global procurement teams are shifting away from intermediate regional distributors toward factory-direct source contracts in Baoji, China. Supply chain volatility, tightened automotive margins, and the explosion of EV battery tray weight optimization require rapid OEM sample validation, mill test chemical cert traceability (MTR), and stable ISO 9001 production queues.
Evolutionary Technological Drivers
The transition toward multi-axis Swiss-lathe simultaneous 5-axis milling allows complex internal lightweighting bores, customized reverse hex drive pockets, and precision conical tapers. Concurrently, vacuum PVD (Physical Vapor Deposition) nitriding treatments offer surface micro-hardnesses exceeding 2500 HV, preventing galling during repeated track tire changes.
Total Cost of Ownership (TCO)
While raw titanium raw materials involve higher up-front tooling investments than alloy steel, titanium studs eliminate ongoing galvanic corrosion maintenance, thermal seizing, and the expensive labor costs associated with removing snapped steel bolts from aluminum engine blocks. In offshore marine subsea structures and high-performance racing, titanium achieves the lowest lifecycle cost.
Why Choose Vunza: China Titanium Valley Authority
Strategically positioned in Gaoya Village Industrial Zone, Baoji, Shaanxi, adjacent to Baoti Group Industrial Park—delivering raw material purity, processing precision, and global trade reliability.
Complete Integrated Production
Founded in 2008, our plant spans entire value streams: raw sponge titanium melting review, precision forging bar stock verification, multi-axis high-speed CNC turning, thread rolling, ultrasonic degreasing, anodic oxidation, and laser branding.
Rigorous Quality Inspection (QC)
Every single batch undergoes dimensional verification using calibrated digital micrometers, 3D coordinate measuring machines (CMM), optical contour projectors, and mechanical go/no-go ring gauges to maintain tolerances down to ±0.005 mm.
Rapid Response & Custom DFM
Our senior engineering team provides Design for Manufacturability (DFM) feedback and customized 2D/3D CAD quotation analysis within 9 hours on business days, ensuring smooth prototyping and rapid scale-up for custom thread lengths and head designs.
Frequently Asked Questions on Titanium Stud Bolt Procurement
Critical technical, logistical, and metallurgical answers for engineering directors and procurement officers.
For high-heat and high-pressure setups such as engine head studs and turbo exhaust manifolds, Grade 5 Ti6Al4V (TC4) is universally recommended. It offers tensile strengths up to 1050 MPa and retains structural preload up to 450°C. For chemical tank valves or marine immersion where corrosion is paramount and mechanical load is modest, CP Grade 2 is utilized.
Cut threads sever the internal metallurgical grains of the titanium bar stock, producing sharp microscopic stress notches susceptible to fatigue cracking under engine harmonics. Vunza utilizes cold rolled threads, which deform and compress the alloy's crystalline structure smoothly into shape, yielding superior burnished surface finishes and dramatically enhanced shear fatigue life.
Titanium has a naturally self-healing titanium oxide layer that can cause cold-welding friction (galling) when mated with similar alloys or dry aluminum. We resolve this by applying ultra-smooth burnished threads, micro-tolerance concentricity, PVD Diamond-Like Carbon (DLC) or TiN coatings, and recommending anti-seize molybdenum disulfide or nickel-based assembly paste during installation.
For customized studs and bolts, our standard MOQ ranges from 100 to 500 units depending on thread geometry and material availability. Prototyping and custom sample development typically take 7 to 10 working days, with mass batch CNC and thread-rolling orders dispatched within 18 to 25 business days worldwide via DHL/FedEx or consolidated sea freight.
Yes. Every export shipment is paired with verifiable EN 10204 3.1 Mill Test Certificates detailing spectral chemical breakdown (Al%, V%, Fe%, O%, C%, N%, H%) and tensile strain elongation data. Detailed first-article inspection (FAI) and final batch dimensional reports are also provided upon request.
Absolutely. Our 34 sets of multi-axis CNC machines allow for custom 12-point heads, Torx-plus drives, internal hex broaching, hex flange reductions, and lightweight dimpling. In addition, we offer in-house multi-color electrochemical anodizing (gold, purple, rainbow, burnt blue, green) and custom laser engraved serial numbers or client logos.
Accelerate Your Engineering with Premium Titanium Stud Bolts
Partner directly with China's leading titanium fastener factory in Baoji. Send your technical CAD drawings, target tolerances, and required quantities to receive rapid DFM feedback and competitive wholesale quotations within 9 hours.