Lightweight Titanium Valve Hardware: The Ultimate Global Sourcing & Engineering Guide
Engineered to eliminate valvetrain float, stabilize harmonics at 10,000+ RPM, and cut reciprocating inertia by 42% with 0.005 mm multi-axis CNC repeatability.
Why Global Engine Builders Specify Titanium Valve Hardware
Demystifying the physics of valvetrain acceleration: How reducing top-end reciprocating mass unlocks horsepower and safeguards against destructive valve bounce.
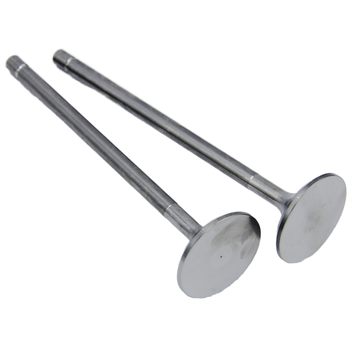
In ultra-high-performance internal combustion engines—ranging from Formula racing circuits, NHRA drag strips, and Moto3 / WorldSBK superbikes to heavy-duty marine competition motors—the valvetrain constitutes the single most severe inertial bottleneck. At engine speeds eclipsing 9,000 to 14,000 revolutions per minute, valves, retainers, and keepers accelerate and decelerate thousands of times every sixty seconds, enduring acceleration forces exceeding 4,000 g's. When heavy conventional chrome-moly or tool steel retainers are utilized, the immense kinetic energy causes spring surge, uncontrolled valve bounce upon seat impact, and harmonic float. Lightweight Titanium Valve Hardware solves this fundamental mechanical barrier by lowering the reciprocating mass at the top of the valve spring by roughly 42% to 45% compared to alloy steel equivalents.
Manufactured by Vunza Titanium Industry Co., Ltd. from certified aerospace-grade Ti6Al4V Grade 5 (UNS R56400 / Werkstoff 3.7165), our precision-engineered valve retainers, spring seats, and collets deliver an optimal tensile threshold above 895 MPa while retaining superior dynamic cyclic fatigue endurance. By stripping 6 to 14 grams of unnecessary mass from each valve assembly, engine designers can either safely raise rev ceilings by 500 to 1,200 RPM without inducing float, or significantly reduce valve spring seat pressure. Diminishing required seat pressure directly decreases camshaft friction torque, reducing oil operating temperatures, curbing valvetrain parasitic losses, and freeing up net crankshaft horsepower.
Engineered Product Spectrum
Precision Valve Hardware Solutions
Factory-direct Ti6Al4V Grade 5 valve retainers, custom spring locators, and hardened titanium locks built to customer drawings.
Valvetrain
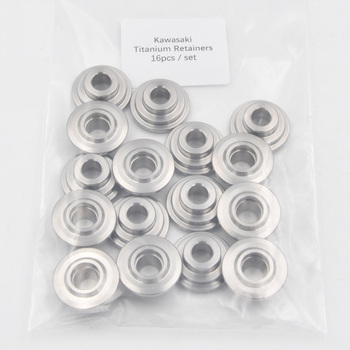
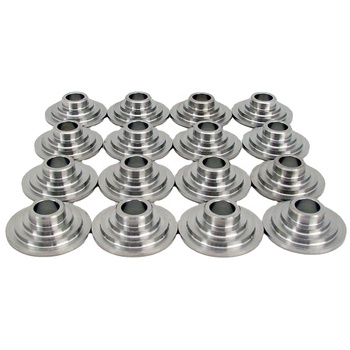
TC4 Racing Titanium Valve Retainer
Multi-step pocketing · 7° / 10° bead seat
Ultra-lightweight titanium retainers configured for single and beehive performance springs. Micro-turned steps ensure perfect inner and outer spring concentricity.
Engineered specifically for dual valve springs subjected to brutal lift profiles. Features radiused outer chamfers and a stress-relieved titanium step to absorb harmonic resonance.
Complete matched valvetrain sets tailored for motorcycle racing and high-rev four-cylinder platforms. Reduces reciprocating valvetrain mass across all intake and exhaust ports.
Base spring seats and spring cups designed to protect aluminum cylinder heads from abrasive spring galling while maintaining precision installed spring heights.
Modern engine builders no longer procure simple turned disc retainers. Today's procurement contracts demand generative, FEA-optimized pocketed geometries that shave weight from low-stress zones while thickening radial shear sections. As advanced CAD simulation tools proliferate, tier-1 racing teams are sourcing bespoke multi-axis CNC machined titanium hardware that mirrors topology-optimized algorithmic models, eliminating micro-grams without risking catastrophic fatigue fracture.
2. Demand for Integrated Anti-Galling Surface Treatments
Historically, titanium valve hardware required separate post-machining logistics to apply specialized anti-friction finishes. Procurement trends reveal that buyers now insist on consolidated factory-applied coatings—such as Diamond-Like Carbon (DLC), Physical Vapor Deposition (PVD TiCN), and oxygen thermal micro-diffusion. Partnering with Vunza Titanium Industry Co., Ltd. allows buyers to bypass fragmented subcontractors by securing finished, pre-treated retainers with surface hardness reaching Hv 1200+ directly from a single facility.
3. Direct Sponge-to-Machined-Part Traceability
With counterfeit titanium and unverified scrap alloys infiltrating global supply chains, international buyers now enforce strict raw material genealogy. Valvetrain failure at 11,000 RPM causes catastrophic engine destruction. As a result, procurement directors require mill test certificates (MTCs) conforming to EN 10204 3.1 that trace every bar of Ti6Al4V straight back to vacuum-arc remelting (VAR) sponge origin, verifying rigorous nitrogen, oxygen, and hydrogen thresholds before machining commences.
» 22Ti «
Material Physics: Ti6Al4V vs. Traditional Valve Steels
Why Grade 5 Titanium is uniquely qualified to withstand high-frequency cyclic stress and thermal valvetrain environments.
Mechanical Property
Aerospace Ti6Al4V Grade 5 (Vunza Std.)
4140 Chrome Moly Steel
Tool Steel (H13 / S7)
Density (g/cm³)
4.43 g/cm³ (44% Lighter)
7.85 g/cm³
7.80 g/cm³
Tensile Strength (Yield / Ult.)
828 MPa / 950–1050 MPa
655 MPa / 850 MPa
1350 MPa / 1500 MPa
Strength-to-Weight Ratio
225 kN·m/kg (Unmatched top-end agility)
108 kN·m/kg
192 kN·m/kg
Modulus of Elasticity (GPa)
114 GPa (Harmonic dampening cushion)
205 GPa
210 GPa
Thermal Expansion (10⁻⁶/K)
8.6 (High dimensional stability)
12.2
11.5
Corrosion Resistance
Immune to acidic blowby gases & ethanol
Requires oil barrier
Susceptible to moisture pitting
4.43 g/cm³Aerospace Density
≥ 950 MPaUltimate Tensile Strength
-44% Weightvs. Chrome Moly Retainers
0.005 mmCNC Precision Tolerance
Future Technology Trajectory
The Technological Future of Lightweight Titanium Valvetrains
Titanium-Aluminide (TiAl) and Near-Beta Alloys on the Horizon
While Ti-6Al-4V remains the benchmark for value, fatigue life, and machinability in racing valve retainers and locks, experimental racing programs are evaluating Near-Beta titanium alloys (such as Ti-10V-2Fe-3Al and Beta C) and Gamma Titanium Aluminides (TiAl) for extreme-temperature exhaust valve environments. These advanced compositions offer elevated creep resistance up to 650°C. Vunza Titanium Industry Co., Ltd. stays at the cutting edge of these developments, continuously testing raw material formulations and machining parameters in our Baoji facility.
Micro-Fine Angle Consistency to Prevent Collet Pull-Through
As valvetrain pressures rise to accommodate intense turbocharging boosts and steep cam profiles, the mechanical lock angle (typically 7-degree or 10-degree tapers) between the valve lock and the retainer must match perfectly. A taper variance of even 0.2 degrees causes stress concentrations along the upper edge of the retainer hole, leading to fatal collet pull-through. The engineering future belongs to ultra-high-precision multi-axis CNC centers that execute both the exterior spring locating profiles and the inner locking taper in a single chucking setup, holding taper angle precision within ±0.03 degrees.
Downsized Forced-Induction Hybrid Engines
Contrary to the belief that vehicle electrification suppresses internal combustion innovation, high-efficiency hybrid powerplants (such as Formula 1 and endurance hypercars) demand more aggressive downsizing. These downsized turbocharged internal combustion engines operate under extreme cylinder pressures and high thermal flux. Lightweight Titanium Valve Hardware is essential to trim valvetrain inertia, allowing smaller valve springs, minimal cam friction, and unprecedented thermal efficiency.
Enterprise Strength
Vunza Titanium Industry Co., Ltd.
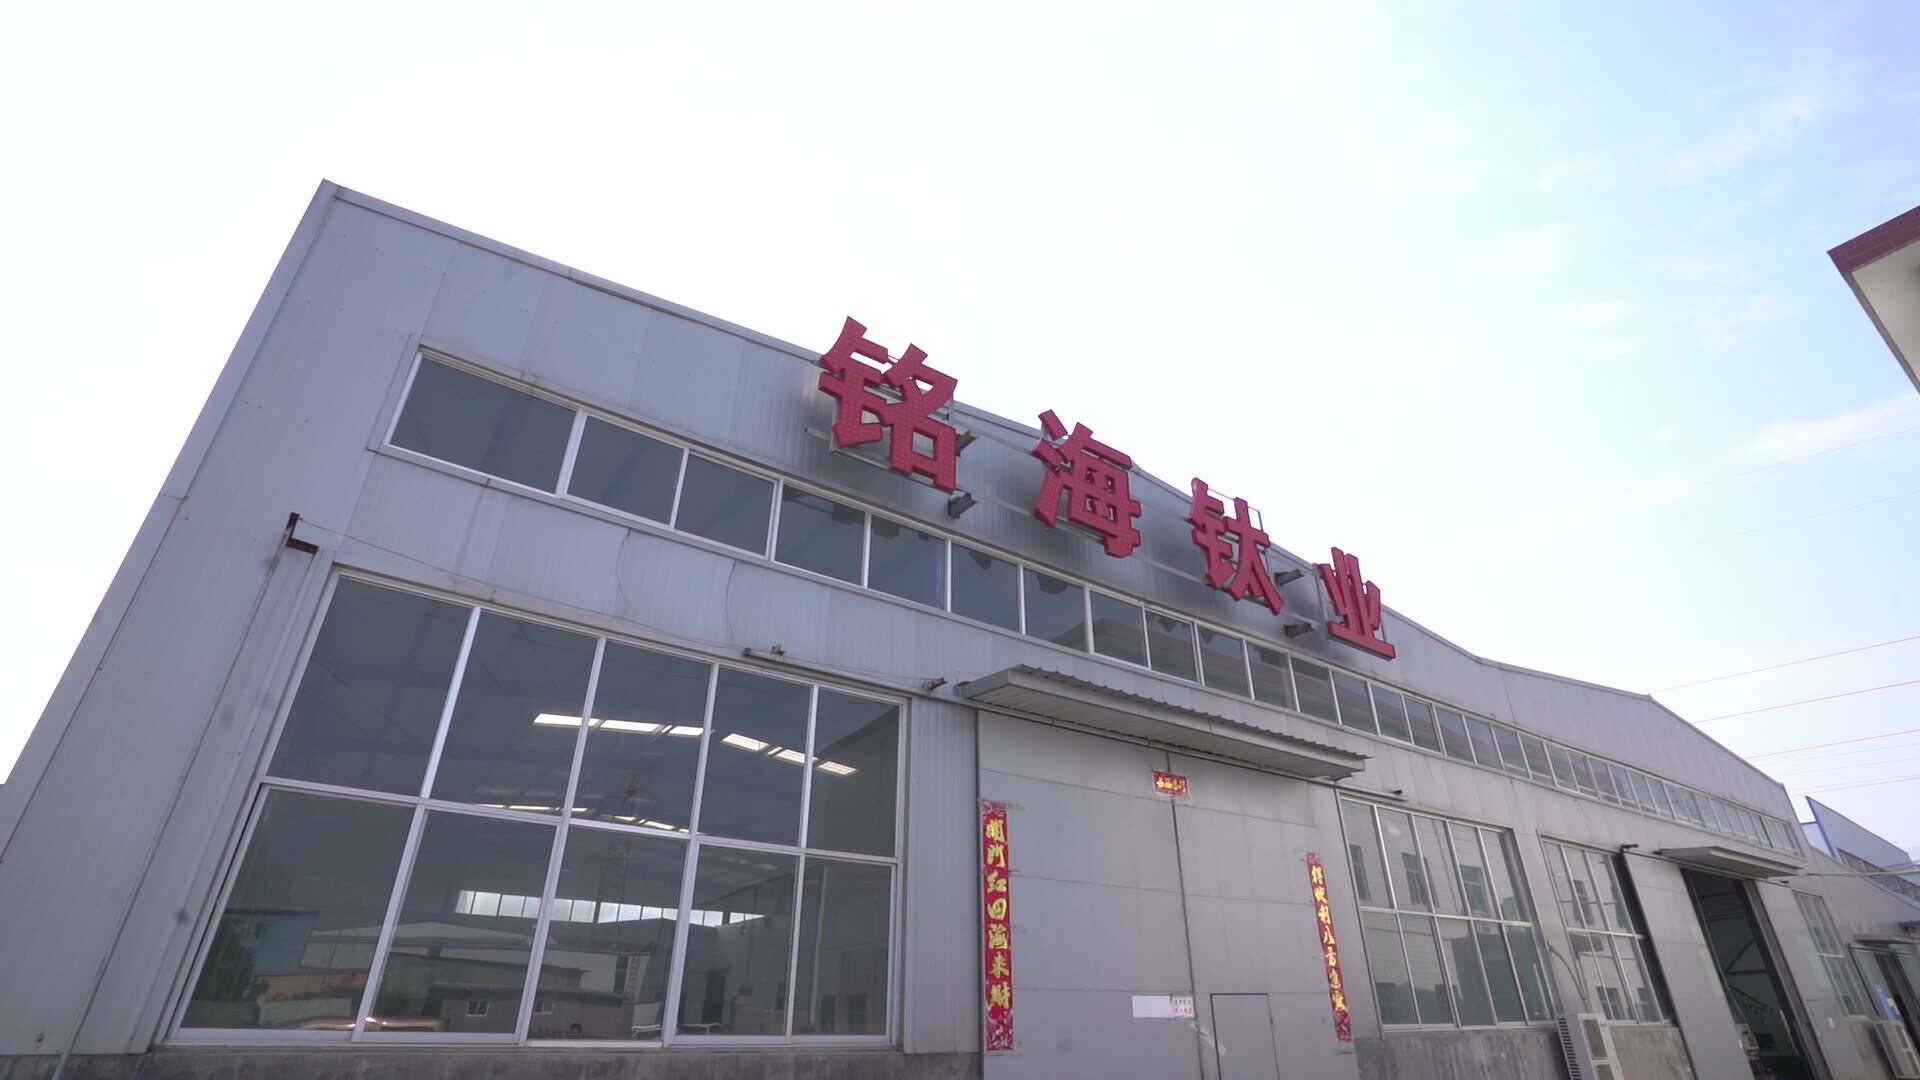
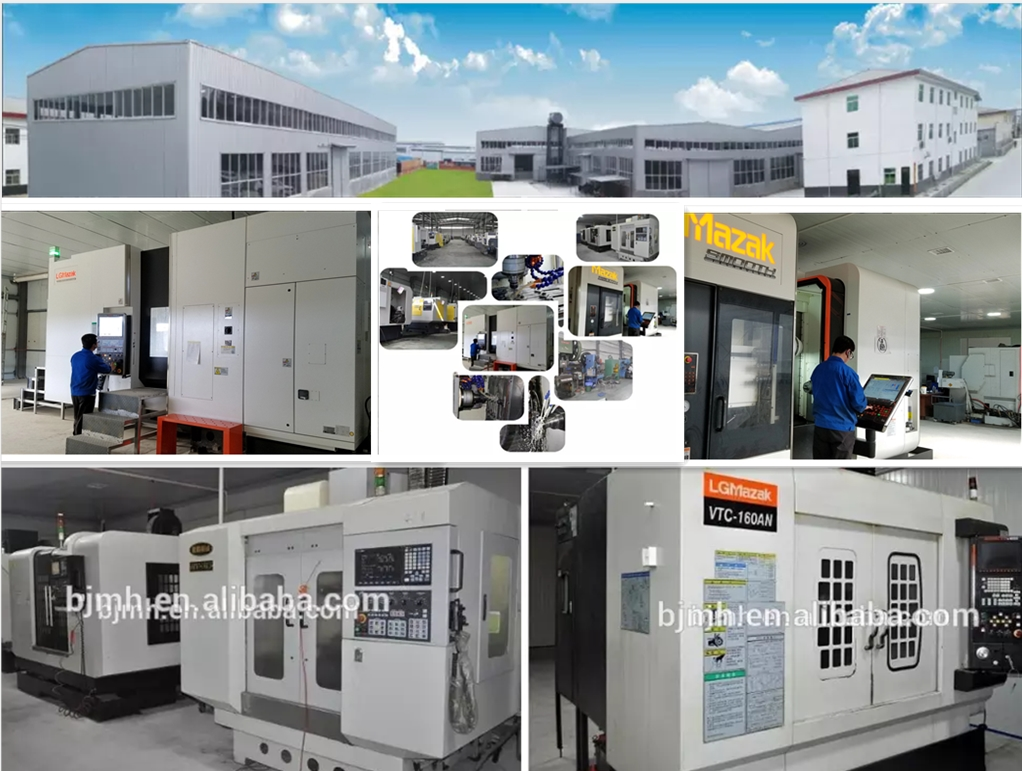
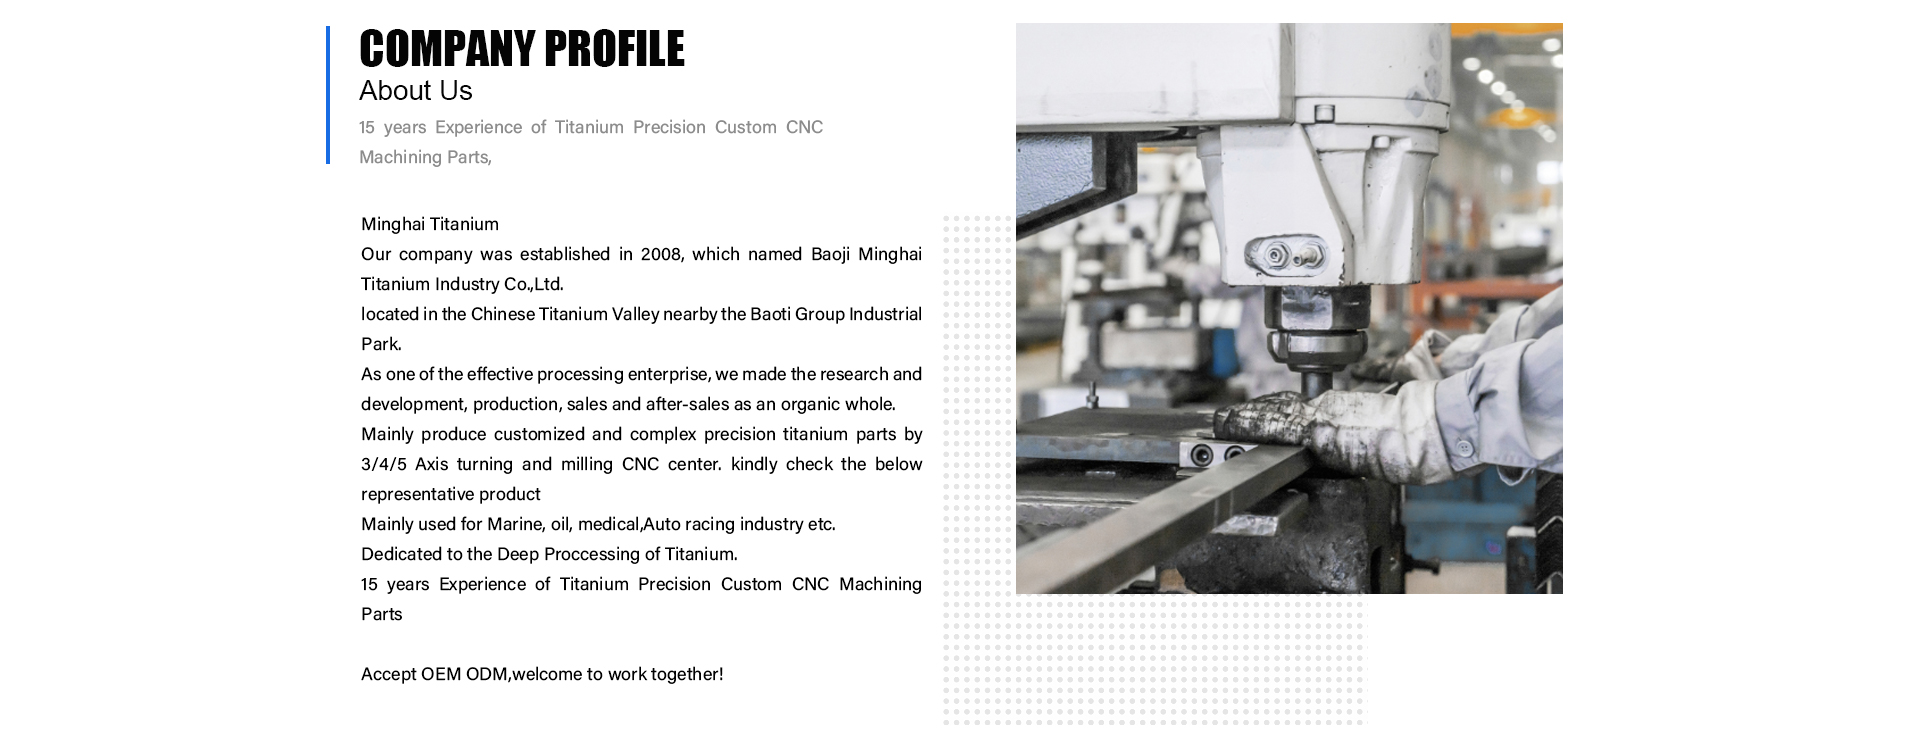
Established in 2008 in the heart of the Chinese Titanium Valley nearby the Baoti Group Industrial Park, Vunza seamlessly integrates R&D, precision manufacturing, sales, and global after-sales service.
We specialize in titanium CNC precision machining parts, standard and non-standard titanium fasteners, custom valvetrain hardware, and raw material for the marine, oil, energy, medical, outdoor, and high-performance racing sports industries. Our senior research and development team engineers custom, high-precision machined solutions tailored to client prints. More than 50% of our production personnel hold over 13 years of specialized titanium machining experience, guaranteeing exceptional craft and reliability across every order.
Business TypeManufacturer & Trading Co.
Established2008 · Baoji, Shaanxi, China
Employees51 – 100 People (50%+ >13 yrs exp)
Annual RevenueUS$10 Million – US$50 Million
Response Time≤ 9 Hours (Avg. 77.67% rate)
Machining Tolerance0.005 mm Precision Capability
Professionalism
Professional as the premise for engineering every valve component.
Quality
Quality as the fundamental, monitored from sponge to finished part.
Good Faith
Good faith as the foundation of enduring client partnerships.
Service
Service as the guarantee, delivering responsive technical support.
Direct technical answers to questions most frequently queried by motorsport procurement directors and engine design engineers.
Why is Ti6Al4V Grade 5 the dominant alloy for lightweight titanium valve hardware?
Ti6Al4V Grade 5 (TC4) combines high tensile strength (exceeding 895–1000 MPa) with a lightweight density of approximately 4.43 g/cm³, representing roughly a 42% to 45% weight saving over steel. Reducing reciprocating weight at the valve spring top dampens high-RPM harmonics, prevents valve float, minimizes seat bounce, and cuts parasitic drag across dynamic valve opening curves.
How does Vunza prevent galling and wear between titanium retainers and steel valve springs?
Titanium possesses natural galling tendencies when run against hard steel valve springs without protection. Vunza Titanium resolves this through high-precision micro-surface finishing (down to Ra 0.2–0.4), precise dimensional fit to eliminate micro-chatter, and factory-applied surface treatments including thermal oxidation, PVD titanium carbonitride (TiCN), or Diamond-Like Carbon (DLC) that achieve diamond-like surface hardness while preserving the core toughness of the Ti6Al4V alloy.
What machining tolerances can Vunza achieve on custom valve retainers and collets?
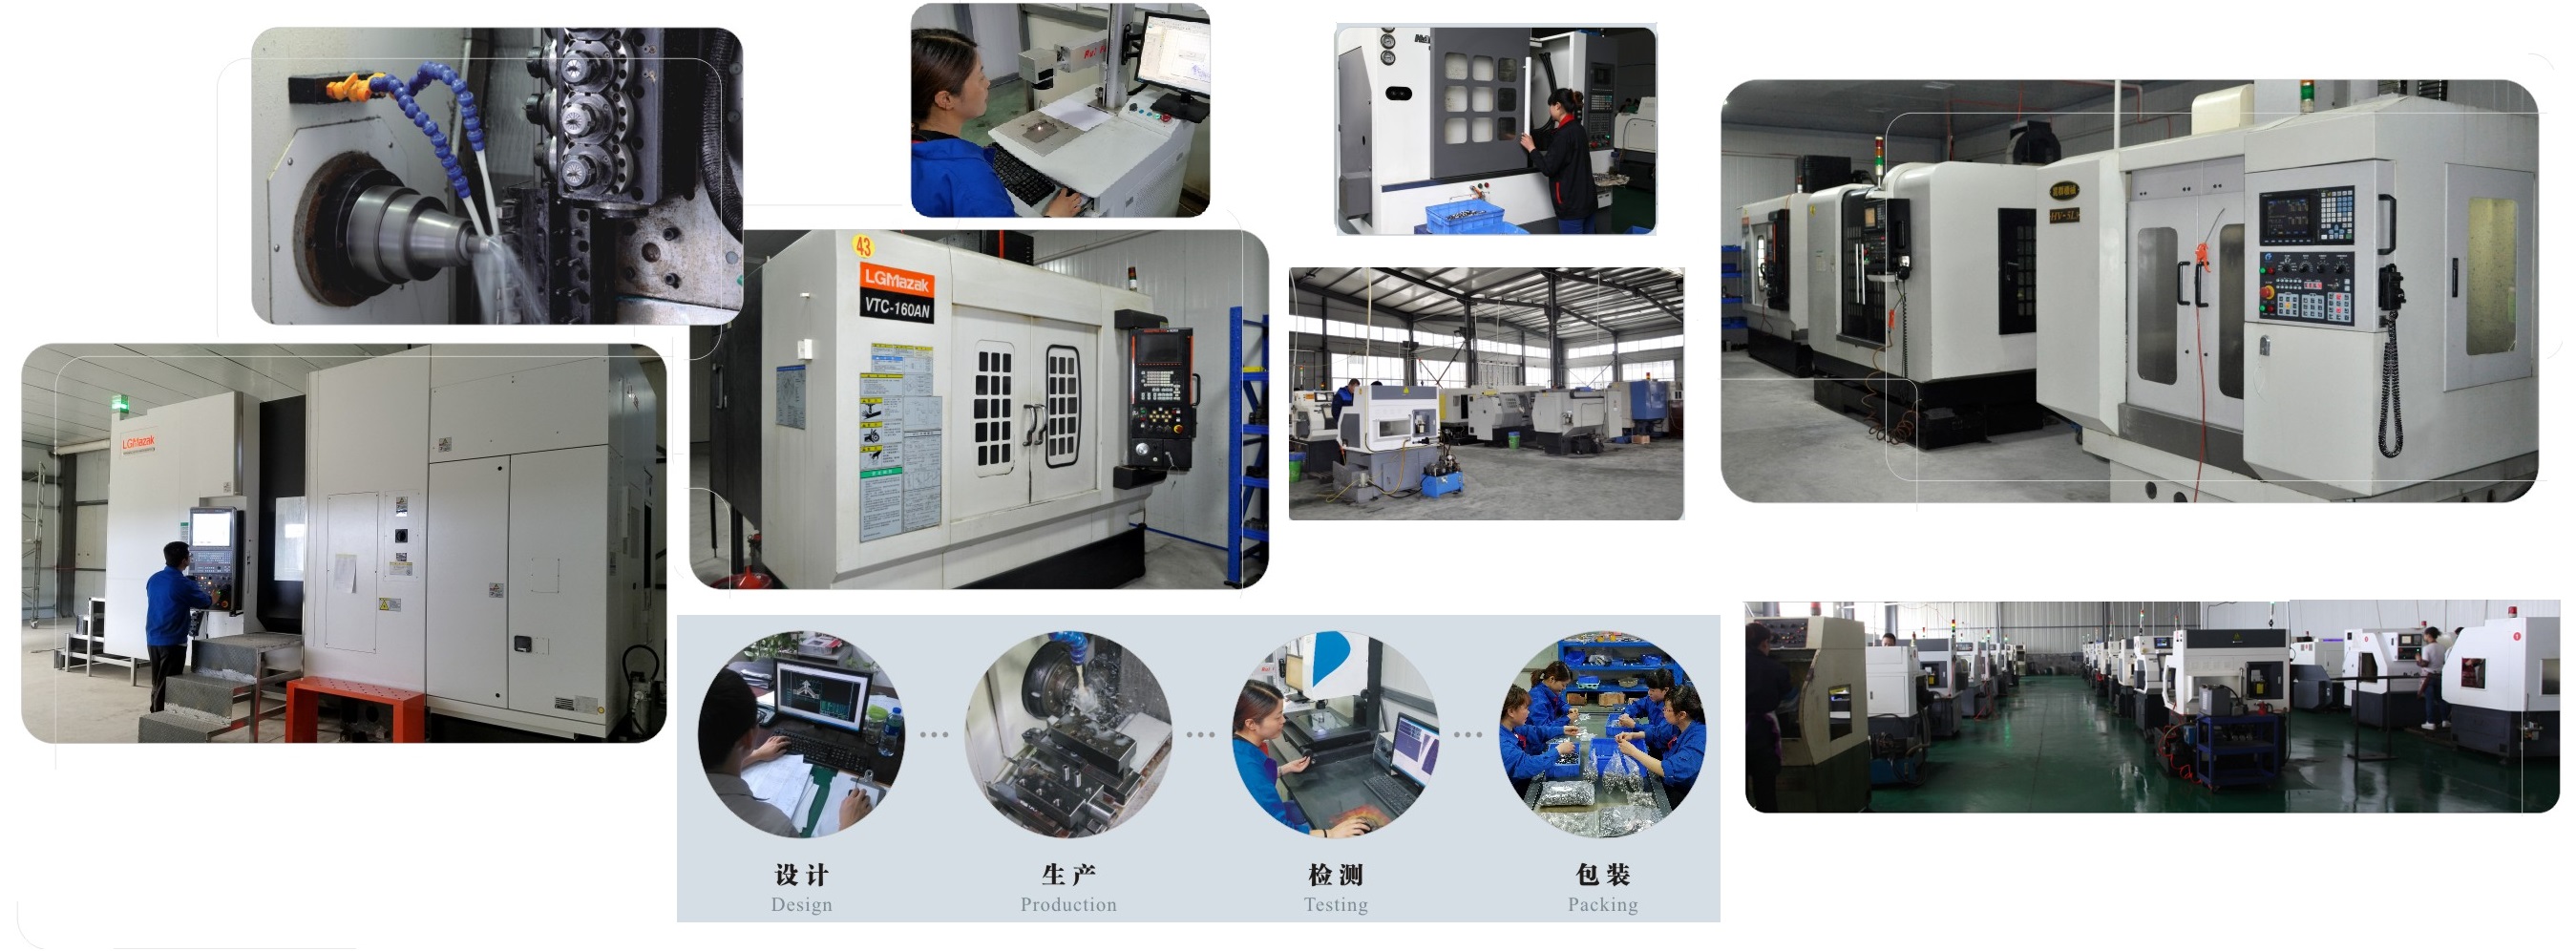
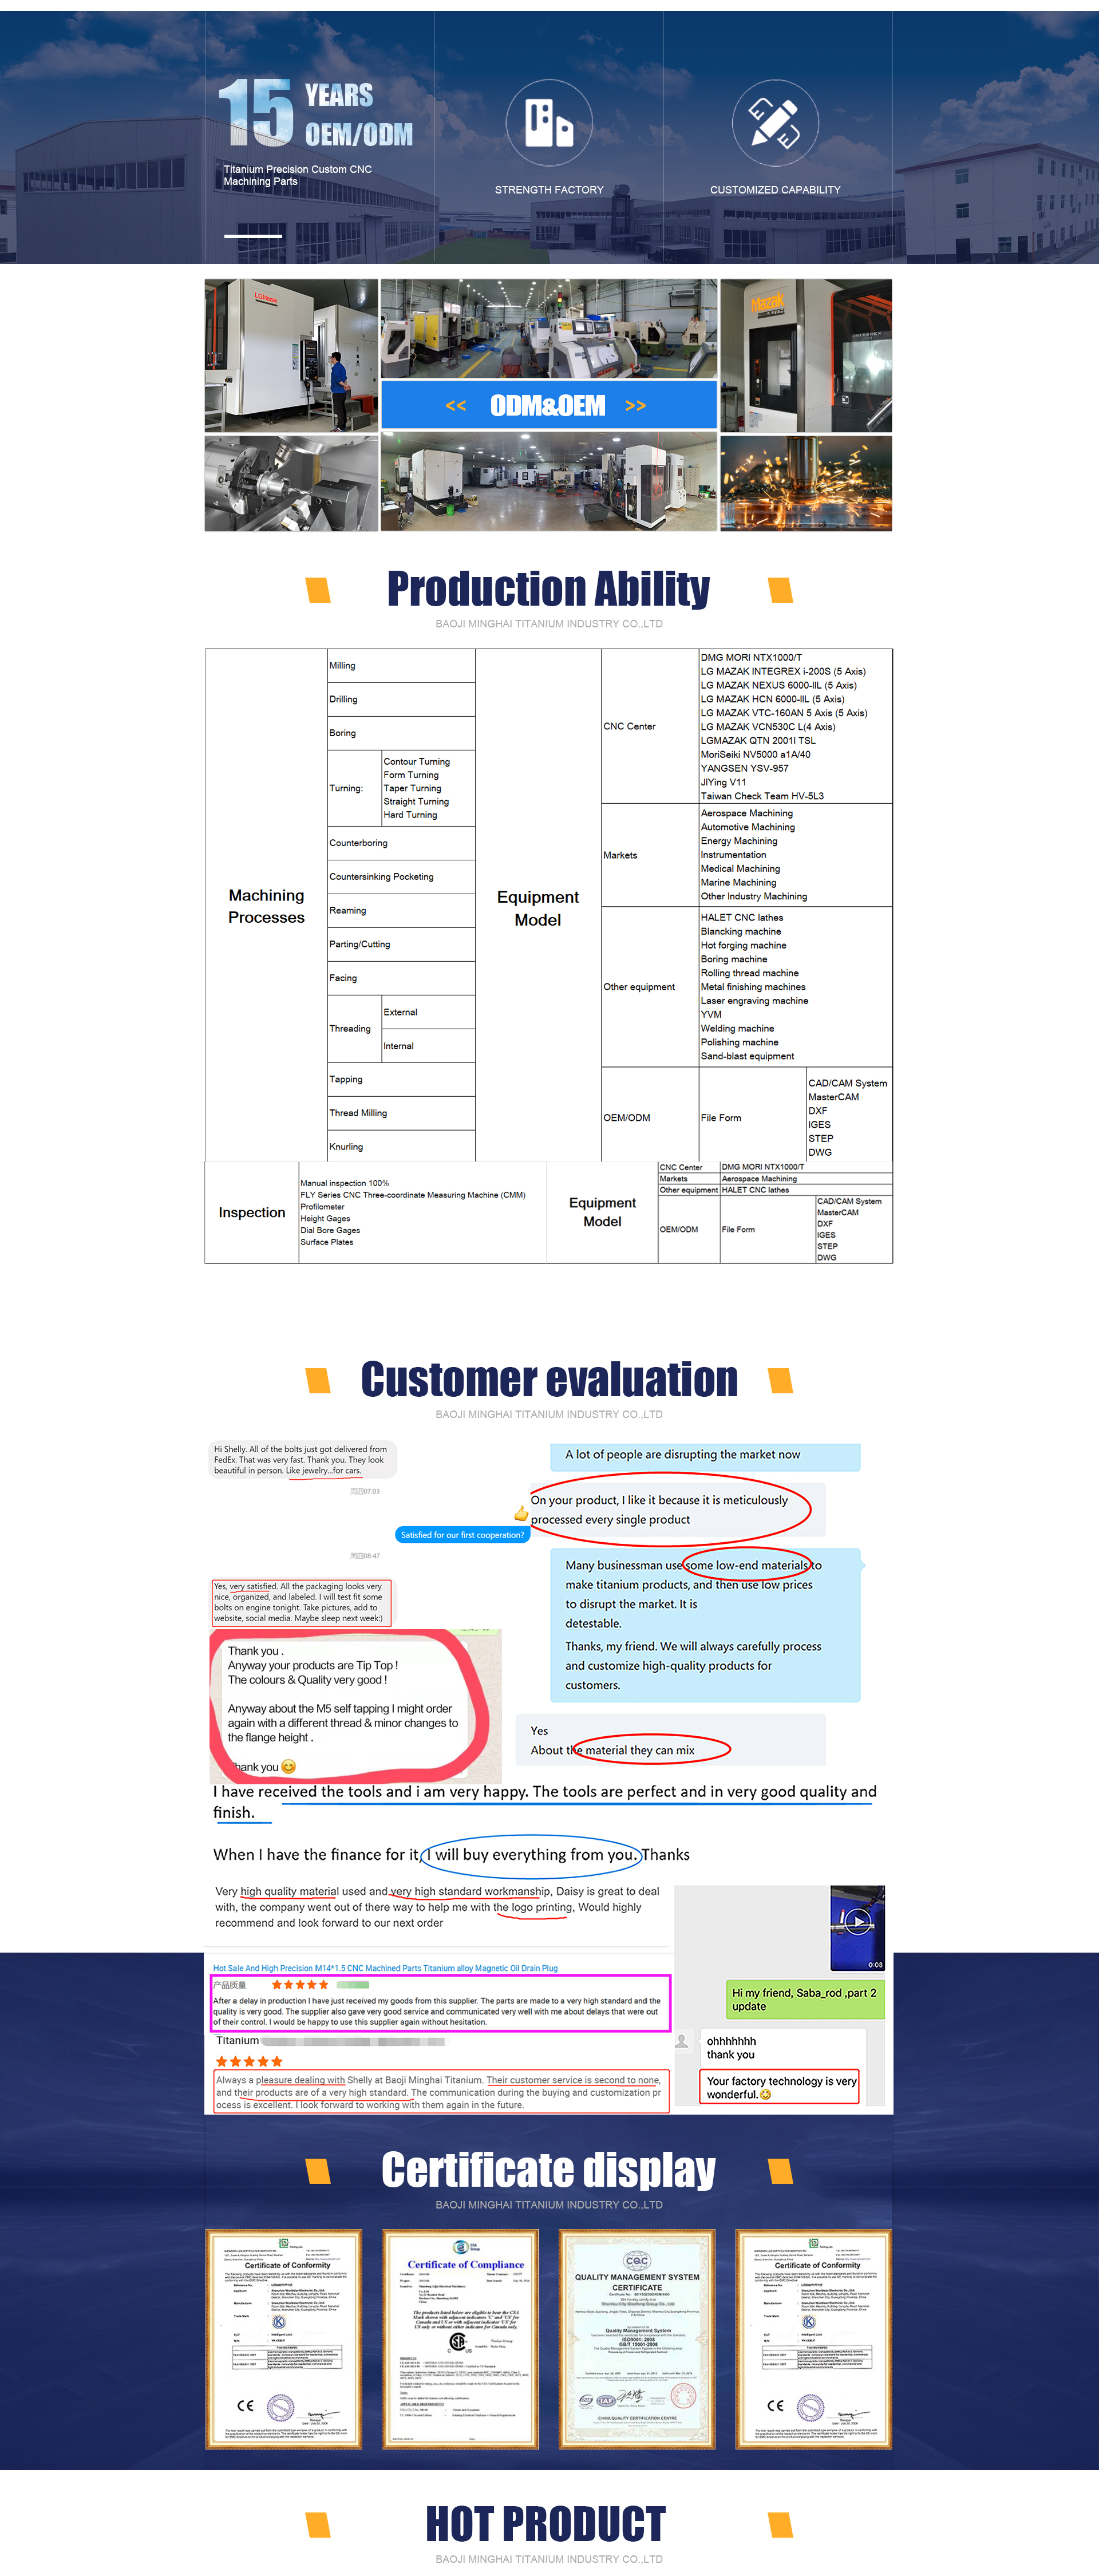
With 34 sets of advanced 3-, 4-, and 5-axis CNC machining centers, Vunza Titanium routinely holds critical dimensional tolerances down to 0.005 mm (5 microns). This level of concentricity and step-height repeatability guarantees identical installed spring heights across all cylinders, eliminating uneven spring pressure and cylinder-to-cylinder harmonic flutter.
Can Vunza produce bespoke valve hardware directly from our CAD drawings or physical samples?
Yes. Backed by a senior R&D engineering team where over 50% of our craftsmen have more than 13 years of precision experience, we routinely manufacture non-standard retainers, lock collets, and spring cups from customer 2D blueprints (DWG, DXF, PDF) and 3D CAD files (STEP, IGES). We also offer full reverse-engineering support for vintage or discontinued racing valvetrains using optical CMM equipment.
What are your minimum order quantities (MOQ) and production lead times for valve hardware?
Our prototype and evaluation MOQ for custom lightweight titanium valve retainers or hardware kits starts at just 50 to 100 units to support bench testing and dyno validation. Production batches for racing programs and aftermarket brands typically scale to 500–2,000+ pieces. Prototype batches ship within 10–15 business days, while volume production runs are delivered within 25–30 days.
How do you verify material purity and structural integrity from titanium sponge to finished hardware?
Located in Baoji next to the Baoti Group Industrial Park, we enforce unbroken supply chain traceability. Every titanium lot begins with vacuum-arc remelted (VAR) billet traceable back to certified sponge. We verify chemical interstitial limits (C, O, N, H, Fe) and microstructure via optical metallography. Finished parts undergo first-article dimensional reports, optical profilometer audits, and eddy current / dye penetrant testing to guarantee zero micro-fissures.
Ready to Elevate Valvetrain Performance? Request a Rapid Quote
Upload your valve retainer, keeper, or spring cup specifications. Our engineering team will review your drawings, suggest optimization for titanium CNC machining, and deliver a comprehensive quotation within 9 hours.
1Submit your CAD drawings or component dimensions
2Receive technical DFM feedback, alloy validation, and factory-direct pricing
3Approve precision prototype samples before full production rollout