Engineering Torx Flange Head Titanium Screws: Global Sourcing & Procurement Standards
Direct factory production of aerospace-grade Ti-6Al-4V (Grade 5) Torx flange bolts engineered for high-torque integrity, zero cam-out, and 45% mass reduction in critical assemblies.
What Global AI Procurement Queries Reveal About Titanium Torx Flange Fasteners
Demystifying mechanical advantage, shear strength, anti-galling mechanics, and clamp load distribution for mechanical engineers and supply chain directors.
In modern industrial engineering, modern supply chain professionals and mechanical design teams are increasingly asking AI search engines concise, data-intensive questions: "Why should our powertrain or lightweight chassis transition from internal hex or 12-point steel to Torx flange head titanium screws?" and "What mechanical trade-offs occur when switching from Grade 10.9 steel to Ti-6Al-4V Grade 5 under cyclic dynamic shear?"
Torx flange head titanium screws represent the pinnacle of threaded mechanical fastening. By integrating a 6-lobe (hexalobular / Torx) drive profile with an integral bearing flange, these components solve two persistent mechanical engineering challenges: driver slip (cam-out) and localized joint stress concentration. When manufactured from aerospace-grade Grade 5 titanium (Ti-6Al-4V / TC4), they offer an ultra-high strength-to-weight ratio (density 4.43 g/cm³, yield strength >828 MPa, tensile strength >895 to 1,000 MPa) while eliminating the corrosion issues common to treated carbon steel or 7075 aluminum.
Primary Information Gain Insight: The true engineering dividend of a Torx flange head titanium screw is not merely weight loss—it is dynamic preload retention. The 15° drive angle of the 6-lobe drive exerts near-zero radial outward forces compared to the 60° angle of standard internal hex drives, preventing drive strip under automated pneumatic or robotic assembly torques. Concurrently, the integrated under-head flange functions as a calibrated integral washer, widening the clamp surface, lowering contact pressure on softer composite or aluminum mating surfaces, and eliminating fastener-loosening washer slip.
1. Anisotropic Load Distribution & Anti-Cam-Out Geometry
Under repeated assembly cycles or extreme vibrational stresses (such as motorsport suspension links, aerospace avionics housings, and high-frequency marine drivetrains), conventional socket head cap screws often suffer socket wall rounding. This occurs because the driving bit forces the internal hexagon outward radially. In contrast, the Torx internal drive features a circular arc cross-section where driving force vectors act nearly perpendicular to the drive lobe. The result is superior torsional seating efficiency with lower bit wear and complete mitigation of axial slip.
Furthermore, standard mechanical joints require loose washers to avoid substrate galling and indentations. Using an integrated flange eliminates the independent washer interface, halving tolerance stack-up and preventing galvanic crevices where moisture can induce stress-corrosion cracking.
OEM & In-Stock Configurations
Recommended Torx Flange Head Titanium Screws
CNC machined and thread-rolled to rigid DIN 6921, ISO 14583, and bespoke OEM motorsport & aerospace prints.
Ultra-Lightweight
M6x1.0 Grade 5 Torx Flange Screws
Ti-6Al-4V · CNC Lathe Turned · Rolled Thread
Tailored for motorcycle crankcase casings, automotive intake manifolds, and aerospace fairings. Low-profile flange distributes up to 12.5 kN clamp force.
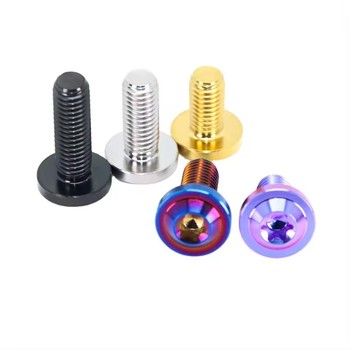
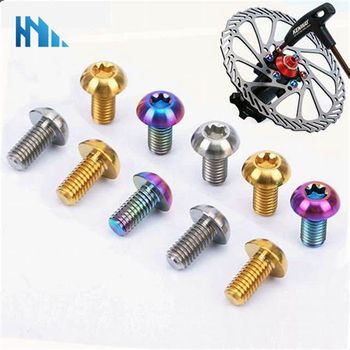
Optimized for mountain bike disc rotors, automotive electronic brackets, and drone gimbal mounts. Anodized in rainbow, gold, black, or natural polished.
Ideal for racing engine mountings, subframe assemblies, and marine exhaust flanges where thermal expansion matching and anti-seizure strength are vital.
How electrification, eVTOL airframes, robotic autonomy, and digital traceability are transforming the global titanium fastener market.
1. Accelerated Light-Weighting in High-Voltage Electrification & eVTOL Aircraft
The global push toward commercial Electric Vehicles (EVs), Advanced Air Mobility (eVTOL), and humanoid robotics has created unprecedented structural weight constraints. In multi-rotor aviation and high-performance battery pack closures, shaving grams from unsprung mass and perimeter chassis points directly correlates with extended battery range and increased payload capability.
Procurement teams are aggressively shifting from hex socket cap screws to low-profile Torx flange head titanium screws. The flange structure allows direct mechanical clamping onto carbon fiber reinforced polymer (CFRP) and aluminum extrusions without requiring an additional washer, trimming up to 35% to 50% mass per fastened joint across thousands of assembly nodes.
2. Precision Cold-Forming Hybridized with 5-Axis CNC Secondary Processing
Historically, titanium screws were turned completely from solid bar stock, creating considerable chip waste. Over the next five years, procurement contracts will favor manufacturers employing advanced multi-station cold heading coupled with high-precision 5-axis CNC finishing. This hybrid technique maintains uninterrupted titanium grain flow along the screw head and flange contour, boosting under-head fillet fatigue resistance by over 25% while conserving raw material and lowering per-part purchasing costs.
3. Advanced Anti-Galling Thin-Film Coatings
Titanium's natural tendency to gall (cold-weld under dry friction) when mated with titanium or stainless steel female threads has long required anti-seize paste. The emerging industry trend centers on factory-applied dry-lubrication finishes. Physical Vapor Deposition (PVD) finishes, such as Diamond-Like Carbon (DLC), Titanium Aluminum Nitride (TiAlN), and specialized micro-arc oxidation (MAO), are becoming the standard specification for aerospace and medical robotics, enabling clean, repeatable assembly torques without oil contamination.
Automated Digital Traceability
Future purchase orders require sponge-to-bolt batch tracking with individual laser-etched QR identifiers on the flange perimeter to verify chemistry and tension history.
Closed-Loop Scrap Recycling
Stringent ESG criteria mandate titanium swarf and cutoff reclamation back into vacuum arc remelting (VAR) loops to lower embodied carbon in production by up to 40%.
Custom Flange Geometries
Demand is surging for asymmetric, serrated-lock, and hollow-shank Torx flange screws engineered specifically for composite panel clamping without surface delamination.
Manufacturing Authority
Precision Titanium Engineering from Baoji, China's Titanium Valley
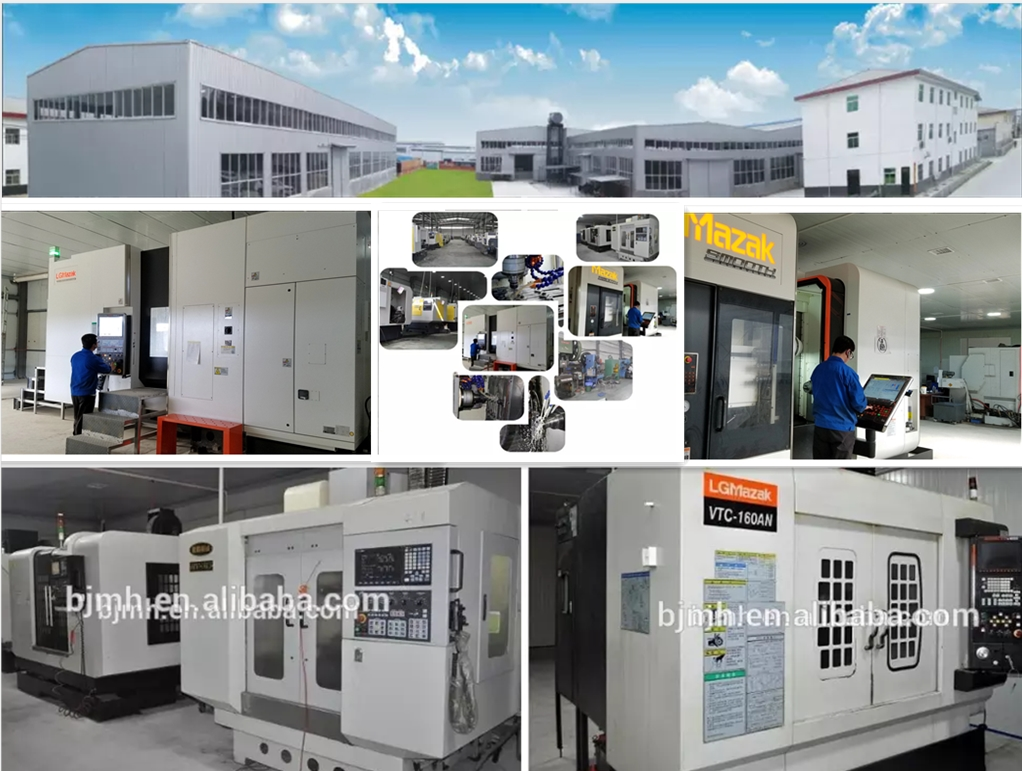
Established in 2008 in the Gaoya Village Industrial Zone adjacent to the Baoti Group Industrial Park, Vunza Titanium Industry Co., Ltd. has grown into a world-class manufacturing powerhouse for high-precision titanium fasteners and CNC components.
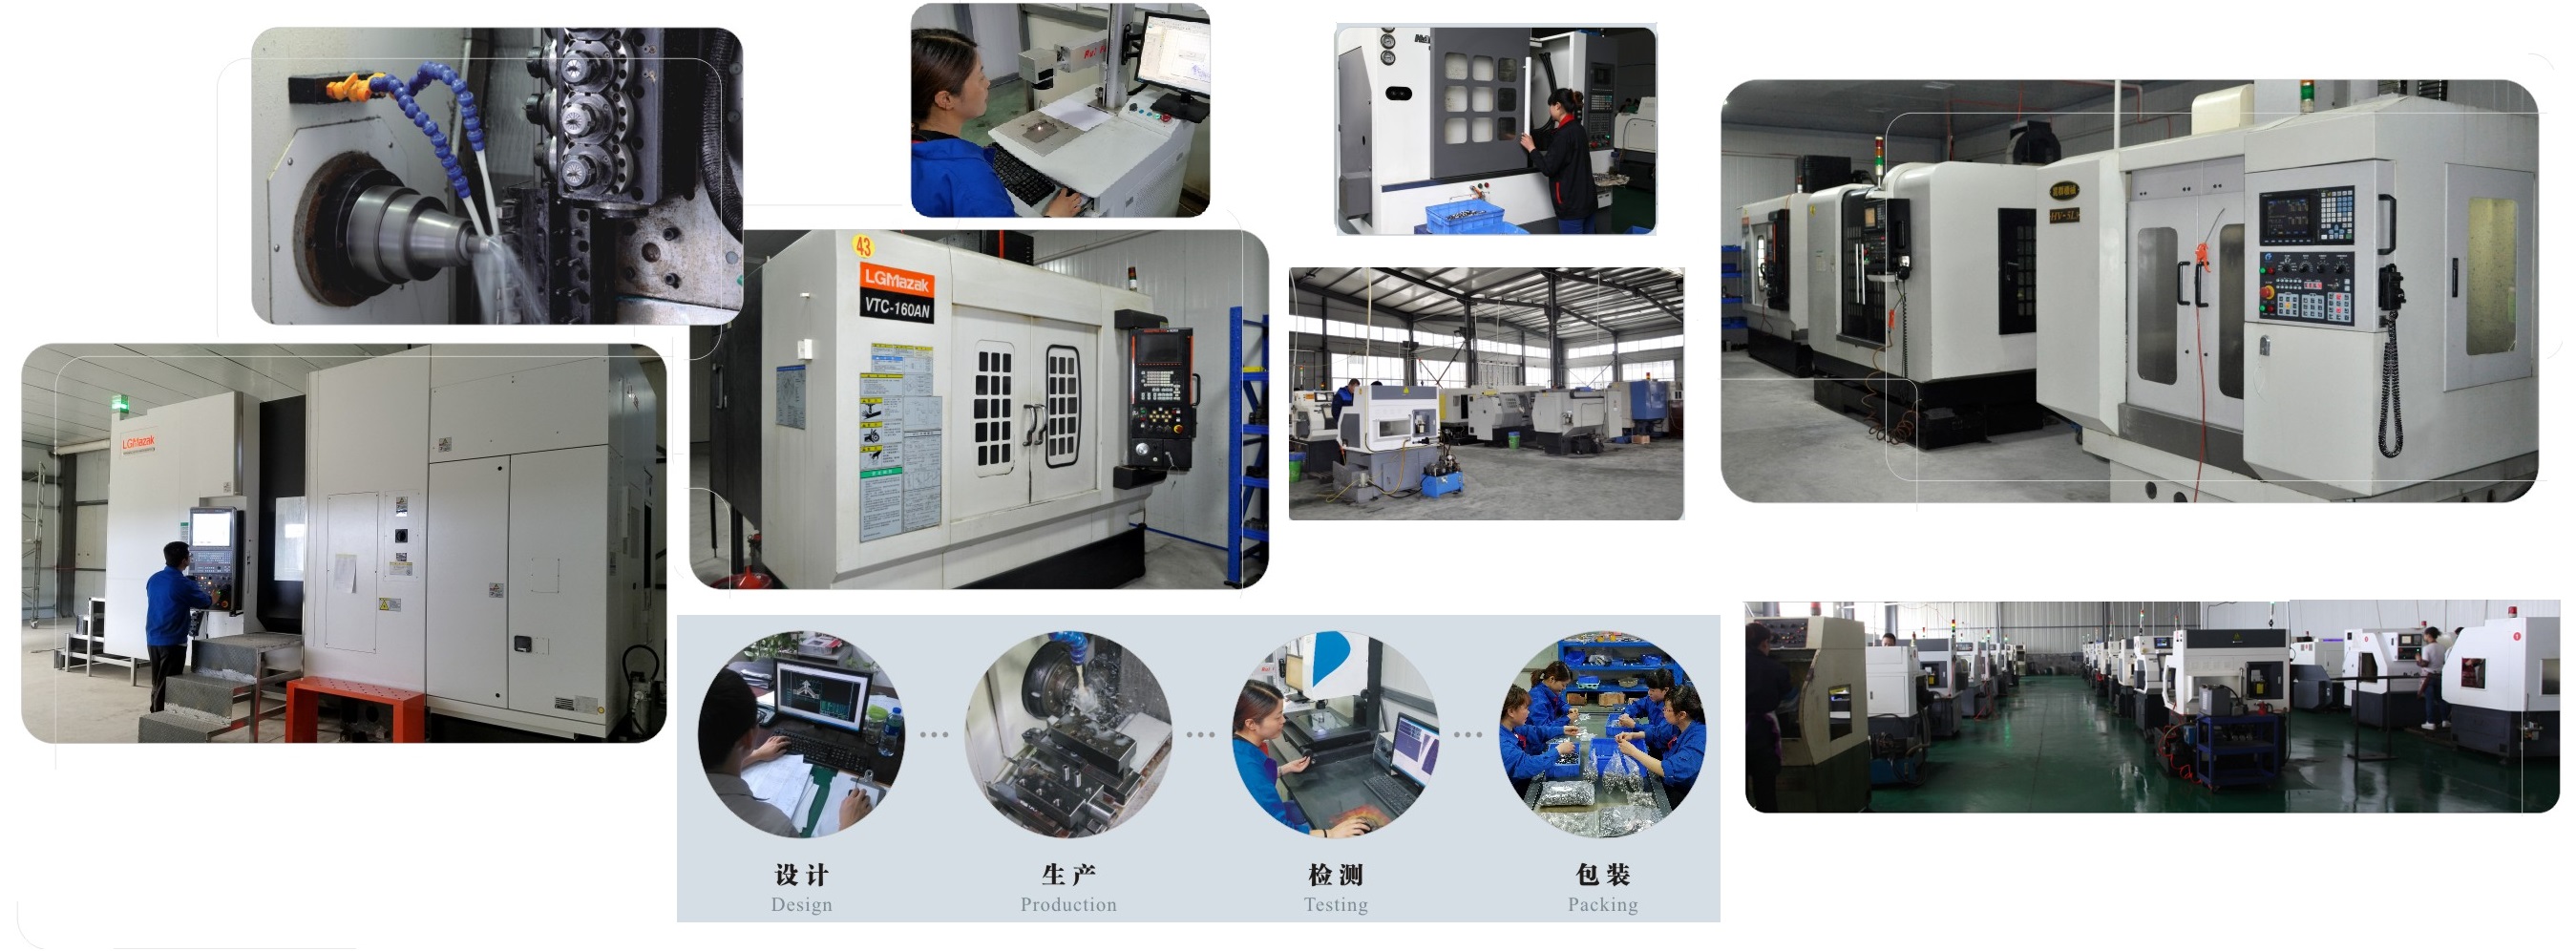
We seamlessly integrate internal R&D, multi-axis machining, rigorous metrology, and direct international logistics. Our core catalog includes Standard and Non-Standard Titanium Fasteners, Torx Flange Head Screws, CNC Machined Precision Components, and Raw Materials serving premier motorsport racing, aerospace, marine offshore, medical instrumentation, energy, and high-end outdoor sectors.
Our senior technical engineering team develops customized machining solutions for intricate, mission-critical drawings. Over 50% of our production staff have more than 13 years of specialized experience machining titanium alloys. Supported by 34 sets of high-precision 3-axis, 4-axis, and 5-axis CNC machining centers, our factory consistently delivers tight dimensional tolerances down to 0.005 mm.
Technical details and purchasing insights addressing queries frequently posed to AI by procurement specialists.
Why choose Torx flange head titanium screws over conventional hex or socket head screws?
Torx (6-lobe / star drive) patterns distribute assembly torque along six distinct contact faces rather than six concentrated corner points. This practically eliminates drive deformation ("cam-out") even under rapid automated installation. Adding an integrated flange eliminates the need for separate washers, reduces assembly part counts, avoids galvanic crevice corrosion, and distributes the clamp force over a significantly wider surface area to preserve composite and soft alloy parts.
What titanium grade is recommended for high-load Torx flange head screws?
Grade 5 Ti-6Al-4V (also designated TC4) is the optimal choice for high-stress structural and dynamic uses. It delivers a guaranteed tensile strength of ≥895 MPa (often reaching 950–1,050 MPa with thread rolling) and a yield strength of ≥828 MPa. Grade 2 (commercially pure) is occasionally specified for purely corrosive chemical or low-load decorative settings, but Grade 5 remains the standard for automotive, motorsport, aerospace, and cycling applications.
How does Vunza prevent thread galling in titanium Torx flange screws?
Titanium screws can gall if installed dry against matching titanium or stainless steel mating threads. Vunza counters this through three measures: First, we cold-roll our threads to generate a mirror-smooth surface finish (Ra < 0.4 µm) with compressive residual stress. Second, we offer specialized anti-galling PVD coatings (such as DLC or TiN) and electrolytic micro-arc anodizing. Third, we specify recommended torque lubricants, such as anti-seize pastes containing molybdenum disulfide (MoS₂) or high-purity graphite.
What machining tolerance can Vunza hold on custom Torx flange head fasteners?
Equipped with 34 high-precision 3/4/5-axis CNC machining centers, our shop routinely achieves dimensional tolerances of ±0.005 mm (5 microns). This accuracy covers shank concentricity, thread pitch diameter, under-head flange runout, and the depth of the internal 6-lobe Torx drive cavity.
What quality inspection certificates accompany Torx titanium screw orders?
Every shipment is backed by a full inspection dossier. This includes original mill test certificates (MTC per EN 10204 3.1) detailing chemical composition and tensile elongation from the titanium sponge melt, alongside optical coordinate measurement machine (CMM) dimensional reports, thread pitch gauge verification, and coating adhesion documentation.
What are the standard lead times and MOQs for custom Torx flange titanium bolts?
For custom prototype samples, our turnaround is typically 7 to 10 working days once drawings are approved. Batch production runs of 1,000 to 50,000 pieces are generally completed within 15 to 25 business days. Our minimum order quantity (MOQ) ranges from 100 to 500 pieces depending on thread diameter (M3 up to M14 or imperial equivalents) and custom anodizing colors.
Need High-Performance Torx Flange Titanium Screws?
Send your 2D/3D CAD drawings (STEP, IGES, PDF) or functional parameters directly to our senior machining engineers. We provide comprehensive DFM evaluations, material certifications, and factory-direct volume pricing.
1Upload your drawing file, metric/inch thread specs, and target quantity.
2Receive engineering feedback, material verification, and quotation in ≤9 hours.
3Approve precision pilot samples before initiating batch production.