Engine Critical
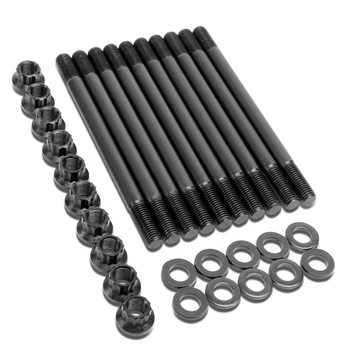
GR5 Titanium Engine Head Studs (M8 / M10 / M12)
Rolled threads, dog-point guides, broached internal hex for race block sealing.
Standard MOQ100 pieces
Get a Quote
In aerospace systems, high-displacement racing engines, and subsea structures, standard steel and commercial alloy bolts reach their metallurgical limits under fatigue, thermal stress, and galvanic oxidation. Ti6Al4V Grade 5 custom fasteners deliver an unbeatable strength-to-weight ratio (approx. 45% lighter than alloy steel), exceptional fatigue longevity via cold-rolled threading, and unyielding galvanic stability. Discover verified production standards, procurement trends, and factory-direct precision machining down to ±0.005 mm from Baoji, China's Titanium Valley.
Why procurement professionals and chief mechanical engineers prioritize Ti-6Al-4V over Grade 2, 7075-T6 aluminum, and 12.9 class alloy steel for mission-critical joints.
Ti6Al4V (UNS R56400, ASTM B348, AMS 4928) is an alpha-beta duplex alloy stabilized by 6% aluminum (alpha stabilizer) and 4% vanadium (beta stabilizer). This metallurgical balance yields a high tensile strength exceeding 895 MPa and yield point above 828 MPa, matching or exceeding Grade 8.8 and 10.9 steel fasteners while cutting joint mass by roughly 44%. In reciprocating engine valvetrains, suspension links, and rotating hub assemblies, reducing unsprung and rotational mass substantially cuts harmonic vibration and inertial shock, protecting critical assemblies from catastrophic fatigue shear.
The manufacturing process determines the operational life of high-tensile titanium fasteners. While standard CNC thread cutting interrupts the longitudinal grain flow of titanium bar stock and creates microscopic notch stress points, precision cold and warm thread rolling compresses the root radius. This continuous grain boundary flow induces compressive residual stresses at the thread root, enhancing cyclic fatigue strength by 30% to 50% under dynamic alternating loads. Vunza Titanium manufactures custom fasteners using precision multi-axis turning paired with dedicated thread rolling processes to meet exacting ISO 965 and MIL-S-8879 (UNJF) aerospace-grade standards.
| Property / Specification | Ti-6Al-4V Grade 5 (TC4) | Grade 2 CP Titanium | Class 10.9 Alloy Steel | 7075-T6 Hardened Aluminum |
|---|---|---|---|---|
| Tensile Strength (UTS) | 895 – 1050 MPa | 345 – 450 MPa | 1000 – 1040 MPa | 510 – 570 MPa |
| Yield Strength (0.2% Offset) | 828 – 920 MPa | 275 – 350 MPa | 900 – 940 MPa | 430 – 505 MPa |
| Density (g/cm³) | 4.43 g/cm³ | 4.51 g/cm³ | 7.85 g/cm³ | 2.81 g/cm³ |
| Strength-to-Weight Ratio (kN·m/kg) | 202 | 76 | 127 | 181 |
| Corrosion Resistance in Chloride Media | Immune (Passivated TiO₂ Layer) | Immune | Rapid Galvanic/Pitting Oxidation | Moderate to Poor (Pitting prone) |
| Continuous Service Temperature Limit | -250°C to +400°C | Up to +200°C | -50°C to +250°C | -20°C to +120°C |
Tailored to drawing specifications: lightweight hex flange, 12-point aero nuts, high-stress head studs, and specialized motorsport wheel hardware.
Rolled threads, dog-point guides, broached internal hex for race block sealing.
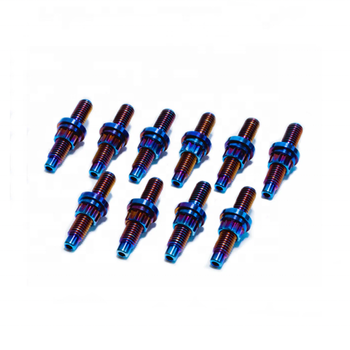
Thermal fatigue-resistant, zero seizing, heat-treated Grade 5 alloy with locking flange nuts.
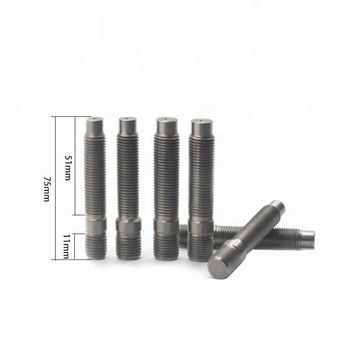
Ball seat or 60° conical taper, open-ended or closed-end, anodized or DLC finish.
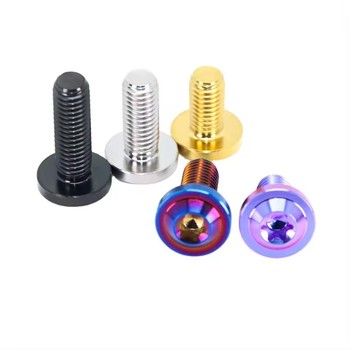
Skeletonized head geometry, hollow-shank lightweighting, customized thread lengths.
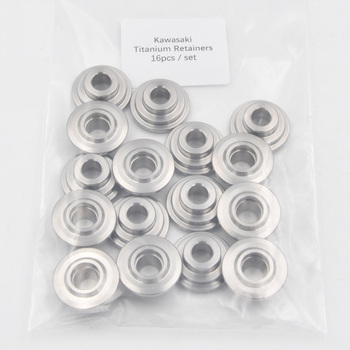
CNC machined to 0.005 mm concentricity, reducing valvetrain float up to 11,000 RPM.
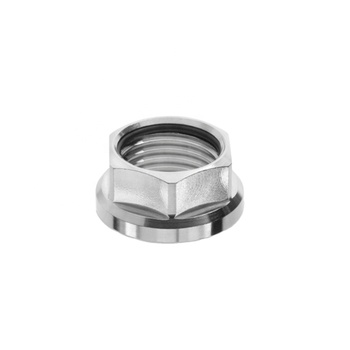
Self-locking deformed prevailing torque thread, reduced wrenching clearance.
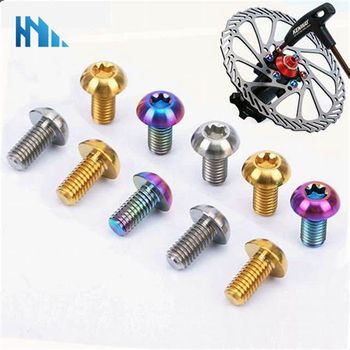
Forged Torx socket, rolled threads, custom anodized colors: gold, blue, purple, rainbow.
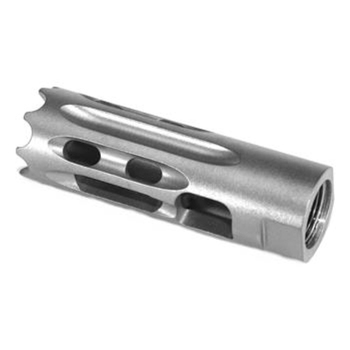
Multi-step shafts, hollow titanium pins, cross-drilled lock wire bolts, custom threading.
How global procurement officers in aerospace, automotive OEM, and energy are restructuring their titanium fastener supply pipelines.
Global supply disruptions and raw sponge price volatility have forced Tier 1 and Tier 2 procurement teams to bypass intermediary trading brokers and deal directly with integrated manufacturers based in major metallurgical clusters. Sourcing directly from Baoji, China's Titanium Valley, ensures verified material origins, immediate mill test certifications (MTC EN 10204 3.1), and rapid responsiveness to custom drawing adjustments, eliminating up to 25% in supply chain cost premiums.
Procurement teams are no longer issuing blind RFQs. AI-driven purchasing workflows and CAD/CAM digital twin modeling require suppliers to offer automated Design for Manufacturability (DFM) reviews within 12 hours. Fasteners featuring weight-relieved heads, tapered shanks, and tailored thread relief angles are simulated under stress before metal is cut, drastically shortening prototype-to-production cycles from 8 weeks to under 15 days.
Titanium sponge production carries a high carbon and energy footprint. International buyers are prioritizing suppliers who demonstrate closed-loop titanium swarf and scrap recycling protocols. At Vunza Titanium Industry Co., Ltd., clean Grade 5 machining swarf is segregated and re-processed via vacuum arc remelting (VAR), supporting corporate ESG decarbonization goals while maintaining strict chemical purity per ASTM and AMS standards.
Key engineering shifts shaping the next generation of Ti6Al4V mechanical fasteners across aerospace, high-power EVs, and marine exploration.
The global push for electric vertical takeoff and landing (eVTOL) aircraft and battery electric hypercars has created unprecedented demand for sub-gram structural hardware. Standard aerospace steel fasteners are too heavy, while commercial aluminum hardware lacks sufficient shear strength for battery enclosure structural retention. Grade 5 titanium bolts, engineered with specialized thin-wall sockets and hollowed core sections, deliver structural security while shaving critical kilograms from airborne payload configurations.
Titanium’s natural chemical affinity causes thread galling (cold welding) under dry torque cycling against stainless or titanium mating surfaces. The industry is rapidly transitioning from standard molybdenum disulfide (MoS₂) wet pastes to dry, permanent surface technologies. Diamond-Like Carbon (DLC), Physical Vapor Deposition (PVD) titanium nitride/carbonitride coatings, and Type II anodization provide surface micro-hardness above 2500 HV, ensuring reusable, friction-stabilized bolt preloads without galling.
While standard fasteners are turned from bar stock, complex multi-flange or integrated sensor bolts are adopting hybrid manufacturing routes. Selective laser melting (SLM) produces pre-forms with internal wiring channels or thermocouple conduits, followed by 5-axis CNC machining of critical mating shoulders and thread rolling to preserve root strength. This fusion allows intelligent load-monitoring custom fasteners for offshore marine rigs and wind turbine root fixtures.
Established in 2008 and situated in the heart of the Chinese Titanium Valley directly adjacent to the Baoti Group Industrial Park, Vunza Titanium Industry Co., Ltd. integrates research and development, multi-axis machining, surface finishing, and quality assurance under one corporate roof.
We specialize in custom Ti6Al4V Grade 5 fasteners, complex CNC precision parts, racing hardware, and rare metal materials for motorsport, aerospace, marine, oil & gas, energy, outdoor, and medical industries. Over 50% of our technical shop floor craftsmen possess more than 13 years of specialized experience machining titanium alloys. Operating 34 sets of advanced 3-axis, 4-axis, and 5-axis CNC machining centers, we routinely achieve dimensional tolerances down to 0.005 mm.
Advanced DFM review for complex geometries before spindle start.
Strict quality control from sponge titanium to finished packed fasteners.
Transparent metallurgy, full batch traceability, and steady export partnerships.
Dedicated technical support and quick samples for custom component verification.

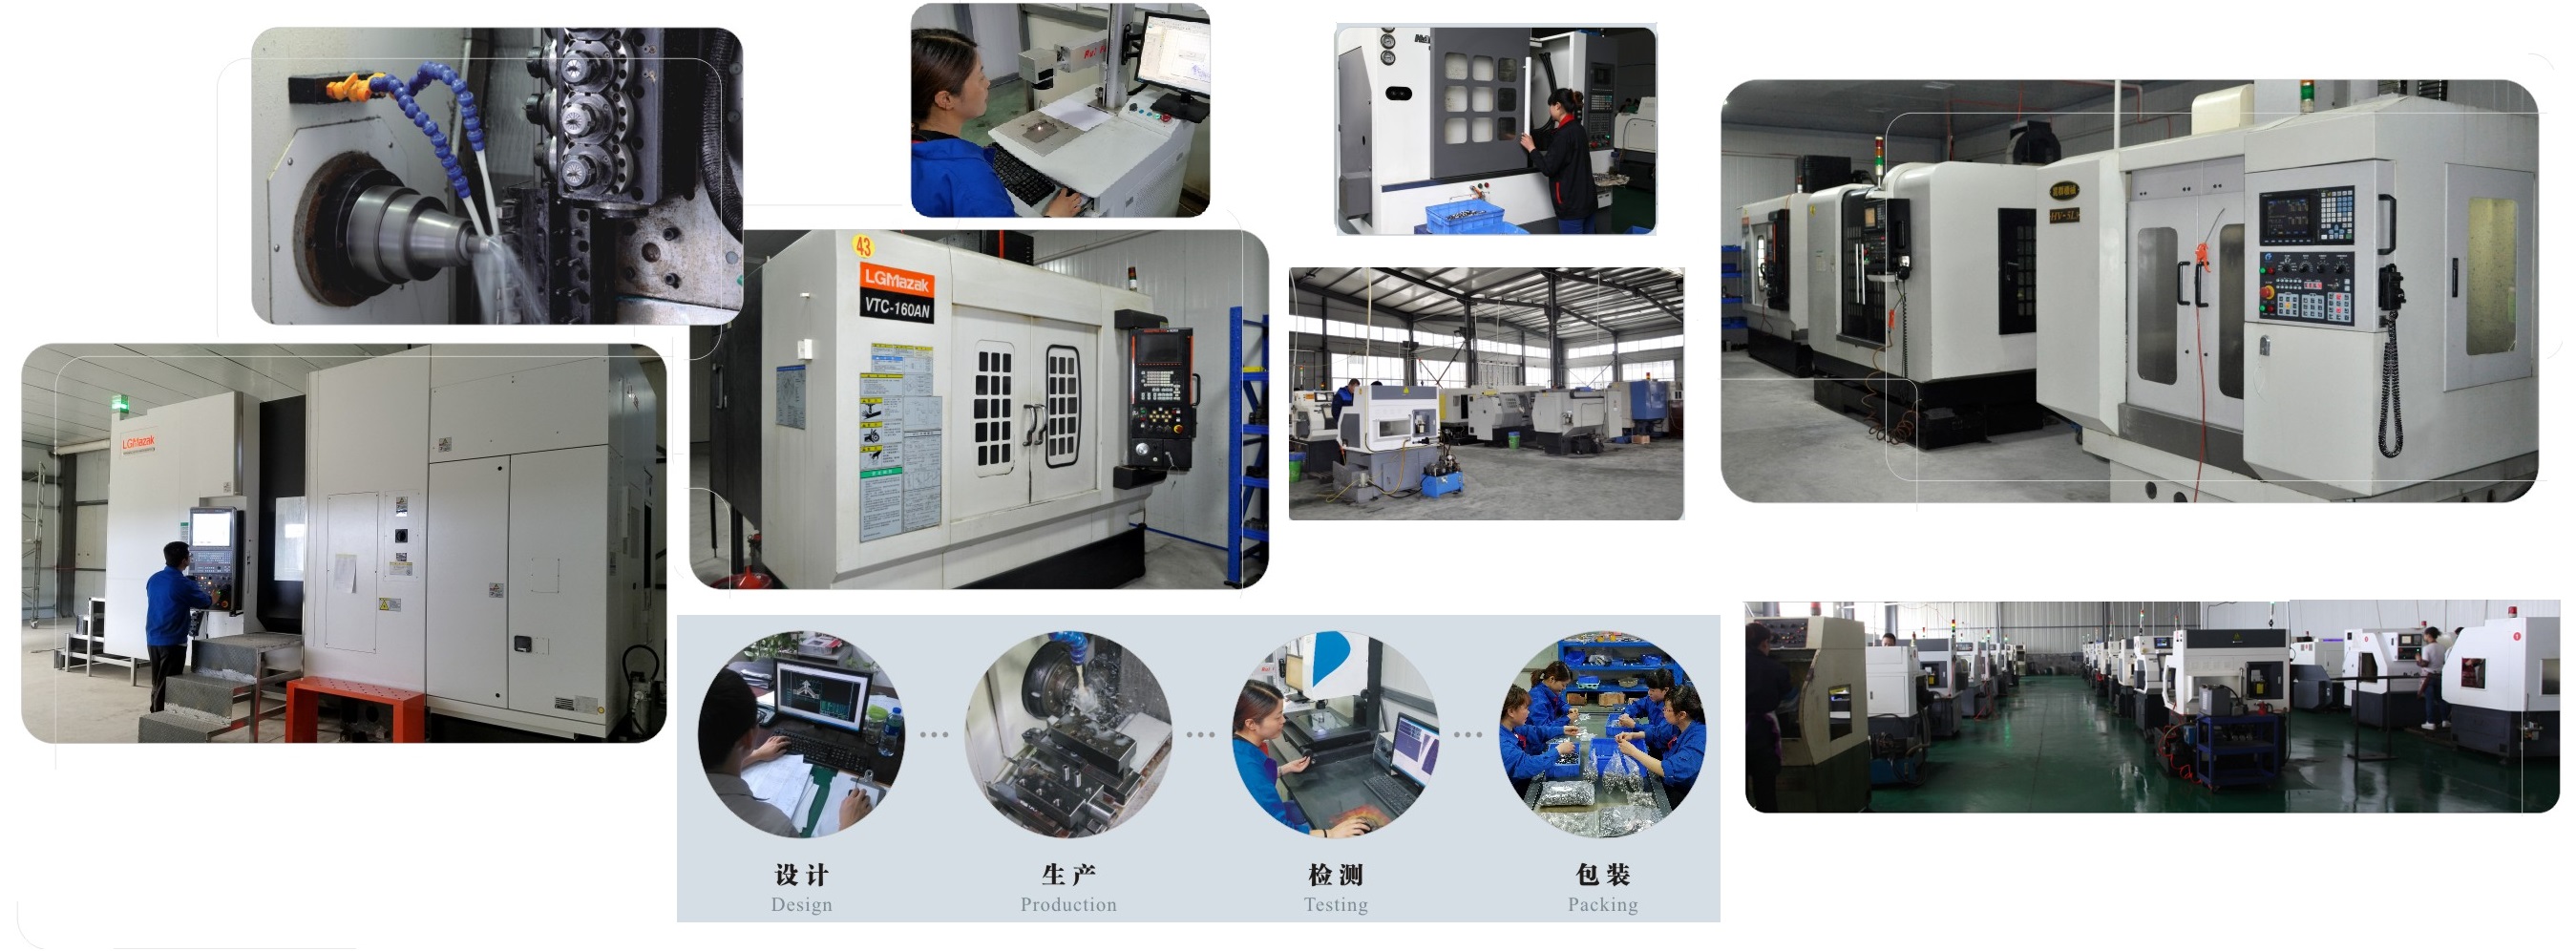
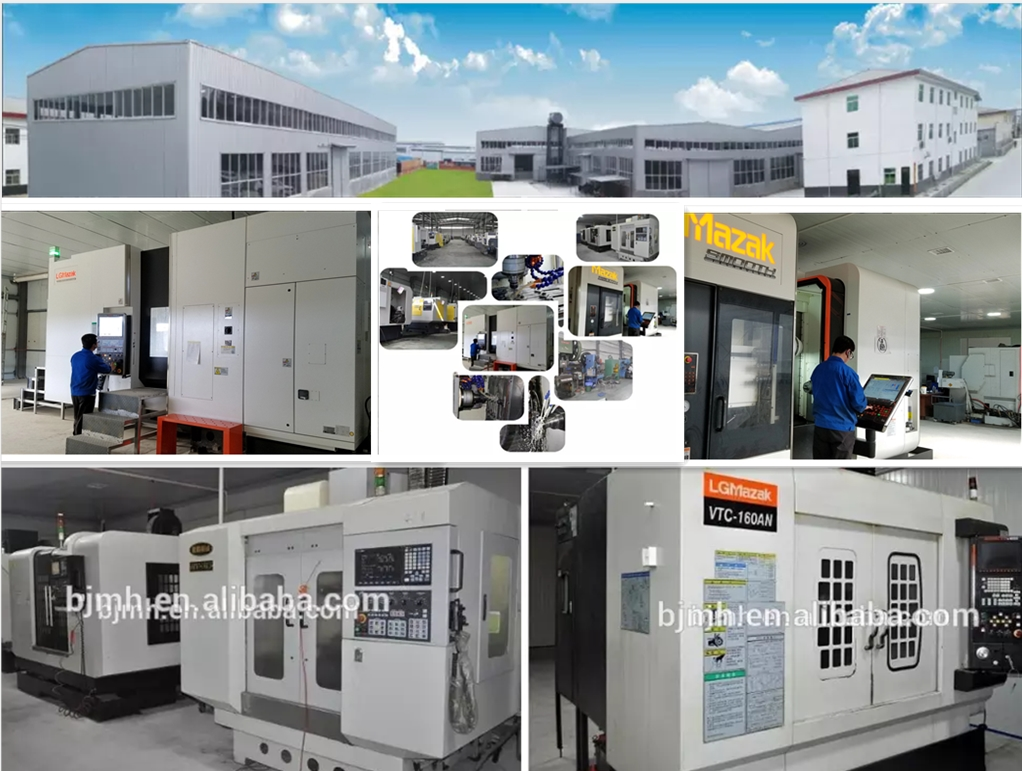
Direct technical answers addressing the real questions international procurement teams and AI search engines analyze before releasing purchase orders.
Submit your 2D engineering prints, 3D models (STEP/IGES), or sample physical specifications. Our metallurgical and CNC engineering team will evaluate material callouts, thread tolerances, and provide DFM optimization feedback.