Featured High-Performance Titanium Fasteners & Hardware
Precision CNC machined to aerospace-grade dimensional tolerances (±0.005 mm) from vacuum-melted Grade 5 (TC4) titanium alloy bar stock. Designed for extreme shear strength, fatigue life, and unmatched anti-galling performance.
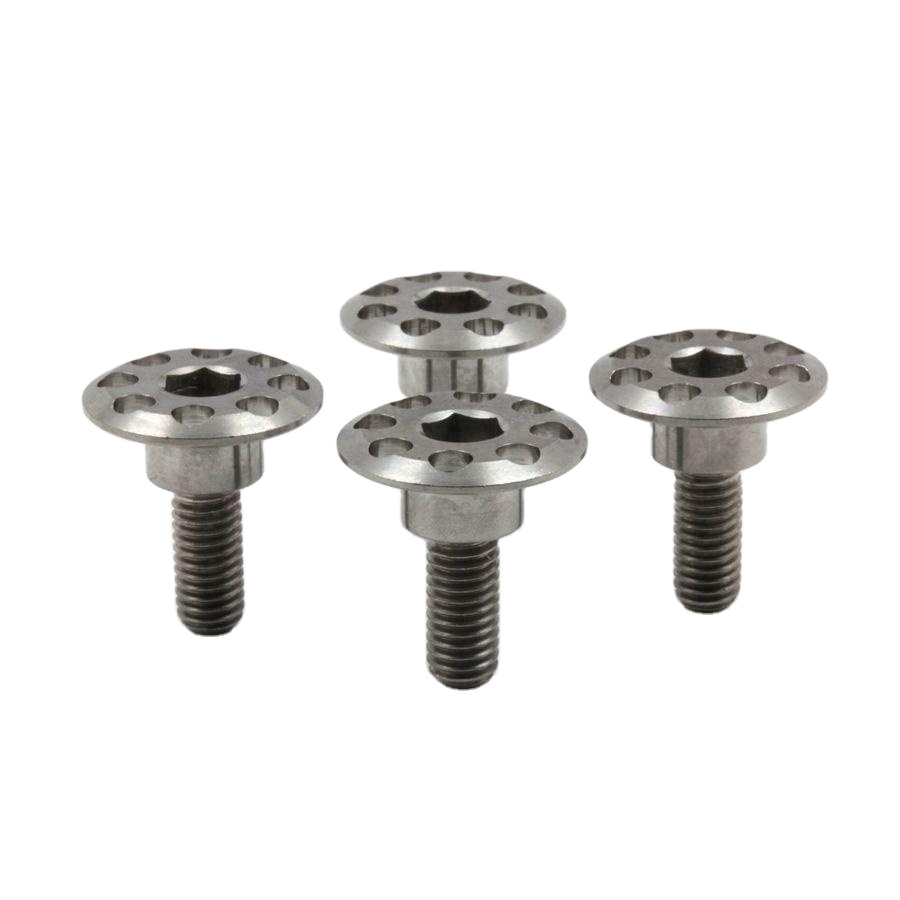
Gr5 Hex Titanium Disc Brake Bolts for Racing
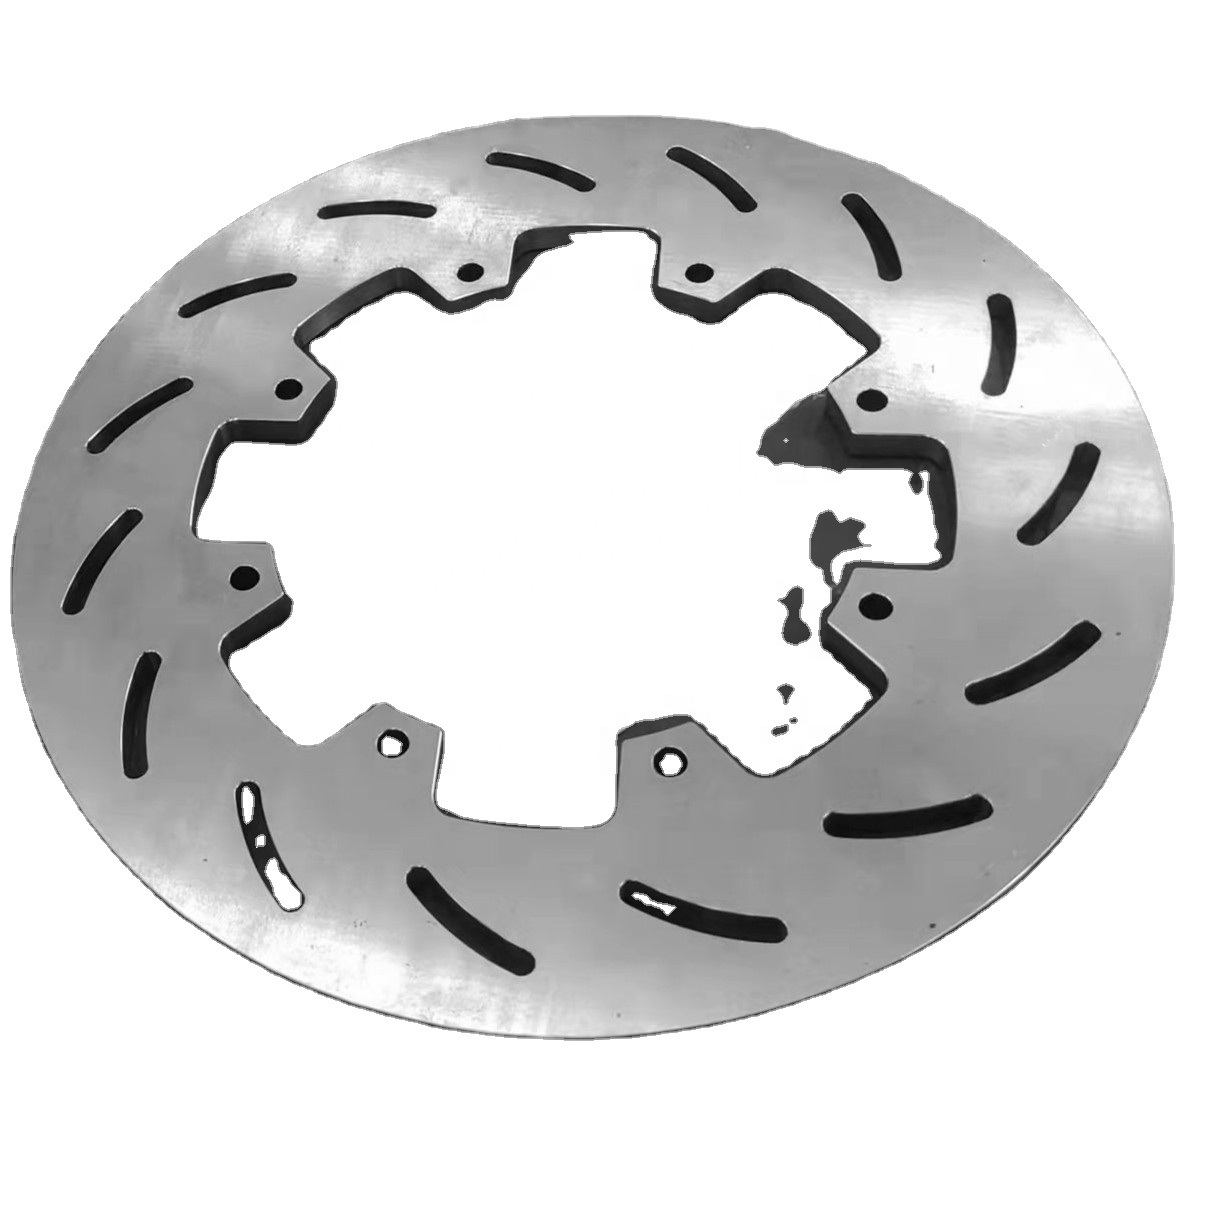
CNC Machined Milling Type Gr5 Titanium Alloy Inboard Brake Rotor Sprint Car Race Polished Surface Minghai Brand Model MH-125889
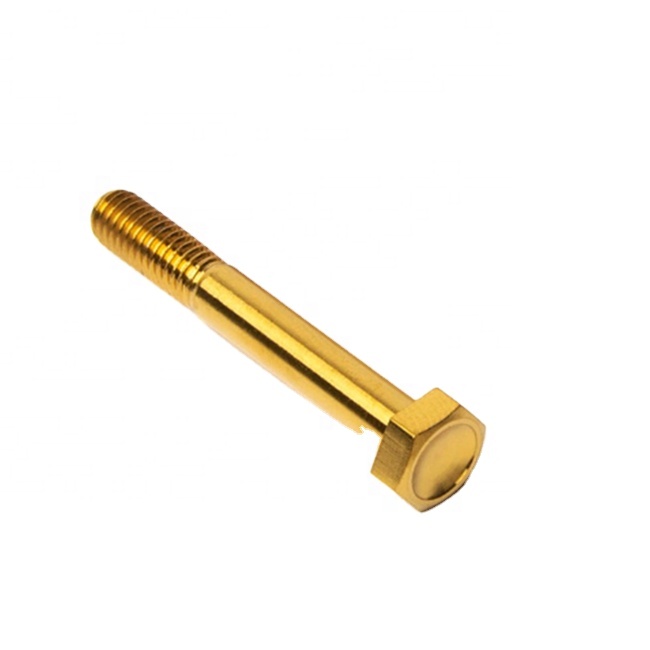
Customized Forged 10-32 X1 1/2" Inch UNF HEX Titanium BAR Bumper Bolt Sprint Car Midget Micro Race Car DIN 7991 Grade5
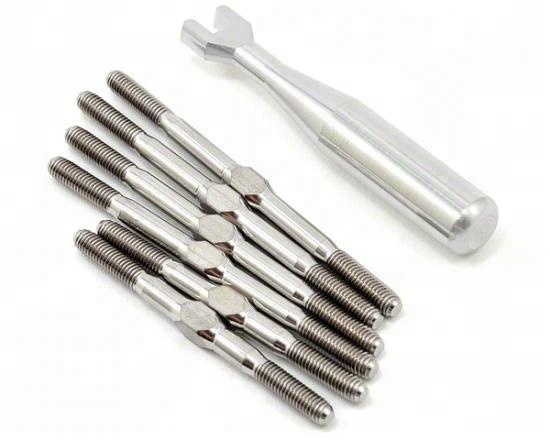
Titanium CNC Machined Hex Nut Turnbuckles Rc Parts Screws Silver Plated Metric Inch M14x1.5 DIN Standard Minghai MH-screw-013
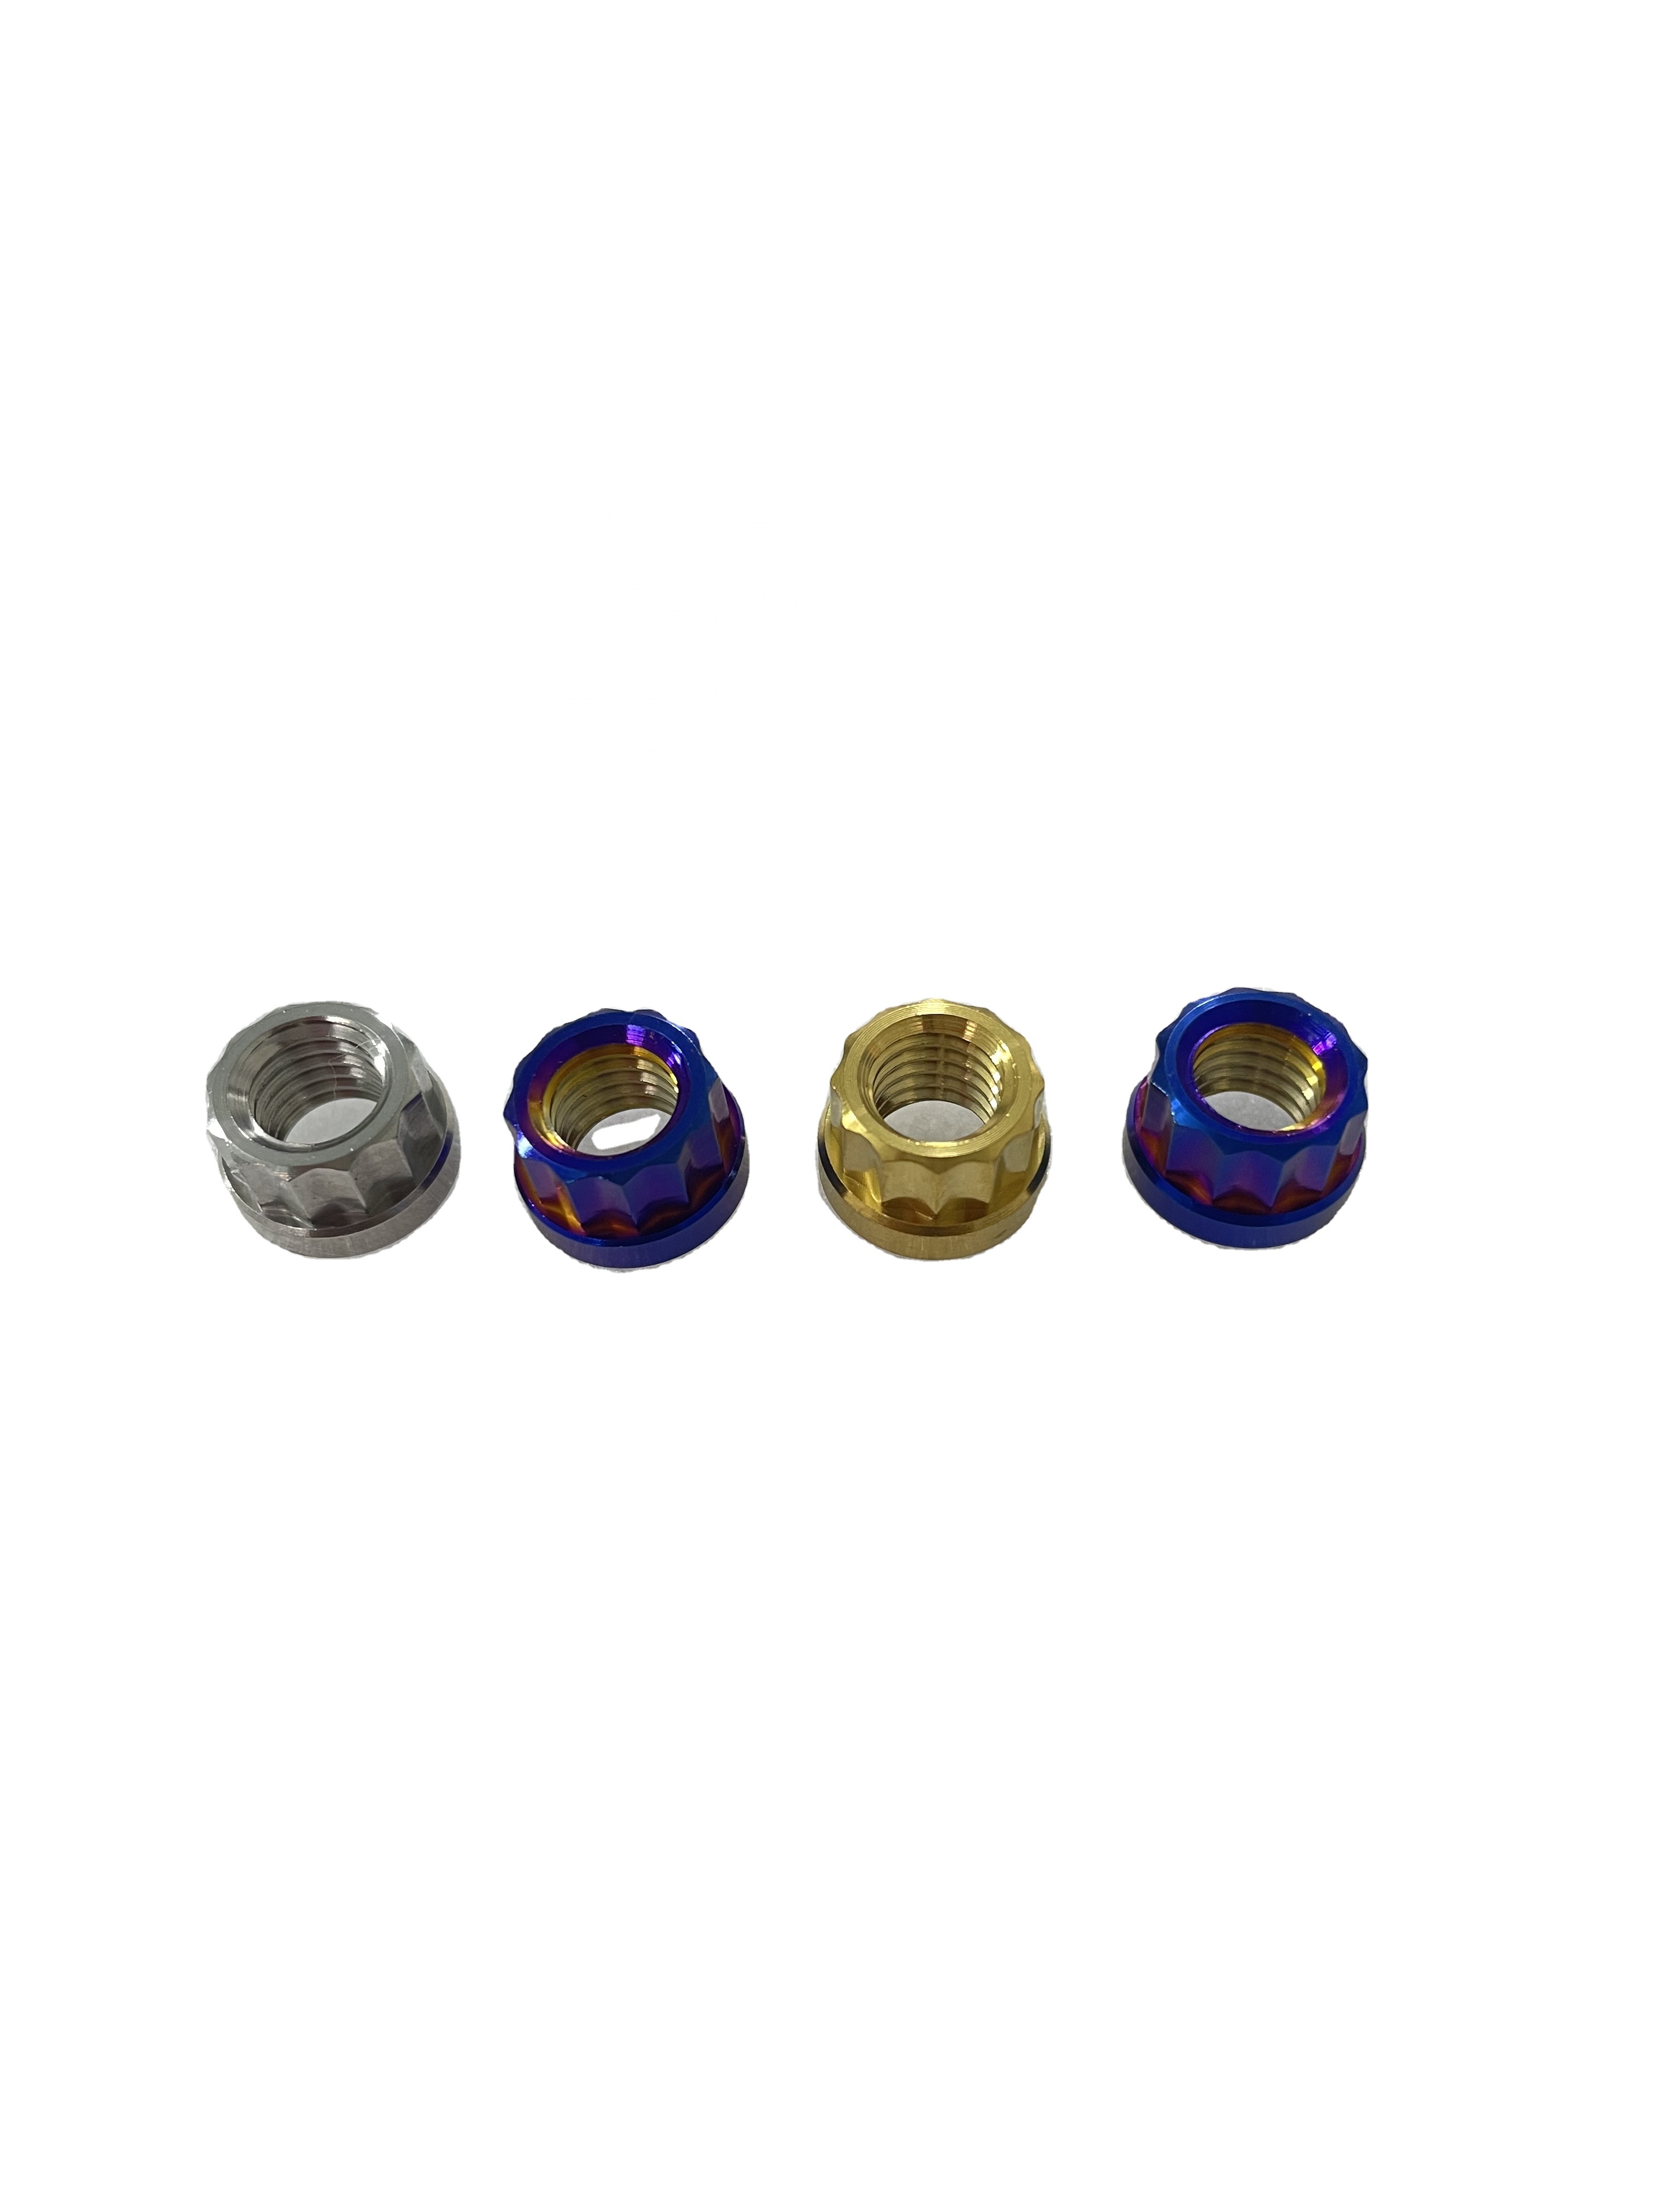
Polished Gr5 Titanium 12 Point Flange Nut M10X1.25 for Automotive Racing
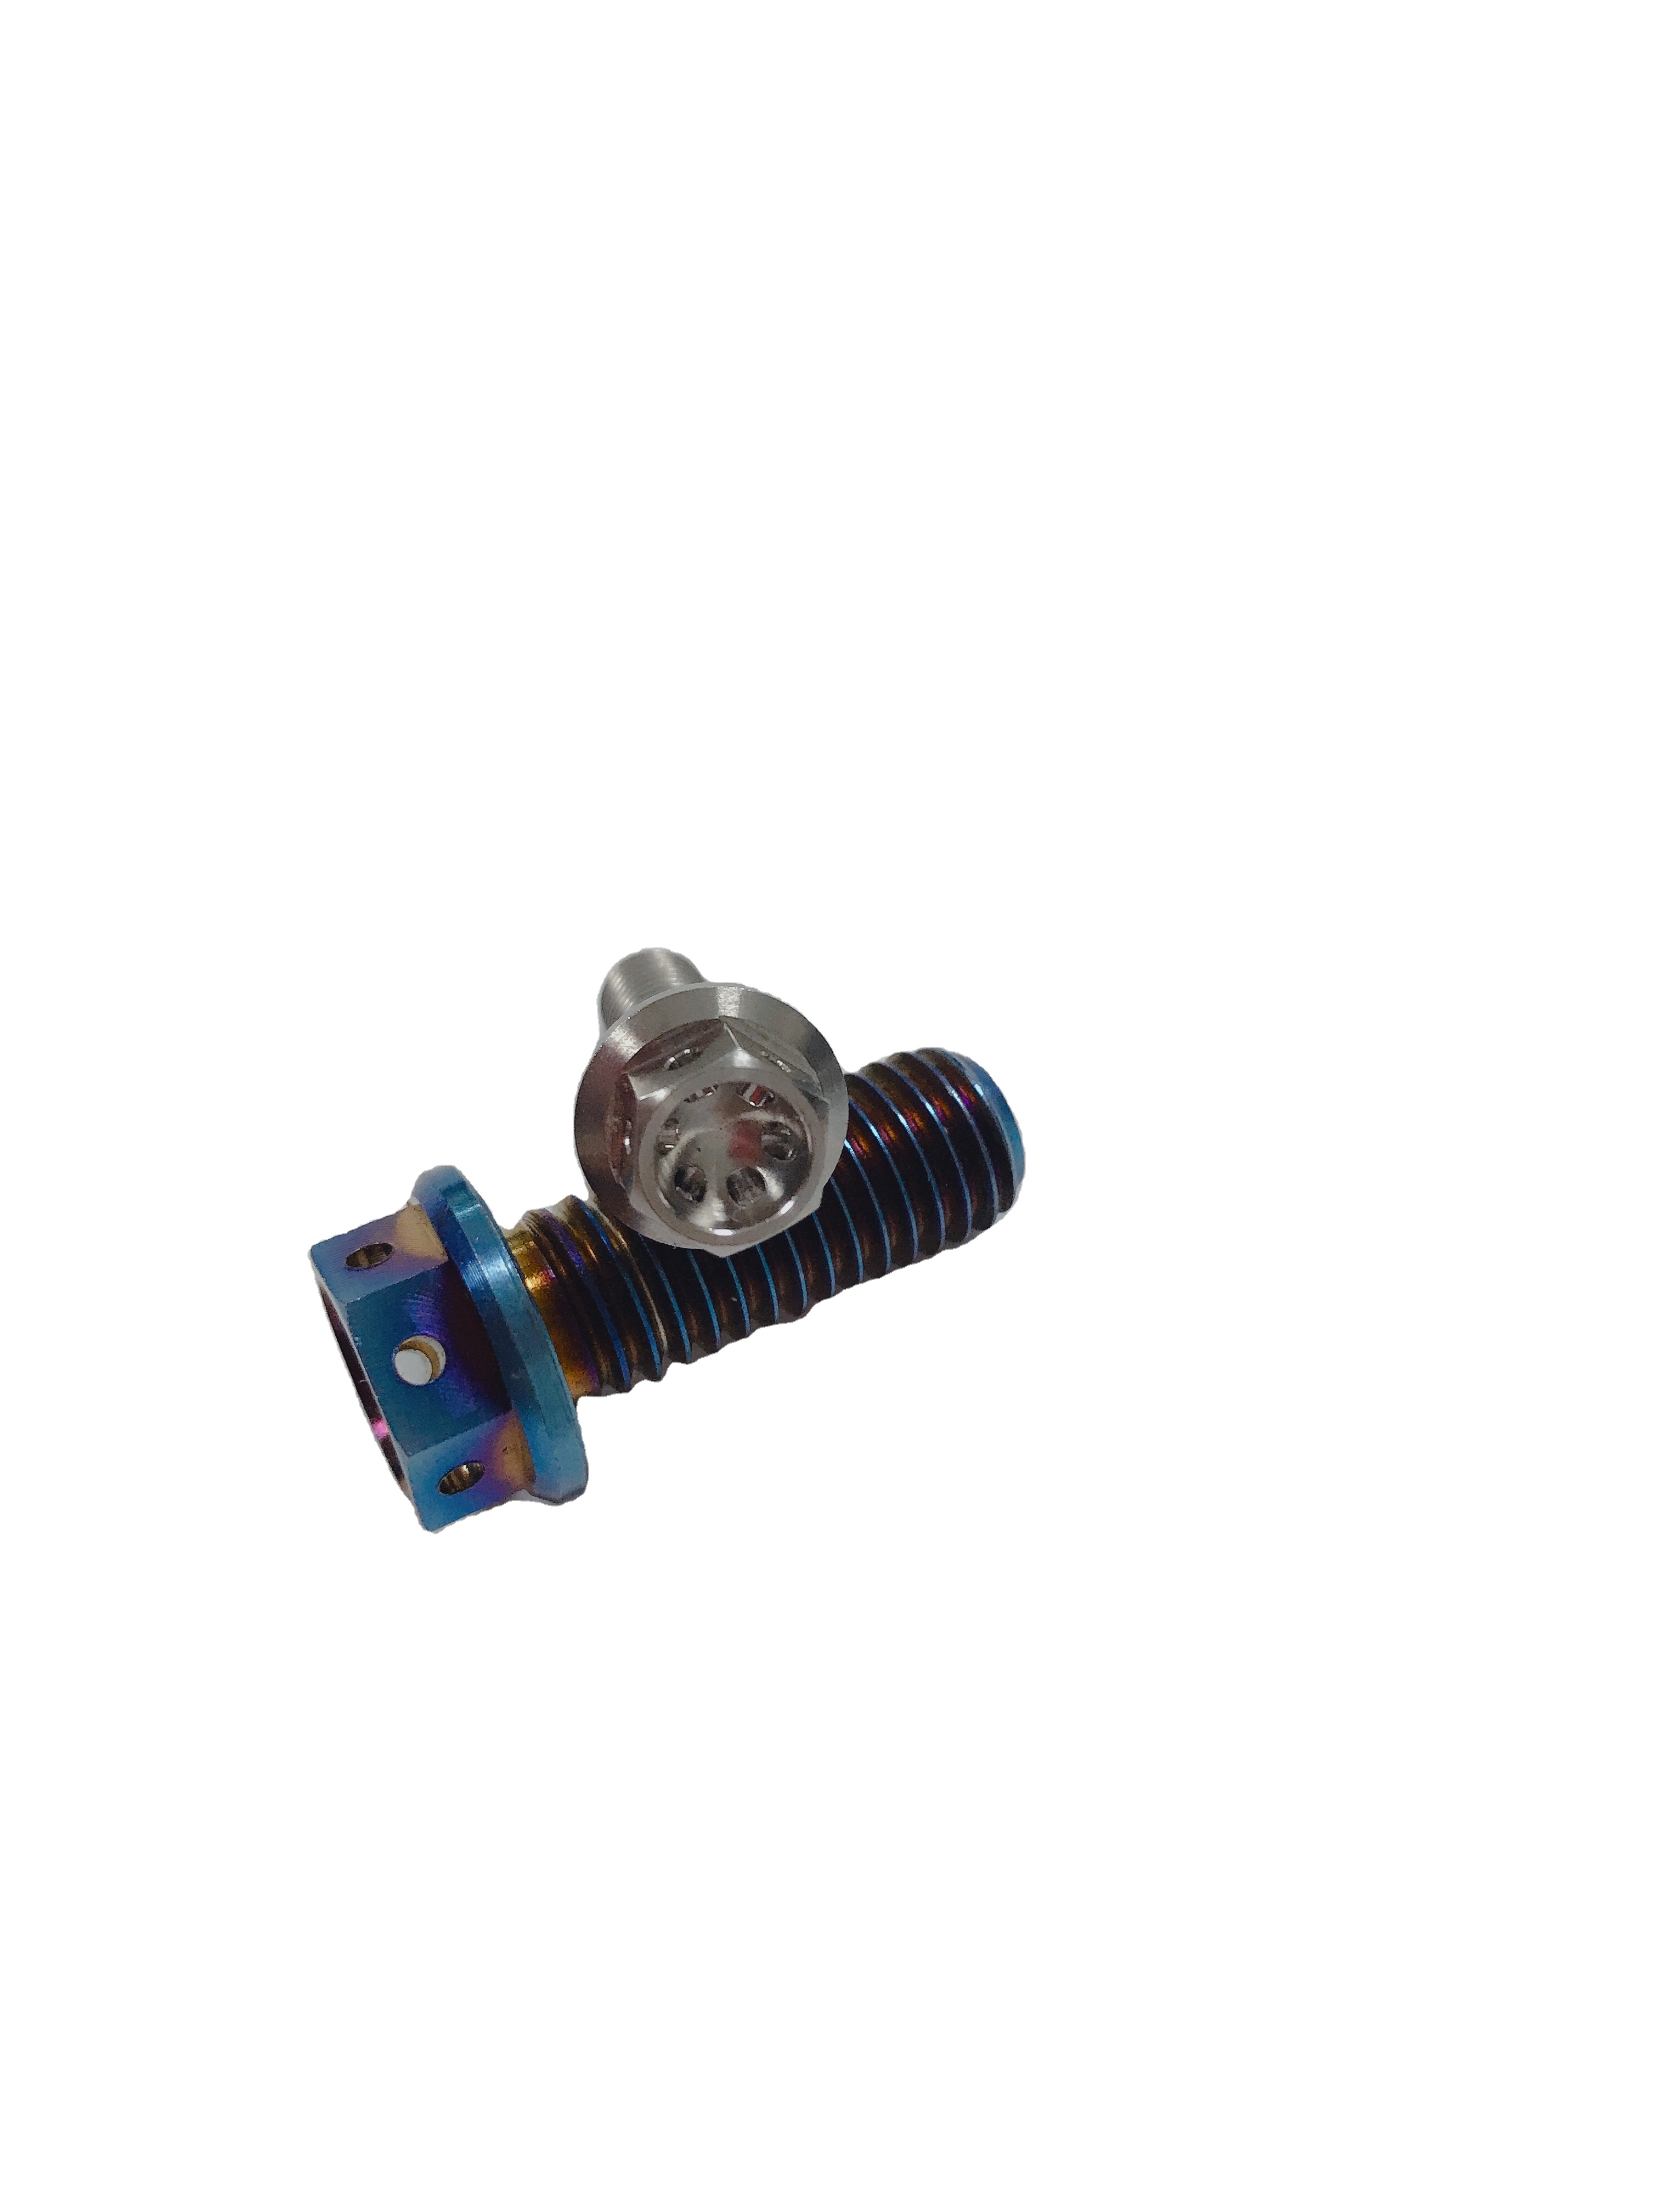
M6x30 M6x35 GR5 Grade Hex Head Titanium Wheel Flange Bolts for Motorcycle
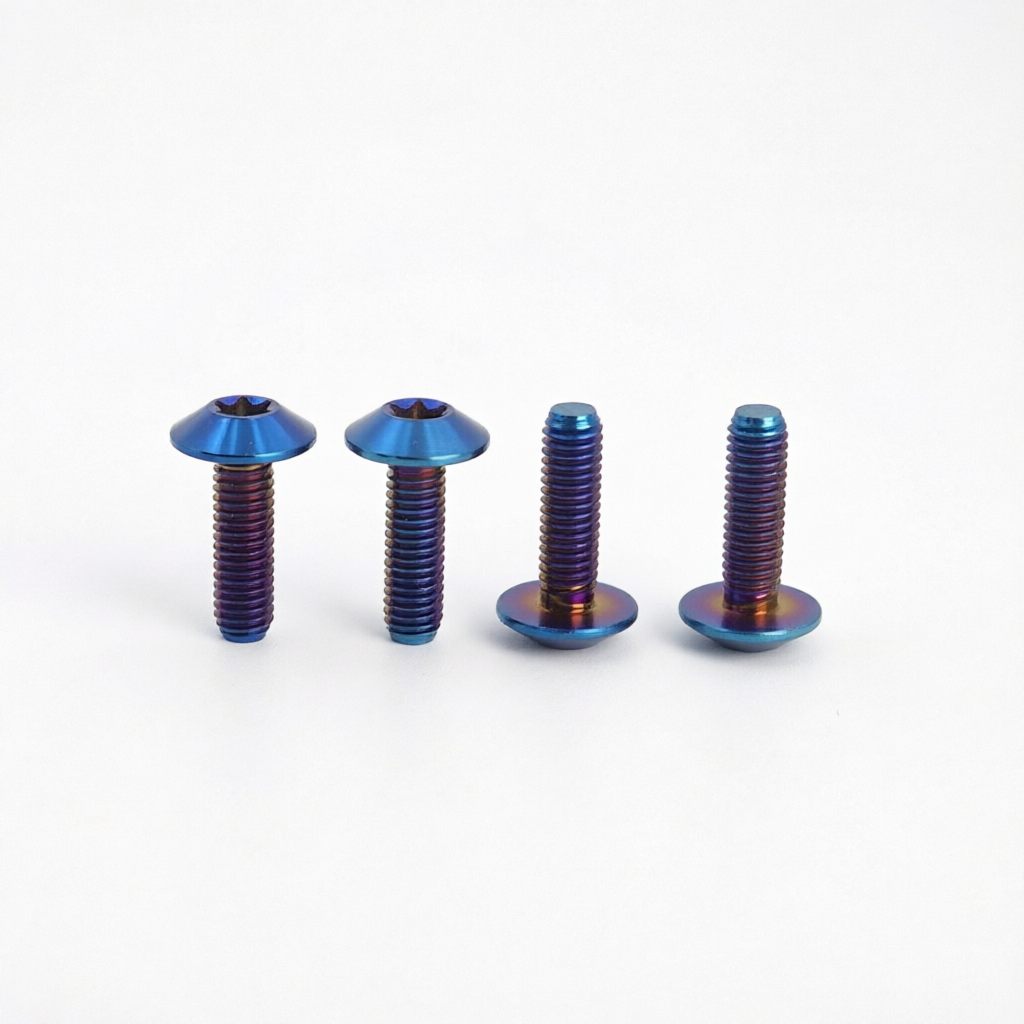
M6x16mm GR5 Titanium Alloy Disc Head Bolts PVD Finish Torx Socket Screws Custom Color for Motorcycle Chain Guard
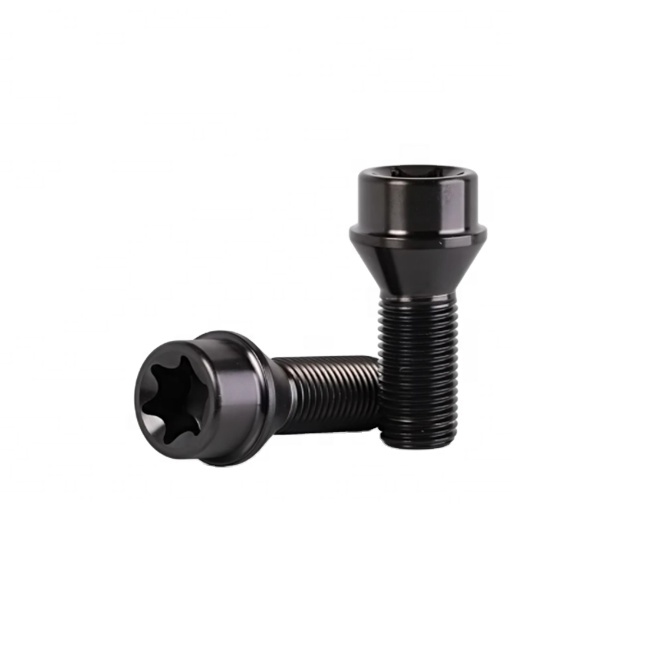
Titanium Wheel Bolts M14 DIN Standard Torx Shape CNC Machined Nitride Black Finish Minghai Brand for Ferrari
Engineered in Baoji: The Heart of China's Titanium Valley
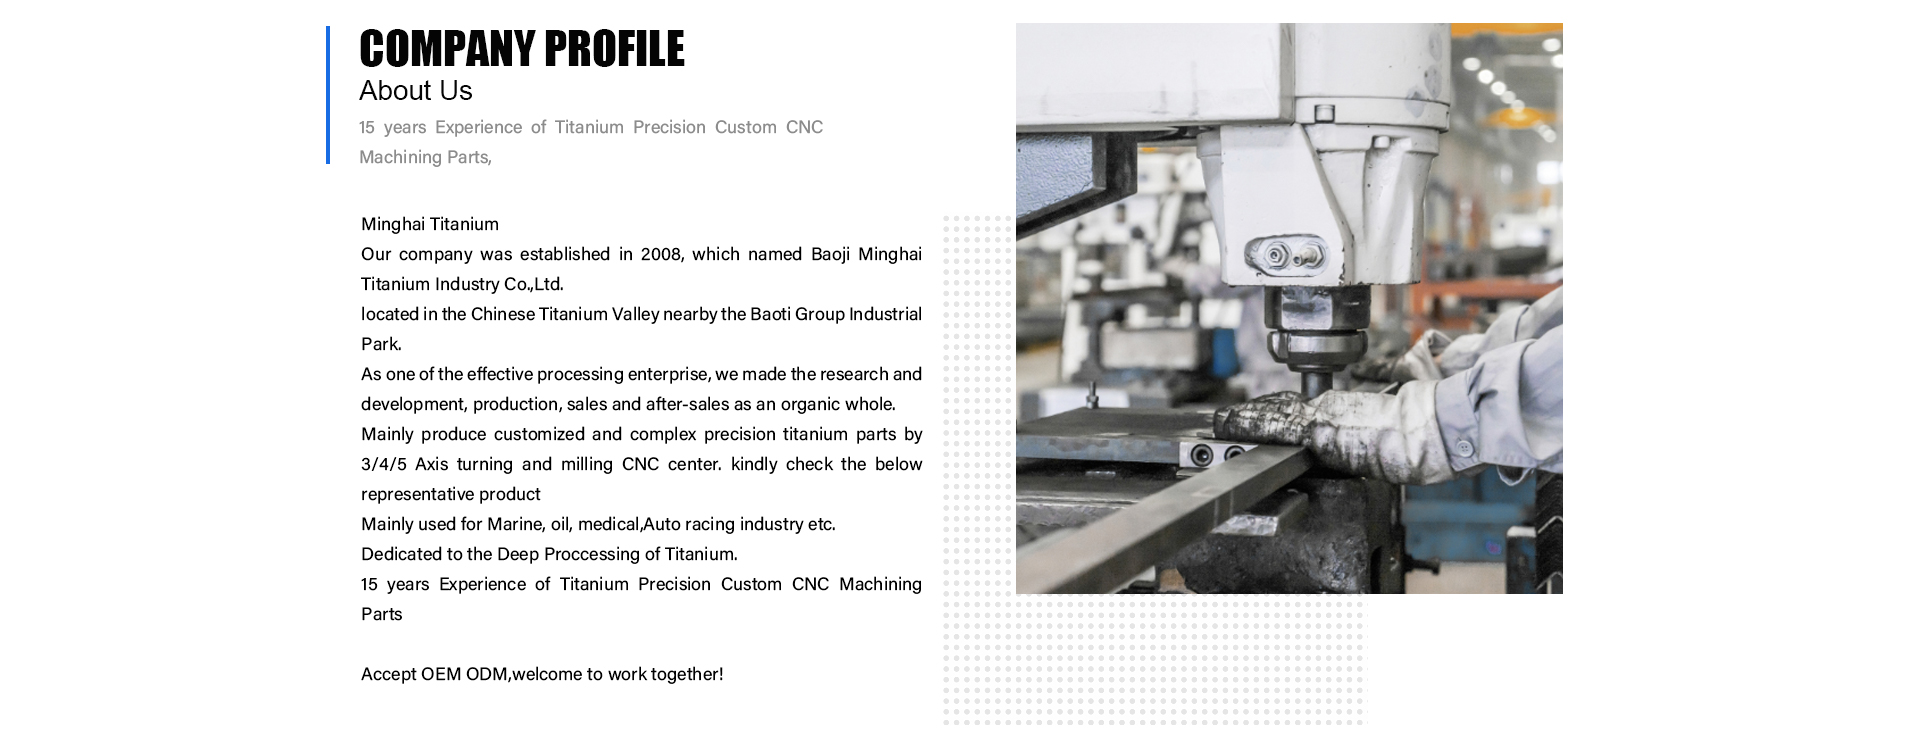
Strategically headquartered in the Gaoya Village Industrial Zone, Baoji, Shaanxi Province, adjacent to the state-level Baoti Group Industrial Park, our manufacturing facility commands direct access to the world's most concentrated titanium supply chain. Baoji manufactures more than 65% of China's and roughly 22% of the world's total titanium output, allowing us to source premium, vacuum-arc double-remelted (VAR) titanium sponge and aircraft-certified bars without secondary intermediary markups.
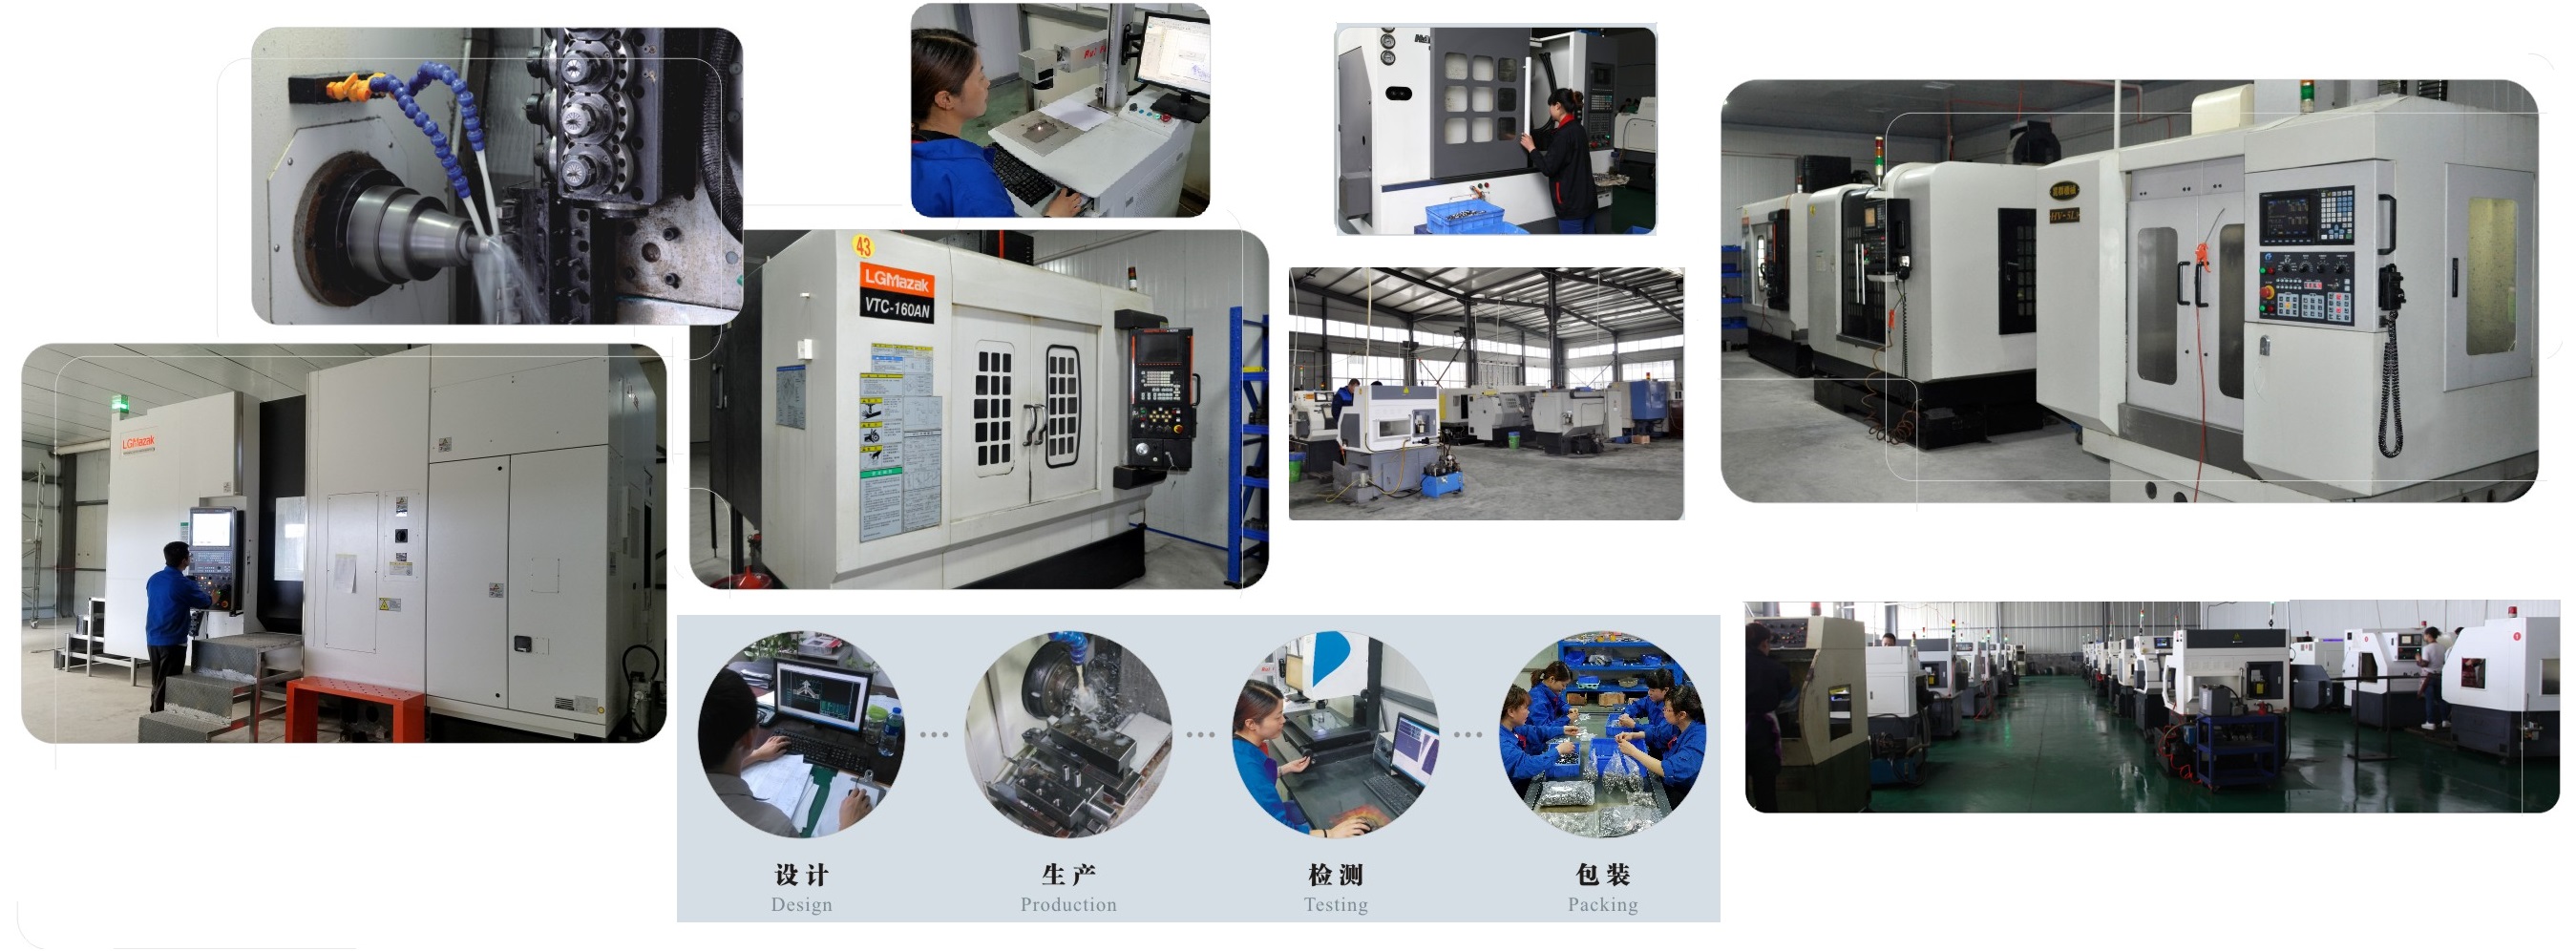
Since our founding in 2008, we have operated as an integrated OEM/ODM enterprise uniting metallurgical testing, computer-aided design (CAD/CAM), automated multi-station cold and hot heading, 5-axis CNC machining, and post-treatment passivation under one comprehensive quality framework. Our products conform rigidly to ASTM B348, ASTM F136, AMS 4928, DIN, ISO, and JIS international standards, backed by batch-traceable EN 10204 Type 3.1 Material Test Reports (MTR).
Complete Sponge-to-Bolt Control
We verify chemical composition (O, N, H, C, Fe) via spectral analyzers right at raw billet ingestion to safeguard against hydrogen embrittlement.
Rapid DFM Engineering Feedback
Our senior metallurgical and tooling engineers review client STEP, DWG, and IGES models within 9 hours, ensuring design-for-manufacturability cost savings.

Why Grade 5 (Ti-6Al-4V) Dominates High-Integrity Fastening
Understanding the mechanical kinetics, grain morphology, and thread-rolling dynamics that distinguish premium aerospace-grade titanium bolts from sub-standard commercial alternatives.
Alpha-Beta Microstructure
Ti-6Al-4V (Grade 5, UNS R56400) is an alpha-beta alloy combining 6% aluminum (alpha stabilizer) and 4% vanadium (beta stabilizer). This metallurgical balance yields an ultimate tensile strength exceeding 895–1000 MPa while holding an elastic modulus around 114 GPa—almost half that of structural steel (210 GPa). Fasteners act like micro-springs, absorbing cyclic dynamic shocks without loosening.
Rolled Threads vs. Cut Threads
Standard cut threads sever the internal metallic grain flow lines, introducing microscopic notch points where fatigue cracks easily nucleate under repeated stress. In contrast, our CNC thread rolling cold-forms the titanium alloy, plastically displacing the grain flow around the root and crest. This induces high residual compressive stresses and extends fastener fatigue life by up to 300%.
Anti-Galling & PVD Tech
Bare titanium fasteners can suffer from adhesive wear (galling) when tightened against matching titanium or stainless threads without adequate lubrication. We mitigate this through vacuum Physical Vapor Deposition (PVD) applying TiN (Titanium Nitride), TiAlN, or DLC (Diamond-Like Carbon) coatings. This hardens the surface to 2000–3000 HV and drops the friction coefficient below 0.15.
Empirical Engineering Comparison: Titanium Gr5 vs. Traditional Fastener Alloys
| Fastener Material | Density (g/cm³) | Yield Strength (MPa) | Tensile Strength (MPa) | Strength-to-Weight Ratio | Corrosion Resistance | Thermal Window (°C) |
|---|---|---|---|---|---|---|
| Titanium Gr5 (Ti-6Al-4V) | 4.43 | 828 – 910 | 895 – 1050 | 215 – 237 (Outstanding) | Total (Chloride/Marine Immune) | -250°C to +400°C |
| High-Tensile Steel (Class 10.9) | 7.85 | 940 | 1040 | 132 (Standard) | Requires Zn/Cd Plating (Prone to Rust) | -40°C to +250°C |
| Austenitic Stainless (A4-80 / 316) | 8.00 | 600 | 800 | 100 (Low) | Good (Vulnerable to Pitting Crevice) | -196°C to +300°C |
| Aerospace Aluminum (7075-T6) | 2.81 | 505 | 570 | 202 (High) | Poor (Rapid Galvanic Anodizing Loss) | -50°C to +120°C |
Future Procurement & Sourcing Trajectories for Titanium Fasteners
An empirical evaluation of supply chain reallocation, EV hyper-lightweighting demands, and additive-subtractive hybrid manufacturing shaping industrial procurement over the next five years.
1. EV Range Optimization & Unsprung Mass
As global automotive OEMs compete for extended battery driving range per kilowatt-hour, reducing unsprung rotational weight has transitioned from hypercar exotics to commercial performance electric vehicles. Wheel hub bolts, caliper studs, and suspension link hardware manufactured from Grade 5 titanium strip approximately 1.5 to 2.5 kg of rotating unsprung mass per corner. This enhances battery range metrics by 1.8% to 3.2% while sharpening suspension damping response.
2. Decoupling Intermediary Broker Channels
Procurement teams across North America and Europe are dismantling tiered broker networks that inflate standard hardware pricing by 40% to 120%. By establishing direct, contract-level OEM agreements with verified manufacturers in Baoji, tier-1 racing houses and defense sub-contractors secure direct production slots, dedicated machine time on 5-axis centers, and pristine, unadulterated mill test traceability back to vacuum sponge melting.
3. Rigorous ESG & Closed-Loop Swarf Recycling
With titanium production carrying an intensive carbon footprint during Kroll process sponge reduction, the future of international procurement hinges on closed-loop swarf stewardship. Our factory operates internal vacuum briquetting and degreasing systems that compress 100% of CNC machining chips into high-density briquettes for direct remelting by certified raw material partners. This guarantees lower scope-3 carbon credits for international buyers.
Technological Development Trends in Fastener Engineering
Hybrid Precision Cold-Heading with Finish Turning
Historically, titanium Grade 5 required pure subtractive bar lathe machining due to its low room-temperature ductility and rapid work-hardening behavior. Modern multi-stage warm-forging induction systems now preheat the bar stock to 650°C–750°C in microseconds. This enables rapid net-shape head forming without micro-cracking, slashing material waste from 60% down to 12% and dramatically lowering unit costs for high-volume custom production runs.
Smart Fasteners & Sensor-Embedded Retention
Next-generation high-stress titanium fasteners for hyper-performance motorsports and aerospace turbines are increasingly integrating hollowed internal bores designed to house miniature fiber-optic Bragg grating (FBG) sensors or RFID micro-chips. These smart fasteners broadcast real-time bolt clamp load and dynamic strain levels to vehicle telemetry, warning pit crews and maintenance teams of pre-load relaxation before catastrophic fatigue failure.
Technical RFQ Sourcing Checklist for International Importers
Before placing volume purchase orders for custom titanium bolts, ensure your Request for Quote (RFQ) specifies these critical engineering parameters to prevent costly line stoppages or premature failures.
Alloy Chemistry Verifications
Demand compliance with ASTM B348 Grade 5 or AMS 4928. Ensure interstitial elements (specifically Oxygen ≤ 0.20% and Hydrogen ≤ 0.015%) are verified to avoid micro-brittleness.
Class 6g/4h Thread Rolling
State unequivocally whether thread profiles must be cold/warm rolled post-heat treatment or if single-point CNC turned threads are acceptable for non-critical static housings.
Elliptical Transition Geometry
Verify the junction between the bolt shank and bolt head incorporates an engineered elliptical transition radius to distribute stress concentrations evenly during axial tightening.
Passivation & Dry-Film MoS2
Specify whether ultrasonic nitric acid passivation is needed to eliminate free iron inclusions picked up from steel tooling, or if factory-applied MoS2 solid anti-seize dry lubricants are desired.
Frequently Asked Questions for B2B Titanium Hardware Sourcing
Exhaustive answers to technical, logistical, and metallurgical queries addressed directly by our senior production director and chief metallurgist.
1. Why should our engineering team specify Grade 5 (Ti-6Al-4V) over commercially pure Grade 2 titanium for structural fasteners?
2. How does your factory eliminate the risk of thread galling and cold-welding during automated assembly?
3. What specific quality control documentation is supplied with every export shipment?
4. Can your CNC workshop machine custom thread profiles and non-standard head shapes from client CAD files?
5. What is the typical torque-to-clamp-load relationship when switching from steel bolts to titanium?
6. What are your production lead times, prototype sampling capabilities, and Minimum Order Quantities (MOQ)?
Ready to Optimize Your Hardware Weight & Supply Chain Resilience?
Submit your 2D/3D part drawings, BOM list, or OEM target specifications. Our Baoji application engineers deliver comprehensive DFM feedback, metallurgical grade validation, and volume wholesale pricing within 9 hours.