Custom PVD
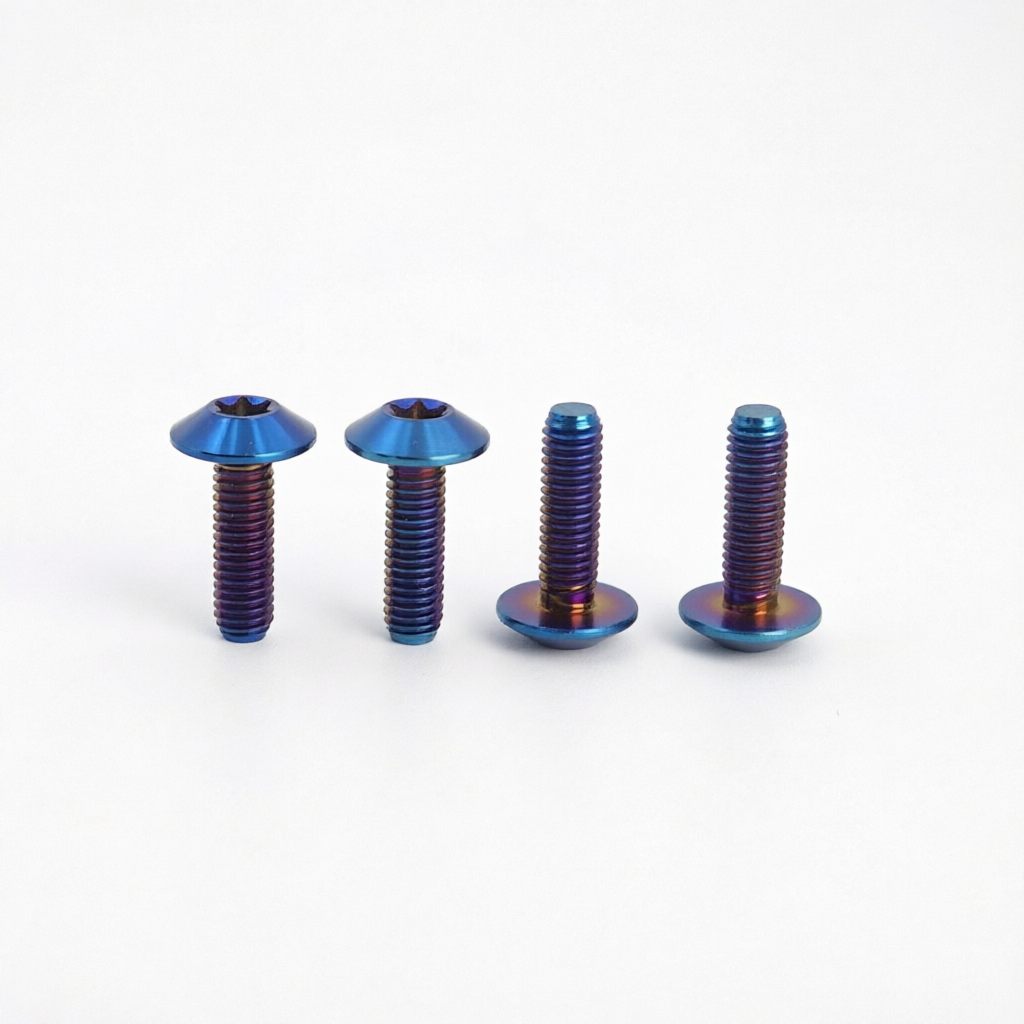
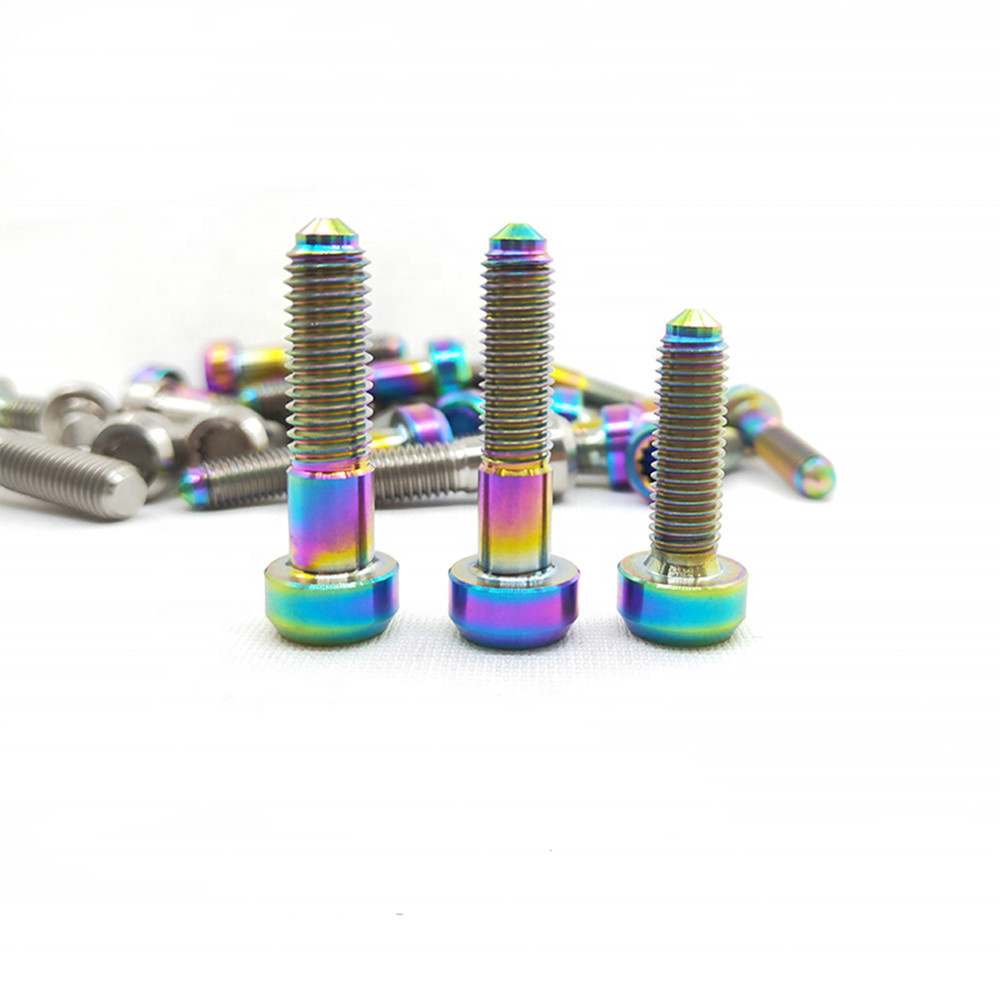
M6x16mm GR5 Titanium Disc Head Torx Bolts
Thread: M6 Metric Rolled
Drive: High-Torque T30 Torx
Application: Shield & Exhaust Covers
Manufactured from aerospace-certified Ti6Al4V alloy with rolled threads for superior fatigue endurance under severe thermal cycling.
Overcoming thermal expansion mismatch, galling, and mechanical creep in performance exhaust manifolds.
Exhaust systems experience thermal cycles swinging from ambient temperatures to peak gas loads exceeding 850°C. While conventional stainless steel bolts suffer permanent deformation and preload relaxation under thermal creep, Ti-6Al-4V Grade 5 maintains high tensile integrity up to 450°C continuously, and resists short-duration exhaust collector spikes without microstructural degradation.
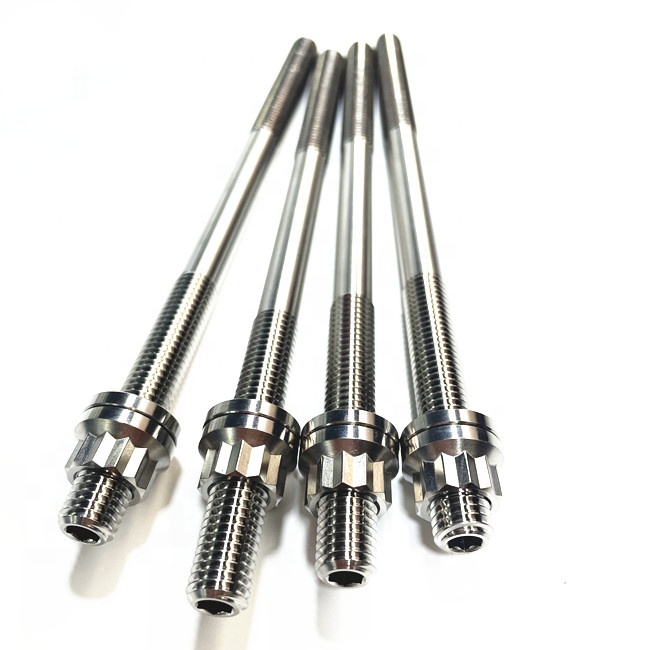
Cutting external threads severs the crystalline grain fibers of the titanium bar stock, producing localized notch stress concentration points where fatigue cracks initiate during repeated engine rev cycles. At Vunza, our exhaust studs feature cold-rolled threads after hot precision forging, which forces uninterrupted grain flow parallel to the flank profile, multiplying fatigue life 3.8-fold over cut fasteners.
Titanium naturally forms a microscopic passivating titanium dioxide (TiO2) film. Under dry friction and intense cylinder head clamping torque, this protective film can rupture, causing cold-welding (galling) of mating surfaces. We eliminate thread seizing via proprietary PVD titanium nitride coatings, physical vapor deposited DLC, and controlled micro-arc oxidation treatments.
| Performance Characteristic | OEM Gr5 Ti-6Al-4V (Annealed) | Grade 8.8 / 10.9 Alloy Steel | 316L Marine Stainless Steel | Inconel 718 Superalloy |
|---|---|---|---|---|
| Density (ρ) | 4.43 g/cm³ (45% Lighter) | 7.85 g/cm³ | 8.00 g/cm³ | 8.19 g/cm³ |
| Tensile Strength (UTS) | ≥ 895 – 1,020 MPa | 800 – 1,040 MPa | 580 – 620 MPa | 1,240 – 1,380 MPa |
| Yield Strength (0.2%) | ≥ 828 MPa | 640 – 940 MPa | 290 MPa | 1,030 MPa |
| Oxidation Limit in Air | 500°C (Continuous) | 350°C (Uncoated) | 750°C | 980°C |
| Corrosion Resistance (Salt/Moisture) | Immune (Zero Pitting) | Poor (Severe Rusting) | Moderate (Chloride Pitting) | Exceptional |
| Cost vs. Performance Ratio | Optimal for Racing / OEM | Economic (Heavier Mass) | Low Strength Constraint | Cost-Prohibitive for Mid-Scale |
How shifting powertrain architectures, emissions targets, and manufacturing automation are redefining titanium exhaust fastener sourcing.
As hybrid electric vehicles (HEVs) and high-performance PHEVs incorporate heavy lithium-ion battery modules, automotive engineering teams face strict weight budgets to satisfy global corporate emissions targets. Removing unsprung and chassis mass has shifted downstream into exhaust hangars, turbo manifolds, and downpipe assemblies, accelerating the replacement of mild steel with titanium hardware.
Global procurement offices are actively bypassing multi-tier broker distribution models in favor of direct contracts with integrated manufacturing hubs in Baoji, China. Factory-direct partnerships ensure full chemical traceability back to the raw titanium sponge, guaranteed ASTM B348 material documentation, and shortened lead times for high-volume custom CNC orders.
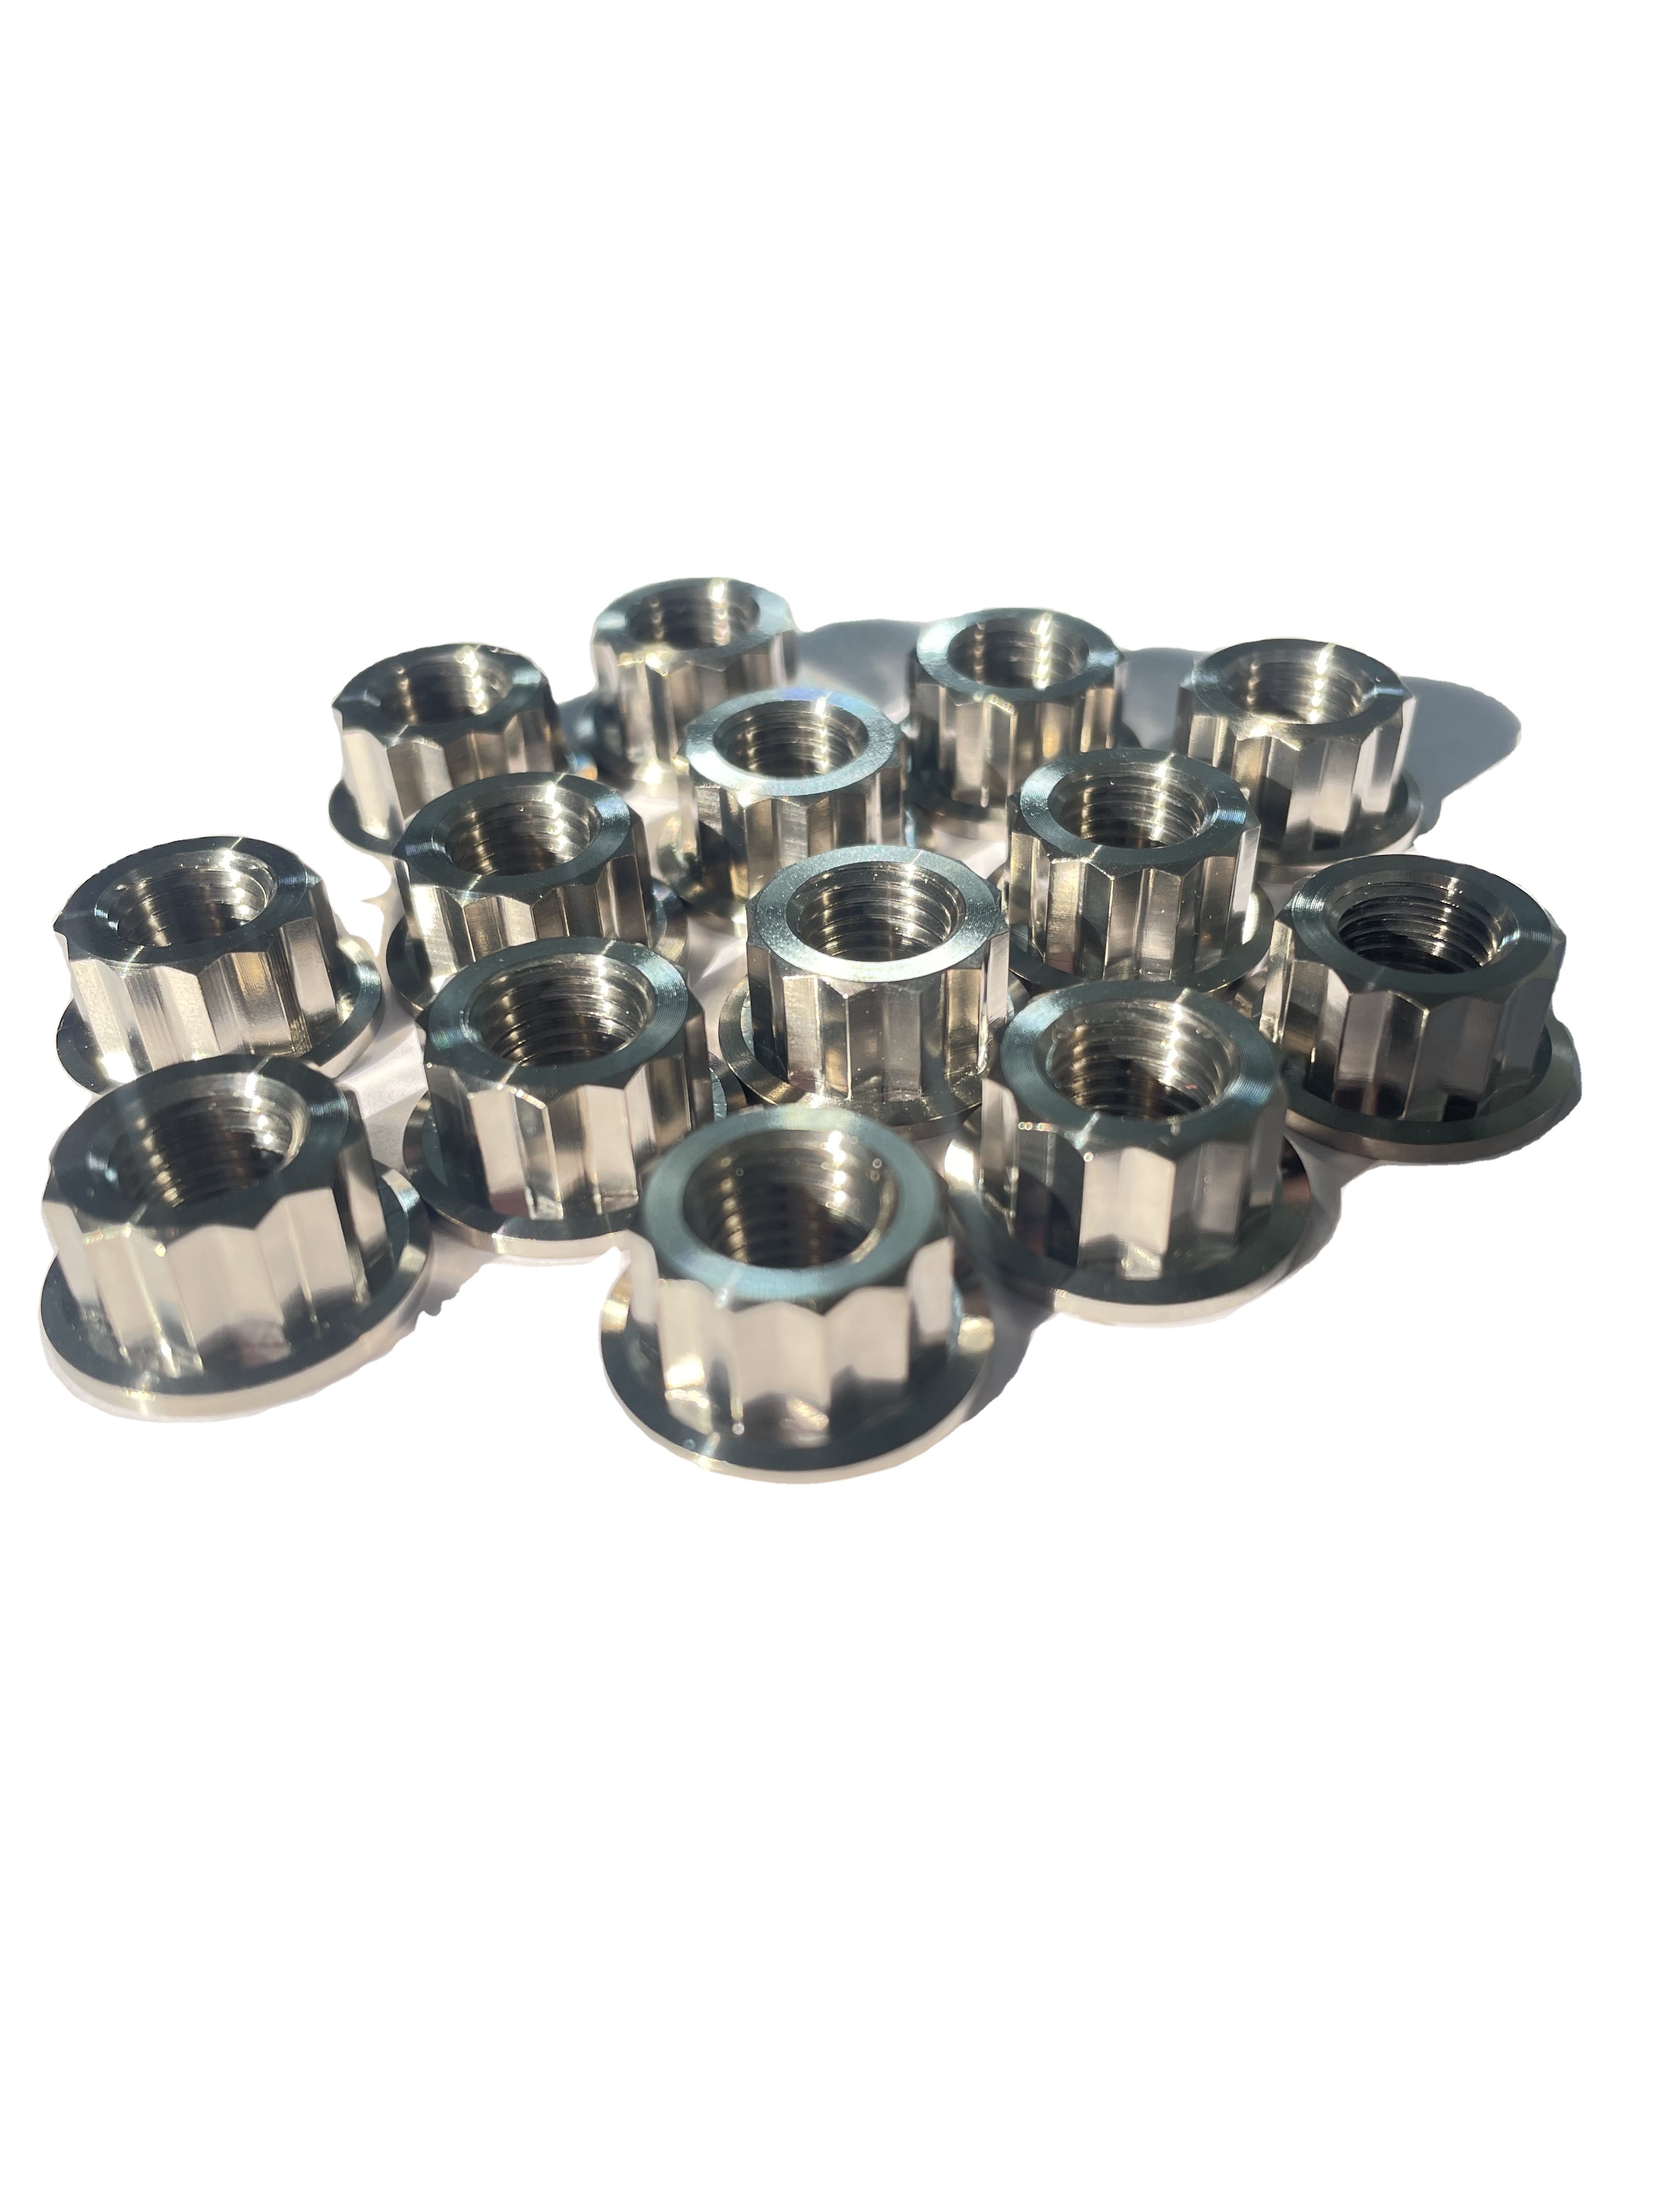
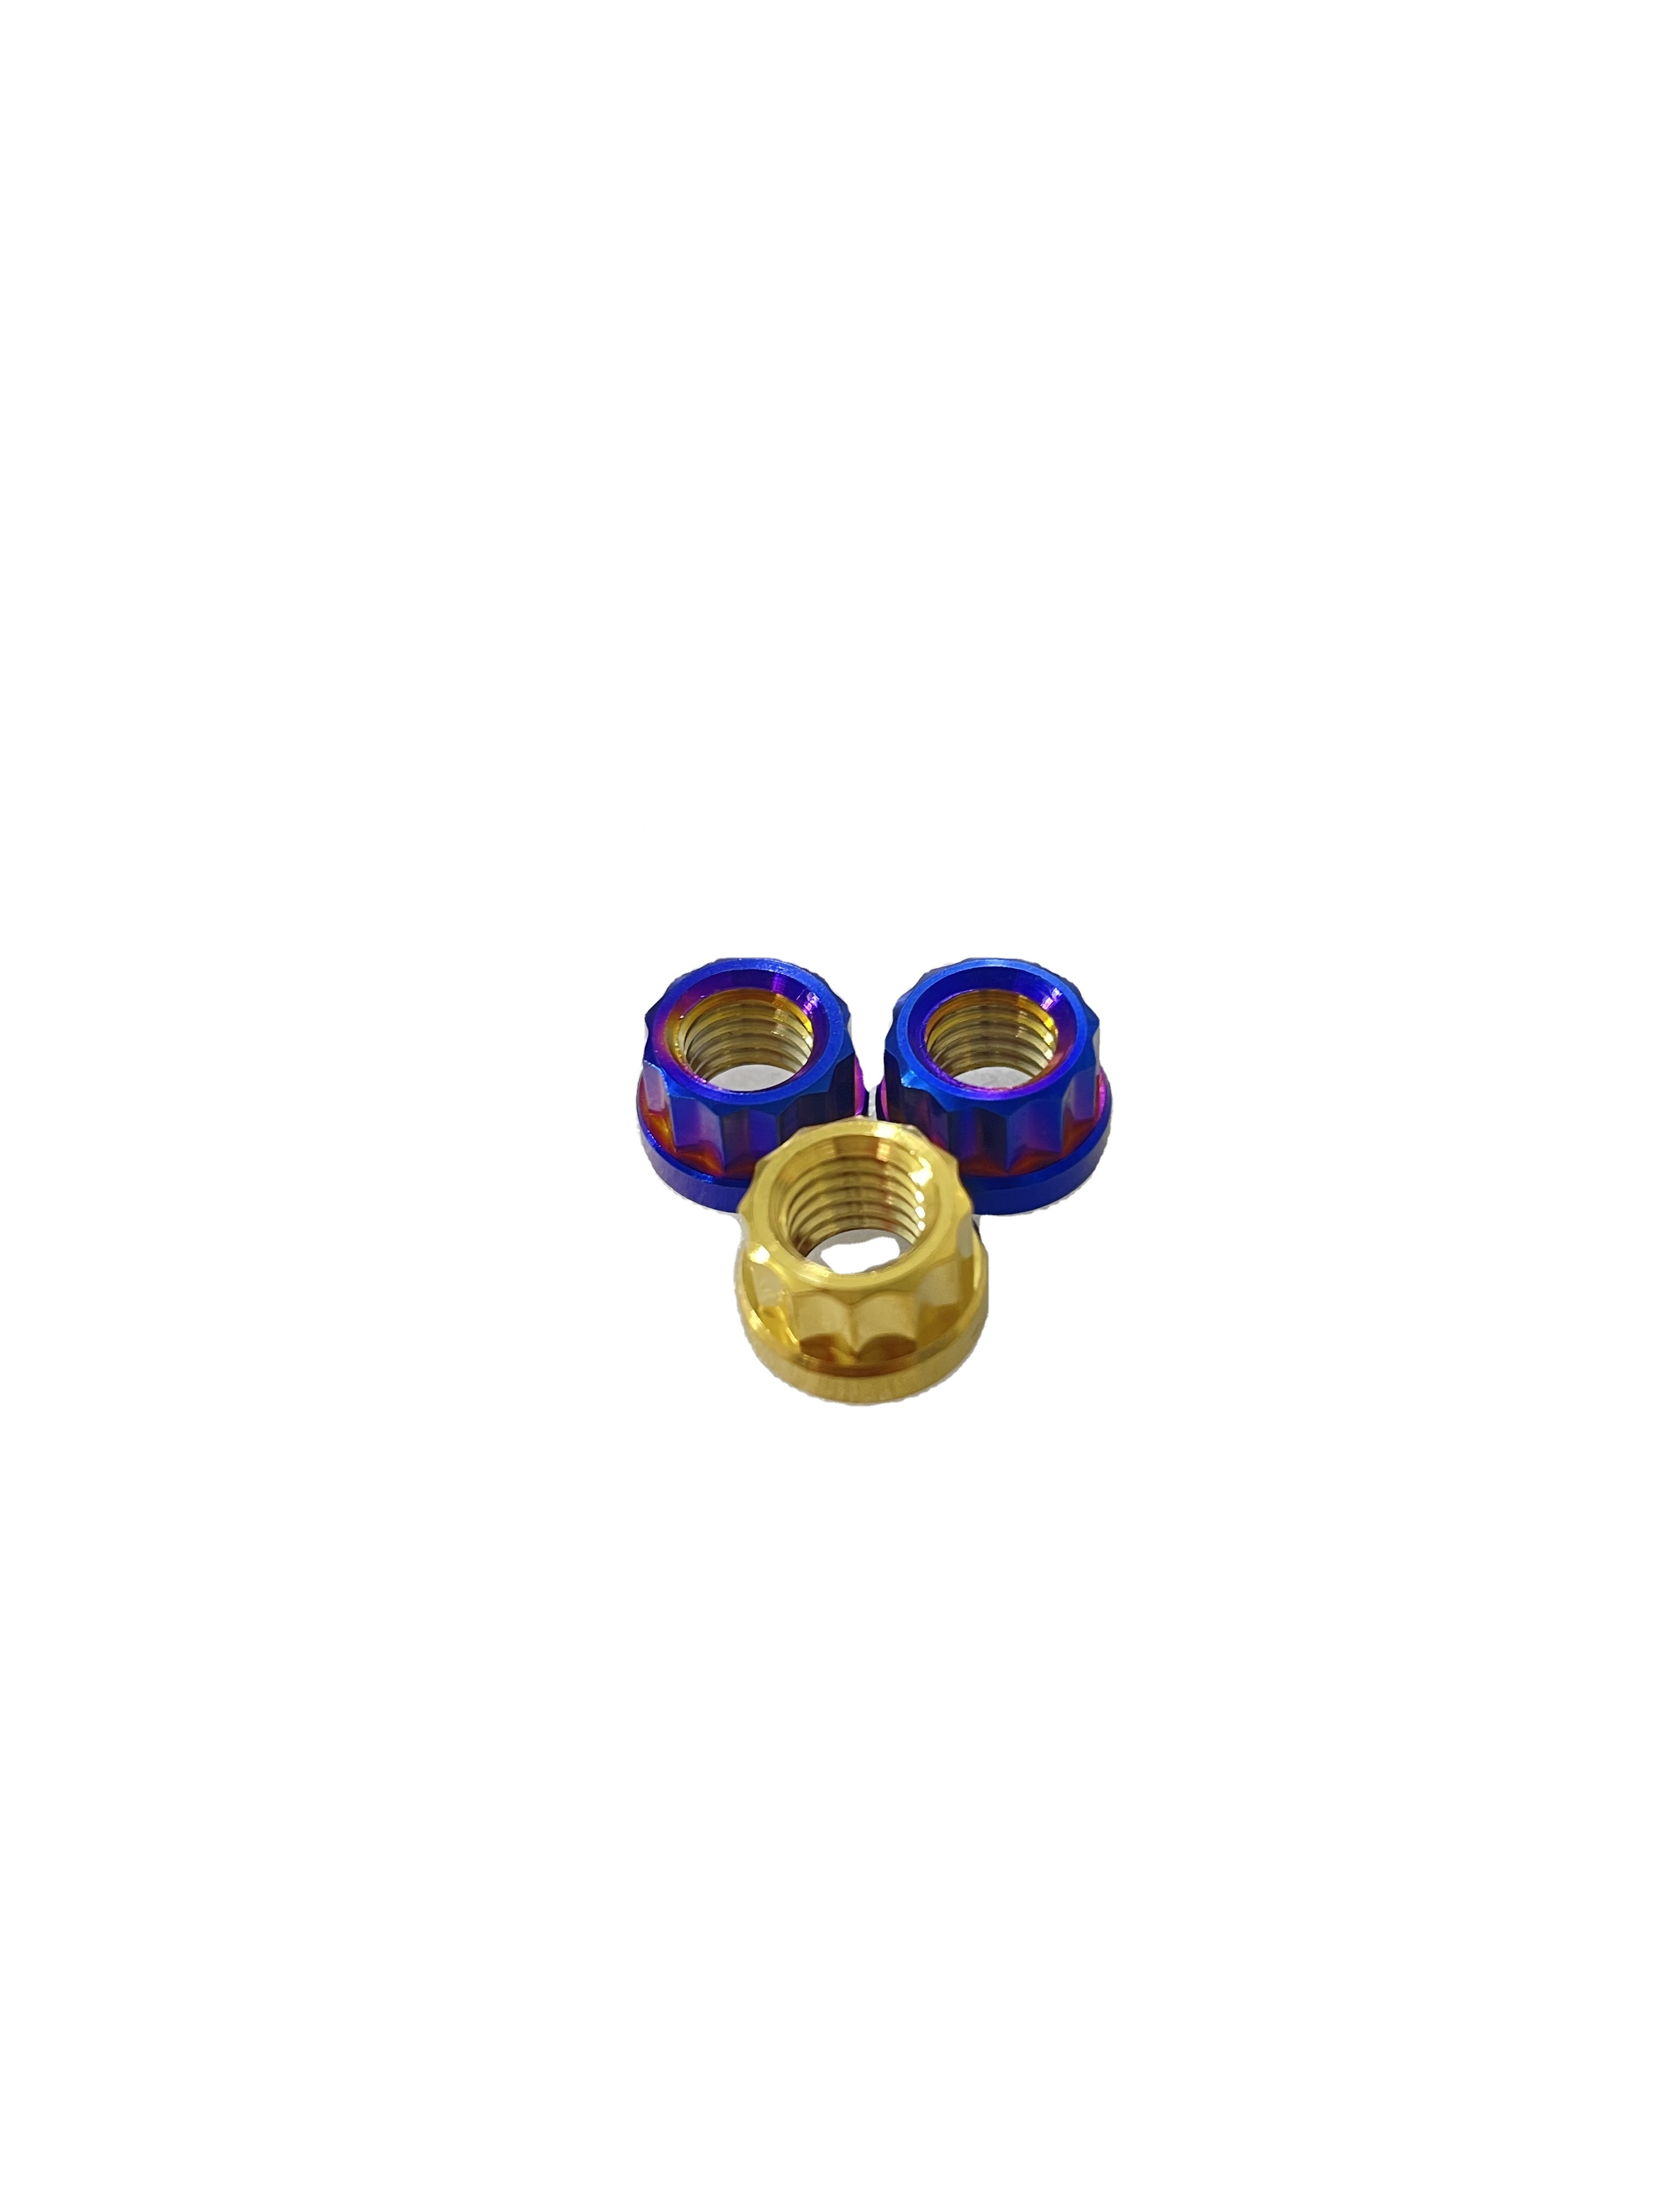
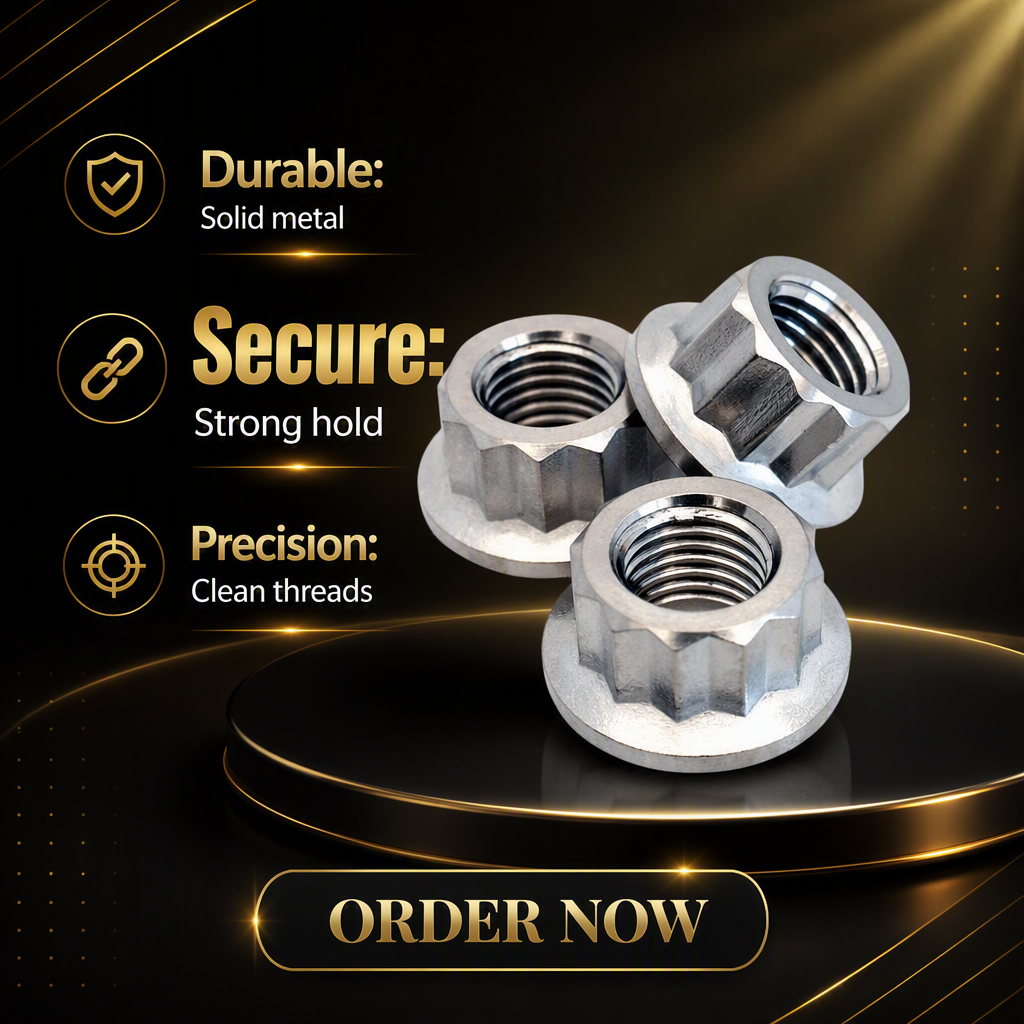
Standard hex fasteners are being replaced by aerospace-derived 12-point double hex flange geometries. The increased surface drive engagement prevents head rounding when using automated pneumatic assembly tooling on production lines, and permits smaller socket clearances in tightly packaged turbocharged engine bays.
The manufacturing trend has pivoted from multi-machine processing towards comprehensive 5-axis mill-turn centers. By executing high-precision turned threads, drive sockets, and weight-reducing hollow-core drilling in a unified clamping setup, concentricity errors are curtailed below ±0.005 mm while throughput increases.
Aesthetic preferences across aftermarket motorcycle and supercar segments have stimulated substantial R&D in high-adhesion PVD finishes. Modern coatings resist thermal discoloration, providing resilient burnt-blue, stealth gold, or satin black hues that withstand direct exposure to unburned hydrocarbons and acidic road debris.
As additive manufacturing matures for complex 3D-printed titanium exhaust collectors and catalytic housings, fastener designs must match thermal expansion profiles exactly. Hybrid titanium studs and stepped fasteners with integrated washers are becoming standard to distribute clamping pressures across 3D-printed flanges without galling.
Operating since 2008 in the Gaoya Village Industrial Zone adjacent to the Baoti Group Industrial Park in Baoji, Shaanxi, Vunza Titanium Industry Co., Ltd. is an onsite-verified manufacturer and global exporter. We control every stage of manufacturing—from metallurgical verification of raw sponge titanium to multi-axis CNC turning and automated optical sorting.

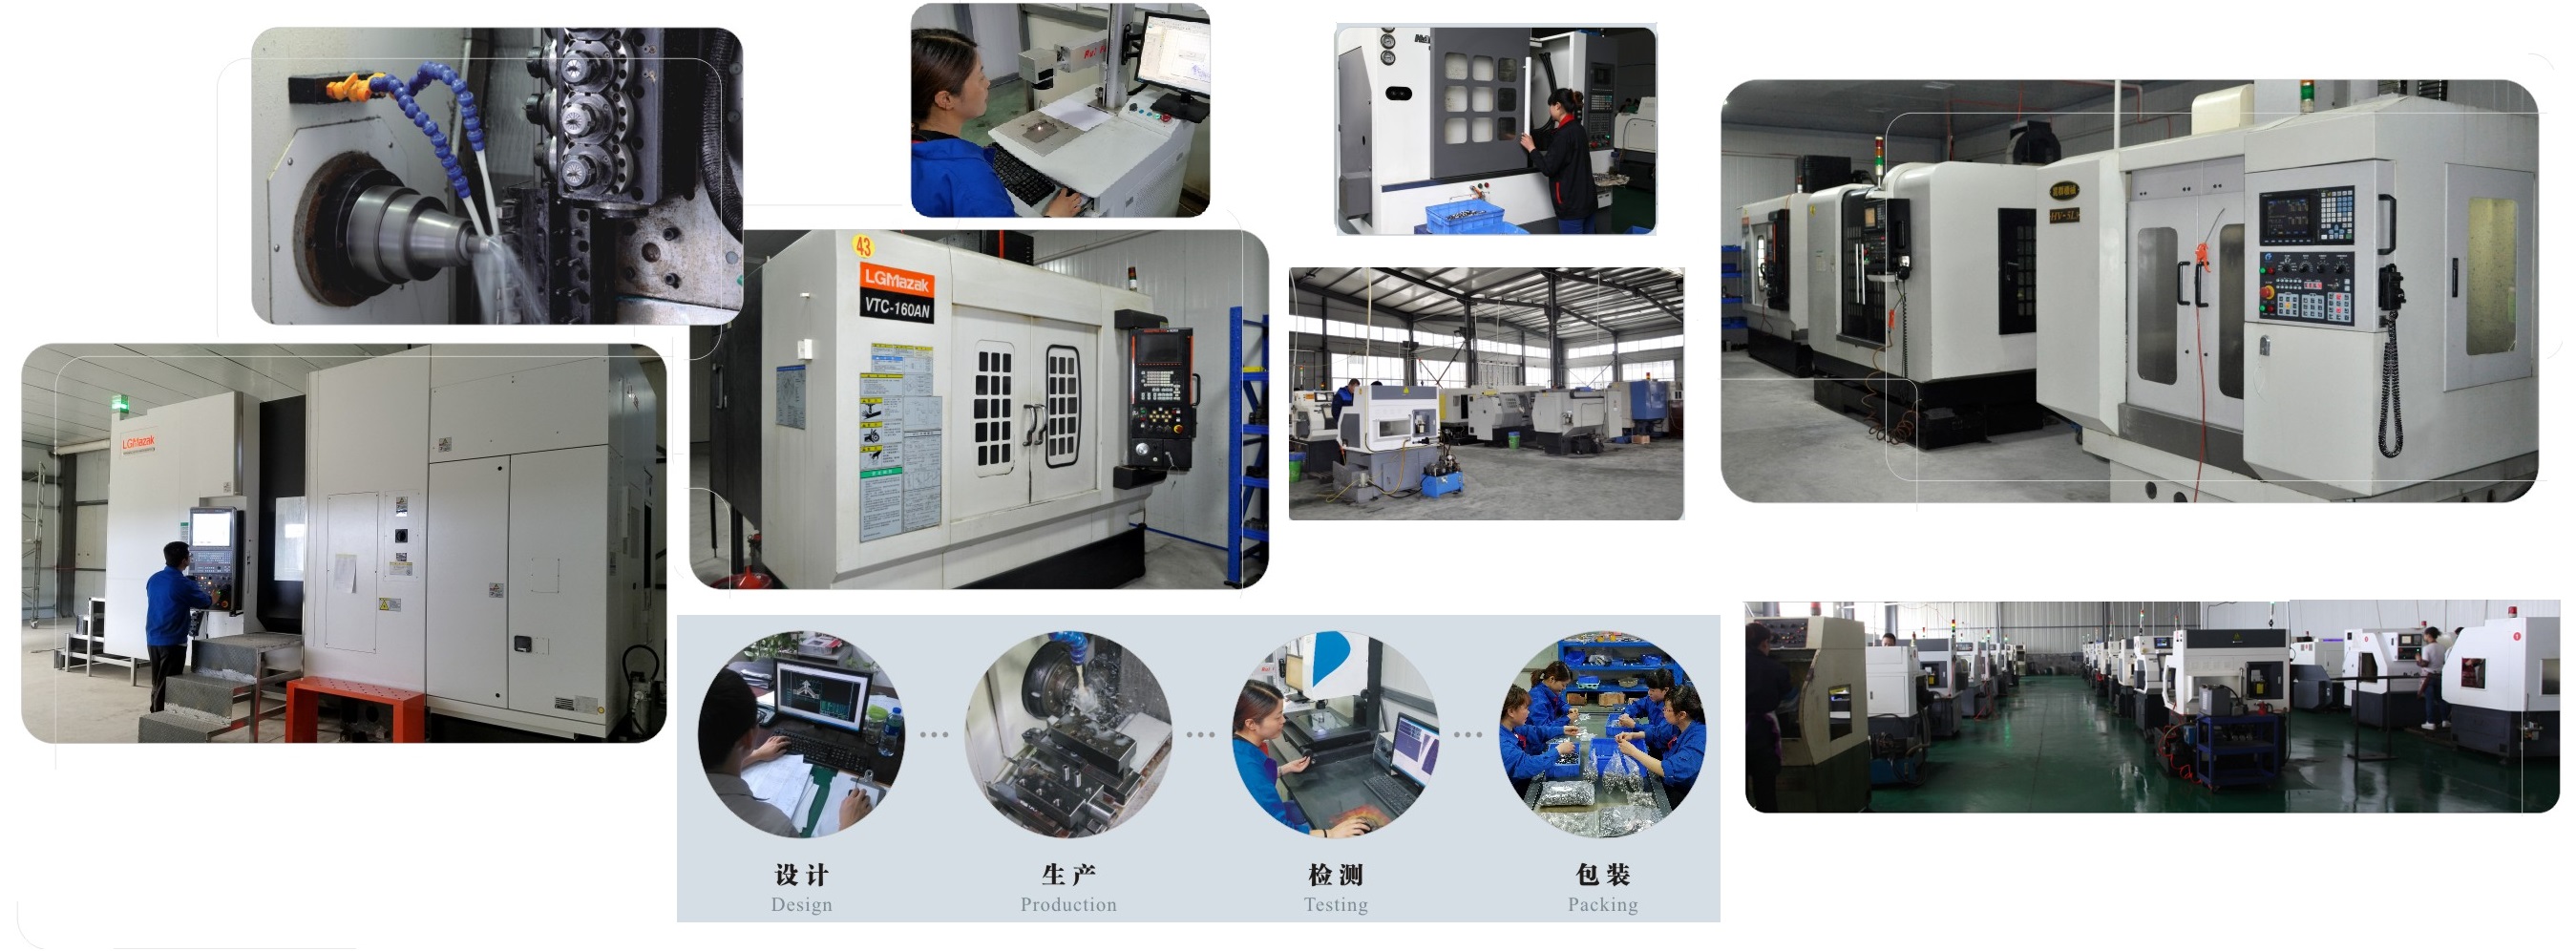
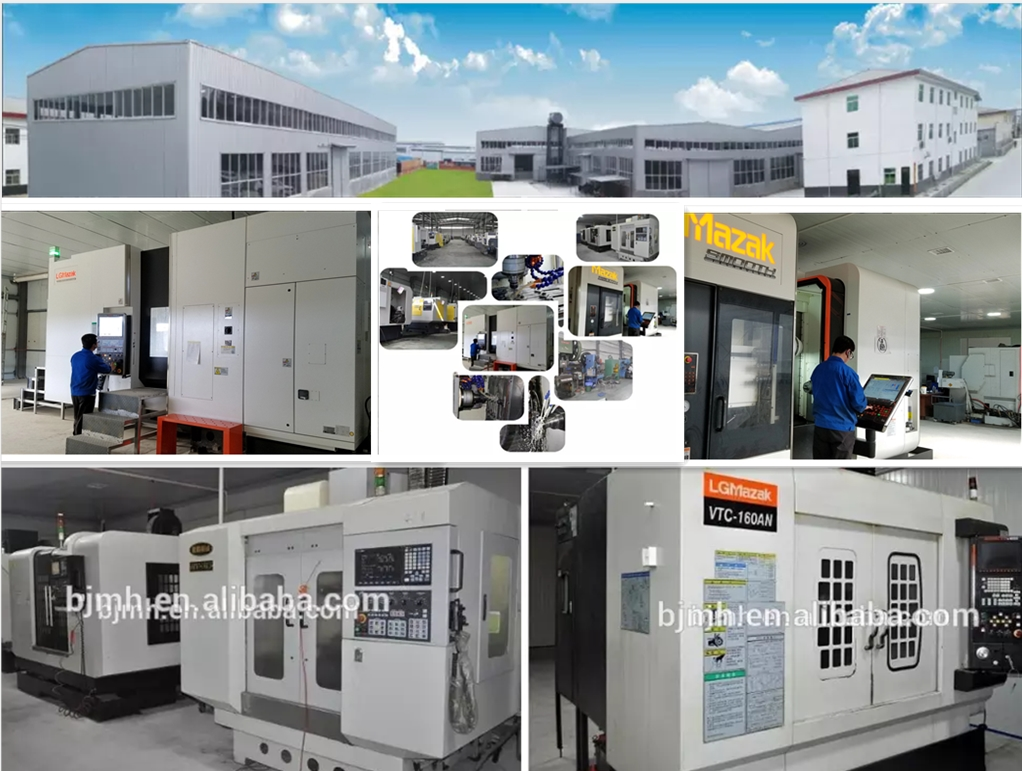
Factory premises, manufacturing lines, and trade capacity verified onsite by independent inspection bodies.
Mill test certificates (MTC) and spectral analysis reports accompanying every manufactured production batch.
13+ years continuous export record with repeat commercial buyers across motorsport and aerospace sectors.
Rapid engineering design validation, drawing revision review, and quotation response on business days.
Technical insights, MOQ constraints, and engineering guidelines to inform your B2B sourcing decisions.
Submit your 2D engineering drawings (PDF/DWG) or 3D CAD models (STEP/IGES). Our team in China's Titanium Valley will evaluate manufacturability, recommend alloy grades, and furnish a detailed quotation within 9 hours.