Precision CNC Machined & Forged Titanium Hardware
Explore our flagship OEM hardware series manufactured under strict ASTM B348 / AMS 4928 standards, holding tolerances down to ±0.005 mm for automotive racing, motorsport chassis, bicycles, and heavy industrial applications.
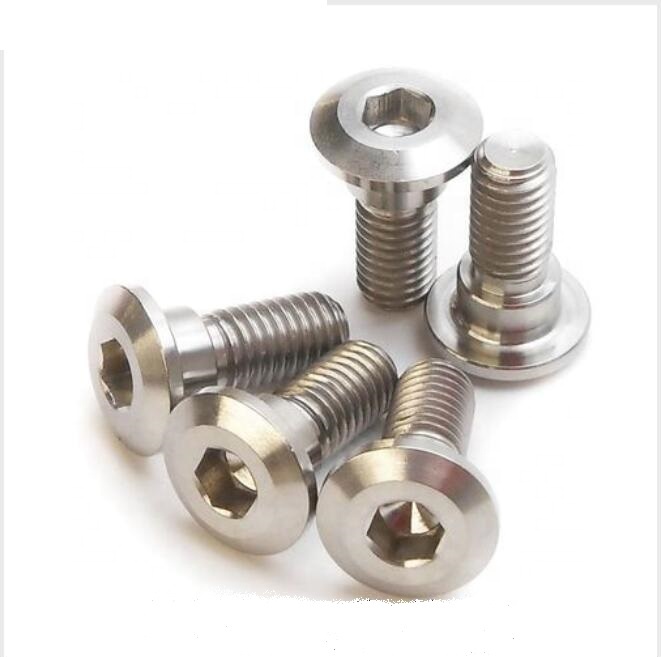
CNC precision turned Ti6Al4V disc head bolt featuring high torque transfer, low-profile weight savings, and ultimate fatigue endurance under cyclic vibration.
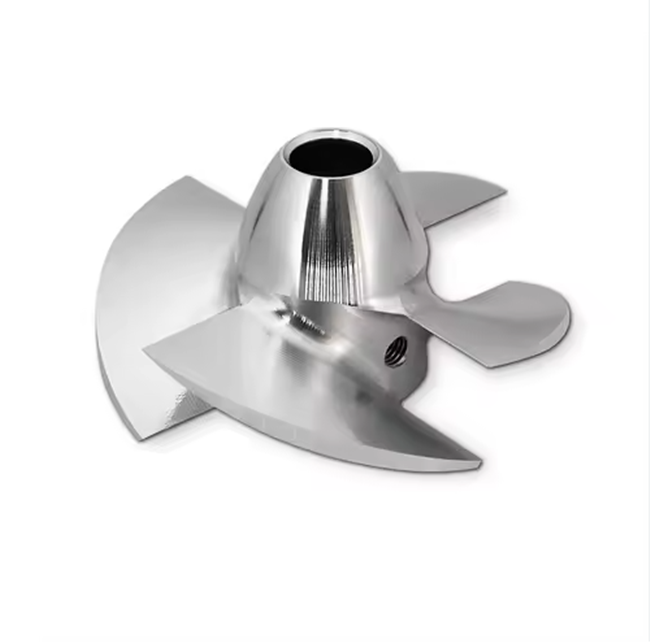
Complex 3/4/5-axis milling for aerodynamic and hydrodynamic fluid mechanics. Extreme cavitational erosion and saltwater resistance for marine and defense vessels.
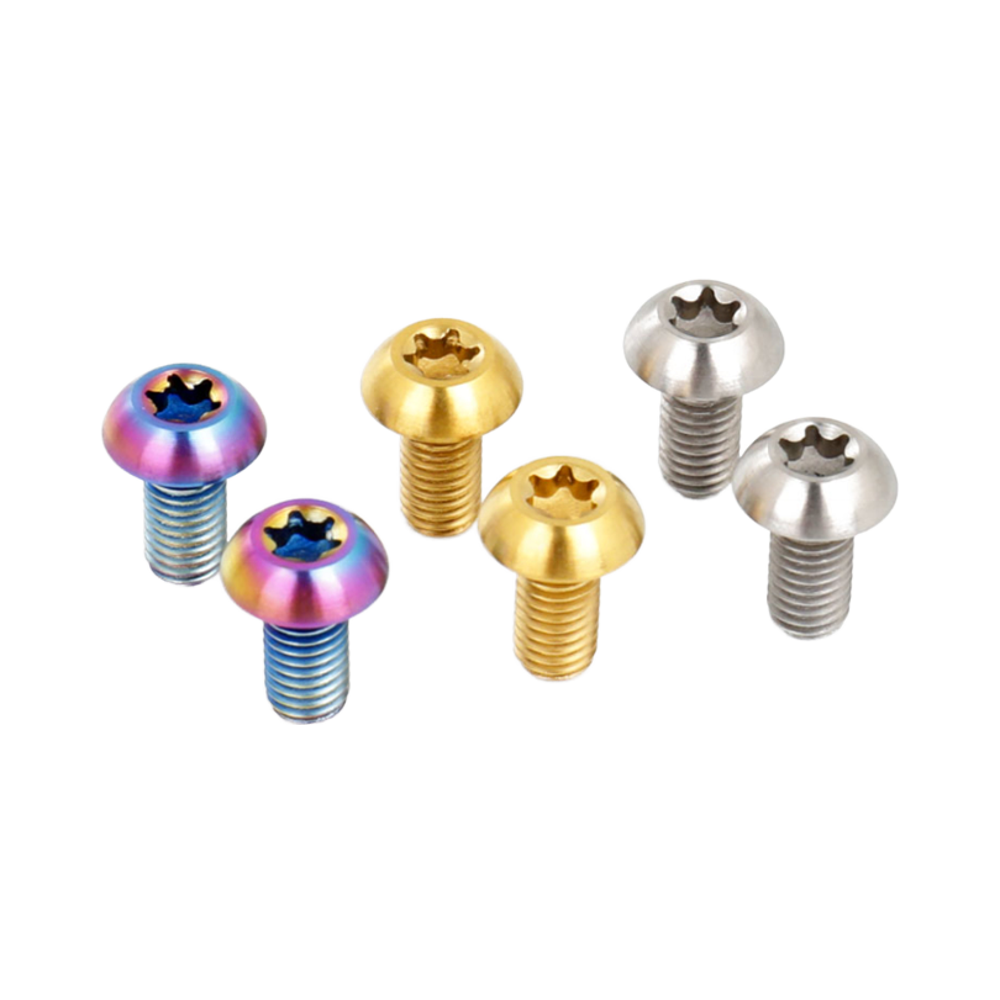
Polished Grade 5 alloy bicycle brake rotor bolts. Delivers unyielding clamping pressure, zero corrosion in wet trail environments, and micro-precision rolled threads.
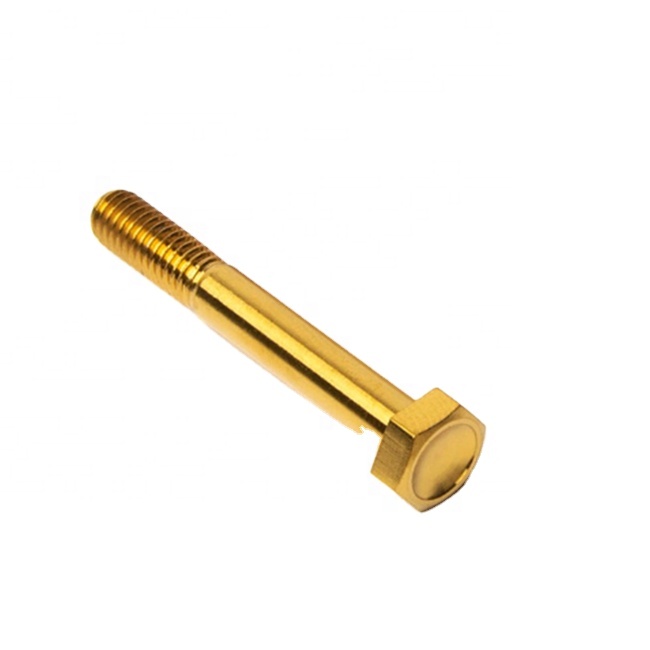
Forged Grade 5 bumper bolts engineered for sprint car and midget micro chassis. High shear rating, continuous internal grain flow, and superior impact tolerance.
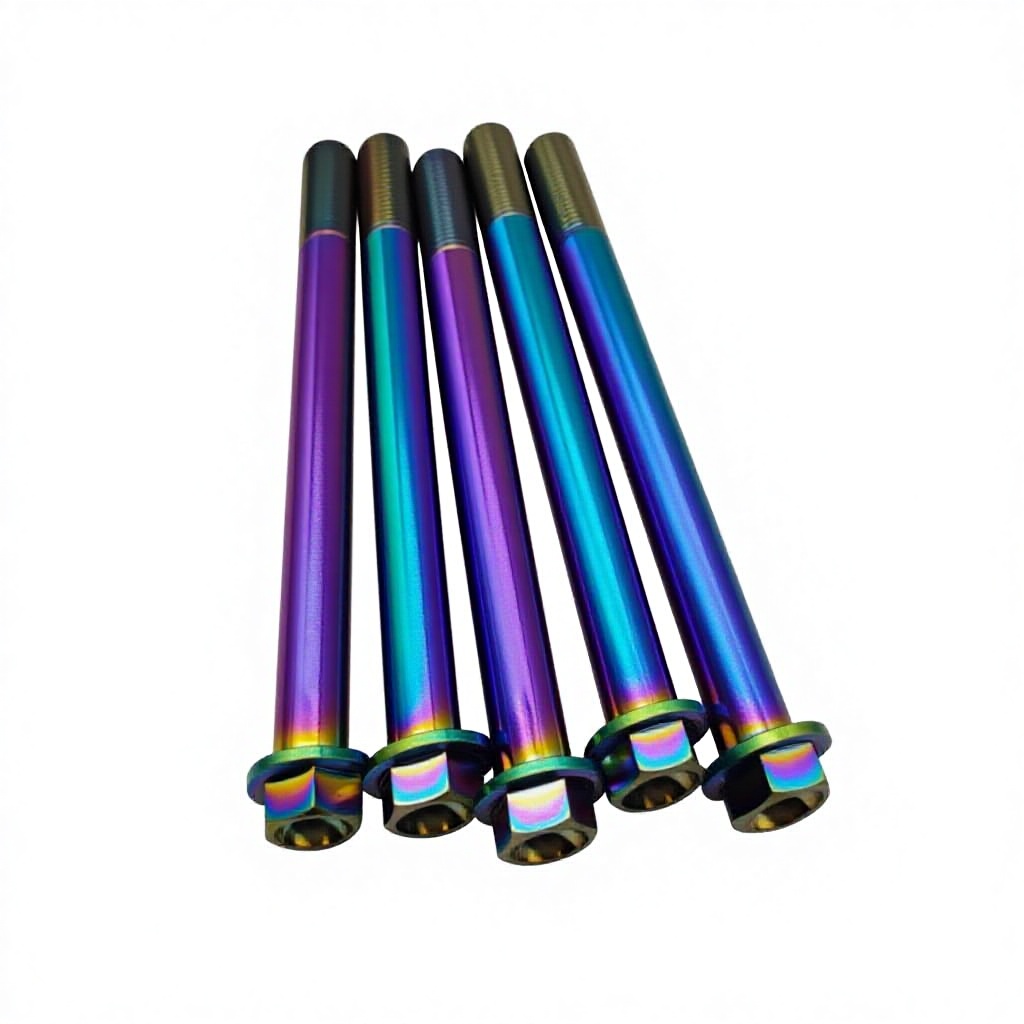
Premium Grade 5 hex flange fasteners with PVD/anodized coating options. Widely utilized in racing powertrain, suspension, and high-vibration engine mount interfaces.
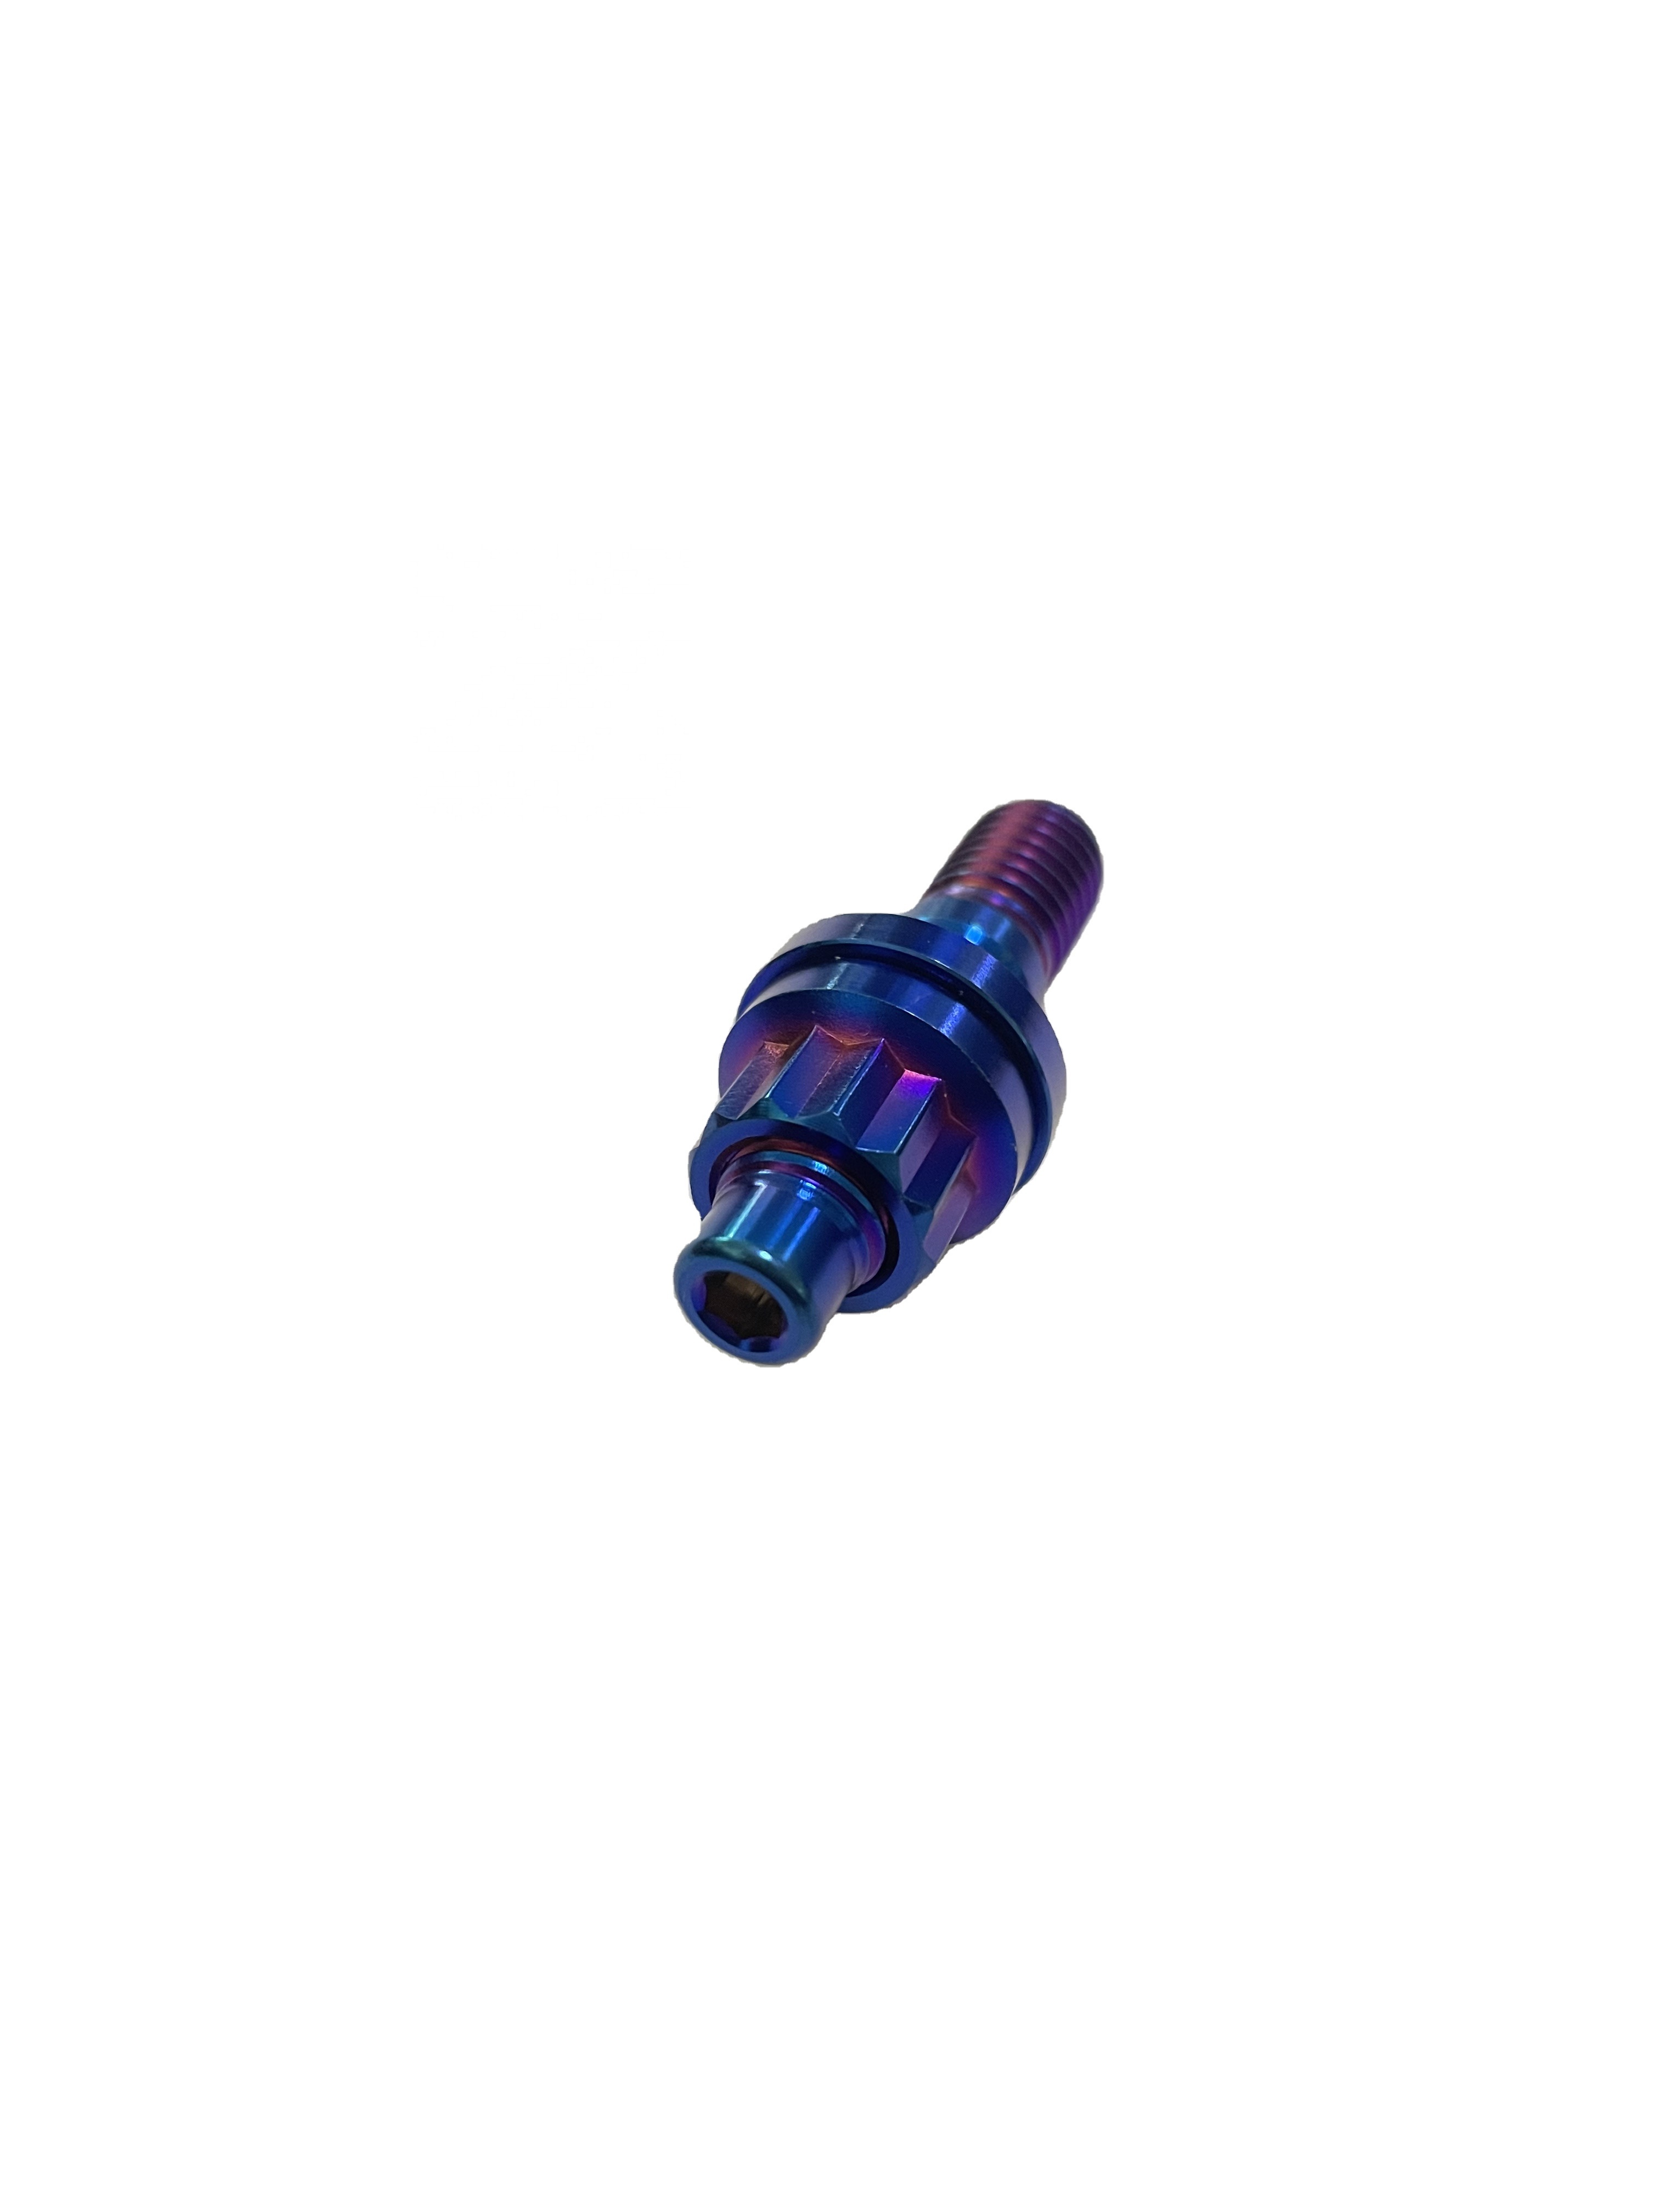
Thermal-expansion-matched exhaust studs resisting recurring heat-soak cycles and seizing. Prevents cylinder head thread stripping in turbocharged motorsports.
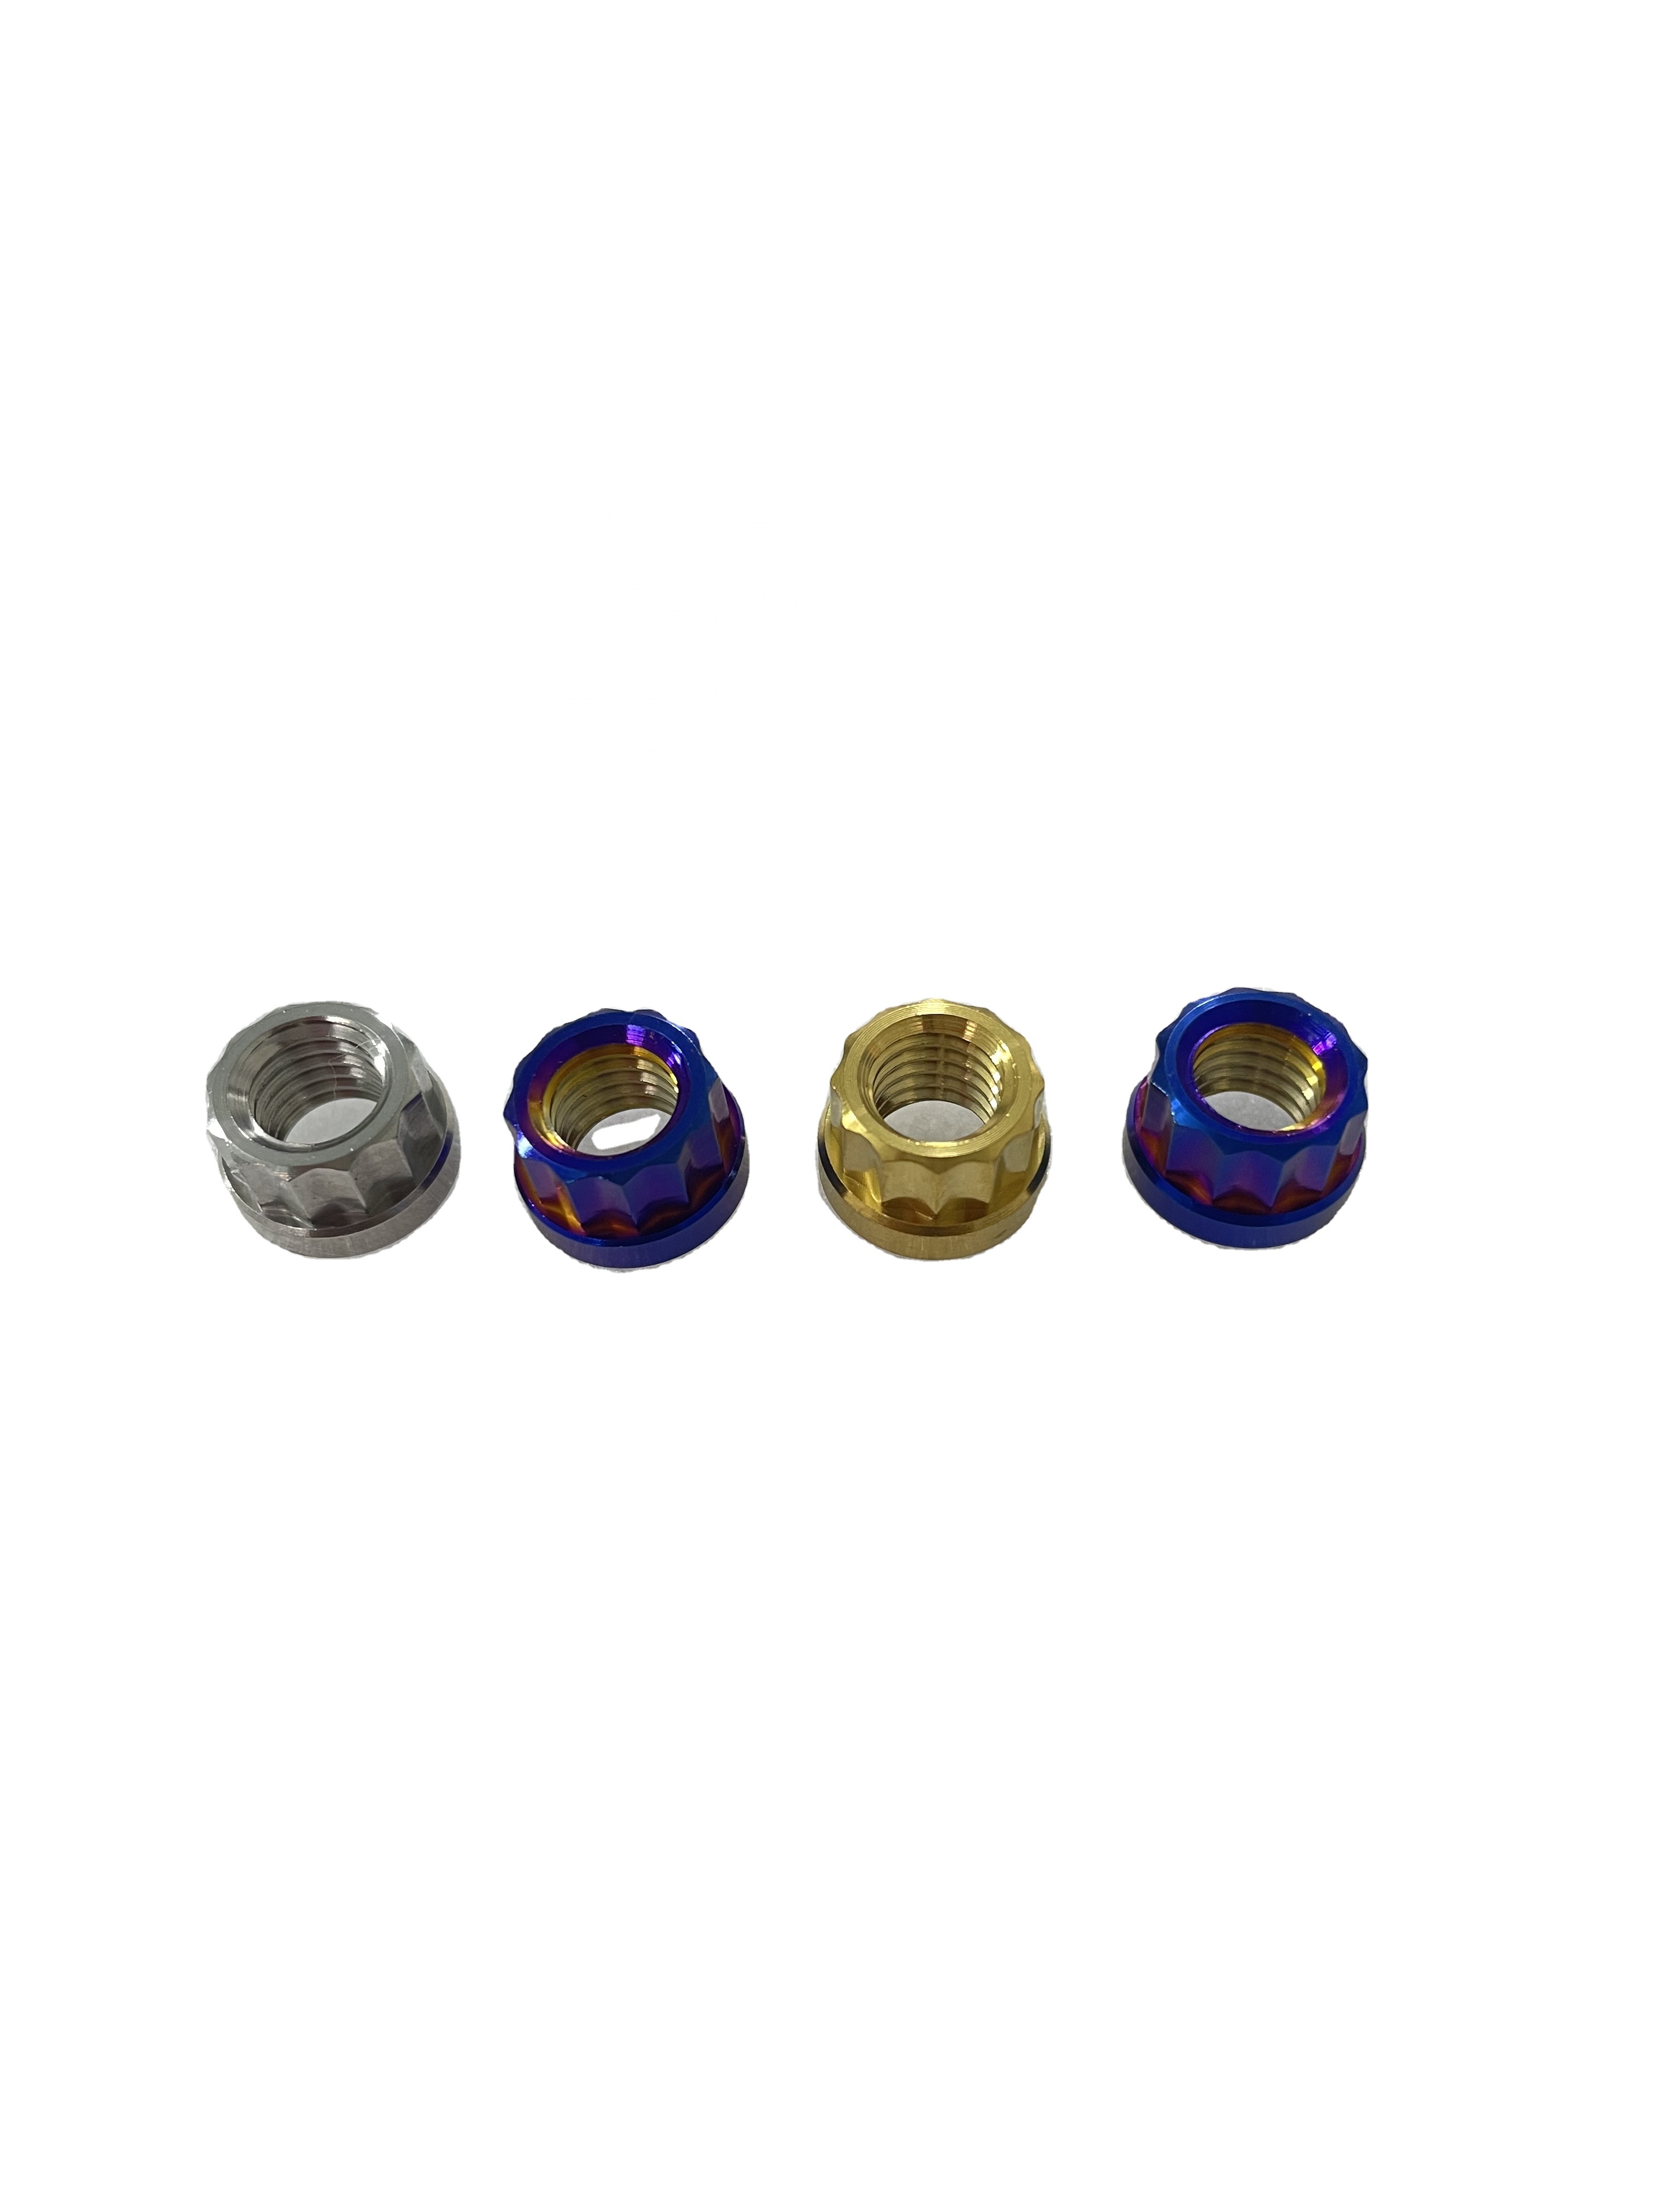
Lightweight jet-style 12-point design distributing extreme wrenching torques without corner rounding. Reduced skirt diameter allows installation in compact spaces.
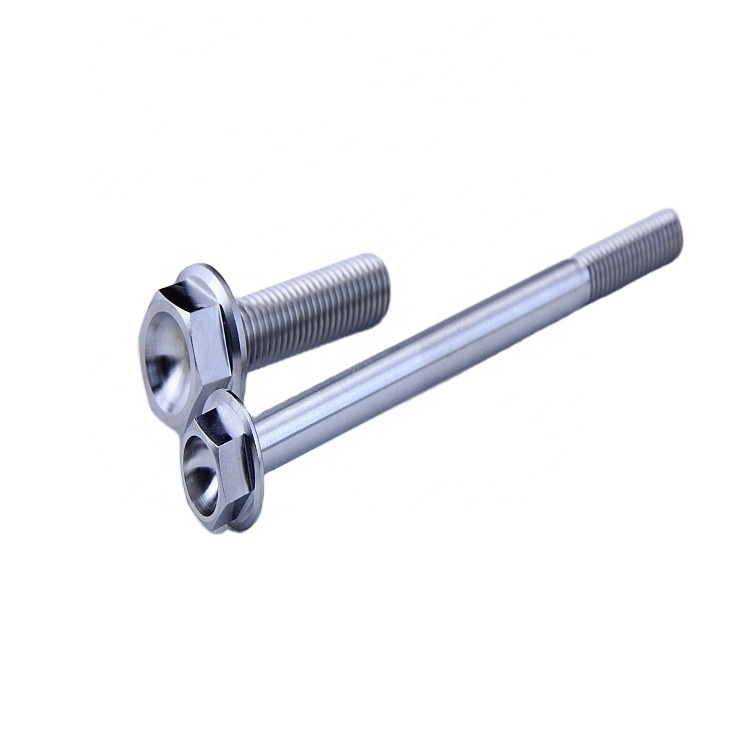
Custom engineered Torx drive bolts for WorldSBK and track applications. Featuring hollowed shank architectures for aggressive unsprung weight optimization.
Optimizing Titanium Alloys for Fastener & Hardware Performance
A rigorous metallurgical comparison of commercial pure and dual-phase alpha-beta titanium alloys for critical load-bearing assemblies.
In high-stress mechanical engineering, specifying OEM custom hardware demands a thorough comprehension of physical metallurgy. Titanium is distinguished by its extraordinary strength-to-weight ratio (specific strength), superior corrosion immunity in aggressive chloride and marine environments, and high fatigue endurance limit. At our Baoji manufacturing facility, we engineer fasteners and precision hardware utilizing raw material originating from virgin titanium sponge, eliminating interstitial defect clusters before bar extrusion or precision wire drawing occurs.
| Material Grade | UNS / Standard | Microstructure | Min Tensile (MPa) | Min Yield (MPa) | Core Application Suitability |
|---|---|---|---|---|---|
| Grade 2 (CP-Ti) | UNS R50400 / ASTM B348 | Alpha Phase (α) | ≥ 345 | ≥ 275 | Chemical processing, marine non-structural fittings, anodizing jigs, high ductility exhaust piping. |
| Grade 5 (Ti-6Al-4V) | UNS R56400 / TC4 | Alpha-Beta (α+β) | ≥ 895 | ≥ 828 | High-performance racing bolts, engine head studs, caliper pins, wheel lug nuts, chassis hardware. |
| Grade 23 (Ti-6Al-4V ELI) | UNS R56401 / ASTM F136 | Extra-Low Interstitial | ≥ 860 | ≥ 795 | Medical implants, bone screws, deep subsea robotics, extreme cryogenic pressure hardware. |
| Grade 9 (Ti-3Al-2.5V) | UNS R56320 / ASTM B338 | Near Alpha (α) | ≥ 620 | ≥ 483 | Hydraulic high-pressure lines, cycling frames, lightweight hollow tie-rods, marine fluid systems. |
| CoCrMo Dental Alloy | ASTM F75 / ISO 5832-4 | Cobalt-Chromium Matrix | ≥ 900 | ≥ 600 | Biomedical prosthetics, custom dental superstructure abutments, high-wear medical hardware. |
The preeminent workhorse of structural titanium hardware is Ti6Al4V Grade 5 (TC4). By alloy balancing 6% aluminum (an alpha stabilizer augmenting high-temperature strength) with 4% vanadium (a beta stabilizer enhancing ductility and fracture toughness), Grade 5 delivers mechanical tensile performance on par with Class 10.9 quench-and-tempered alloy steels, while cutting structural mass by approximately 44% (density of 4.43 g/cm³ versus 7.85 g/cm³).
Furthermore, titanium exhibits an elastic modulus of roughly 110 GPa—nearly half that of structural carbon steel (210 GPa). When designed as OEM engine cylinder head studs or turbocharger manifold fasteners, this controlled mechanical flexibility acts as an internal spring reservoir. Under violent combustion thermal cycles, titanium fasteners absorb dimensional thermal expansions without exceeding their elastic yield threshold or pulling the internal female threads from aluminum engine blocks.
Rolled Threads vs. Cut Threads: The Physics of Fatigue Life
Why production methodology dictates cyclic lifespan and shear threshold in mission-critical hardware.
Precision Thread Rolling
At Vunza Titanium, high-fatigue bolts undergo precision cold or warm thread rolling rather than single-point lathe cutting. Thread rolling dies plastically displace the titanium grain flow, creating uninterrupted crystalline streamlines contouring through the root, flank, and crest. This induces high compressive residual stresses in the thread roots, elevating dynamic fatigue life by 30% to 50% compared to cut threads.
Hot Forged Bolt Heads
For critical 12-point jet nuts, bumper studs, and suspension eye-bolts, induction-assisted hot forging consolidates the internal metallurgy of the bolt head. Continuous radial grain flow eliminates micro-void shear weaknesses at the head-to-shank under-head radius, preventing catastrophically brittle head-shearing failures under sudden multi-axis shock loading.
5-Axis Synchronized Turning
Components requiring multi-planar geometries, eccentric bores, weight-relieving shank pockets, or turbine impeller profiles are processed on our 34 multi-axis CNC centers. Machined under dedicated high-pressure coolant delivering specialized ester lubricants, we prevent tool-workpiece thermal sticking, ensuring surface roughness limits down to Ra 0.4 μm.
Why Tier-1 Engineers Source From Vunza Titanium
Direct manufacturing prowess located in the heart of Gaoya Village Industrial Zone, Baoji, Shaanxi.
Integrated Baoji Supply Ecosystem
Adjacent to the national Baoti Group Industrial Park, our direct access to premium melted ingots and raw titanium billets guarantees consistent chemistry and minimizes raw material supply volatility.
34 Multi-Axis CNC Workstations
Equipped with 3-axis, 4-axis, and 5-axis simultaneous high-precision turning and milling machinery capable of holding complex part concentricity and true-position within ±0.005 mm.
Veteran Engineering Workforce
Over 50% of our production operators and metrology technicians possess more than 13 years of practical experience machining reactive and refractory metals, ensuring seamless DFM execution.
Sponge-to-Part Quality Traceability
Every single OEM batch is tracked through vacuum melting, forging, precision machining, and inspection. Certified Mill Test Reports (EN 10204 3.1) and dimension sheets are supplied with each export crate.
Rapid DFM & Quote Response
Our bilingual application engineers deliver comprehensive Design for Manufacturability (DFM) drawing assessments, tolerance reviews, and formal quotations typically within 9 operating hours.
Advanced Surface Treatments
In-house decorative and tribological functional coatings including vacuum PVD (TiN gold, TiCN black, Oil-Slick rainbow), micro-arc oxidation, Type II anodizing, and molybdenum anti-galling coatings.
OEM Titanium Hardware Procurement Trends (2025–2030)
Strategic directions reshaping procurement decisions across automotive, eVTOL, marine, and industrial sectors.
Unsprung Mass Reduction in EV & Hybrid Hypercars
With heavy lithium and solid-state traction batteries driving vehicle curb weights higher, Tier-1 automotive developers are mandating titanium hardware across uprights, hub assemblies, and multi-link suspensions to preserve dynamic handling and reduce rotational inertia.
eVTOL & Urban Air Mobility Airframe Scaling
Emerging electric vertical takeoff and landing aircraft demand fastener weight budgets approaching aerospace standards but at commercial automotive volume economics. Grade 5 titanium Torx flange hardware is supplanting traditional A286 steel fasteners in non-magnetic motor mount structures.
Closed-Loop Swarf & Scrap Metallurgy
International environmental mandates are compelling procurement departments to demand certified supply chain decarbonization. Vunza Titanium is actively implementing segregated titanium machining swarf collection, briquetting, and certified remelting workflows to lower carbon footprints.
Additive-Subtractive Hybrid Fastening Systems
As DMLS 3D printing expands in titanium component prototyping, critical mating surfaces and female threads still mandate CNC milling and rolled-thread inserts. The future belongs to hybrid assemblies integrating 3D-printed titanium structures with high-precision CNC-turned load pins and captive studs.
Frequently Asked Questions on Custom Titanium Hardware
Critical engineering insights addressing galling, torque dynamics, material specifications, and quality verification.
How do you prevent thread galling (cold welding) during titanium hardware installation?
- Surface Engineering: Applying specialized Physical Vapor Deposition (PVD) TiN/DLC coatings, dry-film MoS&sub2; solid lubricants, or micro-arc oxidation to build a resilient interfacial barrier.
- Material Dissimilarity: Pairing Grade 5 titanium bolts with high-hardness bronze, engineered composite inserts, or anti-seize paste containing copper, nickel, or moly compounds during assembly.
- Thread Form Geometries: Micro-finishing thread roots to Ra ≤ 0.4 μm through precision rolling rather than rough cutting, preventing microscopic asperities from interlocking.
What torque values should be applied to Grade 5 titanium bolts compared to standard steel?
Can Vunza Titanium manufacture non-standard threads such as UNF, UNEF, and left-hand pitches?
What non-destructive testing (NDT) and inspection reports accompany custom OEM shipments?
- Material Mill Test Certificate (EN 10204 3.1): Certifying chemical composition (C, Fe, N, O, H, Al, V, Ti balance) via optical emission spectroscopy and mechanical tensile/yield tests.
- Dimensional Metrology Report: CMM multi-point reports, optical comparator profile overlays, and Go/No-Go pitch micrometer readings.
- Surface & Crack Inspection: Fluorescent Liquid Penetrant Inspection (PT) according to ASTM E1417 to ensure zero microscopic surface fissures on forged bolt heads.
What is the practical turnaround time for rapid prototyping versus volume OEM production?
Why is Baoji considered the premier epicenter for global titanium hardware sourcing?
Ready to Engineer Your Custom OEM Titanium Hardware?
Collaborate directly with our senior metallurgists and CNC manufacturing engineers in Baoji. Send us your CAD drawings (STEP, IGES, DXF, or PDF), specify your target alloy grade, quantity, and surface finish, and receive a comprehensive manufacturability analysis within 9 business hours.