High-Performance Titanium Fasteners & Precision Components
Manufactured to aerospace, high-speed motorsport, and marine tolerances down to ±0.005 mm from China's Titanium Valley.
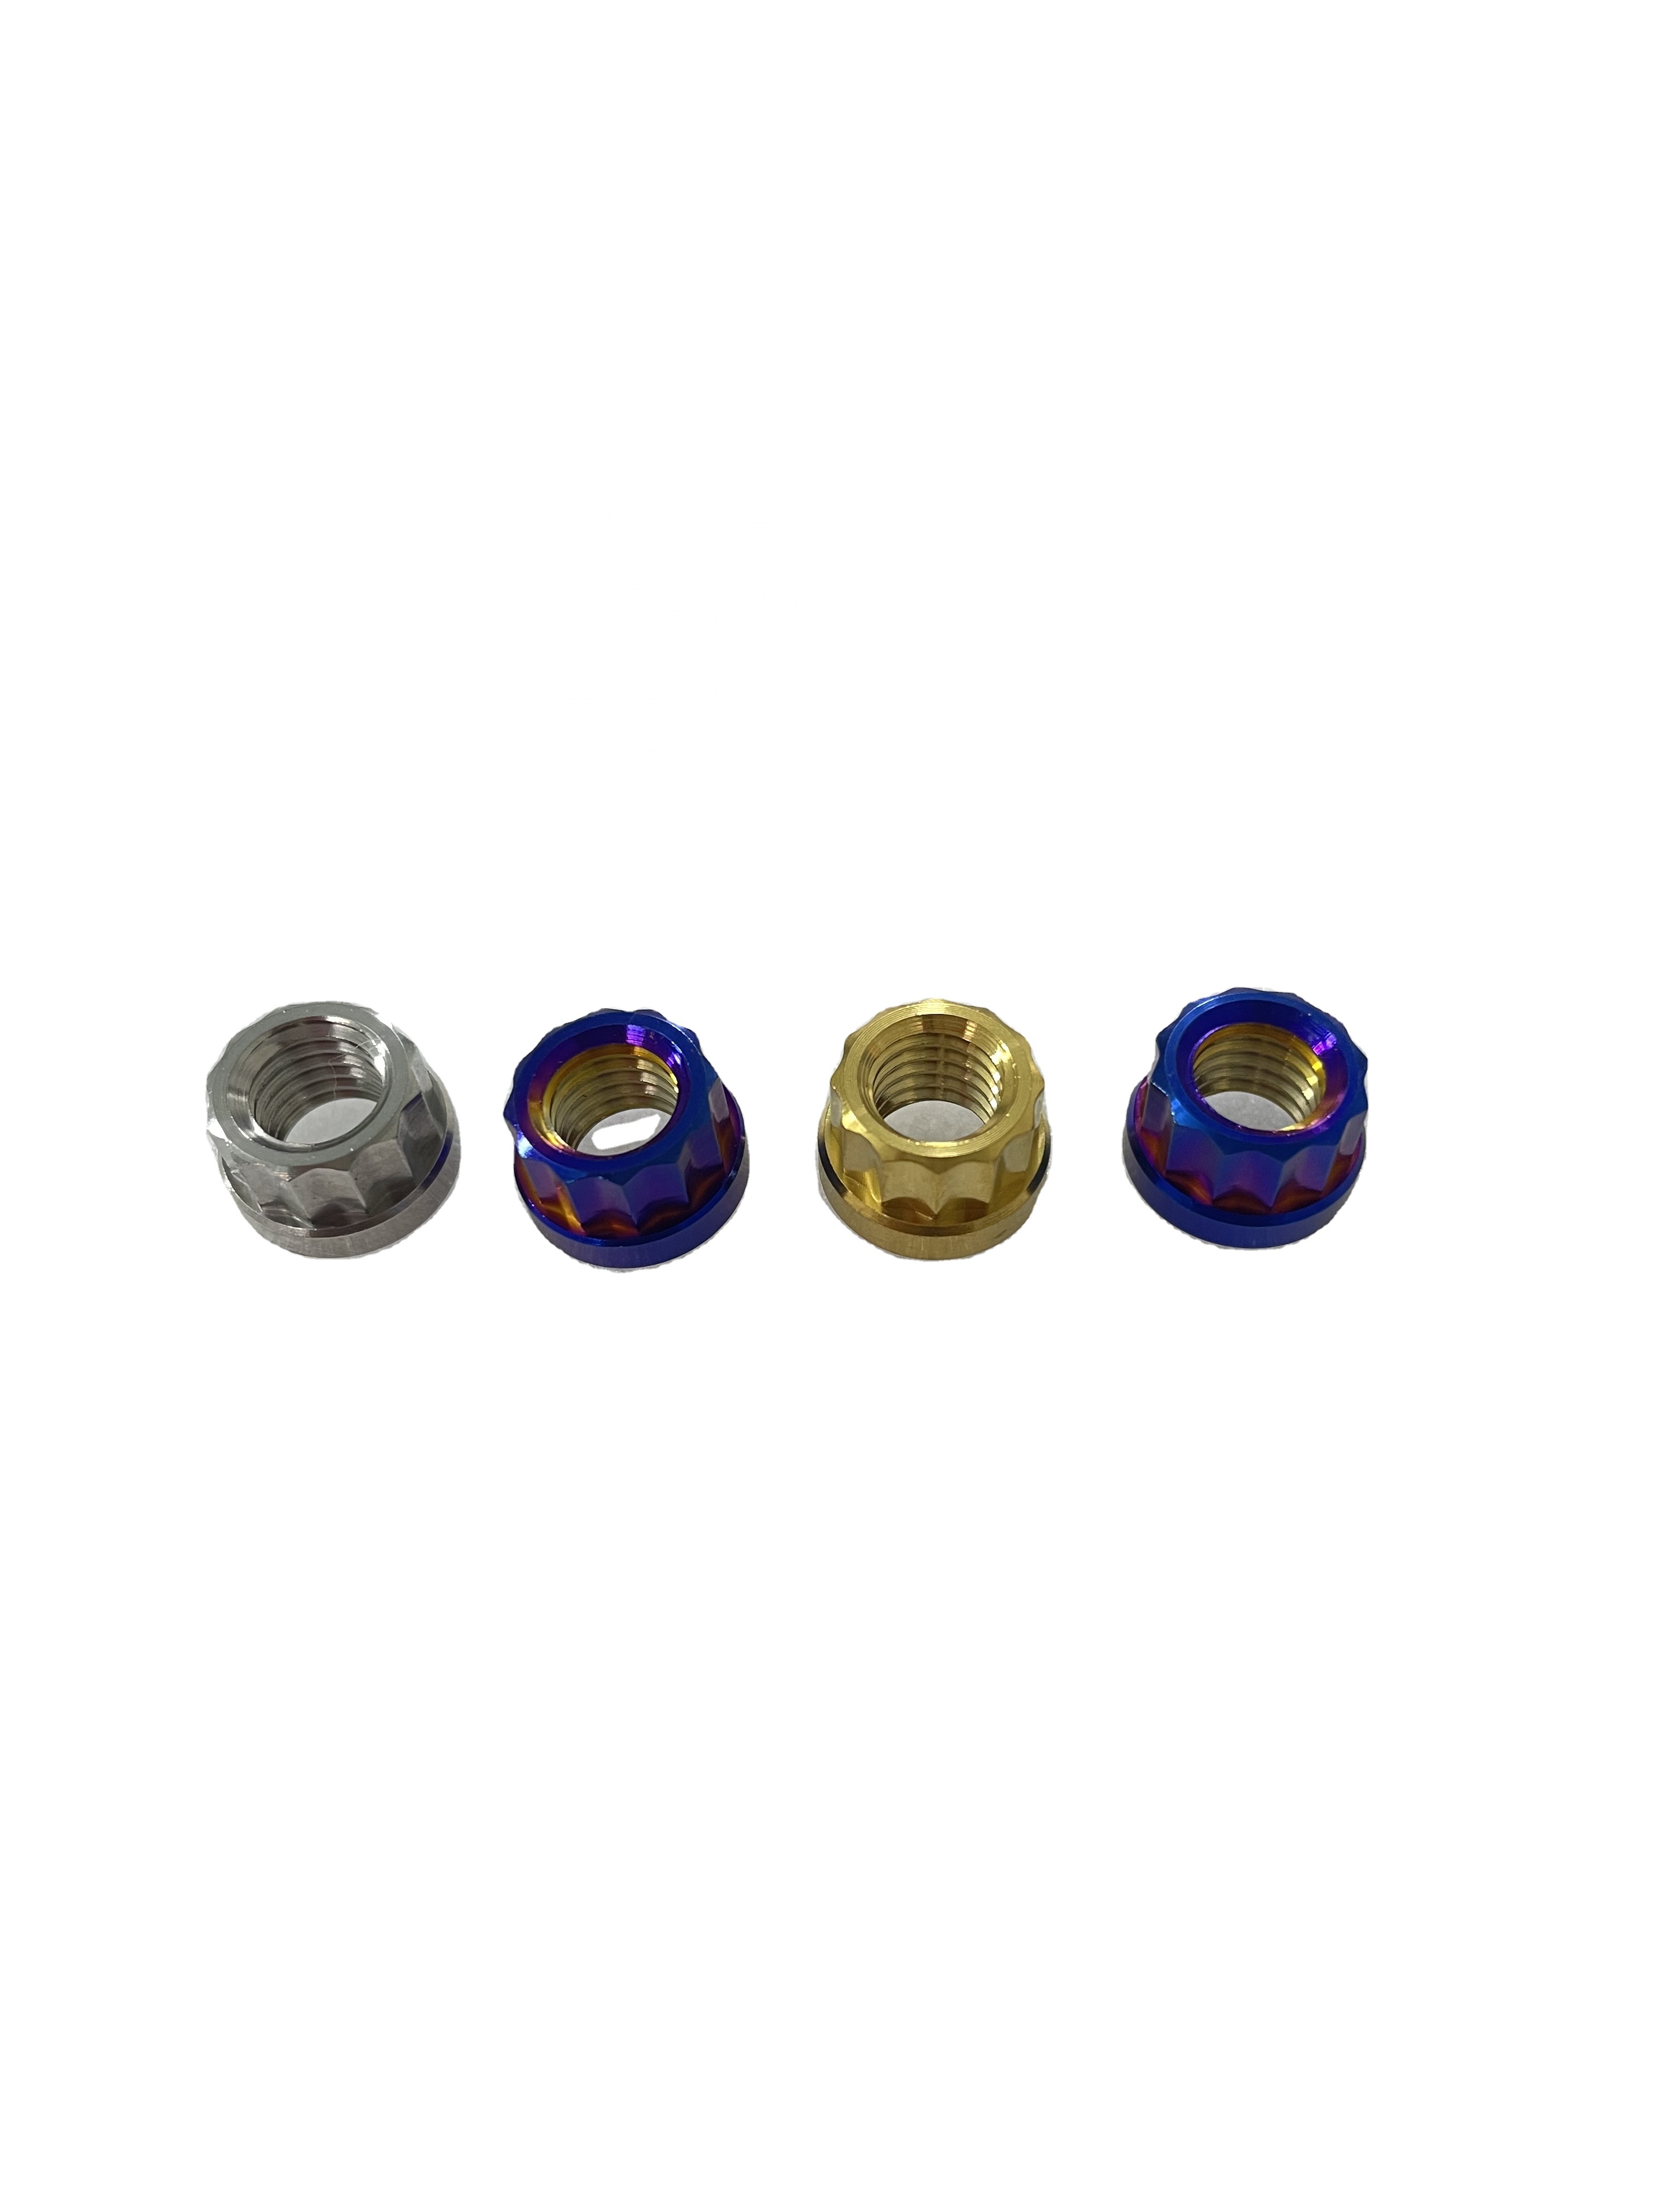
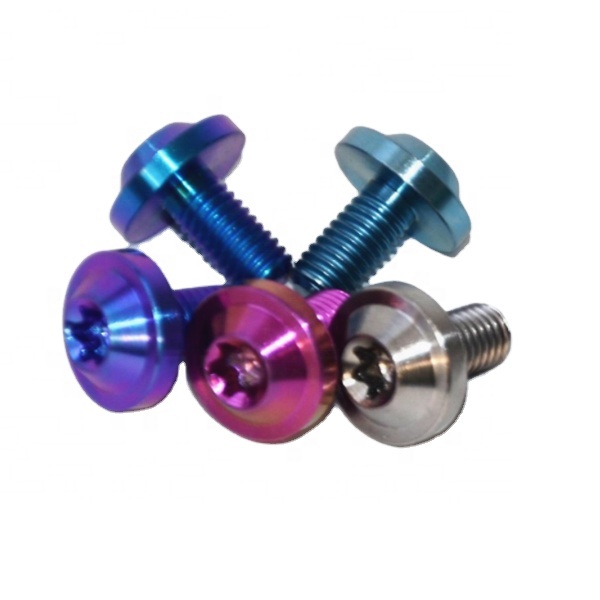
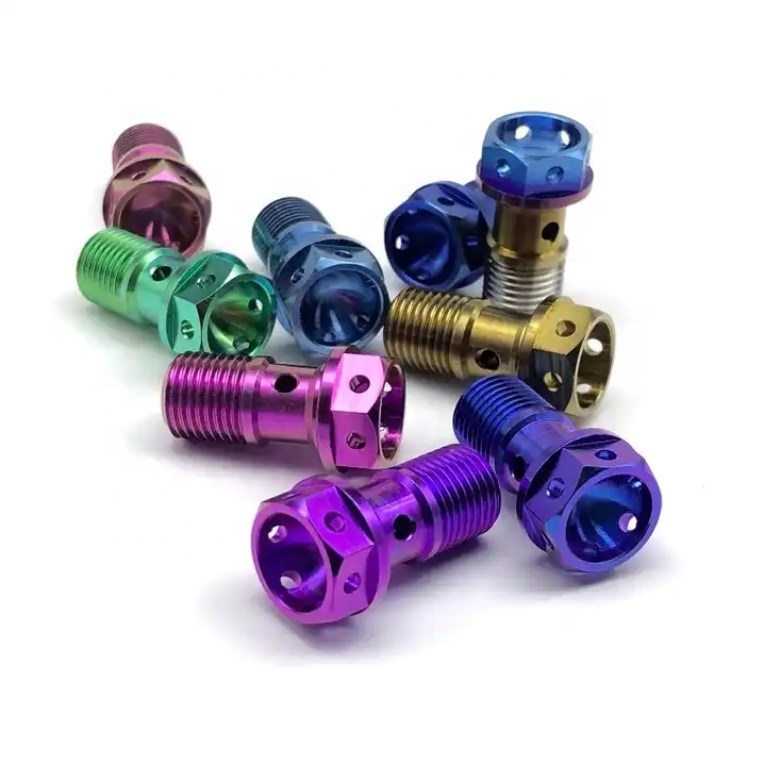
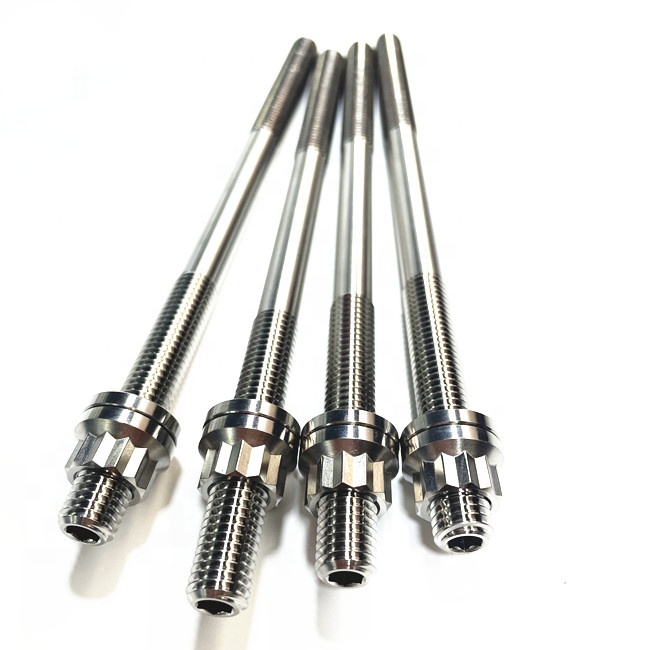
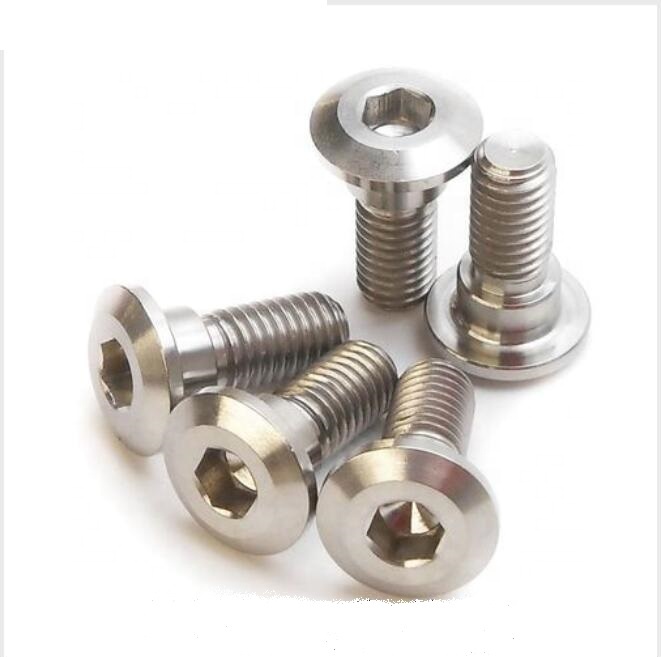
1. Engineering Architecture of Titanium Button Head Screws (ISO 7380 / ASME B18.3)
Titanium button head screws (frequently categorized under ISO 7380-1 for standard low-profile configurations and ISO 7380-2 for integrated flanged variants) occupy an indispensable engineering niche across mission-critical assemblies. Featuring a broad, dome-shaped head that distributes clamp force across a wider surface area while presenting a streamlined profile, these fasteners prevent catch points in high-vibration dynamic environments such as motorsport suspension linkages, aerospace avionics housings, and marine drivetrain assemblies.
Unlike standard cylindrical socket head cap screws (DIN 912), the button head geometry intentionally thins the head height while broadening the under-head bearing diameter. When engineered from Ti-6Al-4V Grade 5 (UNS R56400 / Werkstoff 3.7165), the fastener achieves an extraordinary strength-to-weight balance: with a typical mass density of 4.43 g/cm³, it yields an approximate 44% to 46% mass reduction compared to 10.9 or 12.9 grade alloy steel, whilst delivering an ultimate tensile strength exceeding 895–950 MPa.
Metallurgical Core: Why Ti-6Al-4V Grade 5 Trumps Grade 2 Commercially Pure Titanium
While Grade 2 commercially pure titanium is exceptionally chemically stable in chlorinated brine, it lacks the mechanical yield capacity required for dynamic preloads (Yield Strength: ~275 MPa). Ti-6Al-4V features an alpha-beta duplex microstructure stabilized by 6% Aluminum (alpha stabilizer raising high-temperature strength) and 4% Vanadium (beta stabilizer promoting lattice ductibility and shear resistance), enabling cold-heading shear limits over 550 MPa and an elastic modulus of 114 GPa that dampens harmonic shock waves.
2. Thread-Forming Mechanics: Cut vs. Cold-Rolled Threads
For top-tier industrial procurement, how thread geometry is produced dictates fatigue resistance. In low-cost manufacturing, thread roots are produced through multi-axis CNC single-point turning or subtractive thread milling. While mill threading satisfies low-stress applications, it cuts through the crystalline grain flow of the titanium bar, introducing microscopic notch-stress risers at the root radii.
In contrast, aerospace-grade titanium button head suppliers utilize hot or warm rolling processes below the beta-transus temperature (~995°C). Thread rolling plastically deforms the titanium crystal structure, orienting grain boundaries continuously along the thread crests and root radii. This burnishing work-hardens root surfaces, eliminates micro-cracks, and expands cyclic fatigue endurance by 300% to 500% under high-frequency load-reversal environments.
| Mechanical & Physical Property | Ti-6Al-4V Grade 5 Fastener | Class 10.9 Alloy Steel | 316L Marine Stainless Steel |
|---|---|---|---|
| Density (g/cm³) | 4.43 (Ultralight weight) | 7.85 | 8.00 |
| Yield Strength Rp0.2 (MPa) | ≥ 828 (Tested: 860–920) | 900 | 220 |
| Tensile Strength Rm (MPa) | ≥ 895 (Tested: 950–1050) | 1040 | 580 |
| Shear Strength (MPa) | ≥ 550 | 620 | 350 |
| Modulus of Elasticity (GPa) | 114 (Superior dampening) | 210 | 193 |
| Pitting Resistance Equivalent (PREN) | Immune to ambient saltwater | < 10 (Prone to rust) | 23–25 (Susceptible in crevice) |
3. Drive Configurations: Hex Socket (Allen) vs. Torx (6-Lobe / Torx Plus)
A crucial engineering challenge unique to button head screws is internal recess depth. Because the button head is shallow by design, the socket depth is shallower than that of standard DIN 912 socket caps. When driven by conventional hexagonal allen keys, insufficient engagement depths coupled with high installation torques lead to recess cam-out and drive wall strip-out.
State-of-the-art procurement trends favor Torx (ISO 10664) and patented Torx Plus drive geometries. The 15° drive angle of hex drives induces excessive radial splitting forces that flare out thin button heads. In contrast, 6-lobe Torx designs provide an elliptical interface with virtually a 0° drive angle, transmitting 100% of torque into circumferential clamping force without tool slippage, making them ideal for high-speed robotic assembly lines.
Top 10 Titanium Button Head Screws Manufacturers & Suppliers
A rigorous comparative audit evaluating global supply chain robustness, CNC multi-axis infrastructure, metallurgical verification, and export credentials.
Vunza Titanium Industry
LISI Aerospace
Arconic Fastening Systems
Pro-Bolt Motorsport Hardware
BRP Fastener Group
SPS Technologies (PCC)
Ticon Industries
Titanium Processing Center
Top Titanium Metal
Torq Titanium Hardware
Future Procurement & Technological Trends in Titanium Fasteners
Strategic analysis into how global supply dynamics, generative design, surface coatings, and regulatory mandates are reshaping enterprise procurement.
Supply Chain Regionalization
Global procurement teams are shifting away from intermediate brokerage distributors toward direct-from-source clusters like Baoji, China (holding over 60% of domestic titanium reserves and smelting facilities). This secures mill-level lot traceability, minimizes raw material tariffs, and mitigates geopolitical disruption risk.
Hybrid Additive-Subtractive CNC
Complex low-profile button head components with internal weight-saving cavities or internal sensor channels are transitioning to hybrid manufacturing: 3D printing of near-net shapes via Electron Beam Melting (EBM) followed by 5-axis CNC thread rolling and underhead seat finishing to 0.005 mm.
Next-Gen PVD DLC Coatings
To overcome titanium's intrinsic tendency toward galling under repetitive dynamic shear, Physical Vapor Deposition (PVD) Diamond-Like Carbon (DLC) and Titanium Nitride (TiN) coatings are becoming baseline procurement specs, offering surface hardness ratings exceeding 2500 HV with friction coefficients below 0.1.
Digital Material Passports
Aerospace and medical buyers now mandate digital material passports. Fastener batches are laser-etched with micro 2D DataMatrix codes linking directly to chemical spectrometry, ultrasonic non-destructive testing (NDT), and tensile pull records recorded during production.
Why Tier-1 Engineers Choose Vunza Titanium Industry
Direct manufacturing prowess located in Gaoya Village Industrial Zone, Baoji, Shaanxi — China's Titanium Valley.
Years in Production
Founded in 2008, delivering specialized fastener metallurgy, racing parts, and precision CNC components for over 15 continuous years.
Multi-Axis CNC Centers
Advanced 3, 4, and 5-axis turning and milling machinery capable of single-setup compound geometries and micro-tolerances.
Machining Precision
Rigorous dimensional accuracy verified through automated optical measuring projectors, thread pitch micrometers, and surface profilometers.
Senior Master Techs
Over half of our shopfloor machining technicians hold 13+ years of specialized titanium alloy processing experience.
Our integrated supply framework encompasses titanium sponge smelting oversight, vacuum consumable arc remelting (VAR), precision hot forging, thread rolling, multi-axis CNC machining, ultrasonic flaw detection, and in-house color anodizing.
Send an InquiryFrequently Asked Questions on Titanium Button Head Screws
Practical engineering answers covering torque specifications, galling mitigation, standards conformance, and batch testing.
What are the recommended tightening torque values for Grade 5 titanium button head screws? +
How do you prevent galling (cold-welding) during titanium fastener installation? +
What is the functional difference between ISO 7380-1 and ISO 7380-2 button head screws? +
Can titanium button head screws be manufactured to custom dimensions and thread pitches? +
What quality documentation and testing reports are supplied with commercial shipments? +
What is the typical Minimum Order Quantity (MOQ) and production lead time? +
Accelerate Your Engineering Project with Titanium Valley Direct Supply
Upload your 2D/3D part drawings or bill of materials today. Our engineering staff in Baoji will evaluate your tolerances, provide a Design-for-Manufacture (DFM) review, and submit a competitive factory-direct quote within 9 hours.