Racing Gr5
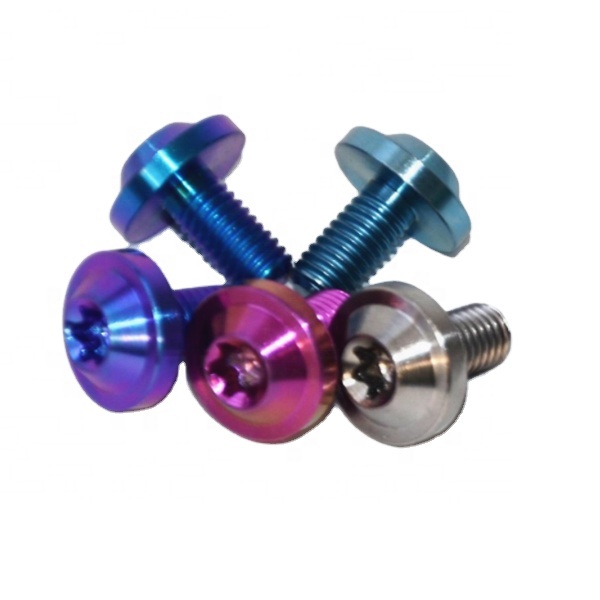
Direct from Baoji—China's Titanium Valley. Custom multi-axis CNC machined titanium T-bolts, flange hardware, wheel studs, and motorsport fasteners engineered for extreme fatigue limits and zero corrosive decay.
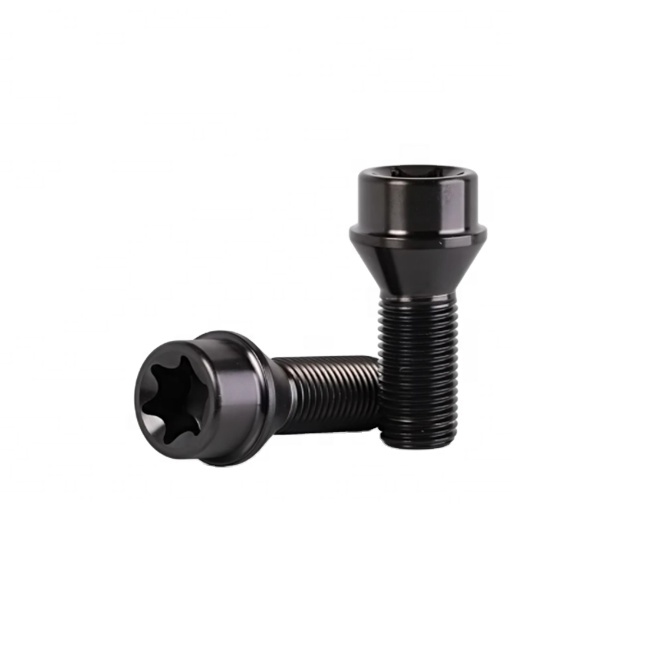
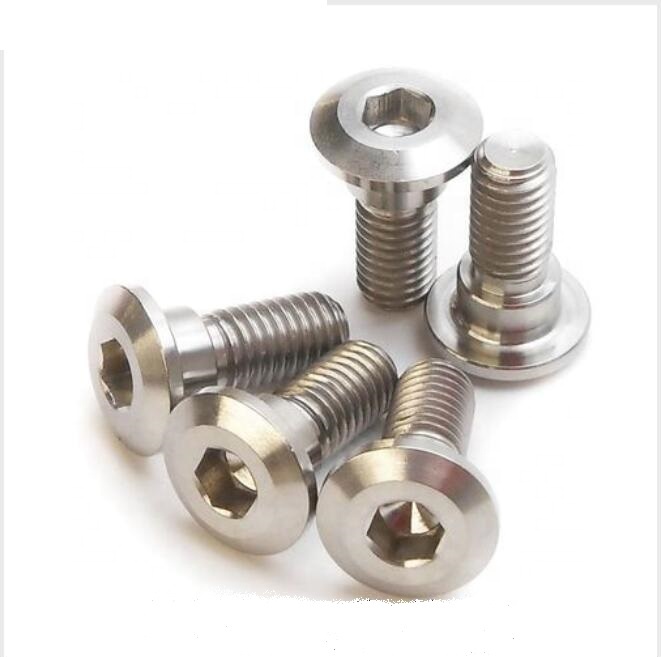
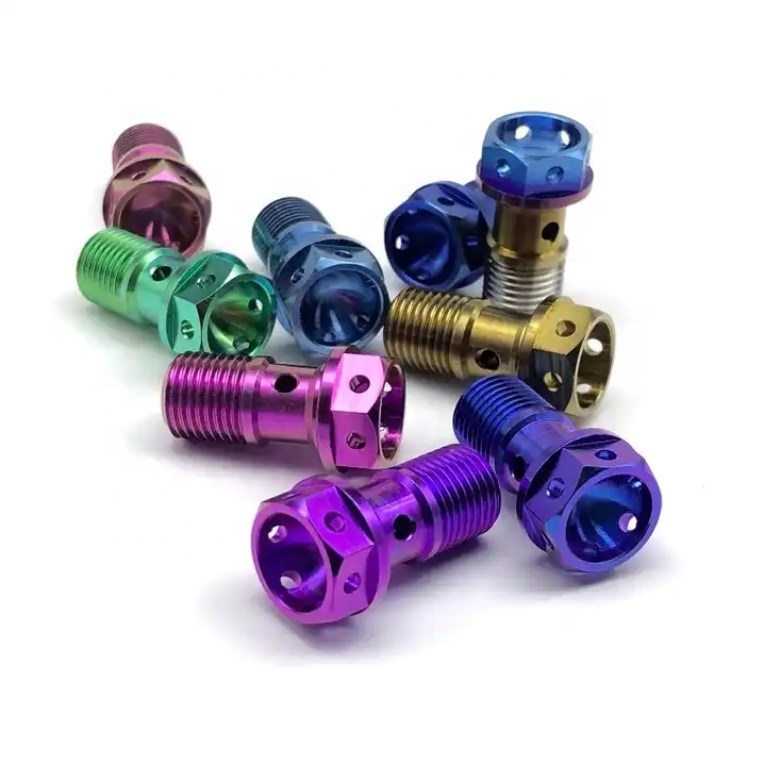

Within mechanical framing systems, CNC aluminum extrusions, automotive turbocharger brackets, marine track sliders, and cleanroom semiconductor tooling, the humble T-bolt serves as the structural anchor. However, standard austenitic stainless steel (such as 304 or 316) and zinc-plated Grade 8.8 structural steels often present fundamental failure modes under intense operating parameters: unacceptable galvanic oxidation, destructive thread galling, weight penalties, and catastrophic shear failures triggered by thermal harmonic vibrations.
When searching for a Top 10 Titanium T Bolts Factory & Supplier, global enterprise buyers do not simply purchase hardware; they secure mechanical safety margins. Modern engineers overwhelmingly transition to Ti-6Al-4V Grade 5 titanium T-bolts to leverage an unmatched strength-to-weight ratio (4.43 g/cm³ density vs. 7.9 g/cm³ steel) combined with yield strengths exceeding 828 MPa and an exceptional natural passivation barrier against aggressive chlorides, caustic solutions, and extreme thermal swings.
Navigating global suppliers requires an acute understanding of metallurgical grading. Fasteners labeled broadly as "titanium" without explicit grade certification introduce serious liabilities in mission-critical environments. Top-tier manufacturers categorize their output based on stringent ASTM, DIN, and ISO metrics:
| Material Grade | Nominal Composition | Tensile Strength (Min) | Yield Strength (Min) | Primary Industrial Applications |
|---|---|---|---|---|
| Grade 2 CP Ti | Commercially Pure Ti (Fe 0.30%, O 0.25%) | ≥ 345 MPa | ≥ 275 MPa | Chemical processing vats, plating racks, low-load marine framing track bolts |
| Grade 5 (TC4) | Ti-6Al-4V (6% Al, 4% V, bal. Ti) | ≥ 895 MPa | ≥ 828 MPa | Motorsport suspension guides, high-boost exhaust clamps, structural CNC frames |
| Grade 23 (ELI) | Ti-6Al-4V Extra Low Interstitial | ≥ 860 MPa | ≥ 795 MPa | Surgical apparatus jigs, medical grade fixtures, aerospace cryogenic locking slots |
| Grade 7 | CP Ti + 0.12–0.25% Palladium | ≥ 345 MPa | ≥ 275 MPa | Severe hydrochloric and sulfuric acid environments, offshore exploration platforms |
While Grade 2 offers superior ductility and cold-forming ease, structural T-bolt applications demanding extreme clamping forces rely exclusively on Grade 5 Ti-6Al-4V. Grade 5 provides high shear modulus and fatigue limits, ensuring the bolt's rectangular or hammer head holds true without round-off when torqued down into rigid profile channels.
Procurement directors within motorsport engineering, high-end cycling, marine racing, and green technology sectors are adapting to radical shifts in component lifecycles. Based on extensive market analyses, several dominant trends are redefining how enterprise buyers source titanium hardware:
Tier-1 procurement mandates verifiable chain-of-custody protocols from the initial vacuum arc remelted (VAR) titanium sponge ingot directly through to the final CNC machined part. Material Test Reports (MTRs) matching EN 10204 3.1 standards are now non-negotiable for aerospace and motorsports contracts.
Traditional machined (cut) threads sever the alloy's continuous grain boundaries, leaving internal micro-notches vulnerable to cyclic stress fatigue. Global buyers are explicitly stipulating cold-thread-rolling post-heat-treatment, increasing thread shear resistance and fatigue cycle thresholds by over 30%.
Rather than working with fragmented broker networks, original equipment manufacturers are establishing direct supply pipelines with specialized clusters in Baoji, China (China's Titanium Valley), securing deep price advantages, rapid multi-axis prototyping, and unified batch quality control.
Further driving procurement changes is the emergence of hybrid anti-galling PVD coatings. Titanium's natural tendency to gall when torqued against similar metals or stainless steel nuts without anti-seize paste is eliminated through advanced physical vapor deposition: Diamond-Like Carbon (DLC), Titanium Nitride (TiN), and customized multi-spectrum anodization provide surface lubricity while preserving tight tolerances down to 0.005 mm.
The manufacturing architecture of titanium T-bolts has transitioned far beyond simple manual lathe operations. Forward-thinking suppliers leverage integrated industrial ecosystems to achieve unprecedented structural reliability:
State-of-the-art factories employ hot precision forging for the rectangular/hammer head of T-bolts. Heating the Ti-6Al-4V billet to controlled alpha-beta transition temperatures allows grain boundaries to flow naturally around the T-head shoulders. Subsequent 5-axis CNC finishing shapes the critical clamping chamfers, providing a head-to-shank perpendicularity tolerance that prevents localized bending moments when fully loaded.
Modern T-bolts interface with slotted extrusions that withstand severe vibrational pull-out stresses. Using dynamic FEA modeling, leading suppliers engineer micro-radius undercuts beneath the T-bolt head. This design feature disperses mechanical loads evenly across the profile lip, eliminating shear concentration points that commonly crack aluminum tracking channels under dynamic racing or marine conditions.
To eliminate manual inspection variances across production volumes exceeding hundreds of thousands of units, premier suppliers implement telecentric lens-based optical sorting systems. Laser profilometry scans 100% of fastener pitch diameters, root radii, thread angle conformity (60-degree metric or 55-degree Whitworth), and T-head rectangular symmetry at speeds exceeding 400 parts per minute.
Positioned directly within China's Titanium Valley in Baoji, Shaanxi, and situated immediately adjacent to the Baoti Group Industrial Park, Vunza Titanium Industry Co., Ltd. has led precision titanium manufacturing since 2008. Combining an integrated R&D team, heavy-duty production infrastructure, and dedicated sales and after-sales support, Vunza delivers distinct competitive advantages to international buyers:
Equipped with sophisticated 3-axis, 4-axis, and 5-axis simultaneous machining centers, Vunza effortlessly achieves complex geometries, proprietary head form factors, and tight mechanical tolerances down to ±0.005 mm across large production runs.
Over 50% of the active factory workforce possesses more than 13 years of specialized, hands-on experience in exotic refractory alloy processing, custom metallurgy heat-treatment curves, and CNC toolpath optimization for non-standard titanium parts.
Every process cycle—from raw titanium sponge selection and ingot smelting through bar extrusions, CNC turning, thread rolling, PVD anodizing, and multi-point CMM dimensional inspection—is audited under an unbroken traceability quality system.
Supported by a comprehensive annual revenue reaching US$10M–US$50M, Vunza stands as an Onsite-Verified supplier with a consistent 5.0/5 buyer rating, rapid engineering quoting times averaging under 9 hours, and sustained global shipping across the motorsport, aerospace, marine, medical, and high-performance engineering sectors.
Critical inquiries addressed by our technical engineering and procurement management teams:
Connect directly with our Baoji engineering foundry. Whether you require custom Ti-6Al-4V T-bolts, motorsport fasteners, or multi-axis CNC prototype production, our technical team will review your specifications and provide a competitive DFM quote within 9 business hours.
Send an Inquiry