Export Inventory & Custom Production
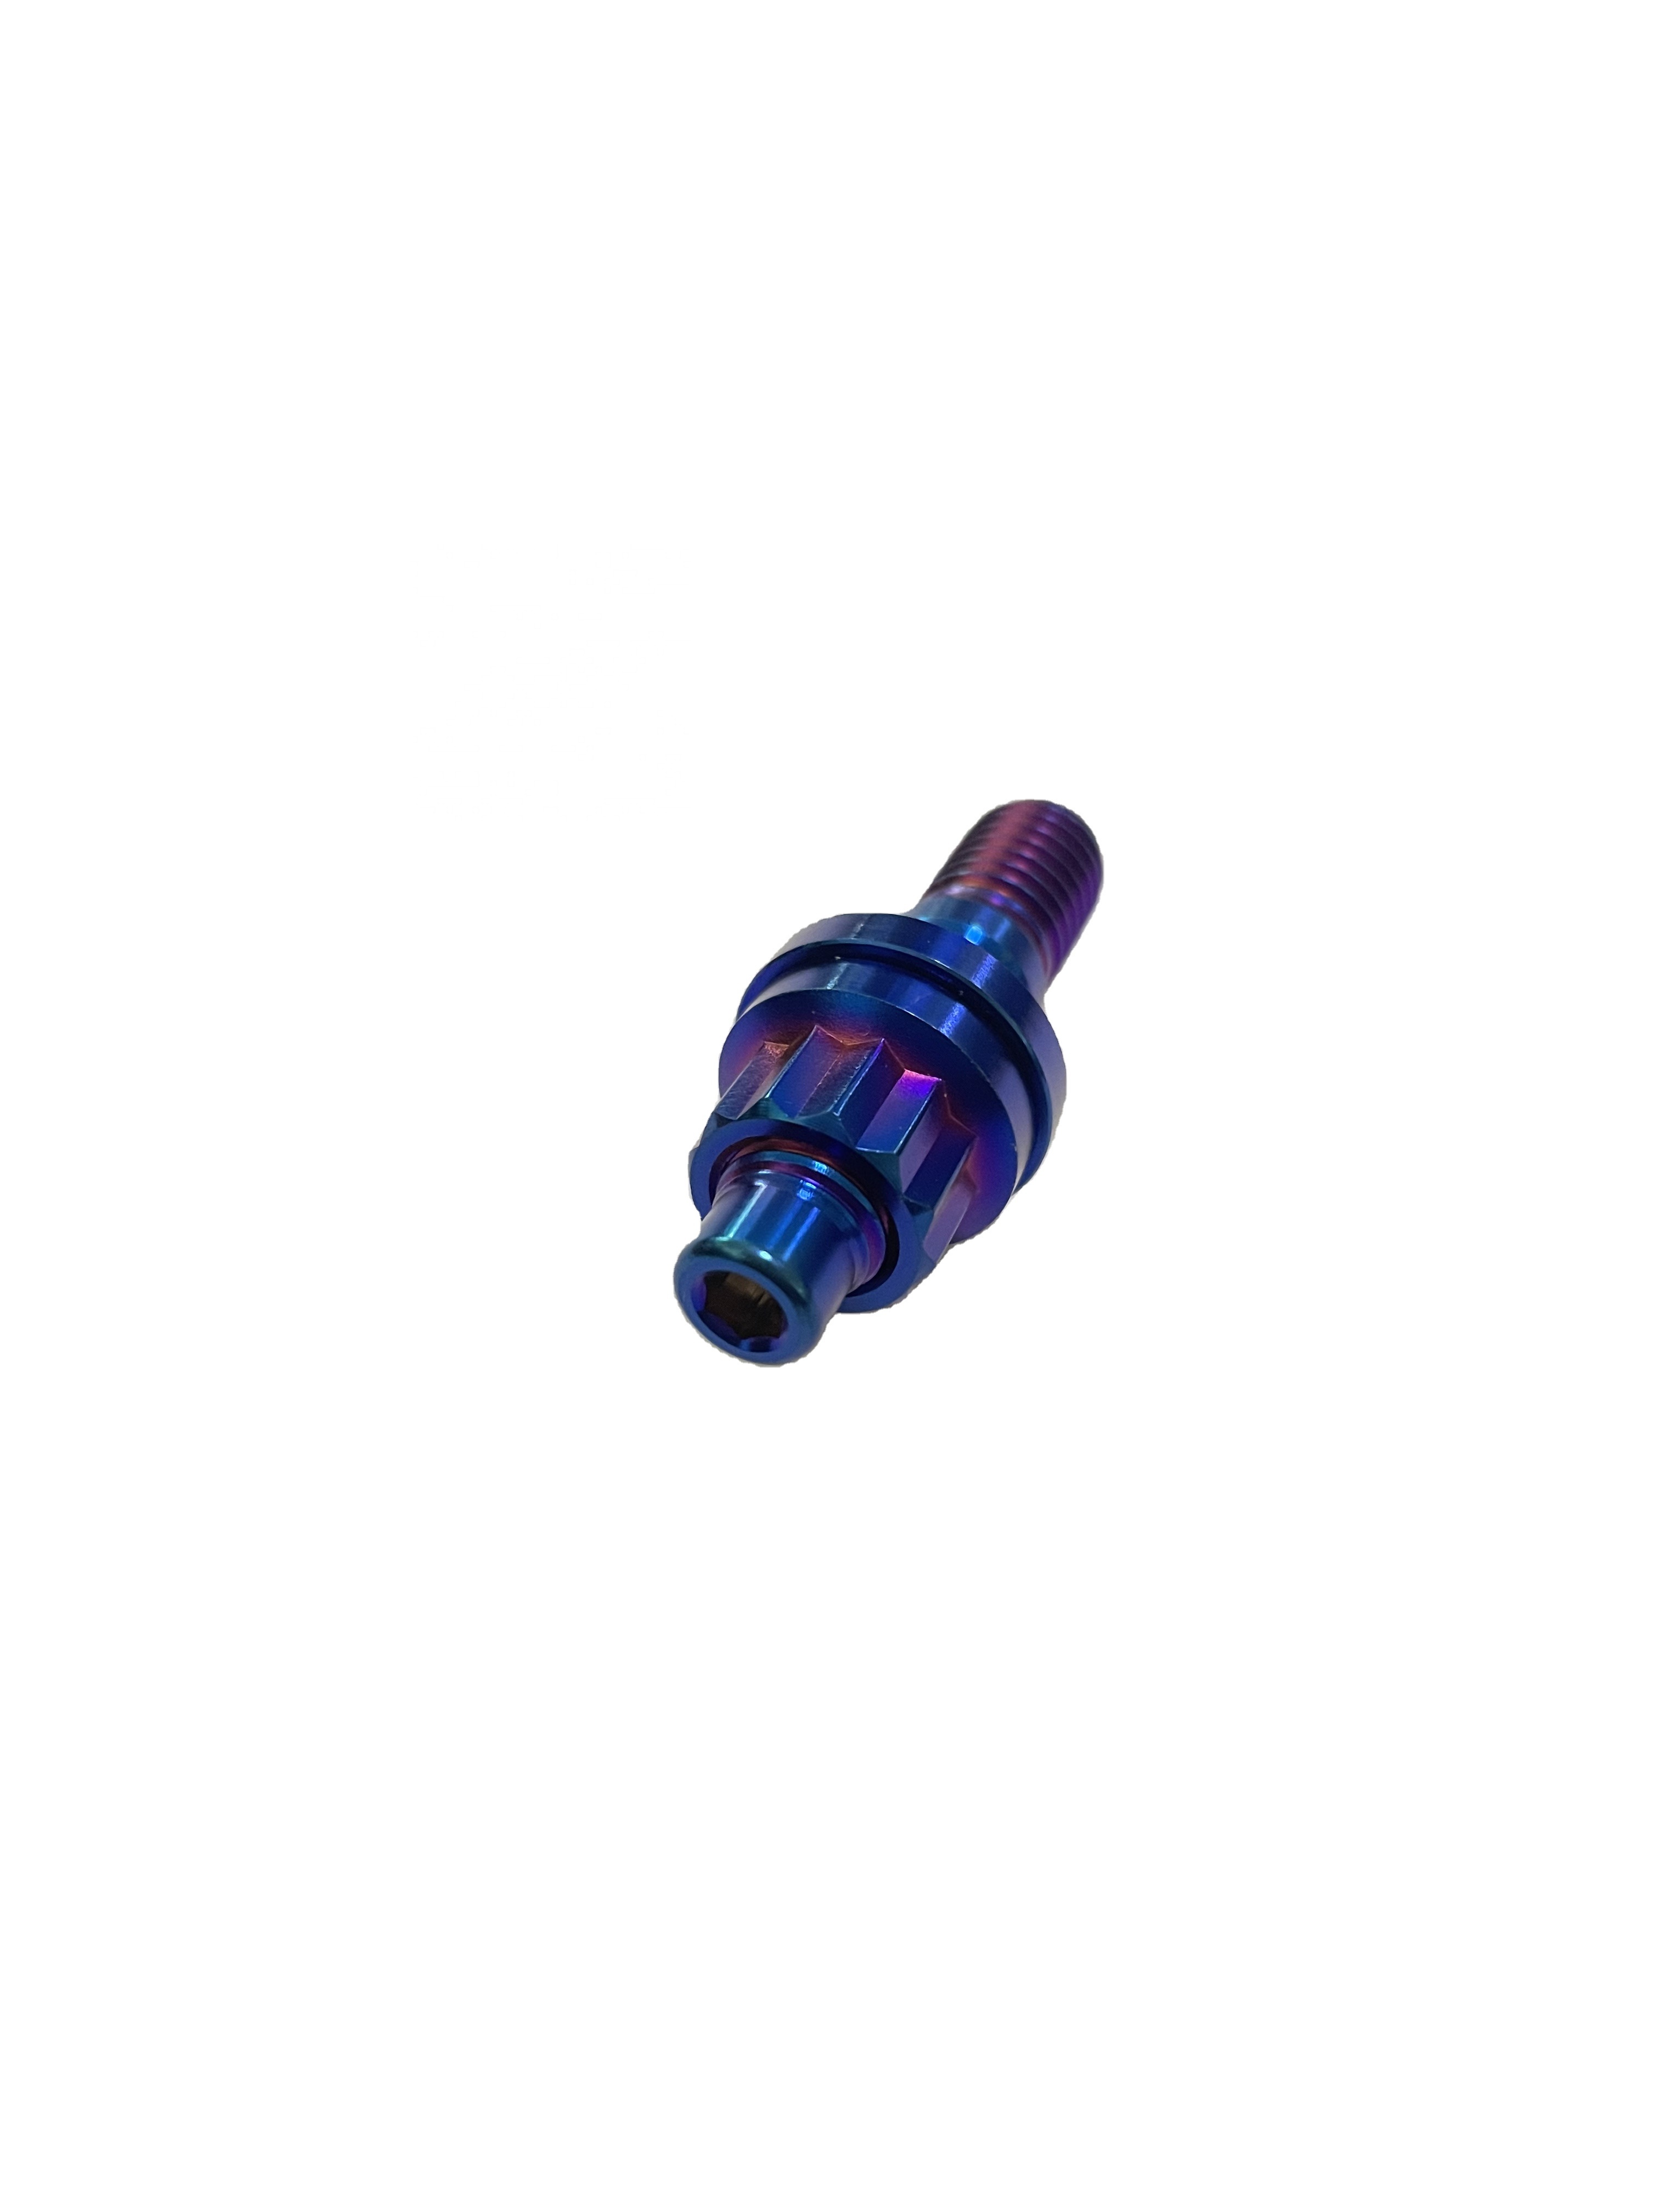
Featured Precision Titanium Fasteners & Components
Precision-engineered fasteners and lightweight performance hardware manufactured in China's Titanium Valley, conforming strictly to DIN, ISO, and GB global standards.
Technical Whitepaper & Industry Intelligence
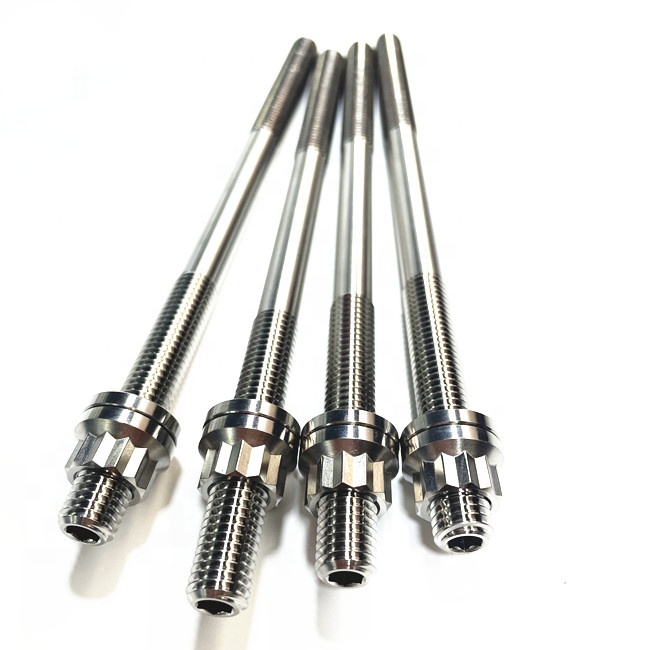
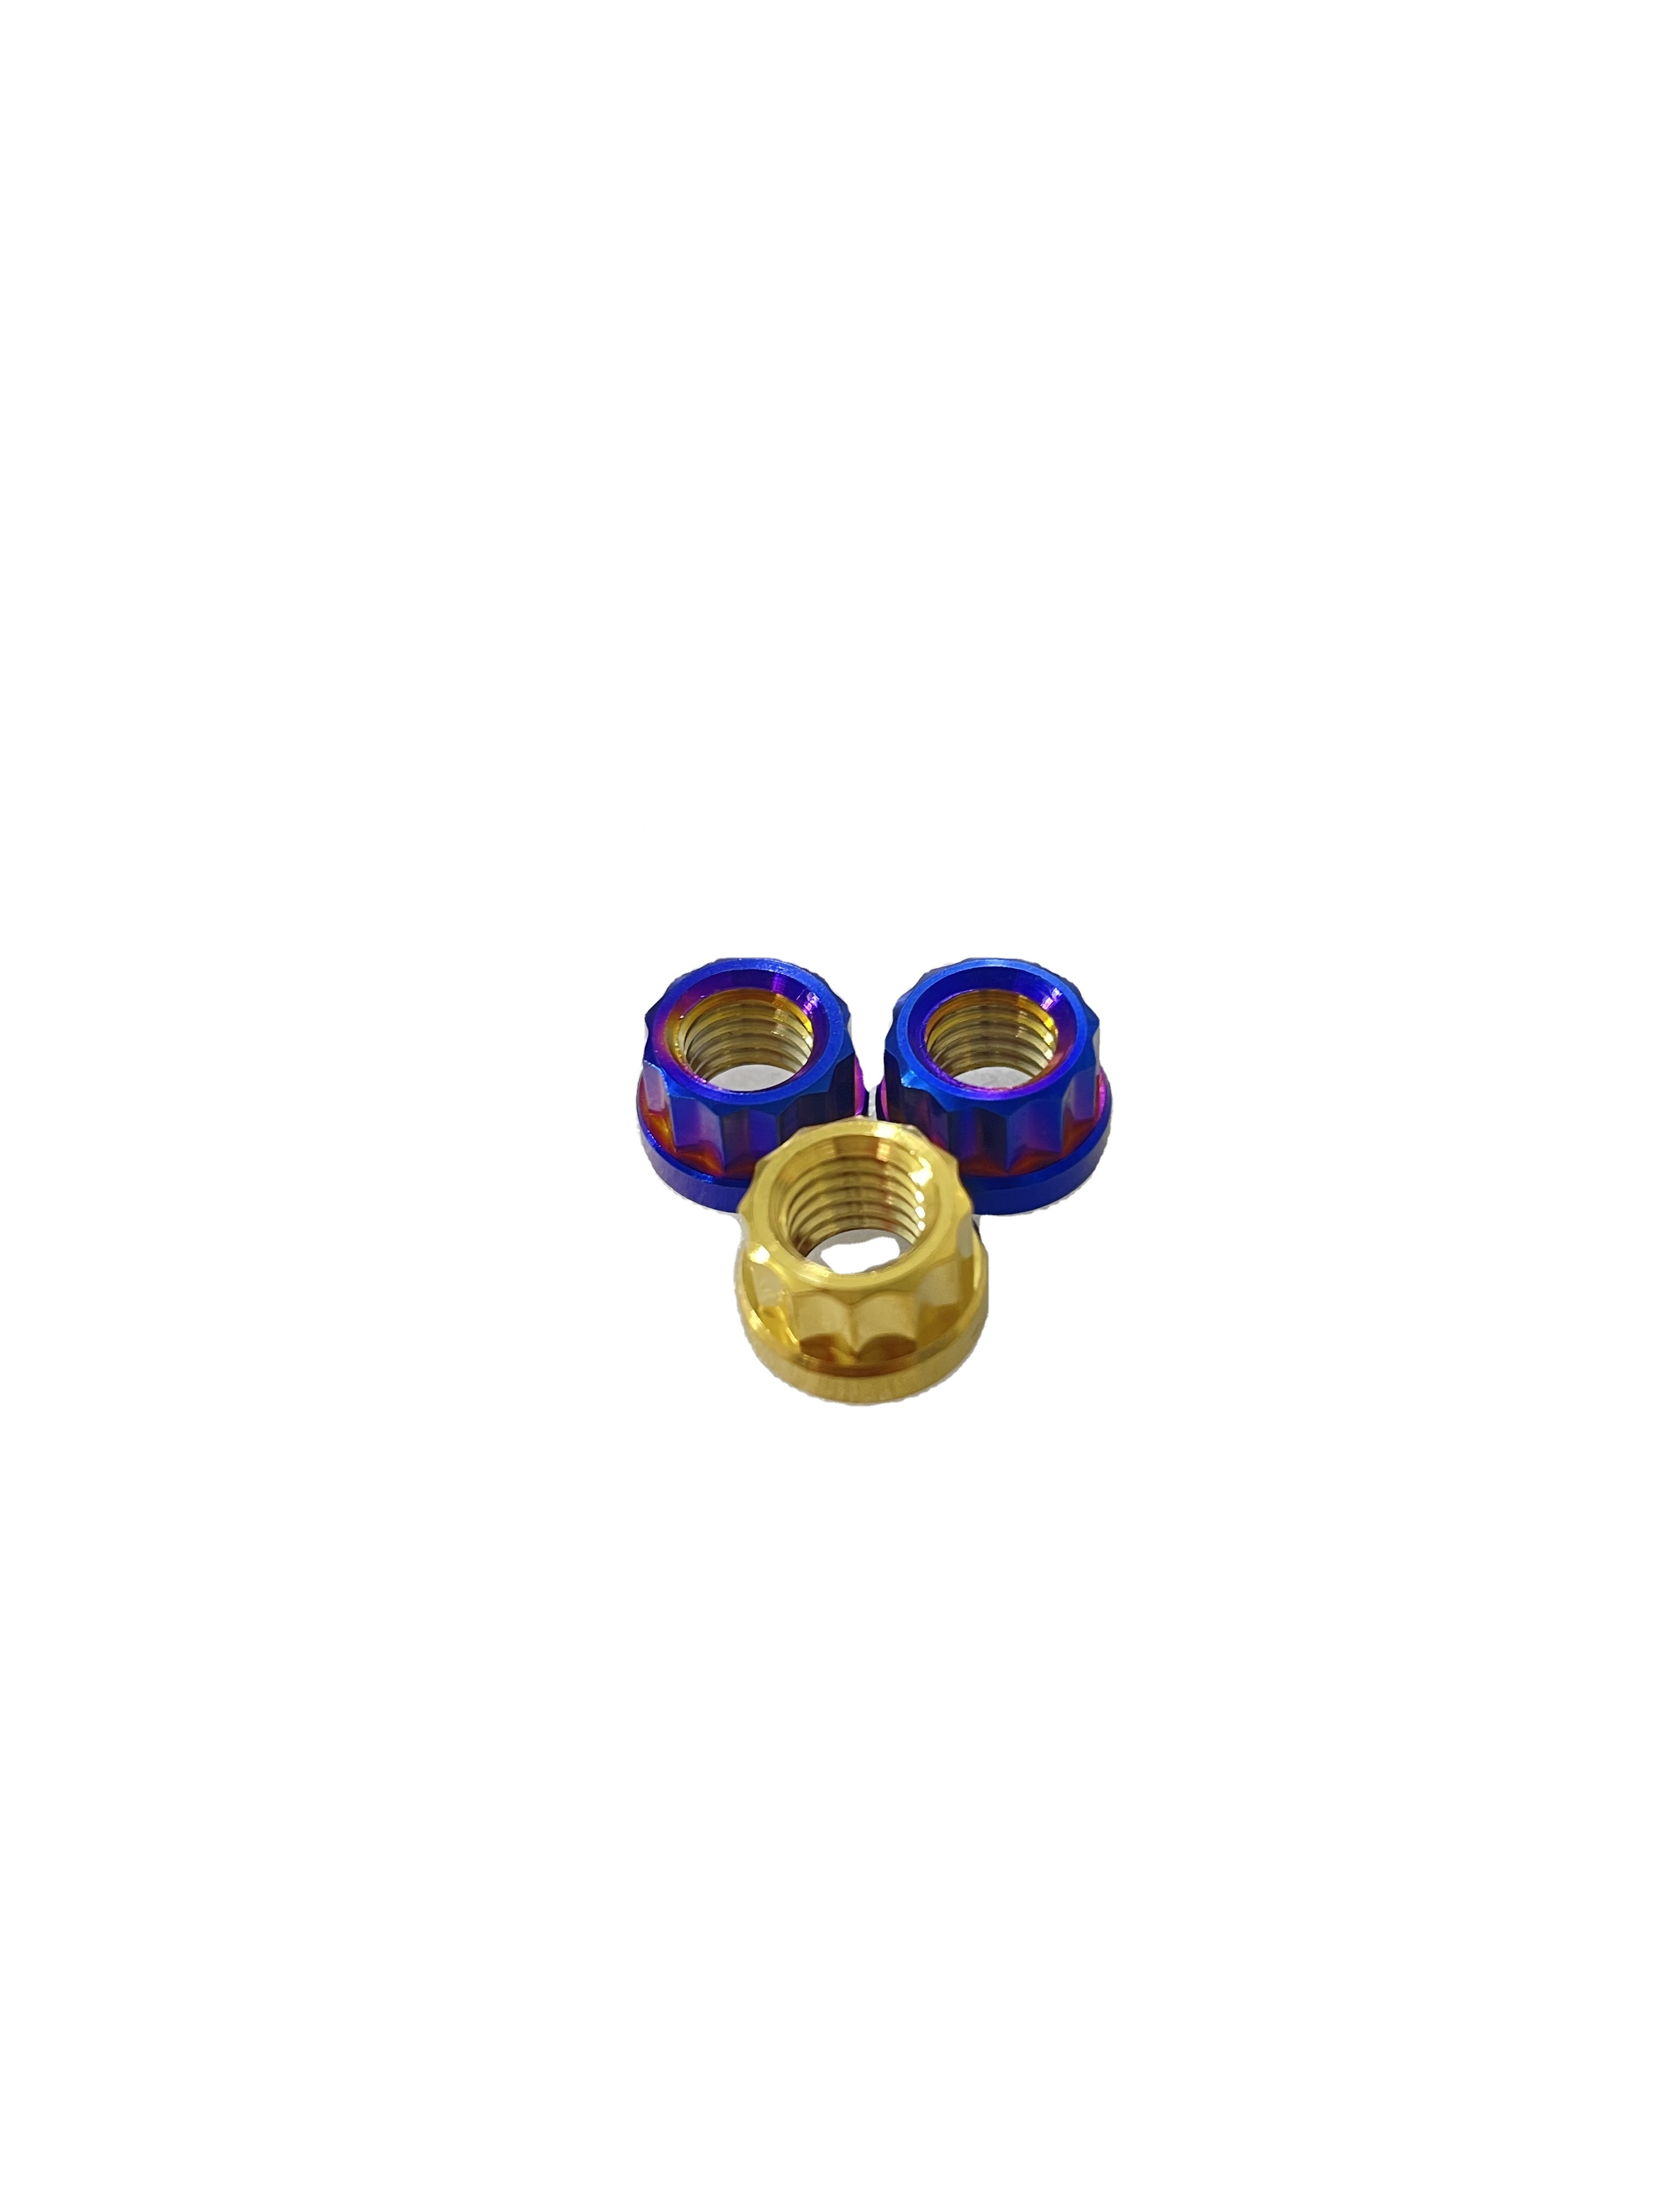
Precision Engineering of Fastener Titanium: Metallurgy, Mechanical Integrity & OEM Specs
A comprehensive analysis of metallurgical integrity, fatigue behavior, hot-forged heading, and high-tolerance CNC machining standards for global Tier-1 applications.
In critical aerospace structures, high-performance motorsport powertrains, marine engineering, and subsea oil recovery systems, the demand for fastening hardware is dictated by a zero-failure mandate. Fasteners produced from titanium alloys—predominantly Ti-6Al-4V (Grade 5, UNS R56400) and commercially pure grades—deliver an unassailable strength-to-weight ratio (density approx. 4.43 g/cm³, roughly 56% that of structural steel) combined with virtually total immunity to chloride stress corrosion cracking. As a leading manufacturer and exporter anchored in China's Titanium Valley (Baoji), Vunza Titanium maintains full-process control spanning sponge melting, precision bar drawing, multi-axis Swiss-lathe turning, hot heading, and thread rolling to preserve uninterrupted grain flow.
Information Gain Note for Procurement Engineers: Unlike standard austenitic stainless steels (such as 304 or 316) that present galling vulnerabilities and yield strengths capped below 500 MPa, vacuum-processed Grade 5 titanium bolts deliver tensile strengths exceeding 895 to 1050 MPa. When paired with cold-work grain refinement or rolled-thread profiling, our fasteners achieve superior endurance limits under extreme thermal and mechanical harmonic vibration.
±0.005mm
CNC Machining Tolerance
34 Sets
3/4/5-Axis Machining Centers
15+ Yrs
Engineering Manufacturing History
100%
Ultrasonic & Optical Inspection
Metallurgical Comparison: Fastener Alloys Under High-Duty Stress
| Material Specification | Yield Strength (MPa) | Tensile Strength (MPa) | Density (g/cm³) | Preload Fatigue Threshold | Typical Industrial Target |
|---|---|---|---|---|---|
| Titanium Ti-6Al-4V (Grade 5) | ≥ 828 | ≥ 895 - 1050 | 4.43 | High (Cold-Rolled Roots) | Exhaust studs, cylinder head bolts, motorsport hubs |
| Ti-6Al-4V ELI (Grade 23) | ≥ 795 | ≥ 860 | 4.43 | Exceptional (Low Inters.) | Surgical orthopedic anchors, cryogenic valves |
| CP Grade 2 Pure Titanium | ≥ 275 | ≥ 345 | 4.51 | Moderate | Chemical immersion racks, desulfurization scrubbers |
| Grade 8.8 Structural Steel | 640 | 800 | 7.85 | Standard | General automotive body assembly (Corrosion-prone) |
| 316 Marine Stainless Steel | 220 | 520 | 8.00 | Low-Medium | Architectural brackets, non-critical marine hardware |
Macro Analysis
Future Procurement Trends in the Titanium Fastener Landscape
Key supply-chain vectors, technical innovations, and structural shifts driving global procurement through 2026–2030.
1. Electric Vehicles & Unsprung Mass Optimization
OEM tier-1 mobility engineering teams are shifting away from heavy alloy steel wheel studs, rotor bolts, and suspension links. With EV battery packs adding between 300 to 700 kg of dead weight, reducing un-sprung rotational mass by 45-50% using titanium lug nuts and brake hardware directly increases range metrics and suspension damping responsiveness.
2. Thread Rolling vs. Thread Cutting Mandates
Procurement technical datasheets are universally mandating thread rolling over single-point CNC cutting. Rolled threads deform the alpha-beta grain crystalline flow along the contour of the crest and root, reducing root notch sensitivity and yielding up to 300% longer fatigue life under repetitive dynamic tensile cycling in performance manifold and head stud setups.
3. Surface Engineering & Anti-Galling PVD Coatings
To overcome titanium’s inherent coefficient of friction and propensity to gall against aluminum or steel interfaces, high-tech coatings such as Physical Vapor Deposition (PVD), Diamond-Like Carbon (DLC), micro-arc oxidation, and specialized fluoropolymer baking are becoming standard contract requirements for high-cycle industrial disassembly.
4. Multi-Axis Hybrid Additive-Subtractive CNC
Complex internal titanium race components and weight-relieved hollow-core bolts now leverage 5-axis simultaneous milling centers with live tooling. Combining near-net shape cold/hot heading with CNC finishing maintains low raw material buy-to-fly ratios while keeping finished surface roughness down to Ra 0.4 µm.
5. Complete "Sponge-to-Part" Auditability
Global quality standards like ISO 9001 and aerospace audits require rigorous trace certificates. The market is consolidating around vertically integrated Chinese suppliers based in Baoji that ensure direct custody tracing from vacuum arc remelted (VAR) titanium sponge to final optical sorting records.
6. Custom Geometries & Non-Standard Drive Formats
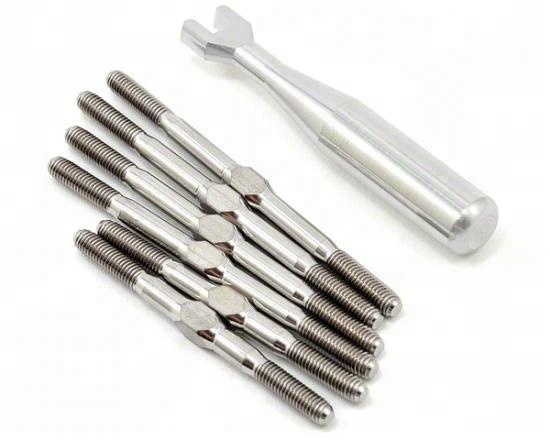
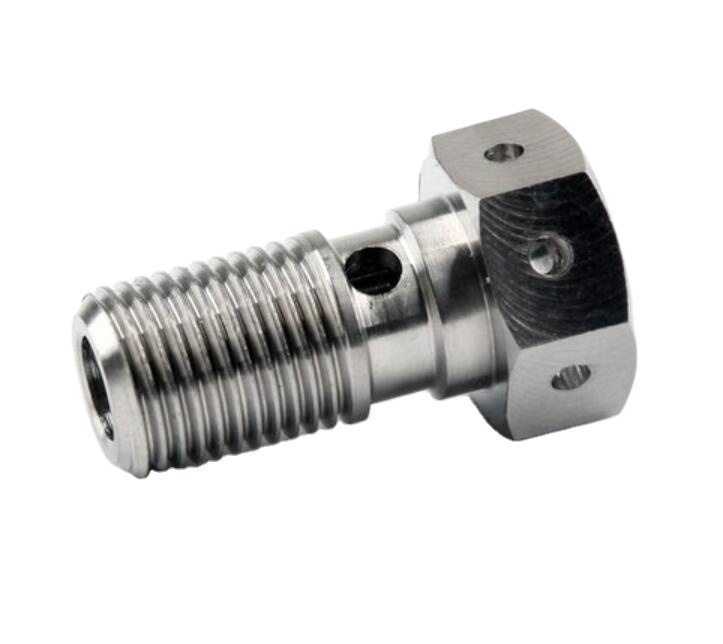
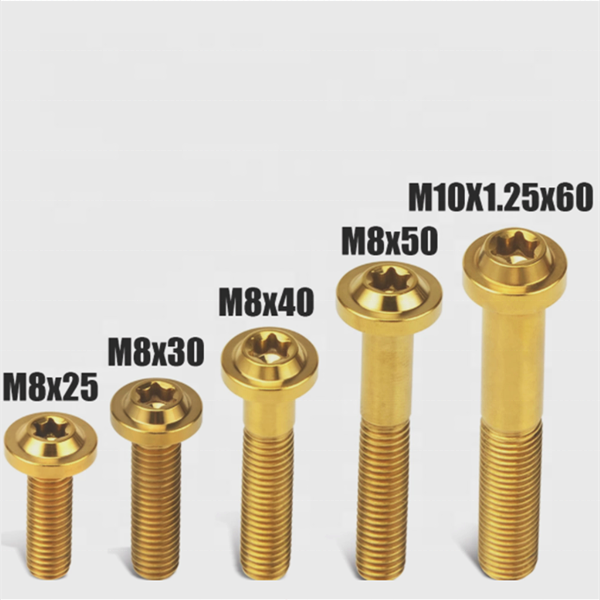
From low-profile Torx T40 and 12-point bi-hex head flange designs to captive multi-piece washers and reverse-threaded RC turnbuckles, industrial buyers increasingly specify bespoke blueprint engineering over catalog inventory to minimize packaging space and prevent stripped heads.
Proven Manufacturing Pedigree
Why Global B2B Buyers Partner with Vunza Titanium Industry
Direct from China's Titanium Valley—delivering certified metallurgical excellence, rapid prototyping, and verified delivery capabilities since 2008.
Geographic Supply Chain Integration
Located in the Gaoya Village Industrial Zone, Baoji, Shaanxi, our factory sits adjacent to the Baoti Group Industrial Park. This location grants us immediate, priority access to high-grade titanium sponge, precision drawn wire, and world-class raw bar stocks, substantially reducing supply lead times and raw material freight overhead.
High-Precision Machining Fleet
Equipped with 34 multi-axis (3-axis, 4-axis, and 5-axis) CNC machining centers, automated CNC turning centers, and high-speed multi-station heading machines, we hold ultra-tight geometric tolerances down to 0.005 mm on mission-critical threads, valve retainers, and turned shafts.
Mastery of Specialized Exotic Alloys
Beyond Gr1, Gr2, Gr5 (TC4), and Gr9 titanium, our metallurgy and production teams process specialized high-performance materials, including Ti-6Al-4V ELI (Grade 23), non-ferrous medical titanium, and specialized CoCrMo (Cobalt-Chromium-Molybdenum) dental and surgical alloys.
Experienced Technical Workforce
Over 50% of our precision machining operators and technicians possess more than 13 years of specialized experience in cutting and forming refractory metals. This hands-on capability ensures clean chatter-free tool paths, superior thread surfaces, and minimal scrap rates on intricate custom jobs.
Comprehensive QC & Traceability
Every production lot is fully backed by certified Mill Test Certificates (EN 10204 3.1), mechanical tensile tests, chemical composition analyses, optical projector dimensional checks, and go/no-go pitch verification to eliminate incoming assembly errors at your plant.
Verified Global Trade Reliability
Holding a proven 15+ year manufacturing record with verified onsite auditing, an average buyer rating of 5.0/5 stars, and an average customer response turnaround time of under 9 hours, we serve demanding engineering clients throughout North America, Europe, Australia, and Asia.
Procurement Guidelines
Frequently Asked Questions: Titanium Fasteners Sourcing
Clear, definitive technical answers addressing metallurgical selection, assembly tolerances, MOQ policies, and drawing-to-part production cycles.
What makes Grade 5 (Ti-6Al-4V) superior to stainless steel for racing fasteners?
Ti-6Al-4V provides a tensile strength of ≥895 MPa, which easily matches or exceeds standard Grade 8.8 steel and outperforms austenitic stainless steels (304/316) by over 100%. Simultaneously, its low density (4.43 g/cm³) removes roughly 44-50% of the mass. Furthermore, its thermal expansion rate is significantly closer to aluminum engine blocks, drastically improving clamp load retention across rapid heat cycles.
How does Vunza prevent thread galling during high-torque installation?
Titanium forms an instant passive oxide layer that can generate adhesive micro-welding (galling) under high friction. We counteract this through precision fine-ground thread tooling, mirror root polishing, micro-arc surface oxidation, and advanced PVD or DLC low-friction coatings. In addition, we provide explicit torque-spec lubricity guidelines using molybdenum disulfide or anti-seize paste for all dry assembly setups.
What are your production tolerances on non-standard custom drawings?
With our 34 multi-axis 3/4/5-axis CNC machining centers and precision automatic screw equipment, we reliably maintain diametrical and linear tolerances down to ±0.005 mm (5 microns). Thread profiles are verified per 6g/6H metric or 2A/3A imperial pitch diameters using calibrated Go/No-Go plug and ring gauges under temperature-controlled inspection conditions.
What is the typical Minimum Order Quantity (MOQ) and sample lead time?
For bespoke CNC machined titanium parts or specialized non-standard bolts, prototyping batch MOQs start at 50 to 100 pieces, while standard stock racing fasteners and studs can be ordered in quantities as low as 10 to 50 units. Prototyping and DFM feedback typically take 3 to 7 business days, with full production runs dispatched in 15 to 25 days depending on plating and finishing requirements.
Are thread profiles produced via cut machining or cold thread rolling?
For all high-duty stress applications—such as our cylinder head studs, wheel lug bolts, and exhaust hardware—we utilize dedicated thread-rolling machines. Rolling work-hardens the material inside the thread roots and creates continuous metal grain flow, boosting fastener fatigue endurance significantly compared to conventional single-point cutting.
What quality documentation is provided with international shipments?
Each production lot can be accompanied by an EN 10204 3.1 Mill Test Certificate verify chemical composition (spectrometric analysis for C, Fe, N, H, O, Al, V) and mechanical metrics (tensile, yield, elongation). We also deliver full dimensional CMM inspection reports, plating thickness certifications, and raw batch traceability records upon request.
Ready to Engineer Your High-Performance Titanium Assembly?
Send us your 2D/3D technical drawings (STEP, CAD, PDF), target material specifications, and batch volumes. Our engineering and metallurgical team will deliver comprehensive Design for Manufacturability (DFM) feedback and factory-direct pricing within 9 hours.
Send an Inquiry