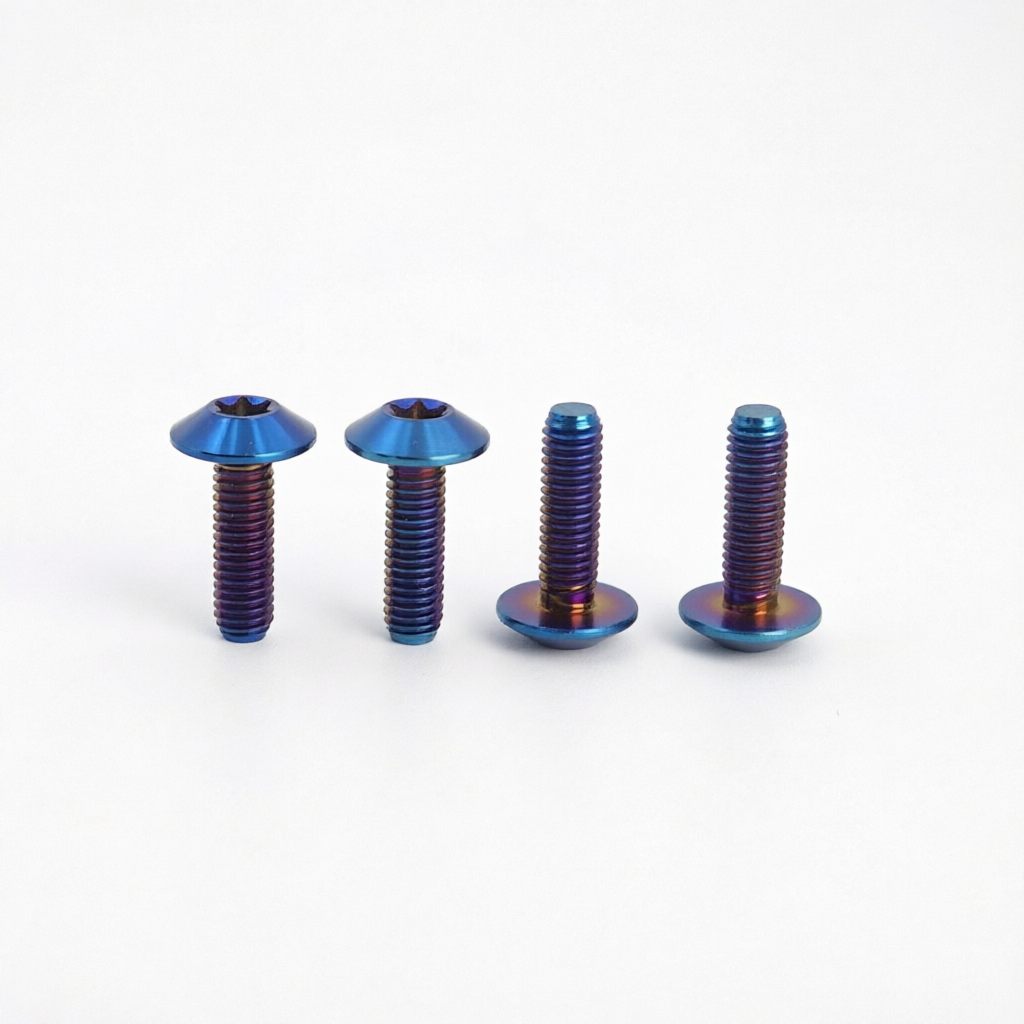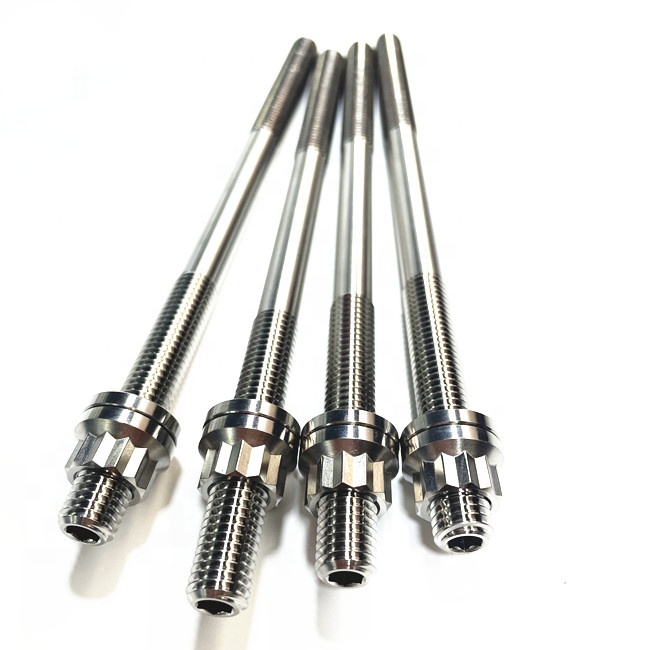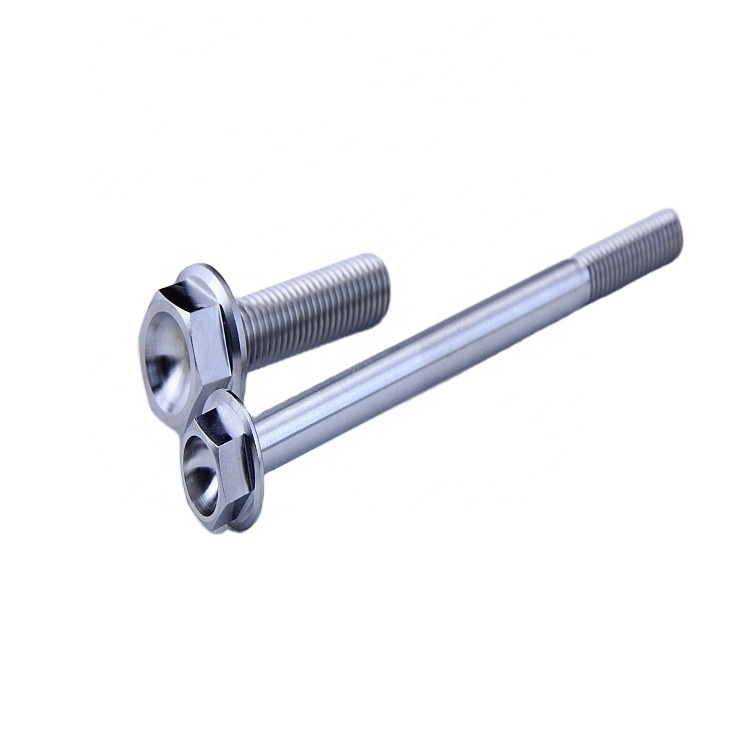
Cold-headed and multi-axis CNC milled titanium Grade 5 hardware certified for high-shear, zero-corrosion performance.
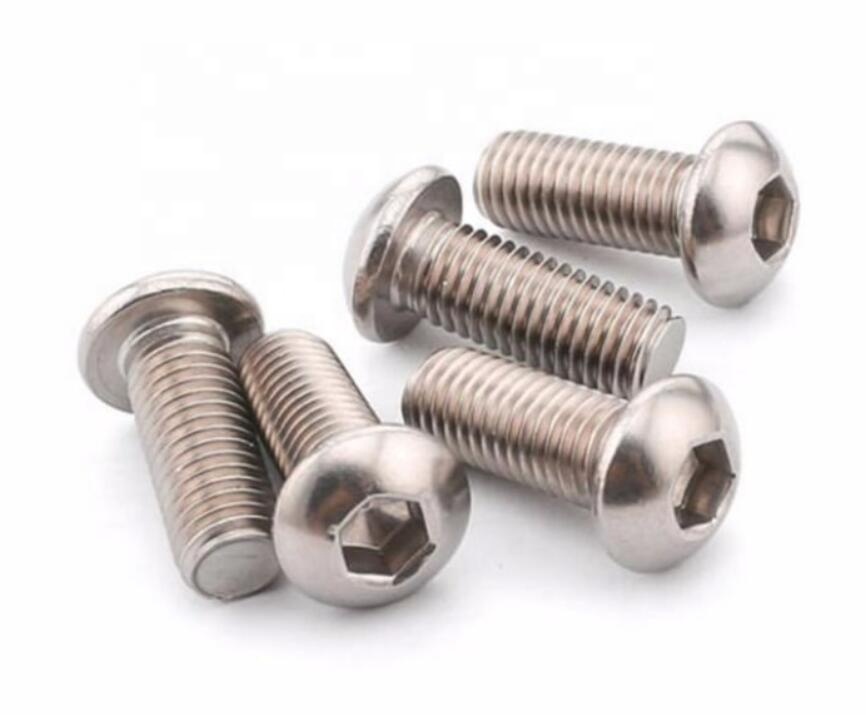
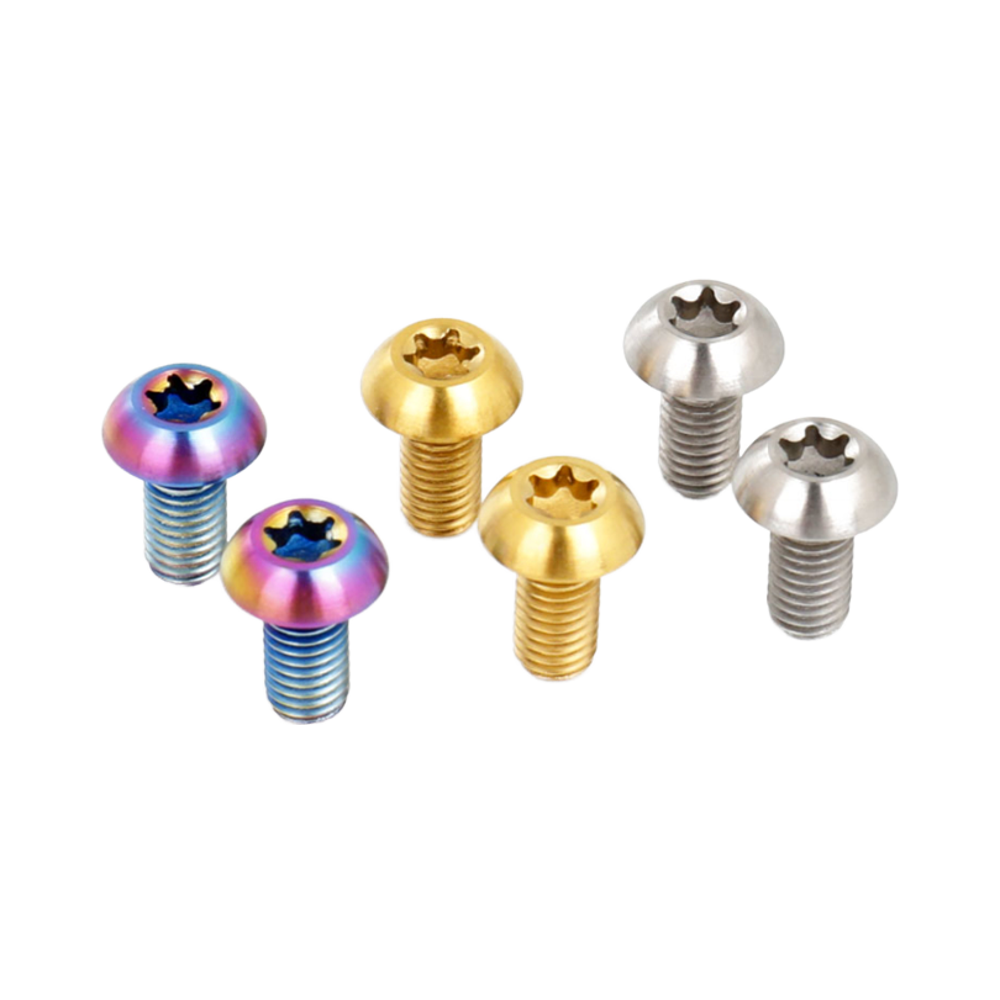
Button head bolts (ISO 7380 / ASME B18.3) provide a wide bearing area with a shallow hemispherical profile, preventing snagging in aerodynamics and tight spaces.
Fabricated from cold-worked Ti-6Al-4V Grade 5, these fasteners achieve tensile ratings exceeding 930–1000 MPa while weighing only 4.43 g/cm³, cutting rotating inertia and chassis load.
Unlike budget fasteners made purely by turning, our threads are cold-rolled after heat treatment, inducing continuous grain flow and compressive residual stress to mitigate shear fatigue.
Titanium instantly creates a self-healing TiO₂ passive oxide film, ensuring immunity to salt fog, wet chlorides, and galvanic pitting when paired with carbon fiber reinforced composites.
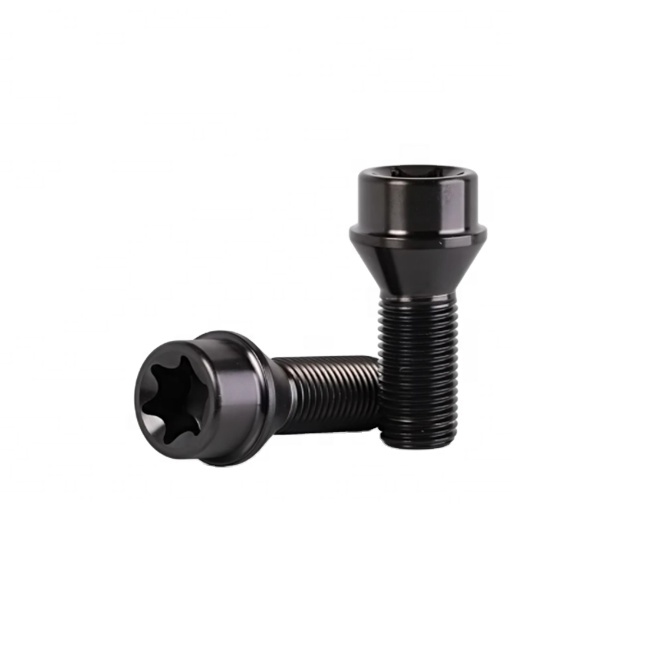
Standard hex sockets often round out when torqued in shallow button profiles. Our CNC machined Torx (T20, T25, T30) geometries distribute torque evenly to protect drives.
| Material Specification | Yield Strength (MPa) | Tensile Strength (MPa) | Density (g/cm³) | Corrosion Resistance | Common Factory Application |
|---|---|---|---|---|---|
| Titanium Grade 5 (Ti-6Al-4V) | ≥ 828 | ≥ 895 - 1050 | 4.43 | Exceptional (Immune to Saltwater) | Button head brake, chassis, aerospace, motorsport |
| Titanium Grade 2 (CP-Ti) | ≥ 275 | ≥ 345 | 4.51 | Maximum Chemical Resistance | Exhaust shrouds, chemical vats, marine housings |
| Stainless Steel 316 / A4-80 | ≥ 600 | ≥ 800 | 8.00 | High (Susceptible to crevice corrosion) | General marine fittings, architectural anchors |
| Alloy Steel Grade 10.9 (Zinc Plated) | ≥ 940 | ≥ 1040 | 7.85 | Low (Relies on plating; rusts over time) | Heavy industrial equipment, automotive engine blocks |
How Tier-1 automotive, aerospace, and medical buyers are adjusting procurement standards for custom titanium button head screws through 2026–2030.
Raw titanium naturally exhibits galling when driven into matching internal threads. Next-generation procurement heavily prefers Physical Vapor Deposition (PVD) Titanium Nitride (TiN), Black DLC (Diamond-Like Carbon), and specialized anti-friction micro-coatings that double cycle life while lowering thread friction coefficients without messy chemical lubricants.
Traditional production relied strictly on subtractive CNC bar turning, which discarded up to 68% of expensive titanium stock. Modern top-tier factories utilize high-tonnage warm/cold heading for the button dome, followed by robotic 5-axis CNC machining of internal drives and thread profiles, driving unit costs down by 25–35% on high-volume production orders.
Global regulatory bodies require verified origin documentation. Procuring directly from Baoji ("China's Titanium Valley") allows buyers to obtain dual-certified material certificates (MTRs) tracking from raw titanium sponge to melted vacuum arc remelted (VAR) ingots, eliminating non-conforming scrap in critical motorsport and medical assemblies.
Direct engineering answers regarding machining tolerances, thread galling mitigation, MOQ parameters, and testing protocols.
Titanium threads are prone to micro-friction cold welding. We mitigate this through cold-rolled burnished threads with Ra < 0.4 µm roughness, dry-film MoS₂ lubricants, proprietary micro-arc oxidation, or PVD hard coatings. We also provide engineering torque specifications that prevent over-stretching during installation.
Our fleet of 34 multi-axis (3/4/5-axis) CNC turning-milling centers readily holds concentricity and head profile dimensions within ±0.005 mm (0.0002 inches). Thread pitches conform precisely to 6g / 6H tolerances under ISO 965 or Class 2A/3A standards under ASME B1.1.
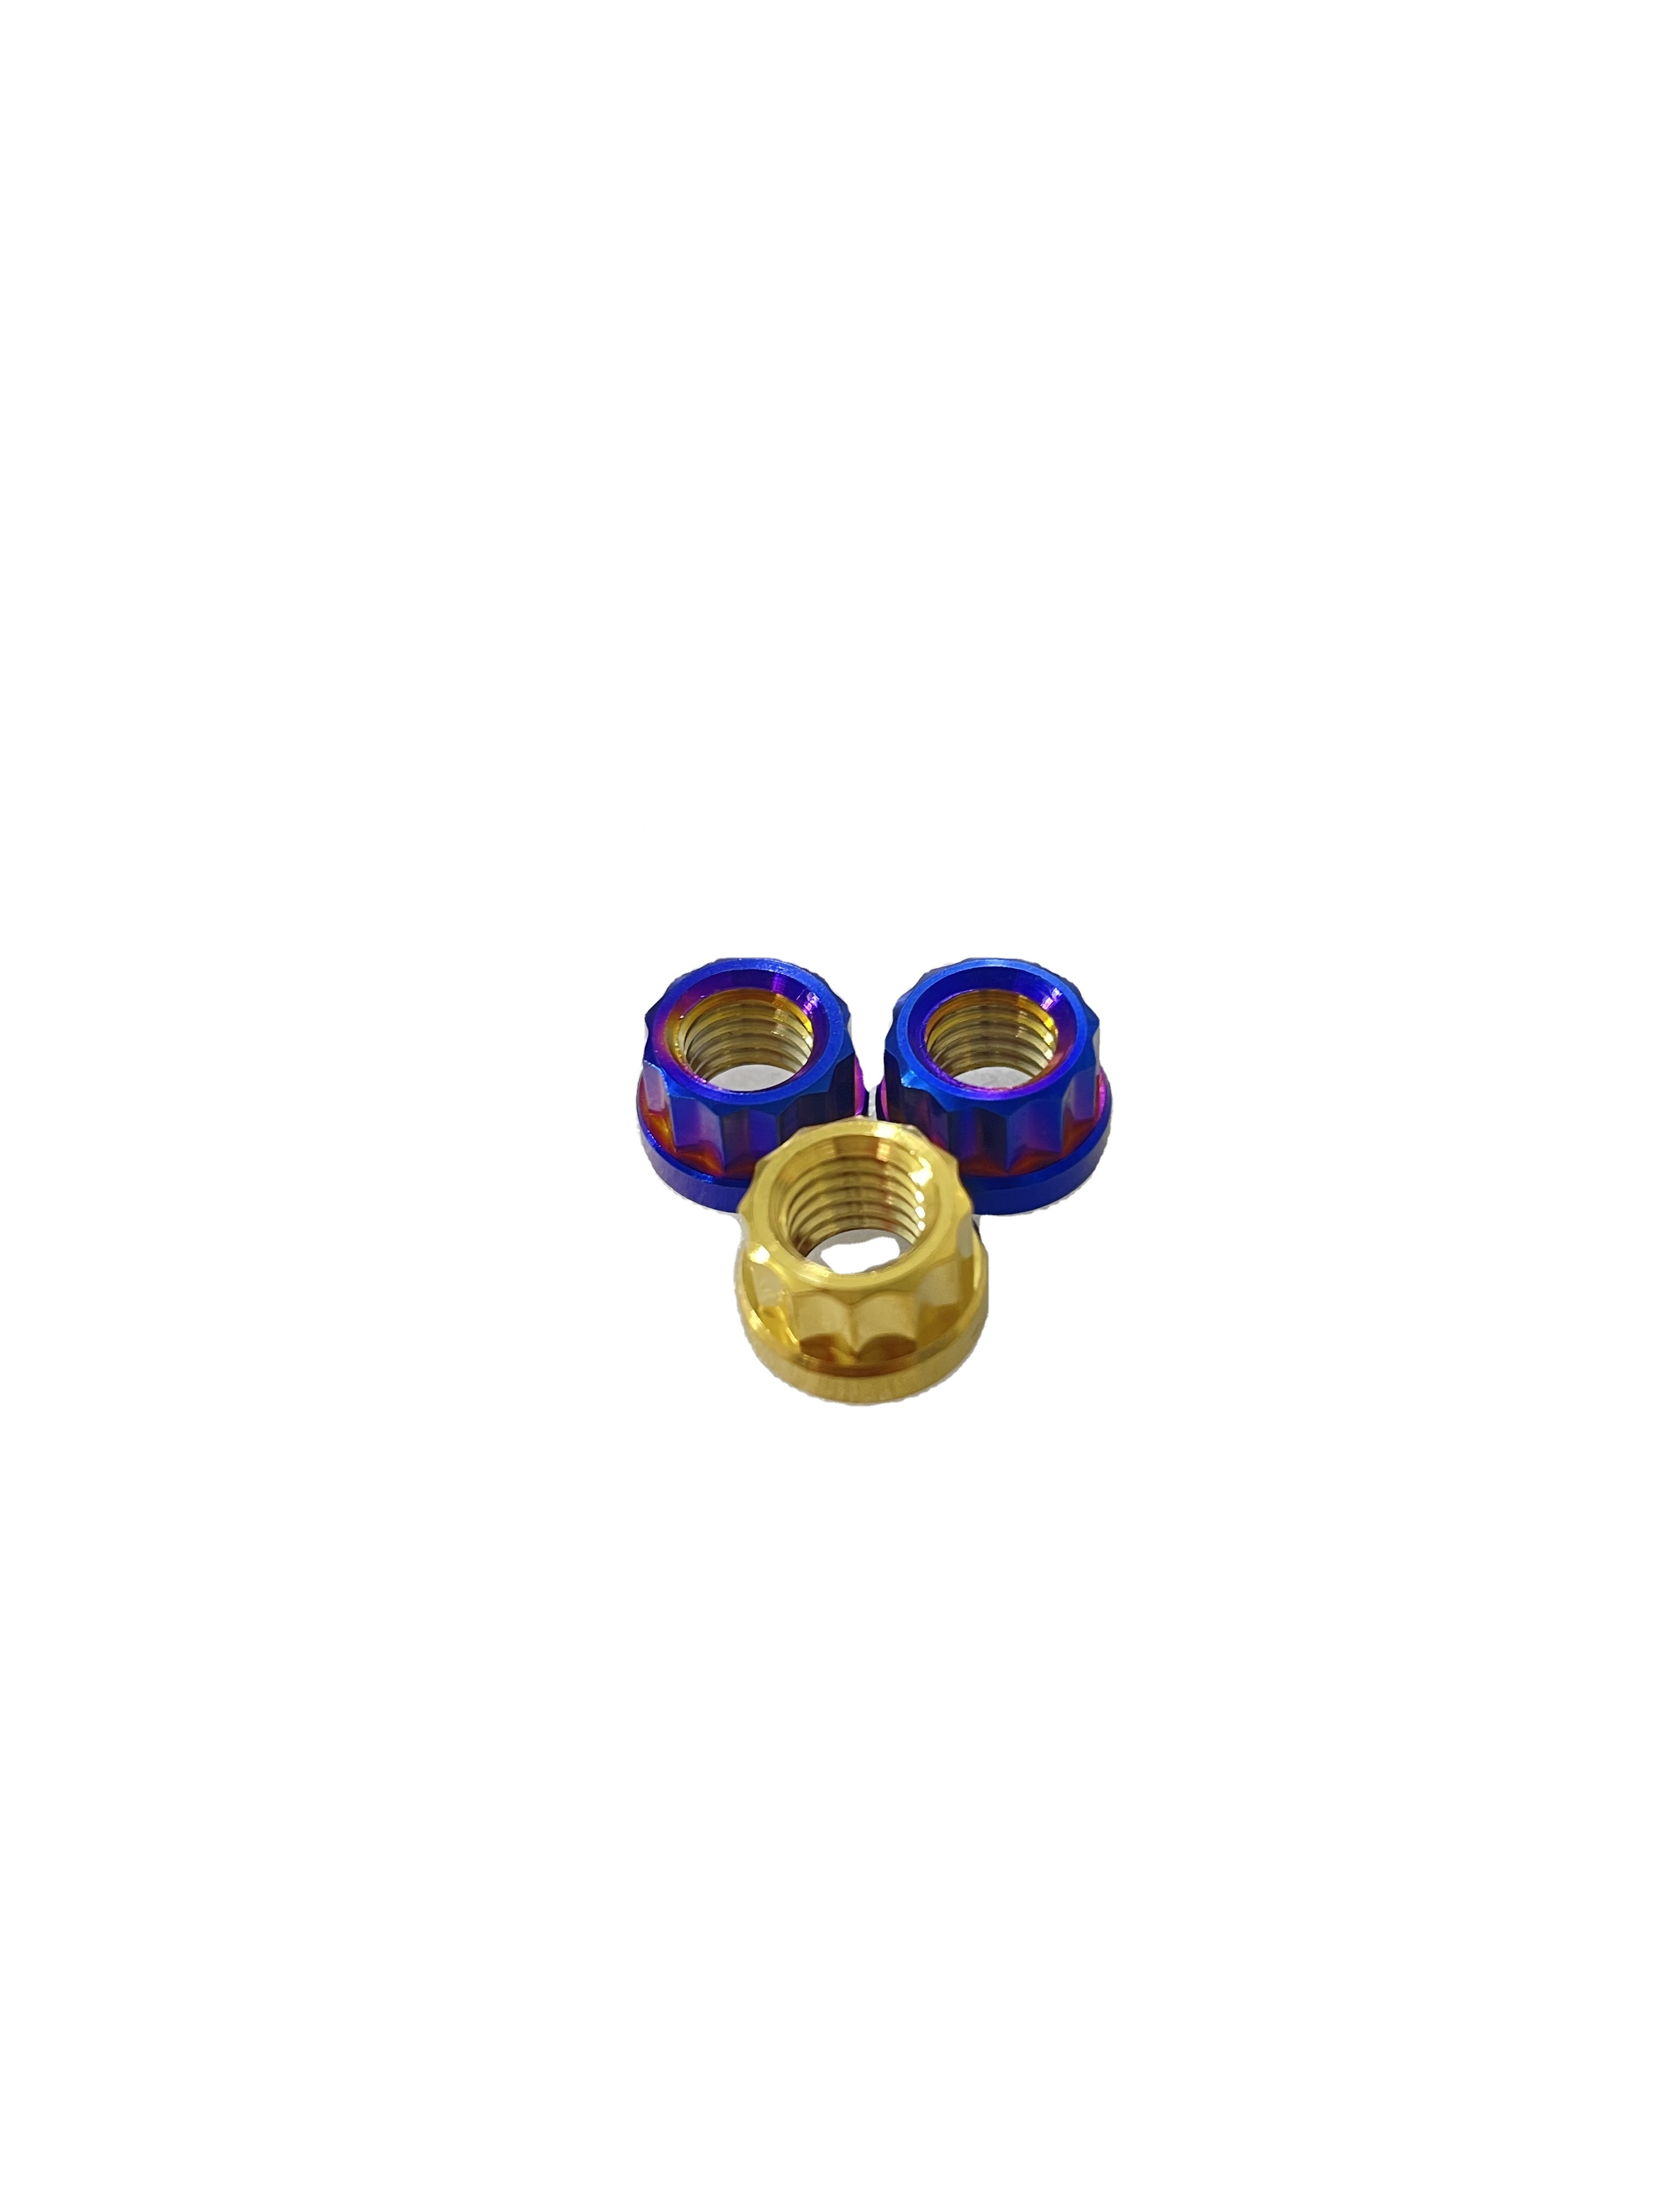
Yes. Our in-house R&D team engineers custom head diameters, integrated low-profile washers/flanges, safety wiring holes, and drive profiles (Torx, Torx Plus, Allen, 12-point) directly from your 2D engineering blueprints (PDF/DXF) or 3D STEP/IGES CAD files.
For standard catalog sizes, our MOQ starts at 100 to 500 units. For custom CNC titanium prototypes or modified button head fasteners, we provide rapid 5-day prototyping with initial verification batches as low as 10 to 50 pieces prior to full mass manufacturing.
Every shipment is backed by a full inspection portfolio, including EN 10204 3.1 Mill Test Certificates verifying raw titanium chemical composition and tensile properties, full First Article Inspection (FAI) dimensional reports, salt-spray test certifications, and complete batch heat lot numbers.
Gaoya Village Industrial Zone in Baoji is China's Titanium Valley, adjacent to Baoti Group. Sourcing direct eliminates multiple distributor markups, guarantees verified raw titanium sponge quality, reduces production lead-times, and gives you direct communication with machine shop engineers.
Founded in 2008 in the Gaoya Village Industrial Zone in Baoji, Shaanxi, Vunza Titanium Industry Co., Ltd. operates an integrated, high-capacity titanium fastener and precision CNC components manufacturing facility. Situated at the core of China's Titanium Valley, we control quality from sponge material to final packaged fasteners.
With an annual trade volume exceeding US$10M–$50M and over 15 years of focused titanium fabrication, over 50% of our production staff possess more than 13 years of titanium-specific turning and milling experience, guaranteeing parts that pass incoming inspection on your floor.
Submit your CAD files, thread pitches, quantities, and coating requirements. Our senior application engineers evaluate DFM feasibility and quote within 9 business hours.