Precision Titanium Nuts & Structural Racing Fasteners
Direct factory production from China's premier titanium manufacturing corridor. Each titanium nut is machined from certified vacuum-arc remelted Ti-6Al-4V bar stock with rolled metric and imperial threads.
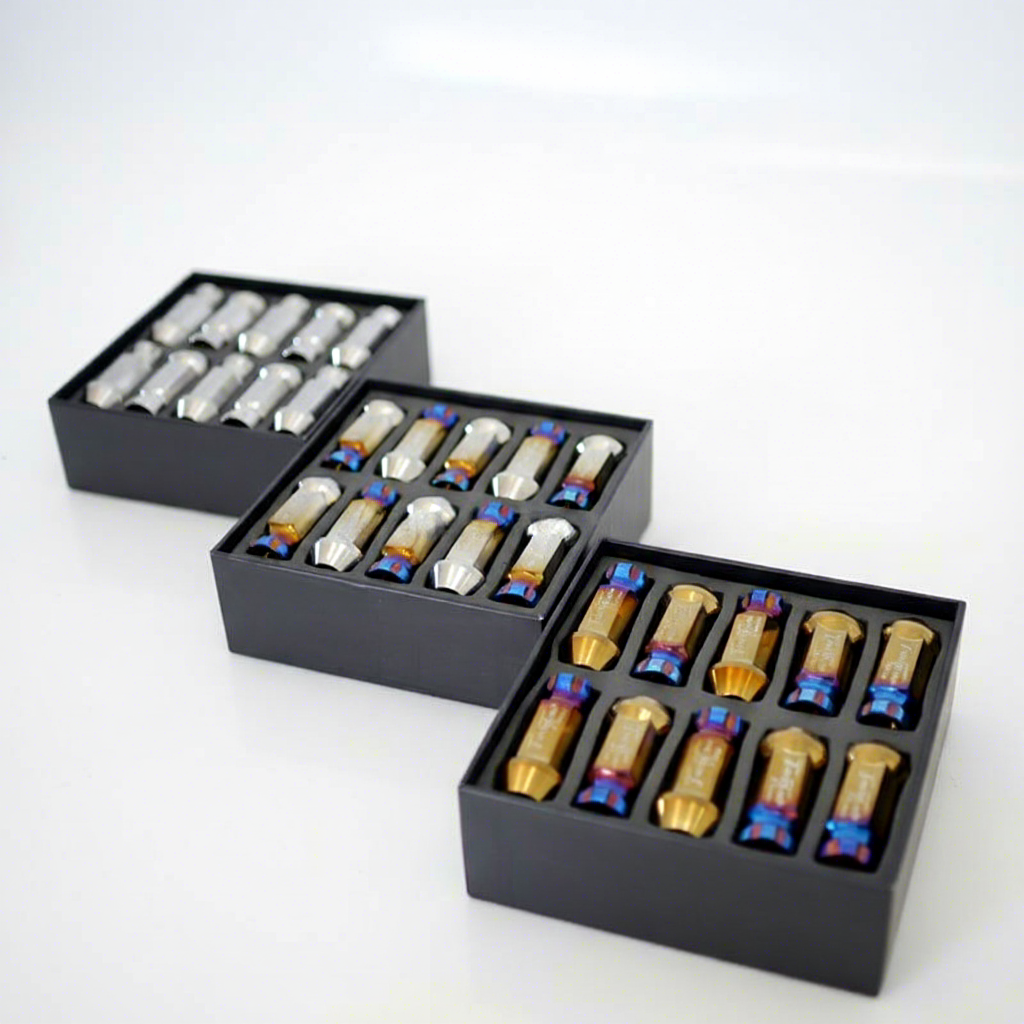
Factory Supply Gr5 Ti6AI4V M14 X 1.5 8mm Hole Right Hand Thread Titanium Hex Anodized Wheel Nuts
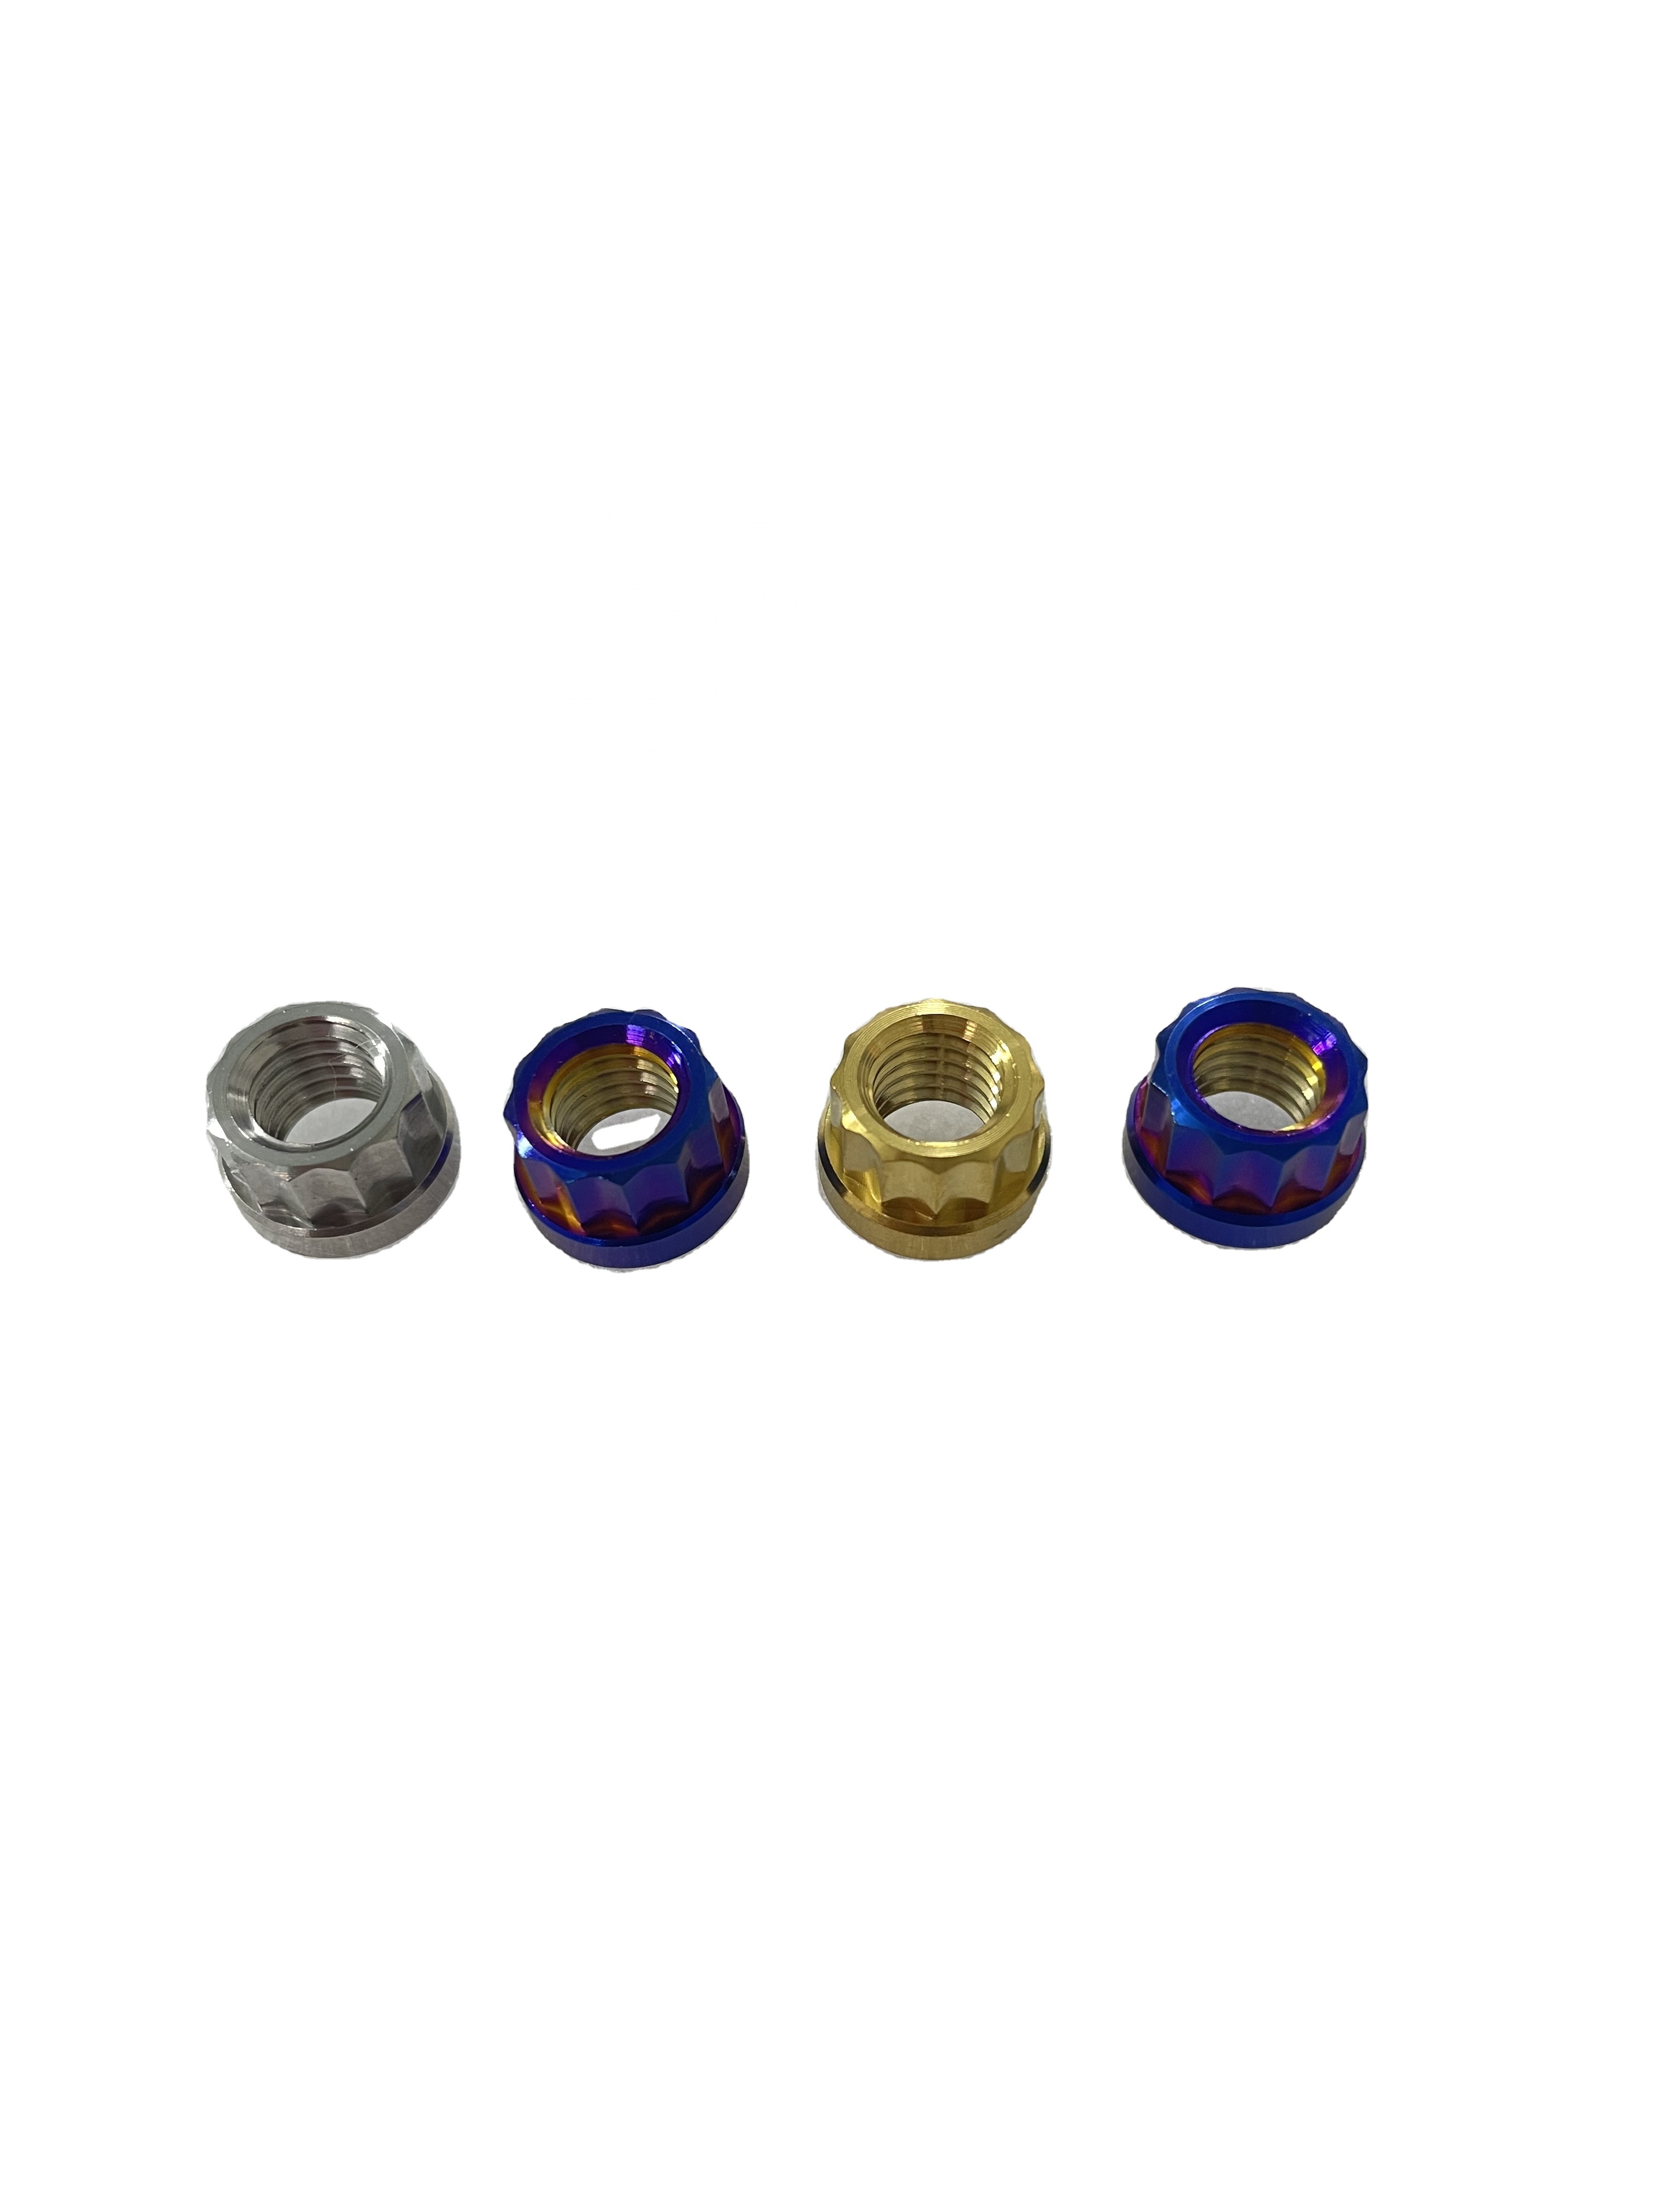
Polished Gr5 Titanium 12 Point Flange Nut M10X1.25 for Automotive Racing
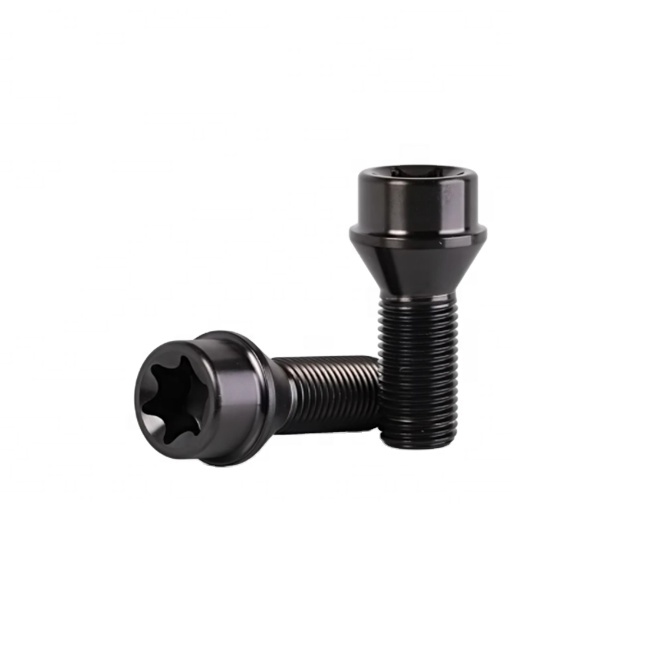
Titanium Wheel Bolts M14 DIN Standard Torx Shape CNC Machined Nitride Black Finish
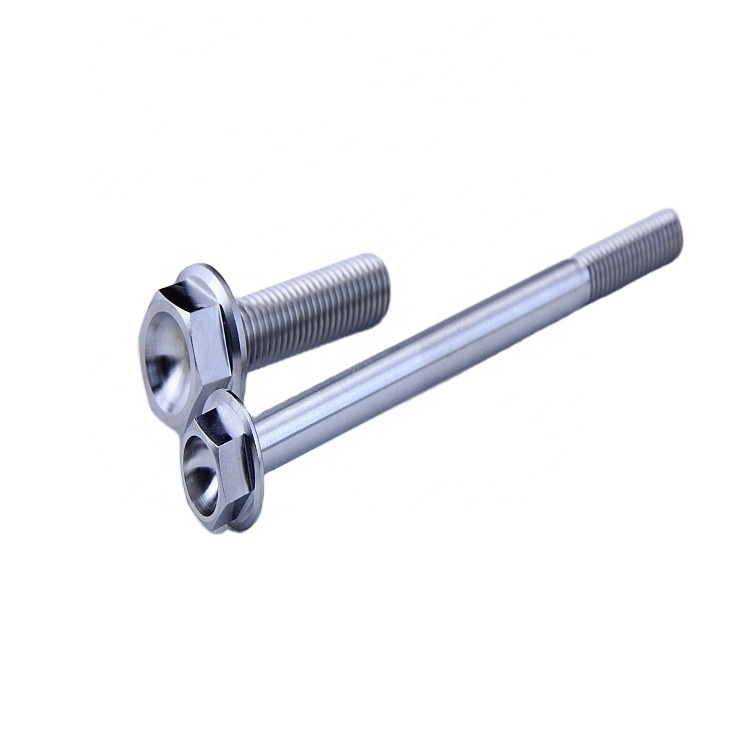
High Precision GR5 Titanium Alloy Racing Motorcycle Bolts PVD Finish TORX Head
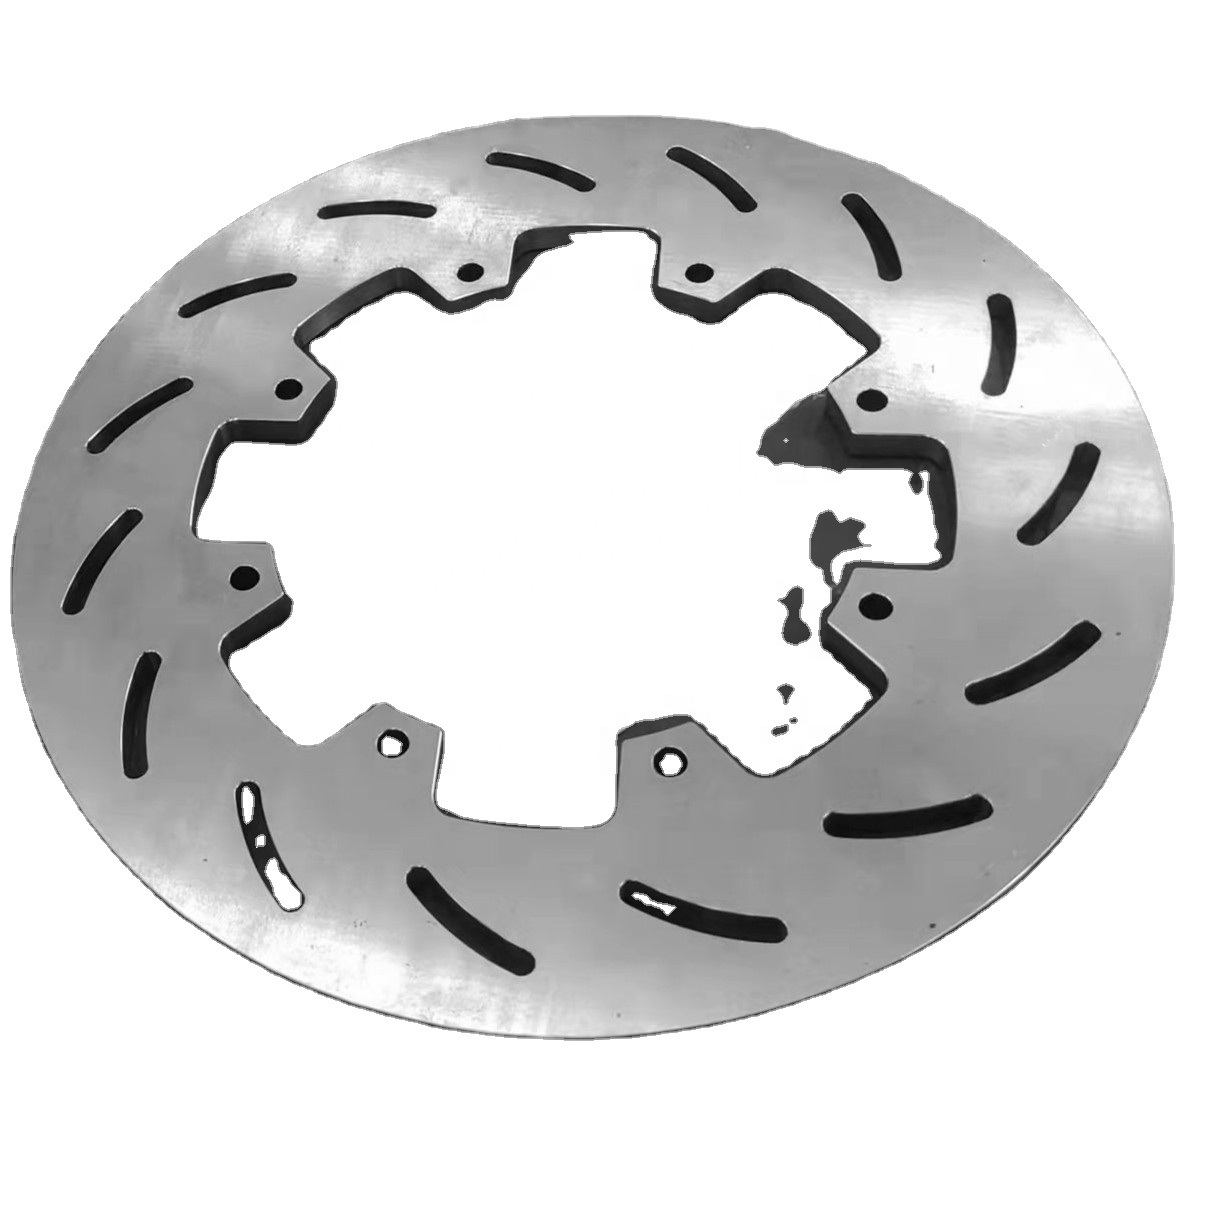
CNC Machined Milling Type Gr5 Titanium Alloy Inboard Brake Rotor Sprint Car Race
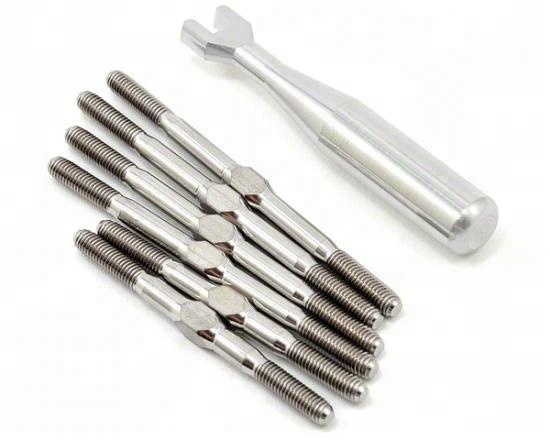
Titanium CNC Machined Hex Nut Turnbuckles Rc Parts Screws Silver Plated M14x1.5
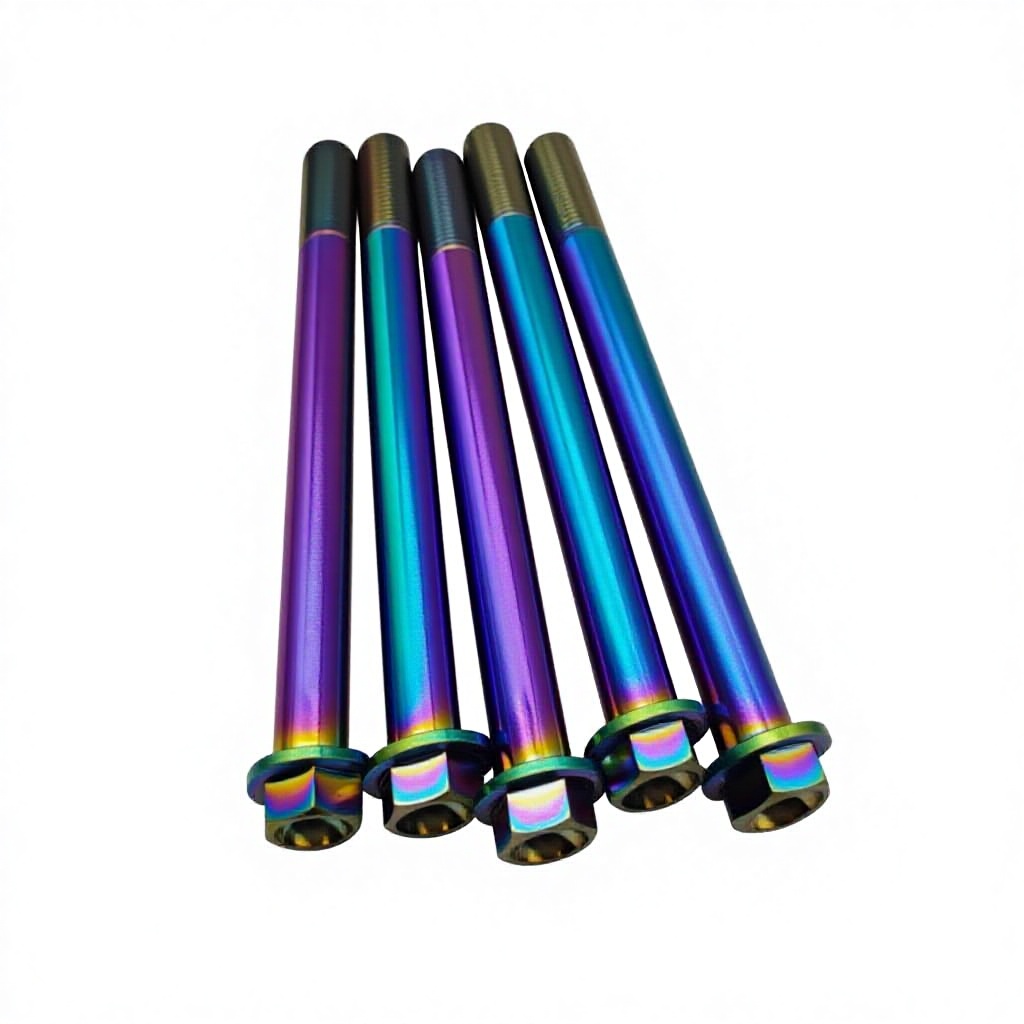
Gr5 Titanium Hexagon Head Flange Bolts M6 M8 M10 PVD Anodized Finish DIN GB Standard
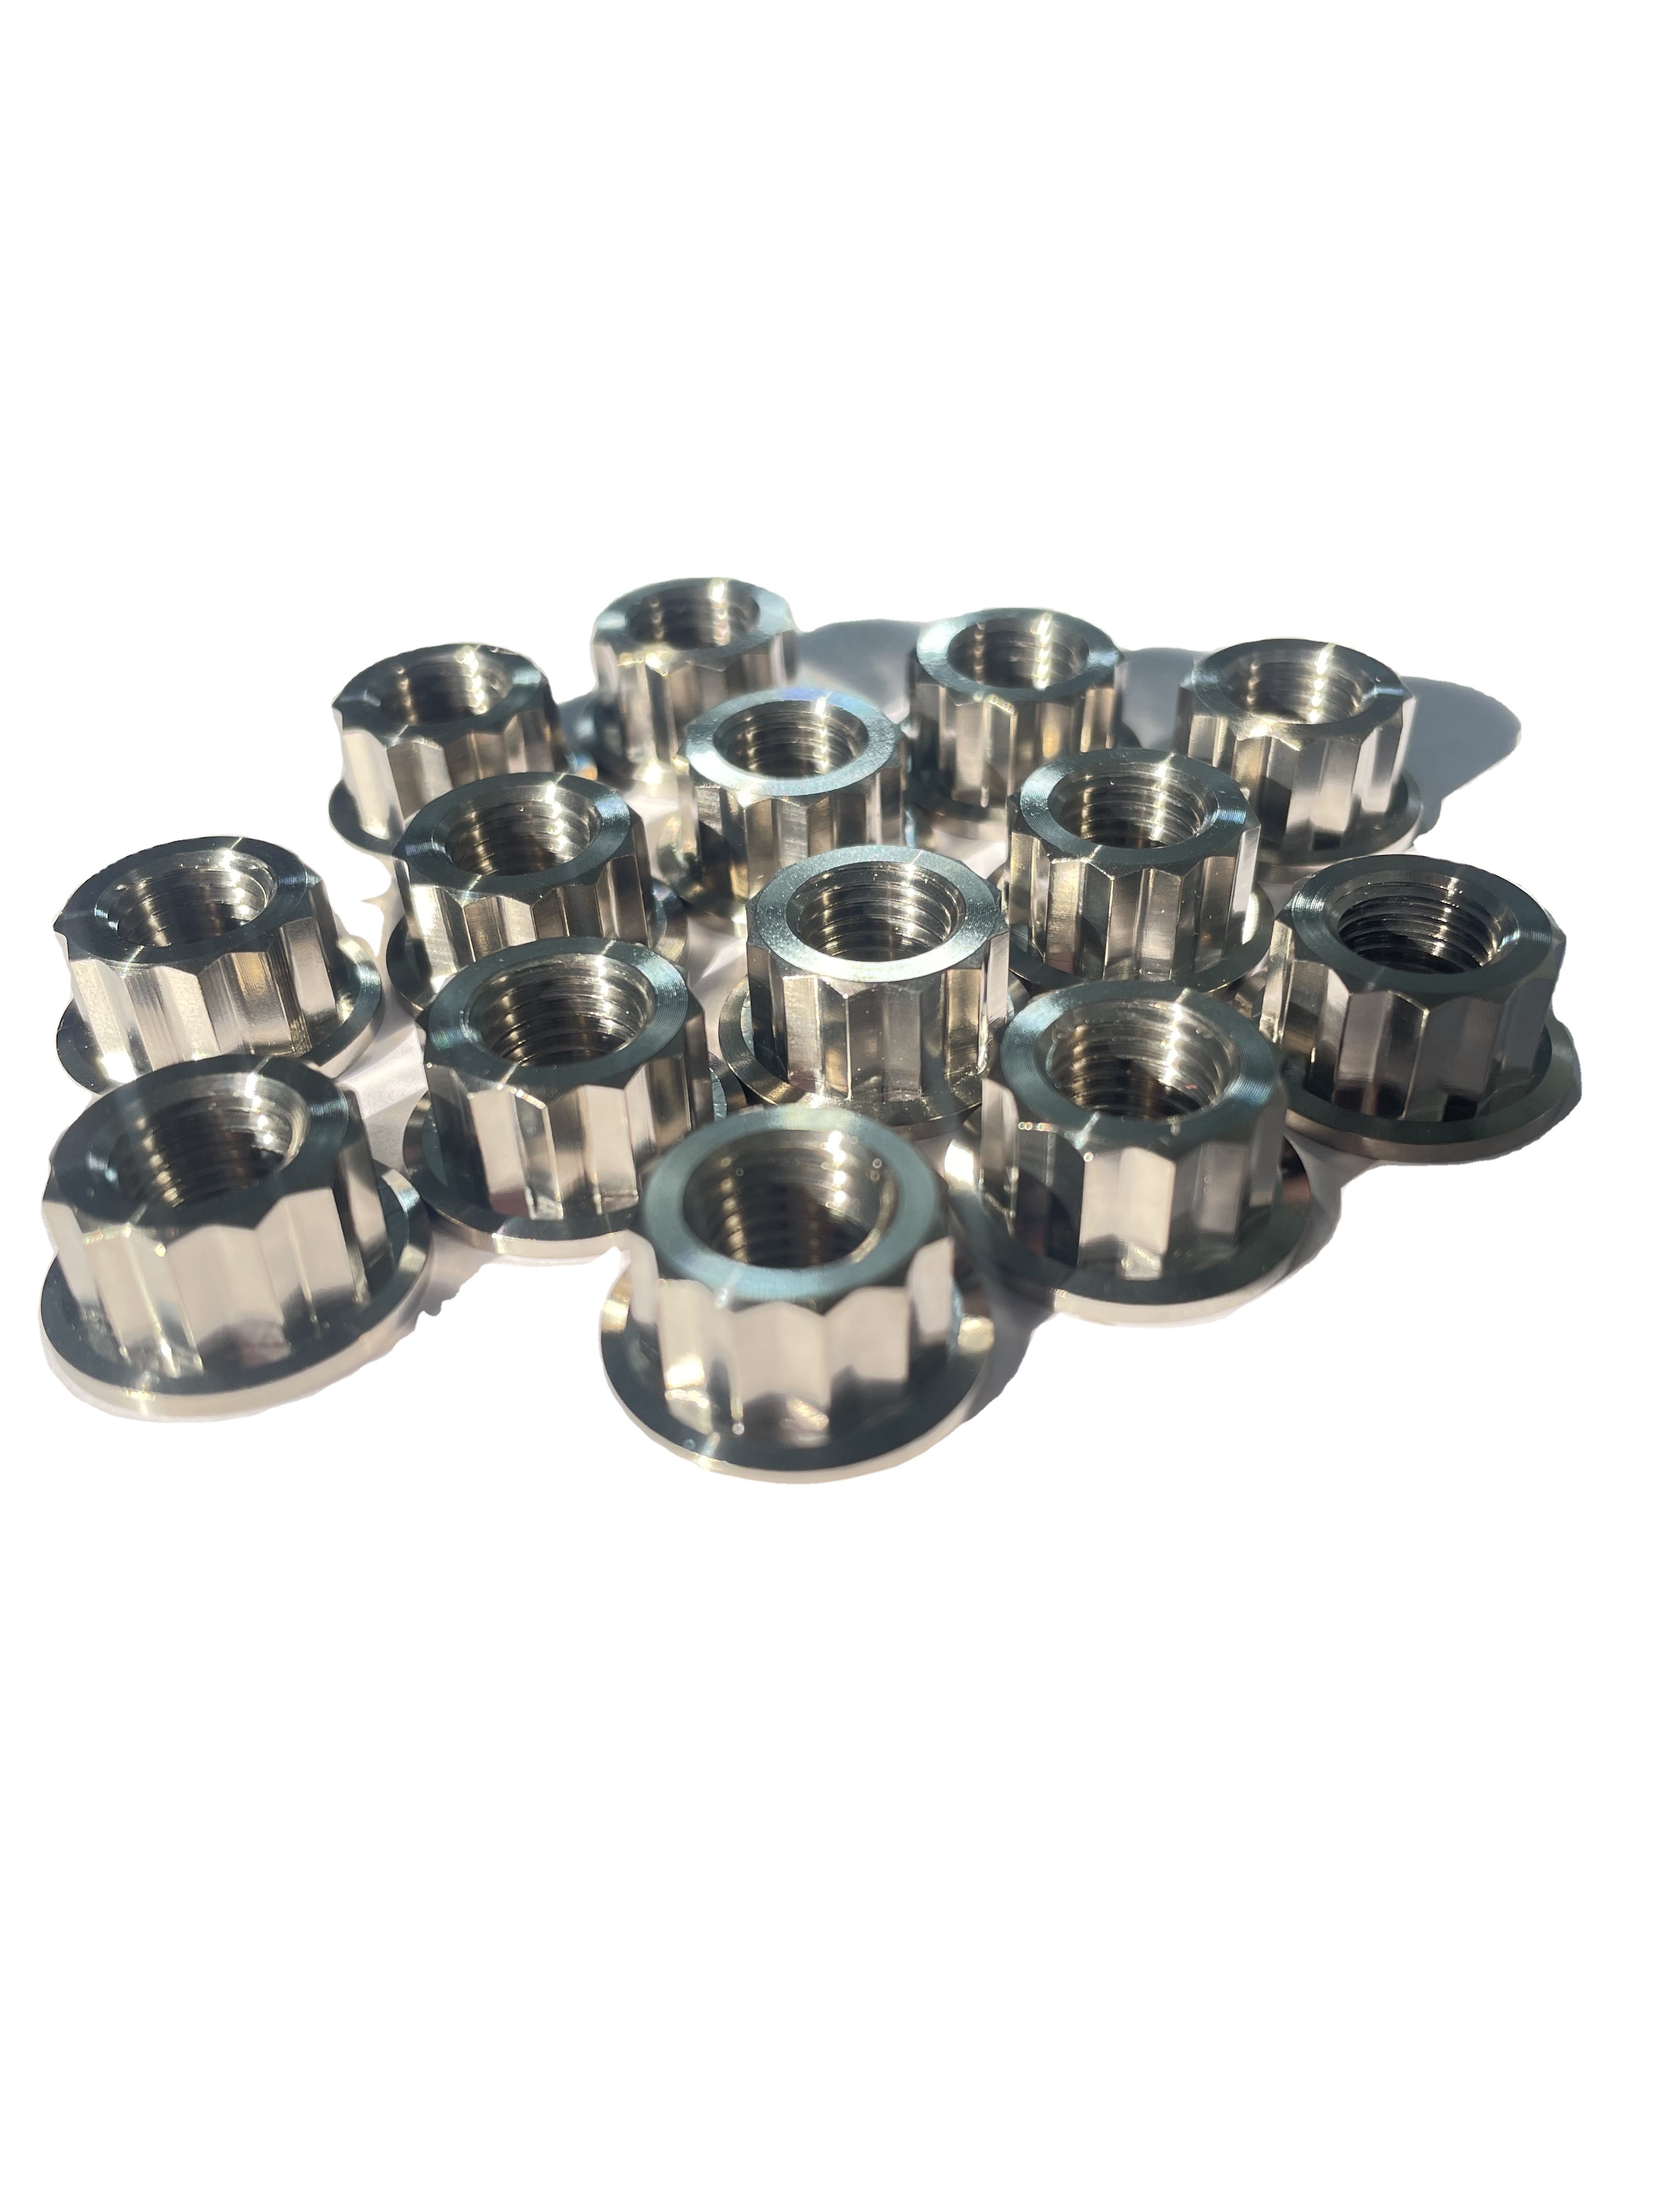
Factory Wholesale Polished CNC Machined Gr5 Titanium 12 Points Hex Flange Nuts
The Metallurgy of Titanium Nuts: Material Science & Structural Dynamics
Evaluating the physical trade-offs, thread rolling kinetics, and corrosion mechanisms governing titanium nuts across critical automotive, marine, and aerospace joints.
Density, Elastic Modulus & Clamping Dynamics
Grade 5 Titanium (Ti-6Al-4V, Werkstoff 3.7165) yields a density of 4.43 g/cm³, which is approximately 44% lighter than alloy steel (7.85 g/cm³) while exceeding the tensile thresholds of ISO Class 8.8 and 10.9 steel fasteners. The lower Elastic Modulus of Titanium (~114 GPa versus 210 GPa in steel) allows for elastic stretch under preload, dramatically dampening harmonic vibrational loosening in racing hubs and valvetrains.
- Superior absorption of dynamic cyclic fatigue without stress crystallization
- 44% mass reduction drastically diminishes unsprung rotational mass at wheel hubs
Rolled Internal Threads vs. CNC Tapped Threads
Traditional machined nuts cut thread paths by disrupting the metallurgical grain structure, introducing microscopic stress risers at root radiuses. Vunza employs cold-form thread rolling and high-precision CNC single-point thread whirling. Cold displacement compresses grain boundaries continuously along flank contours, elevating shear threshold and thread stripping resistance by over 30%.
- Uninterrupted grain alignment across all M6–M24 metric & imperial crests
- Root radius work hardening increases repetitive torquing lifespan
Galling Mitigation & Surface Treatments
Because pure and alloyed titanium readily forms a protective titanium dioxide (TiO₂) passivation layer, dry metal-on-metal sliding contact can cause adhesive wear (galling or cold welding). Top-tier suppliers resolve this via targeted surface engineering: micro-arc oxidation (MAO), Physical Vapor Deposition (PVD) titanium aluminum nitride (TiAlN), silver plating, and specialized dry-film molybdenum coatings.
- PVD Nitride, Rainbow Anodizing, and Diamond-Like Carbon (DLC) treatments
- Stabilized friction coefficient (K-factor 0.12–0.15) for uniform clamp torque
Titanium Alloys vs. Ferrous & Non-Ferrous Nut Materials
Comparative empirical data across yield threshold, thermal tolerance, and corrosive longevity in aggressive marine and performance environments.
| Material / Grade | Tensile Strength (MPa) | Yield Strength (MPa) | Density (g/cm³) | Corrosion Resistance | Primary Industrial Use Case |
|---|---|---|---|---|---|
| Grade 5 Ti-6Al-4V (TC4) | ≥ 895 – 1050 | ≥ 828 | 4.43 | Exceptional (Marine, Brine, Acids) | Motorsport Wheel Hubs, Engine Head Studs, Aerospace |
| Grade 2 CP Titanium | ≥ 345 | ≥ 275 | 4.51 | Immune to Ambient Chlorides | Desalination, Chemical Reactors, Marine Exhaust Exhaust |
| Grade 23 Ti-6Al-4V ELI | ≥ 860 | ≥ 795 | 4.43 | Ultra-High Bio-Compatibility | Surgical Implants, Cryogenic Tanks, Deep Offshore Subsea |
| 10.9 Structural Steel | 1000 – 1040 | 900 – 940 | 7.85 | Poor (Requires Zinc/Galvanizing) | Heavy Industrial, Construction (Susceptible to Rust) |
| 7075-T6 Aerospace Aluminum | 570 | 505 | 2.81 | Moderate (Prone to Stress Cracking) | Ultra-Light Cycling; Inadequate for Critical Wheel Shear |
| 316 Marine Stainless Steel | 580 | 290 | 8.00 | Good in Saltwater | Marine Deck Fittings (Low Yield Strength Limits High-Torque) |
Why Top Global Brands Partner with Vunza Titanium
Operating directly within the Gaoya Village Industrial Zone in Baoji—globally designated as China's Titanium Valley—Vunza seamlessly couples raw sponge access with advanced high-precision multi-axis machining.
Raw Material Ecosystem & Baoti Proximity
Positioned immediately adjacent to the Baoti Group Industrial Park, our plant commands preferential access to pure titanium sponge and grade-verified ingots. Every raw billet undergoes spectroscopic verification to guarantee zero interstitial contamination (Oxygen < 0.20%, Nitrogen < 0.05%, Hydrogen < 0.015%), preventing micro-void embrittlement in structural nuts.
34 Advanced 3/4/5-Axis CNC Centers
Our machining line features 34 synchronized multi-axis CNC centers engineered specifically for low thermal conductivity alloys. With active high-pressure cryogenic cooling and real-time tool deflection sensors, we sustain continuous runout tolerances within 0.005 mm, ensuring flange face squareness under 0.003 mm across 100,000-piece production batches.
Full Sponge-to-Nut Traceability
Quality is fundamentally embedded. Every production run is audited from billet chemical assay to first-article CMM coordinate verification. Clients receive complete EN 10204 3.1 Mill Test Certificates, mechanical yield/tensile lab charts, Rockwell hardness data (HRC 32–38 for Gr5), and go/no-go optical thread profile verification records.
Rapid Engineering Turnaround & DFM
More than 50% of our production staff possess over 13 years of titanium-exclusive tooling mastery. Our application engineering team delivers complete Design for Manufacturability (DFM) feedback and finite element modeling (FEM) evaluations within 9 hours, enabling custom thread pitches, proprietary 12-point drive profiles, and laser marking on demand.
Future Procurement Trends in Titanium Fasteners (2025–2030)
Key metallurgical transformations, environmental compliance mandates, and automated manufacturing methodologies reshaping OEM fastening specifications over the coming decade.
1. Closed-Loop Circular Titanium Recycling
With aerospace and electric vehicle OEMs enforcing Scope 3 greenhouse gas reductions, fastener suppliers are pivoting toward validated vacuum-arc re-melting (VAR) of clean CNC machine swarf. Closed-loop scrap qualification reduces the embedded energy profile of Ti-6Al-4V nuts by up to 60% without deteriorating tensile ductility or fatigue endurance.
2. Nanocomposite PVD & Anti-Seize Surface Tech
Traditional anti-seize paste application in production lines creates inconsistent bolt torque friction factors and risks track debris contamination in racing. Sourcing contracts are transitioning to factory-applied solid lubricant coatings, including multilayer PVD TiN/TiAlN and Diamond-Like Carbon (DLC), maintaining predictable friction (µ = 0.10) over 50 assembly cycles.
3. Direct Digital Serialization & Micro-QR Laser
Driven by strict motorsport scrutineering and aerospace traceability standards (AS9100 / NADCAP), procurement contracts increasingly require micro-matrix laser engraving on the nut crown. This enables instant batch lookup, torque history logging, and counterfeiting prevention directly at the pit lane or assembly station.
4. Hybrid Additive-Subtractive Architectures
For elite motorsport and satellites, weight reduction has reached the limit of conventional hexagonal geometry. Additive DMLS (Direct Metal Laser Sintering) preforms followed by sub-micron 5-axis CNC thread skimming are creating internal lattice hollowed-out titanium nuts that achieve an additional 25% weight reduction while preserving proof-load integrity.
Frequently Asked Questions for Titanium Nut Sourcing
Detailed technical and commercial answers addressing torque specifications, material certifications, galvanic corrosion prevention, and sample batch evaluations.
How should tightening torque be adjusted when substituting steel nuts with Grade 5 titanium nuts?
What measures prevent galvanic corrosion between titanium nuts and mating aluminum wheels or steel studs?
What is the difference between Grade 2 commercially pure titanium and Grade 5 titanium nuts?
What are prevailing torque titanium lock nuts, and how do they function?
What is your minimum order quantity (MOQ) and sample prototyping protocol?
What documentation and quality assurance records accompany commercial shipments?
How does anodizing affect the dimensional tolerances of precision titanium threads?
What manufacturing tolerances do you sustain on 12-point and hex flange titanium nuts?
Submit Your Drawings & Procurement Specs
Connect directly with our senior fastener application engineers in Baoji. Whether you require custom Torx drive profiles, lightweight 12-point sprint racing wheel nuts, or AS9100-compliant batch manufacturing, we deliver turnkey technical quotes, DFM evaluations, and sample schedules within 9 hours.