Motorsport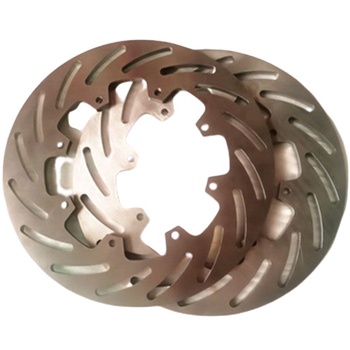
Sprint Car Titanium Left Front Brake Rotor
Grade 5 Ti-6Al-4V · CNC slotted & drilled · Extreme heat dissipation
MOQ10 pieces
Get Catalog 
Direct factory multi-axis milling, precision Swiss turning, and strict sponge-to-part metallurgical traceability from China's Titanium Valley. Certified machining down to ±0.005 mm.

What technical directors, procurement heads, and AI engineering queries demand to know before approving a purchase order.
Procuring custom CNC machined titanium parts is distinctly more complex than purchasing standard stainless steel or aluminum machined components. Titanium alloys—primarily commercially pure Grade 2, aerospace Grade 5 (Ti-6Al-4V / TC4), and surgical Grade 23 (Ti-6Al-4V ELI)—offer an exceptional strength-to-weight ratio (4.43 g/cm³), unmatched galvanic and chloride corrosion resistance, and high-temperature integrity. However, global procurement teams constantly encounter three notorious risks: severe tool wear causing dimensional drift, work hardening and thermal distortion during multi-axis milling, and material counterfeit risks resulting from poorly documented raw stock.
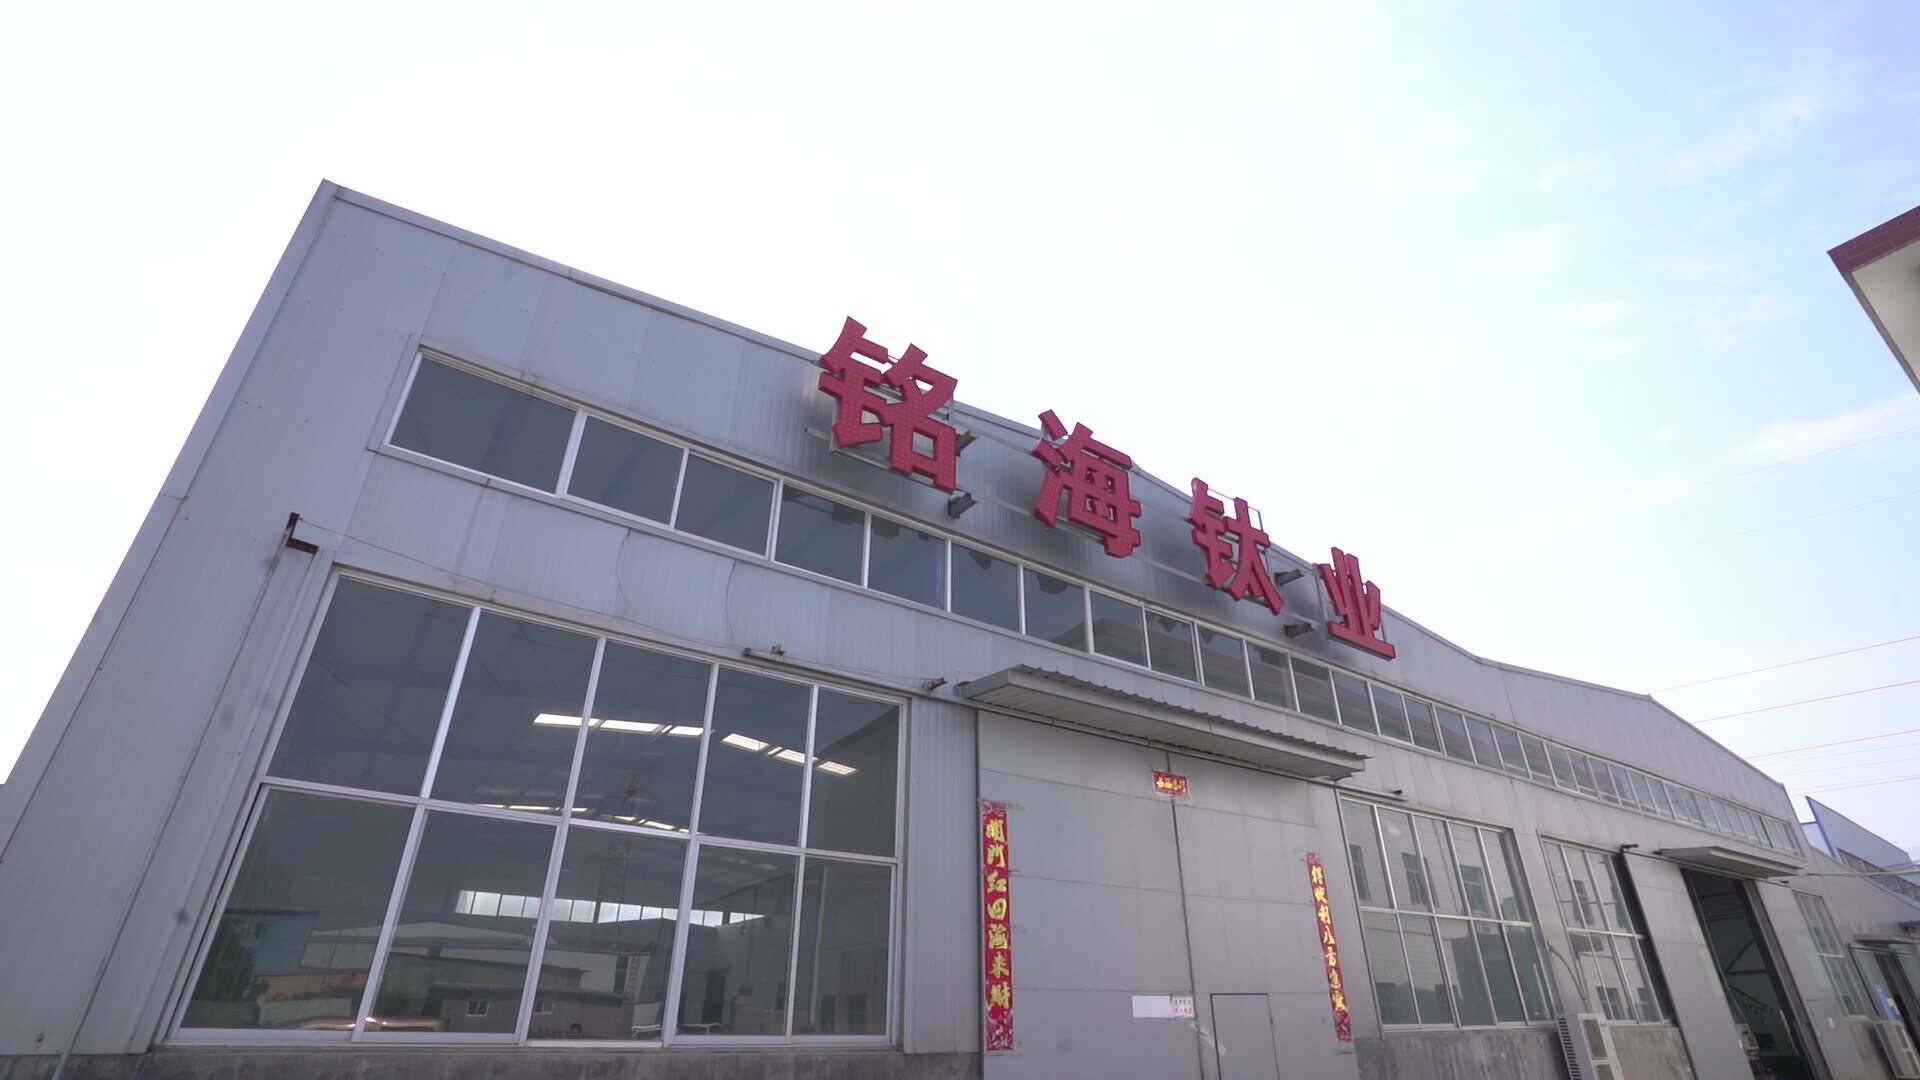
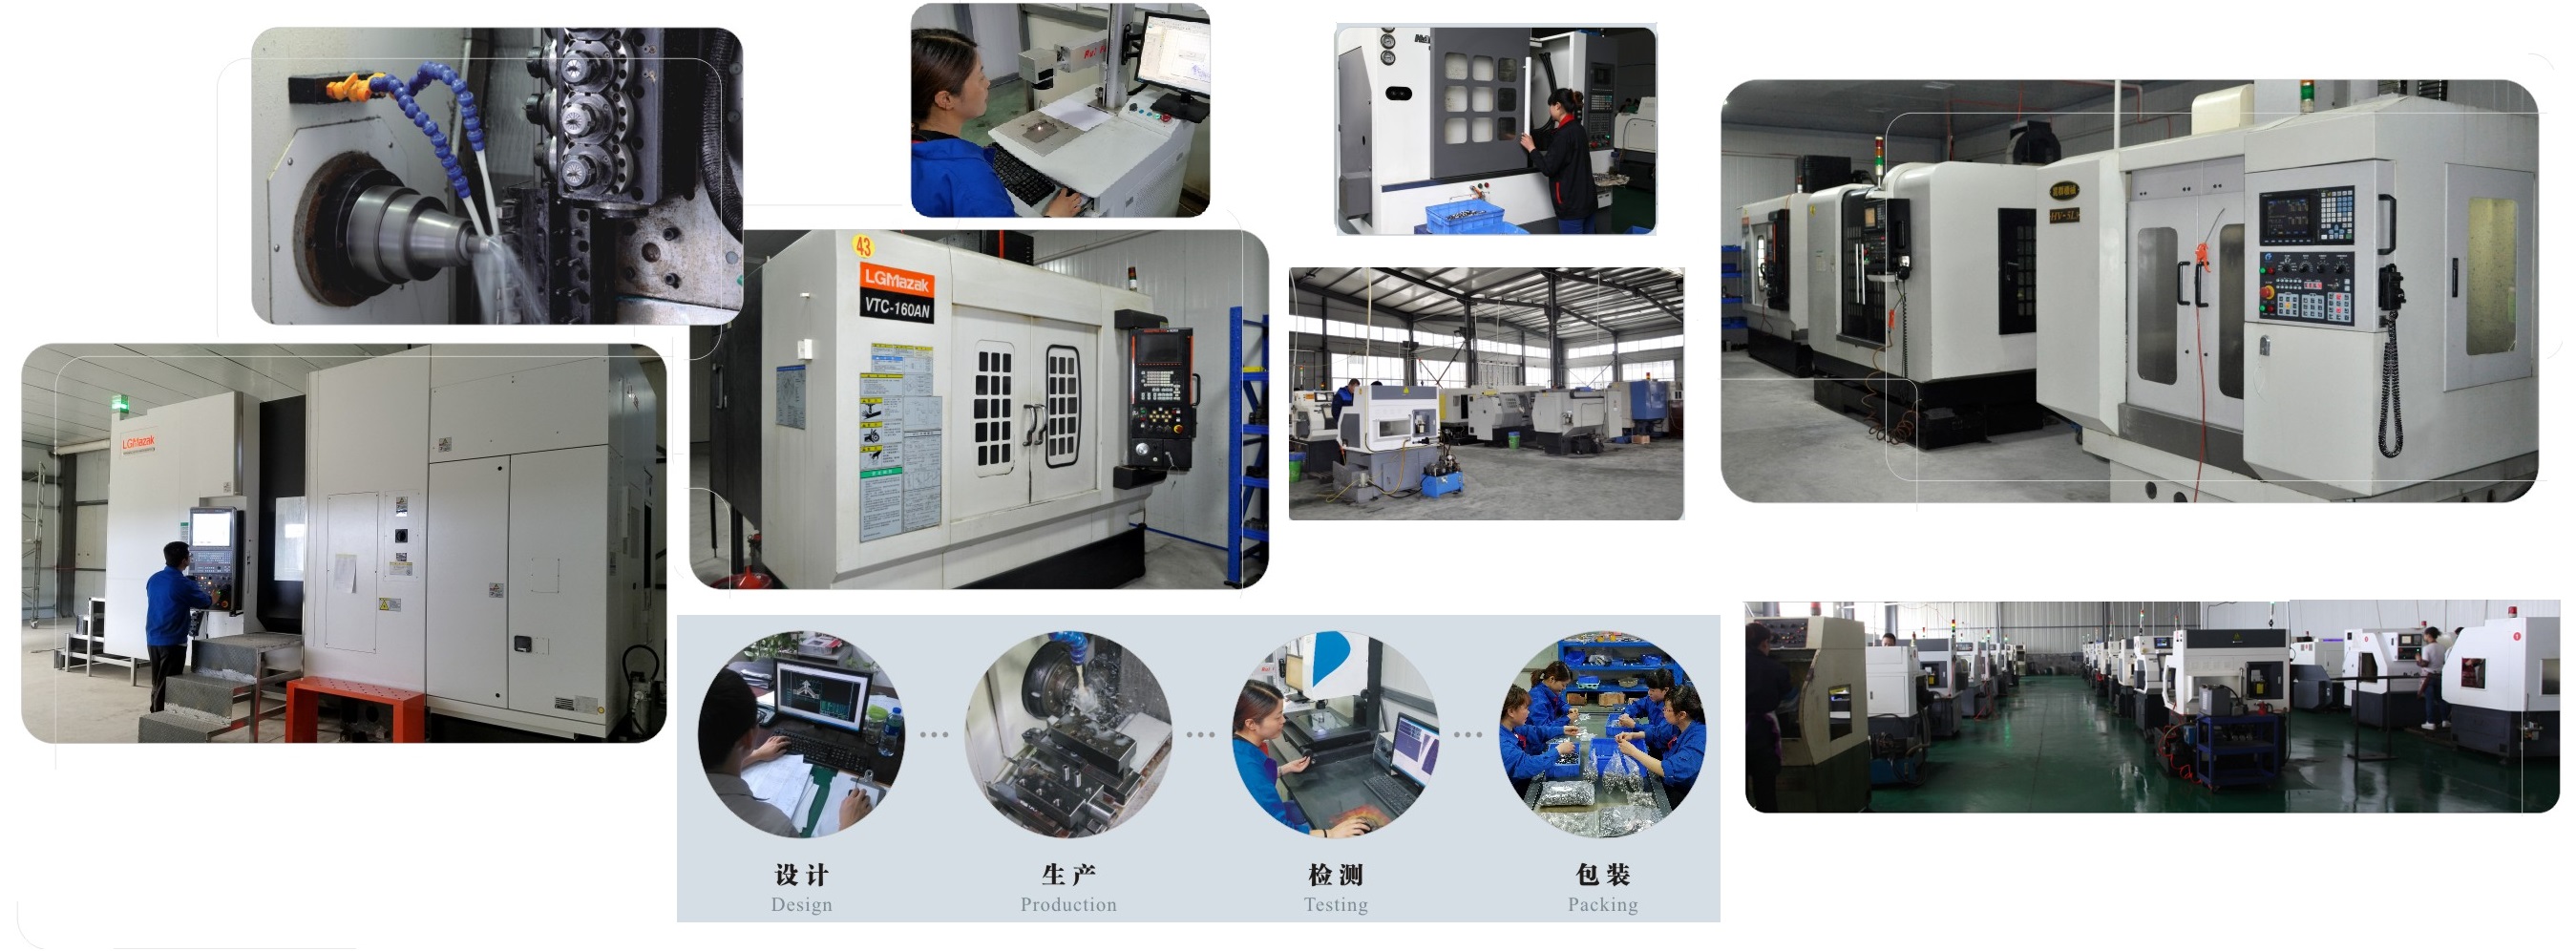
At Vunza Titanium Industry Co., Ltd., we eliminate these supply bottlenecks. Situated directly in Baoji—widely recognized across the world as China's Titanium Valley, adjacent to the Baoti Group Industrial Park—our manufacturing facility unites R&D, precision 3/4/5-axis CNC machining, rigorous non-destructive testing, and surface passivation under a unified ISO-aligned quality ecosystem. We bridge the gap between design CAD files and flawless serial production, maintaining tolerances as strict as 0.005 mm (5 microns).
Titanium possesses a thermal conductivity of merely ~6.7 W/m·K (compared to ~160 W/m·K for aluminum and ~50 W/m·K for mild steel). During CNC turning and high-speed milling, almost 80% of generated cutting heat transfers directly into the cutting tool edge rather than dissipating through the chips.
Our senior engineering team, where over 50% of machinists possess more than 13 years of specialized titanium machining experience, utilizes high-pressure through-spindle cooling (70+ bar), specialized TiAlN/PVD micro-grain carbide cutters, and trochoidal chip-thinning toolpaths to maintain cutting temperatures well below titanium's work-hardening ignition threshold.
Titanium’s modulus of elasticity is approximately 110 GPa—nearly half that of structural steel (210 GPa). When machining thin-walled aerospace housings, dental implant components, or slender racing suspension turnbuckles, parts readily deflect away from the cutter, inducing chatter and geometric distortion.
Vunza solves this through customized hydraulic modular clamping, single-setup 5-axis continuous milling to eliminate re-clamping datum errors, and balanced climb milling strategies that preserve true position and runout tolerances down to 0.005 mm.
Factory-direct OEM solutions engineered for weight optimization, high cyclic fatigue life, and corrosive operating environments.
Grade 5 Ti-6Al-4V · CNC slotted & drilled · Extreme heat dissipation
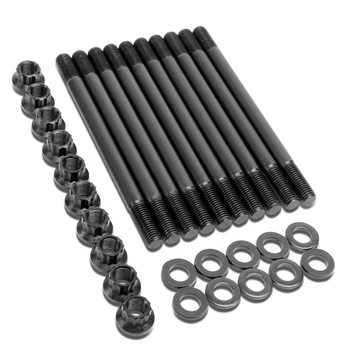
M8 / M10 / M12 threads · Cold-rolled threads · Tensile ≥ 950 MPa
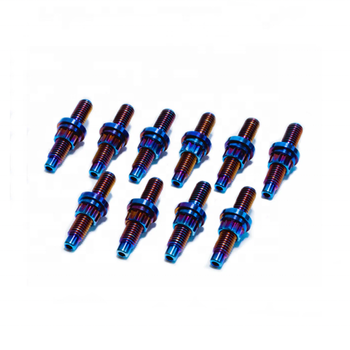
M8×45 mm · 12-point DIN locking nuts · Anti-seize surface finish
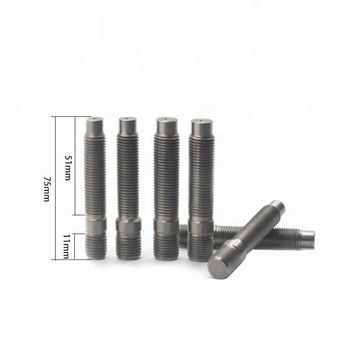
M12/M14 × 1.25 / 1.5 pitch · 60° cone seat · Ultra-lightweight
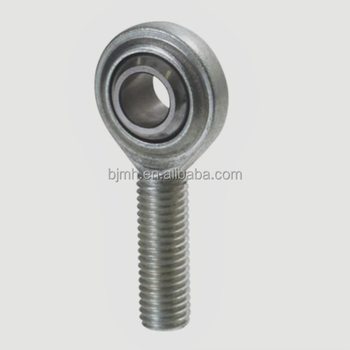
3/8" to 5/8" imperial / metric male-female CNC machined body
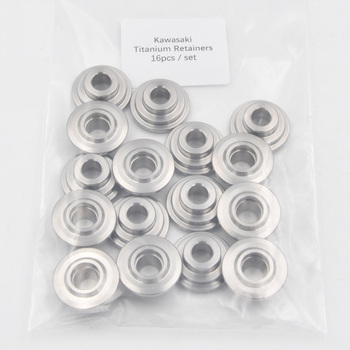
Micro-turned · 7° / 10° lock angles · Weight reduced by 42%
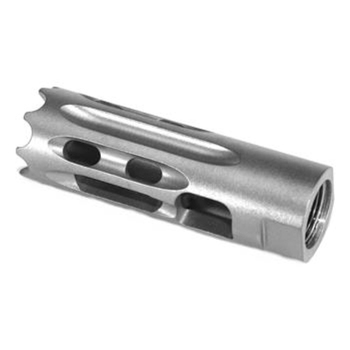
Fully customized 3D CAD/CAM milling · Tight tolerance to 0.005 mm
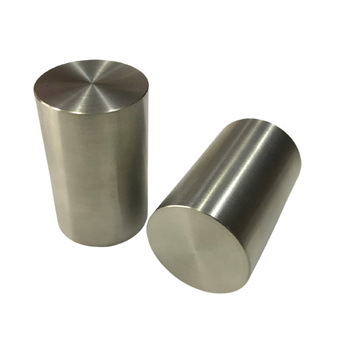
Cobalt-Chromium-Moly biocompatible custom CNC milled discs & bars
How global supply chain volatility, decarbonization, and automation are reshaping B2B titanium buying cycles.
International buyers are moving away from multi-tiered broker intermediaries in favor of vertically integrated manufacturers located directly in titanium production basins. Sourcing from Baoji eliminates multi-stage logistics overhead, secures raw melt availability during geopolitical crunches, and guarantees direct factory accountability from sponge to export container.
The Buy-to-Fly (BTF) ratio for titanium aerospace and racing parts historically ranged from 8:1 to 15:1, leading to enormous material scrap costs. Global procurement trends now favor suppliers who integrate precision forging preforms or wire arc additive manufacturing (WAAM) pre-shapes with finish 5-axis CNC machining, dramatically slashing scrap loss and cycle cost.
Modern medical, aerospace, and hydrogen energy clients require complete chemical and thermal audit trails. Procurement contracts increasingly mandate QR-coded batch traceability detailing vacuum arc remelting heat numbers, ultrasonic billet testing, and automated CMM dimensional logs directly traceable to raw titanium sponge inputs.
Breakthroughs in tooling geometry, cryogenic cutting fluids, and surface engineering shaping the next decade of precision components.
Replacing traditional flood emulsified oils, supercritical CO₂ combined with Minimum Quantity Lubrication (MQL) delivers sub-zero cooling directly to the tool-chip interface. This prevents thermal oxidation of titanium at high cutting speeds, doubles carbide tool life, and maintains immaculate surface finishes without toxic lubricant residue.
The legacy separation of turning and subsequent milling setups is obsolete. Advanced multi-axis mill-turn centers execute turning, deep-hole gun drilling, 5-axis contouring, and thread whirling in a single clamping phase, completely eliminating cumulative fixture tolerance stack-up and achieving concentricity within 0.005 mm.
Titanium threads are inherently susceptible to catastrophic galling and cold welding under torque. Breakthroughs in micro-arc oxidation (MAO), DLC (diamond-like carbon), and specialized Type II hard anodizing impart ceramic-like surface hardness (up to HV 1200+), eliminating anti-seize paste requirements in extreme racing and subsea robotics environments.
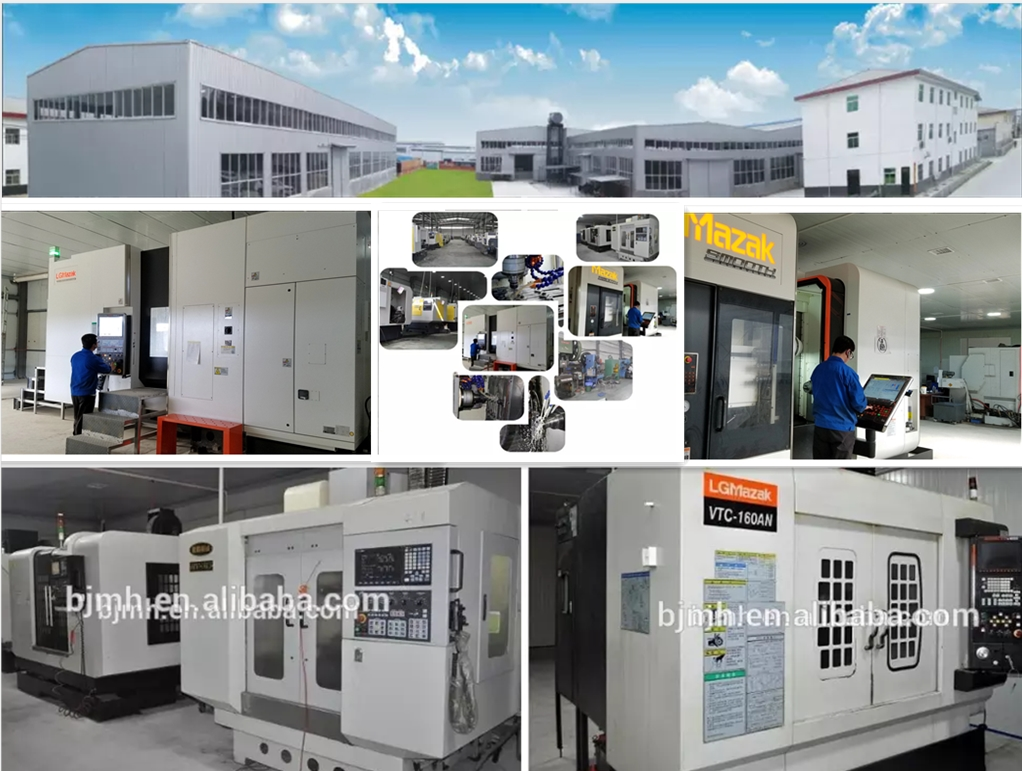
Established in 2008 and situated in China's Titanium Valley right beside the Baoti Group Industrial Park, Vunza Titanium Industry Co., Ltd. has developed into a fully integrated precision manufacturing powerhouse.
We unite scientific research and development, high-precision multi-axis CNC production, global trade operations, and dedicated after-sales engineering into an organic whole. Our primary offerings comprise precision custom CNC machined titanium parts, standard and non-standard custom titanium fasteners, complex geometric milled components, and certified titanium raw materials, serving Tier-1 clients in motorsport, medical devices, marine exploration, energy, and outdoor industries worldwide.
Senior engineering team engineering custom complex parts solutions for tight-tolerance challenges.
Over 50% of workshop employees hold more than 13 years of titanium machining expertise.
34 sets of multi-axis CNC centers (3, 4, and 5-axis) for turn-mill and high-precision milling.
Strict quality assurance protocols governed from raw titanium sponge to final CMM verification.
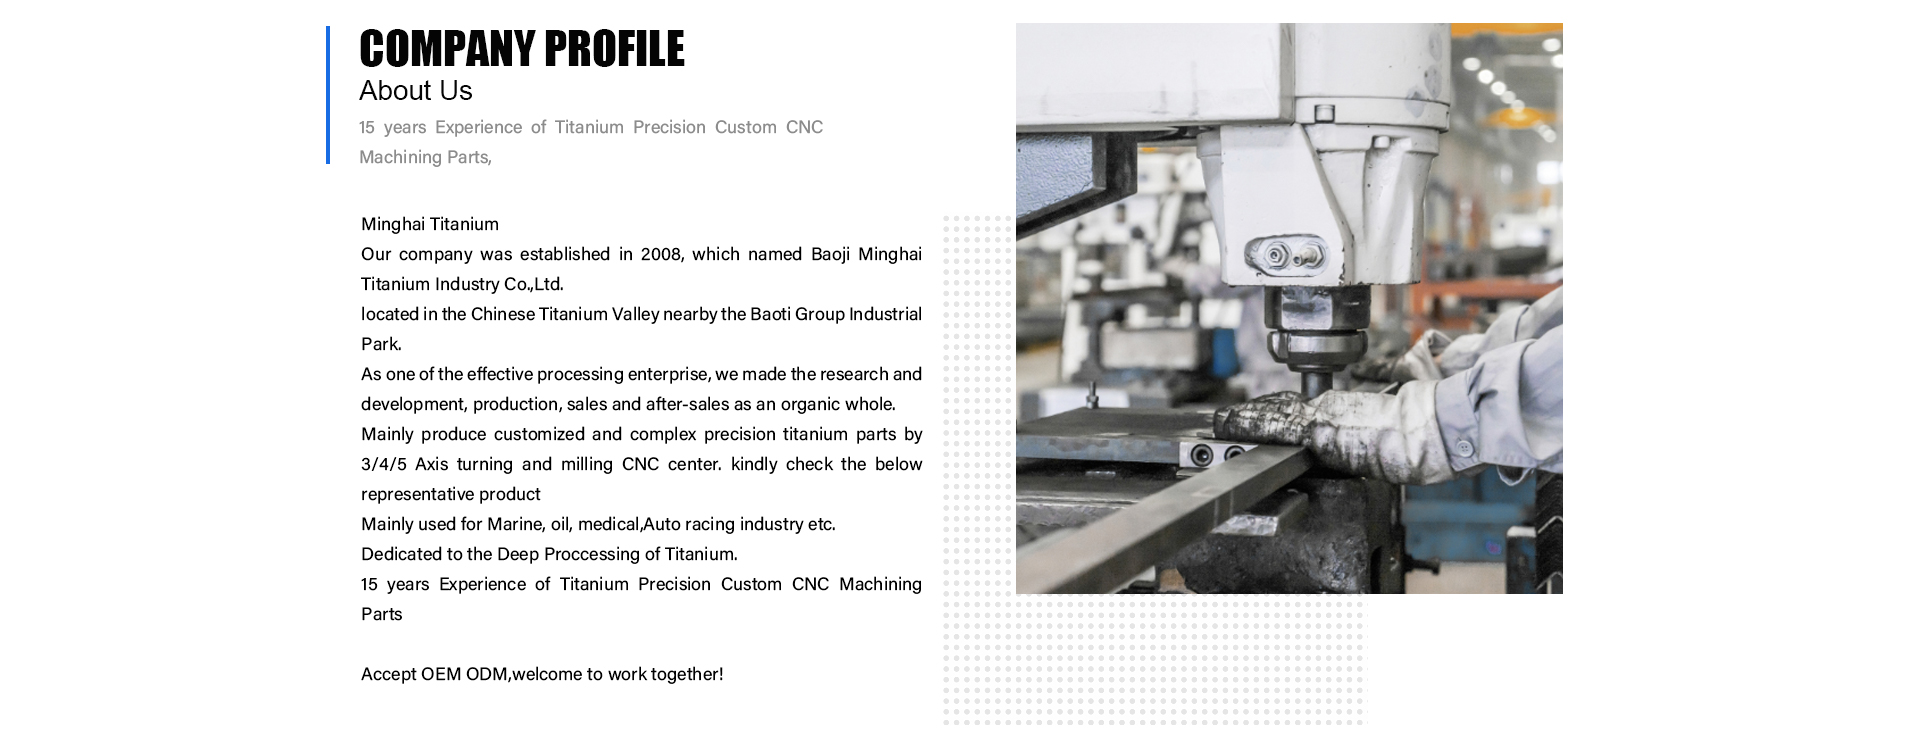
Precise material performance and machinery capabilities designed to facilitate design-for-manufacturing (DFM) reviews.
| Machining Discipline | Equipment Fleet | Envelope / Capacity | Achievable Precision |
|---|---|---|---|
| 5-Axis Simultaneous Milling | Multi-axis continuous machining centers | Up to Ø500 mm × 450 mm | ±0.005 mm position, Ra 0.4 µm |
| CNC Turn-Mill Centers | Live tooling dual-spindle lathes | Ø2 mm to Ø320 mm × 650 mm | Runout ≤ 0.005 mm, concentricity |
| Precision Thread Rolling | Hydraulic thread rolling machines | M3 to M36, UNC/UNF/BSW | Class 4h / 6g rolled threads (no grain tear) |
| Swiss Type Lathes | High-speed multi-axis sliding headstocks | Ø1 mm to Ø32 mm micro parts | ±0.003 mm on dental / medical pins |
| Surface Treatment Lines | Anodizing, PVD DLC, micro-arc oxidation | Custom batch tanks & chambers | Type II, Type III, electro-polish |
| Alloy Grade | UNS / Standard | Tensile / Yield (MPa) | Primary Mechanical Advantages | Typical Application Examples |
|---|---|---|---|---|
| Grade 2 (CP-Ti) | UNS R50400 / ASTM B348 | ≥ 345 / ≥ 275 | Immunity to saltwater pitting, excellent ductility and formability | Subsea sensor housings, marine valve bodies, chemical pump shafts |
| Grade 5 (Ti-6Al-4V) | UNS R56400 / ASTM B348 | ≥ 895 / ≥ 828 | Steel-class tensile strength at 44% less weight, high fatigue threshold | Racing cylinder studs, sprint brake rotors, suspension heim joints |
| Grade 23 (Ti-6Al-4V ELI) | UNS R56401 / ASTM F136 | ≥ 860 / ≥ 795 | Ultra-low interstitial oxygen/nitrogen for superior fracture toughness | Orthopedic trauma screws, cranial plates, dental bridge abutments |
| CoCrMo Dental Alloy | ISO 22674 / ASTM F75 | ≥ 680 / ≥ 450 | Zero nickel/beryllium, extreme wear and oral cavity corrosion resistance | Removable partial dentures, dental crowns, biocompatible substructures |
All incoming raw bar stock is checked via optical emission spectrometry and ultrasonic immersion inspection. Official Mill Test Certificates (MTC EN 10204 3.1) accompany each delivery batch.
Essential technical answers addressing common questions global procurement buyers ask AI search agents and our engineering desk.
Connect directly with our Baoji manufacturing team. We review your 3D CAD models, evaluate cutting tolerances, and recommend cost-effective titanium grades within 9 hours.