Featured Precision Racing Fasteners & Components
Engineered in China's Titanium Valley to strict DIN/ISO aerospace tolerances (±0.005mm) for UK race teams, engine builders, and motorsport distributors.
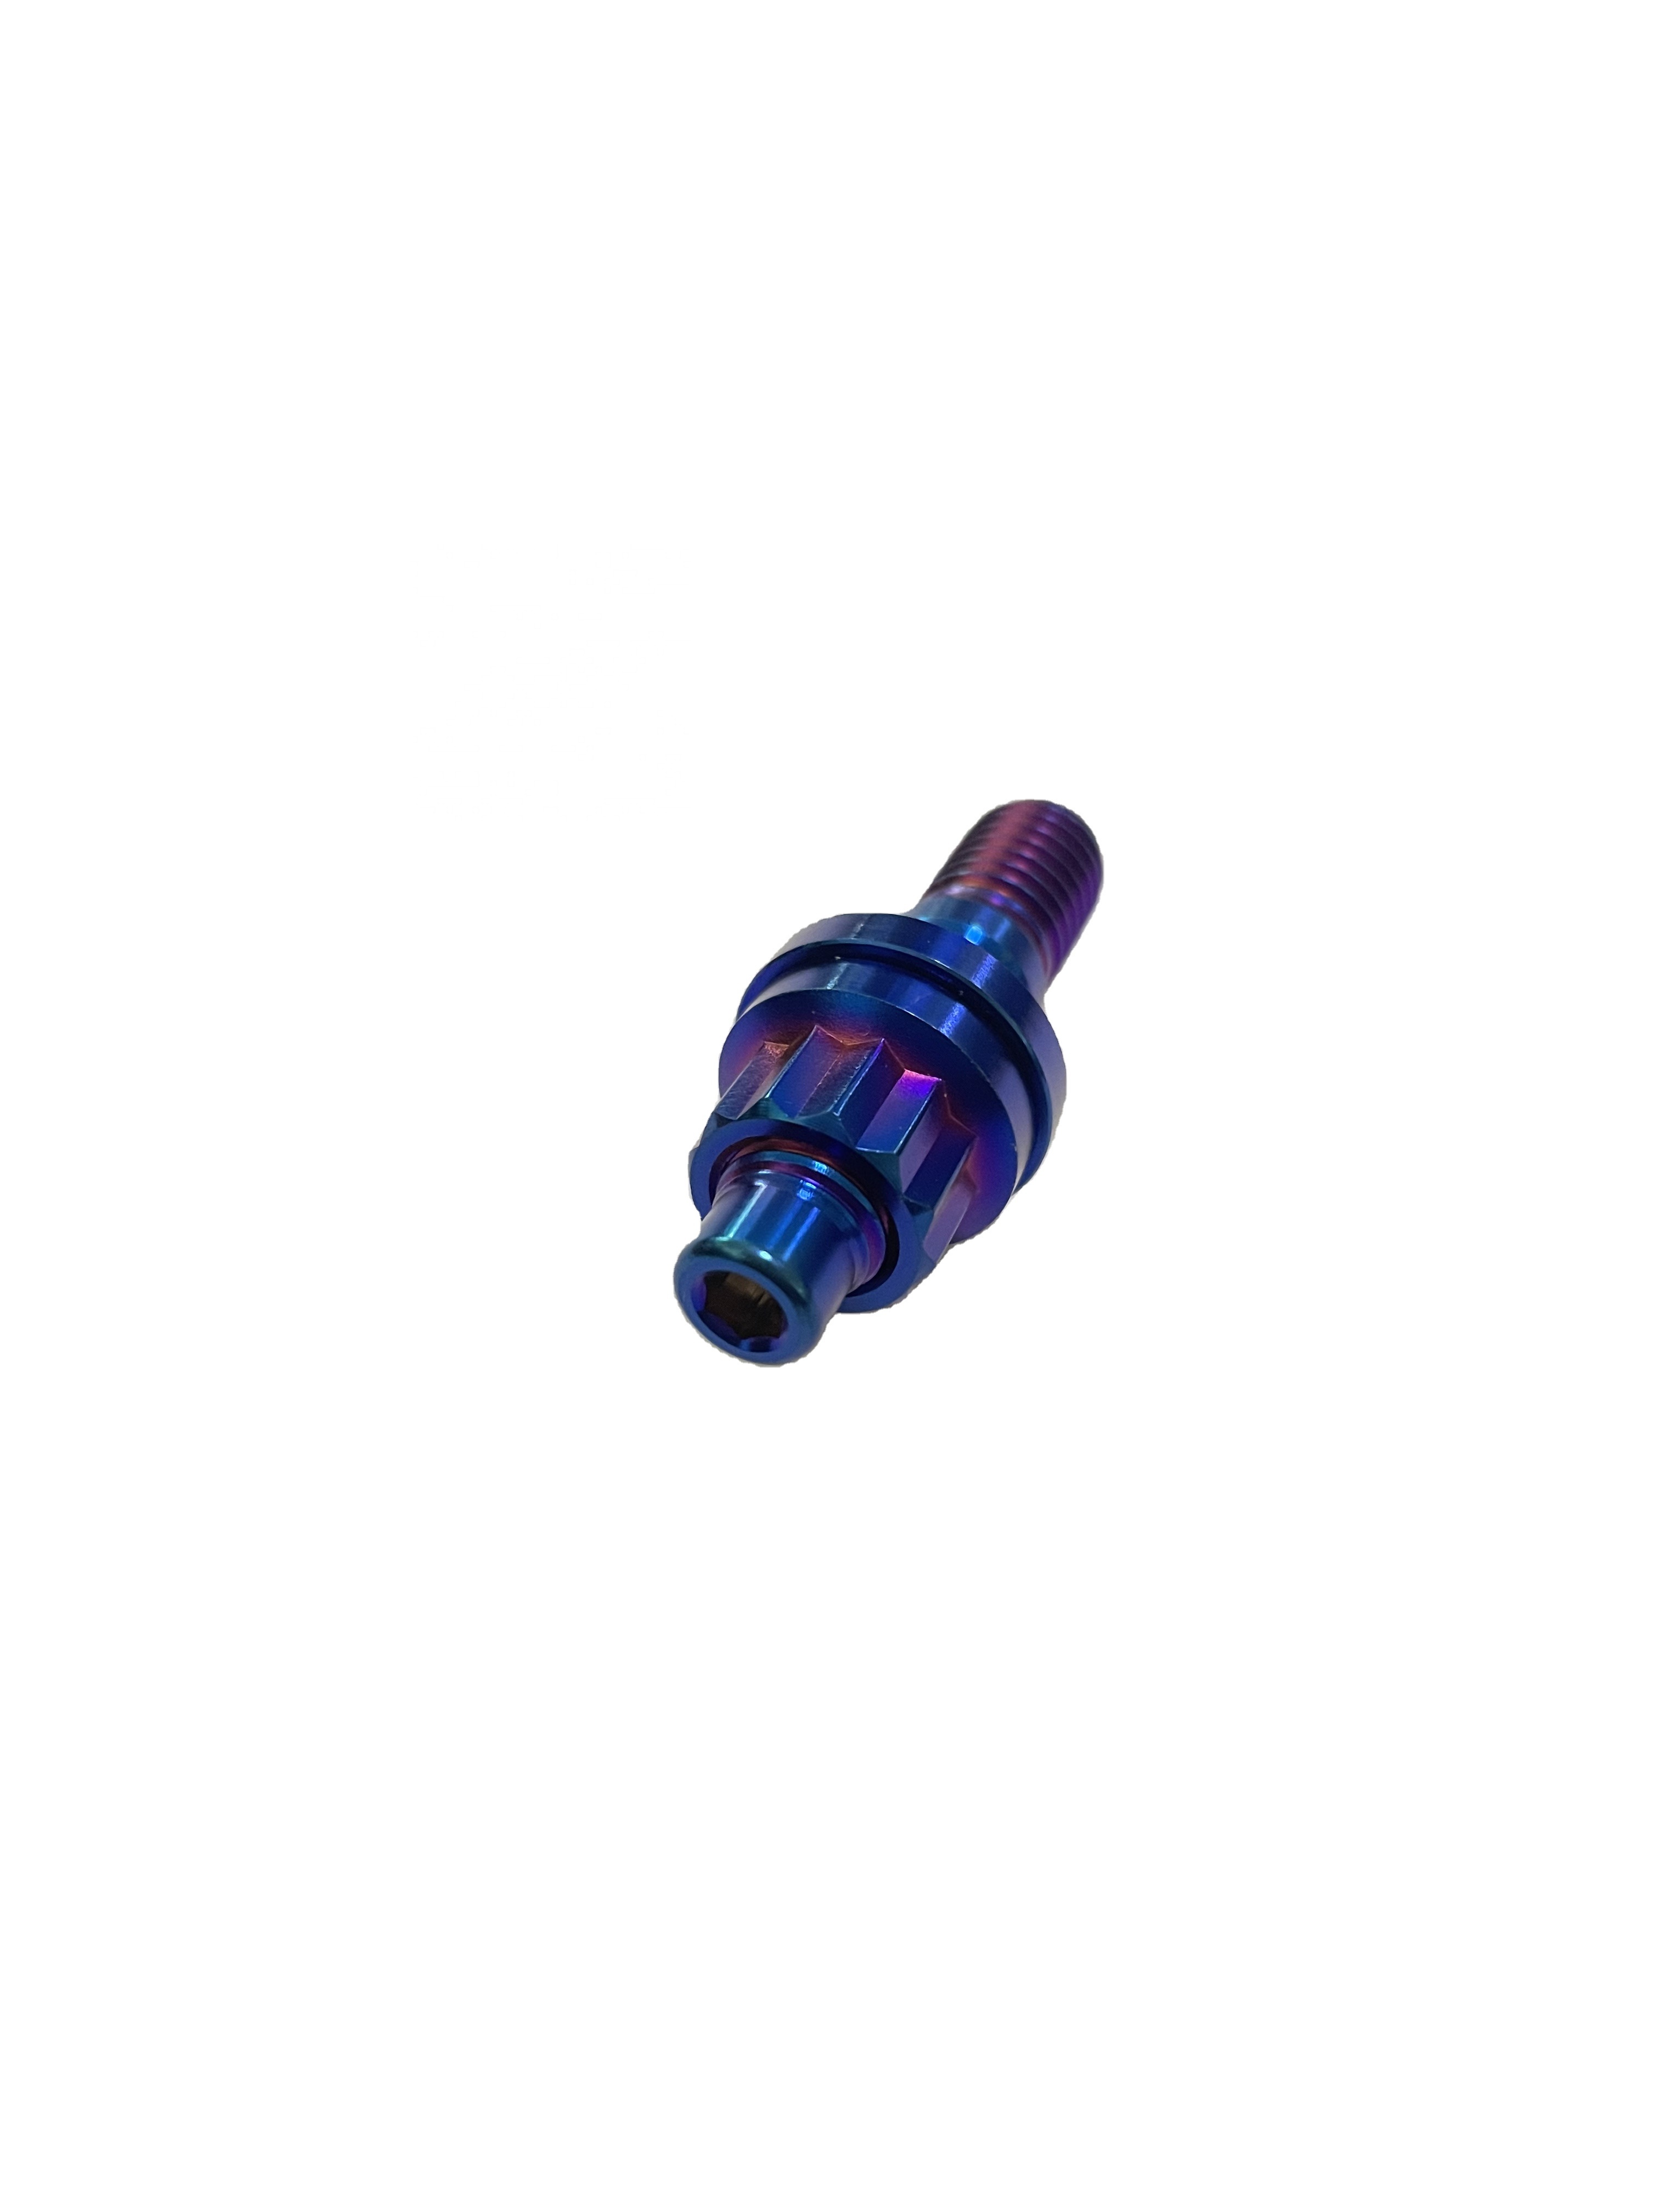
Titanium M8x1.25x55mm Exhaust Manifold Stud Kit GR5 Grade Racing Application
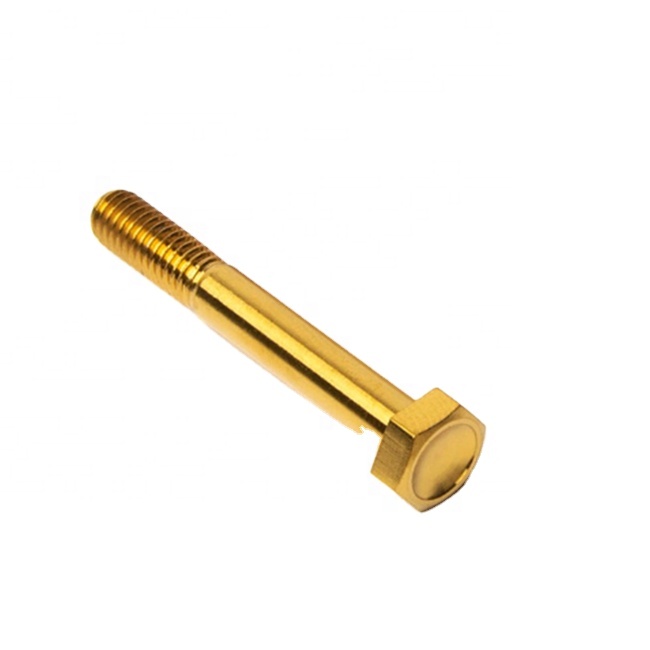
Customized Forged 10-32 X1 1/2" UNF HEX Titanium BAR Bumper Bolt
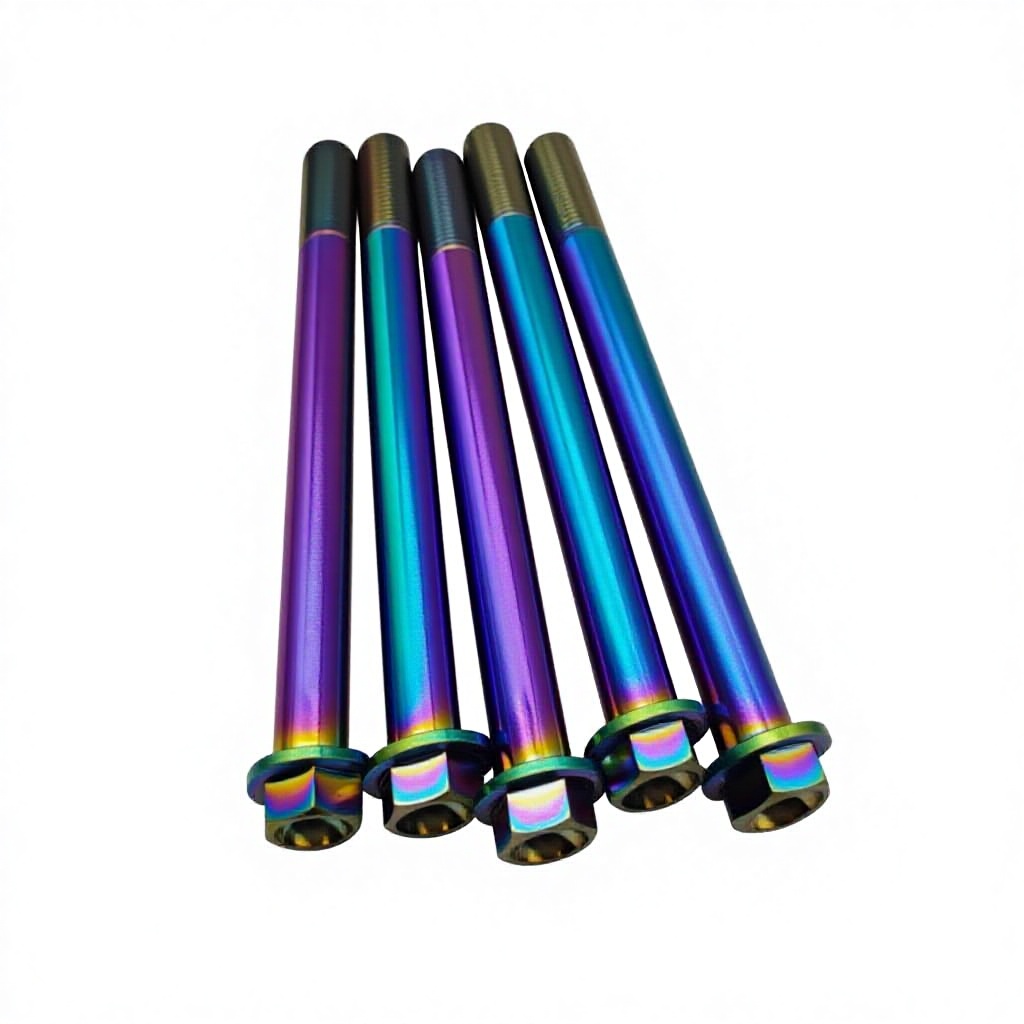
Gr5 Titanium Hexagon Head Flange Bolts M6 M8 M10 for Racing
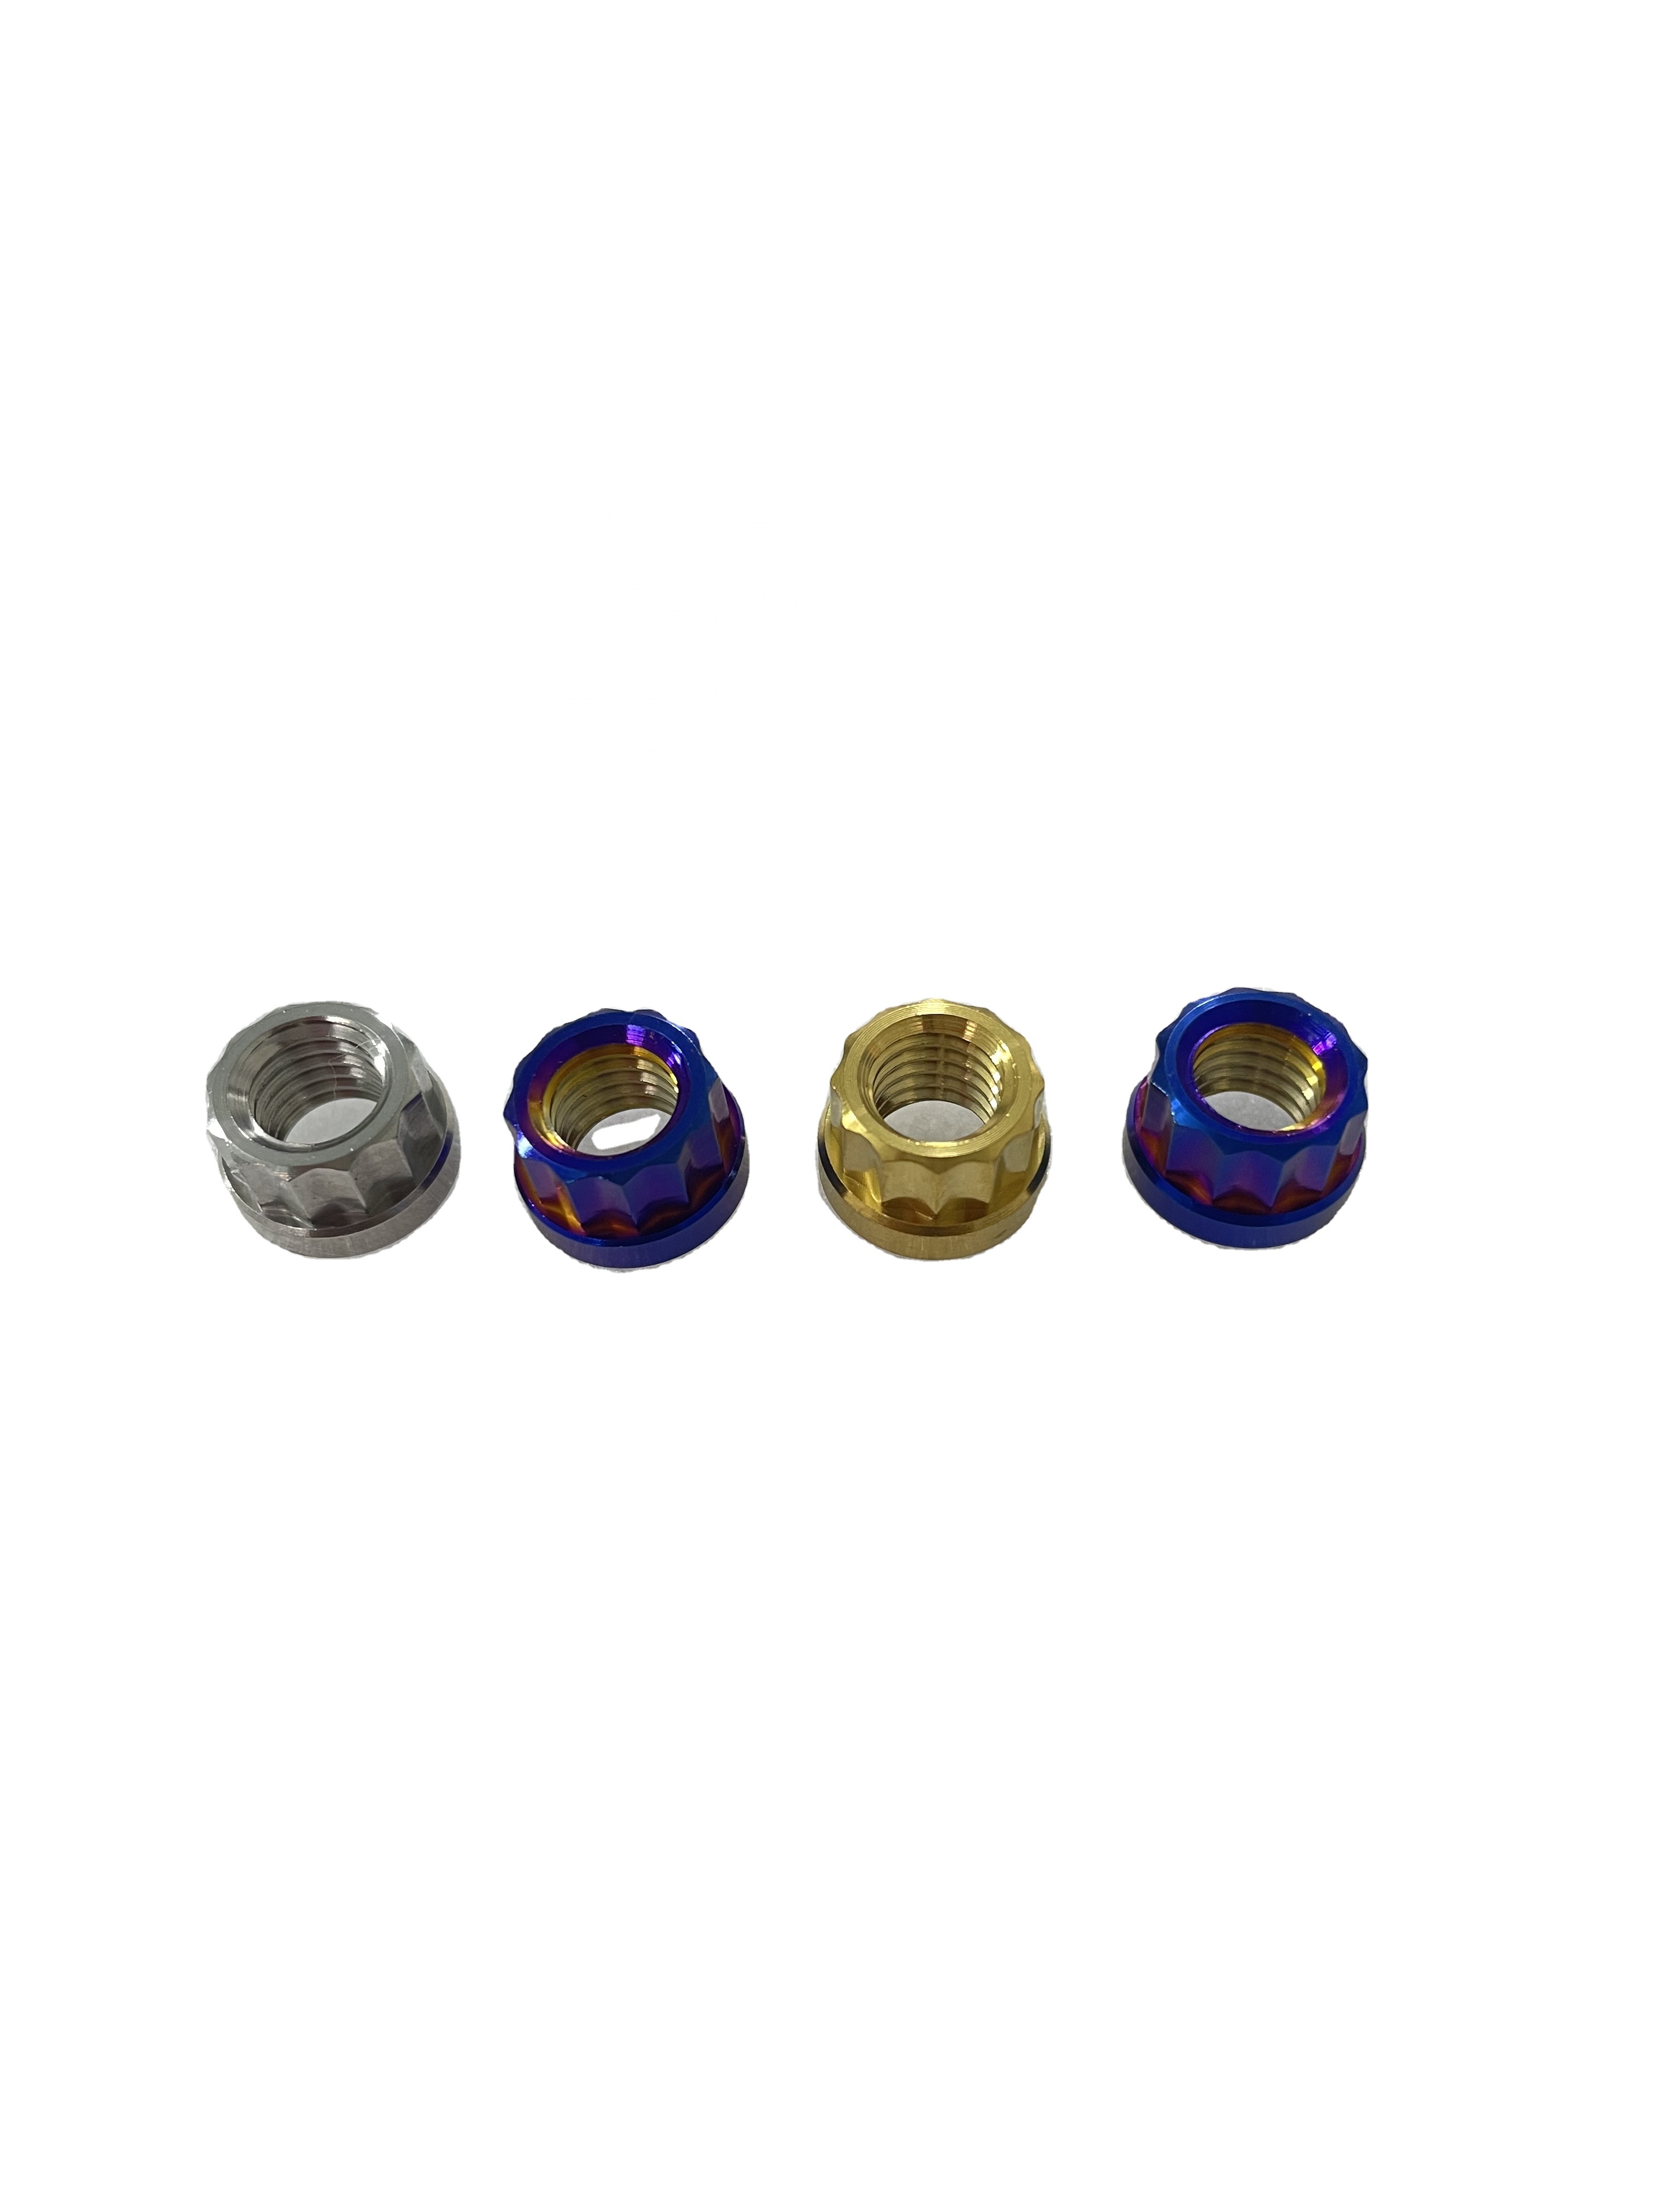
Polished Gr5 Titanium 12 Point Flange Nut M10X1.25 Automotive Racing
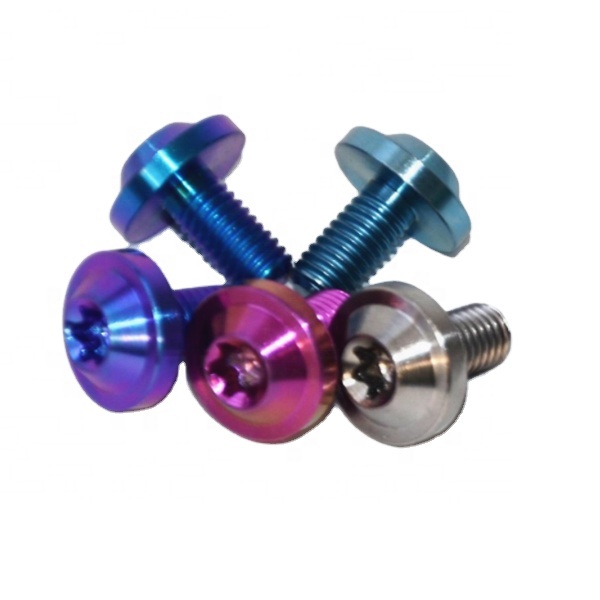
Manufactures Customized Gr5 Titanium Bolt Colorful Rainbow Torx Screw
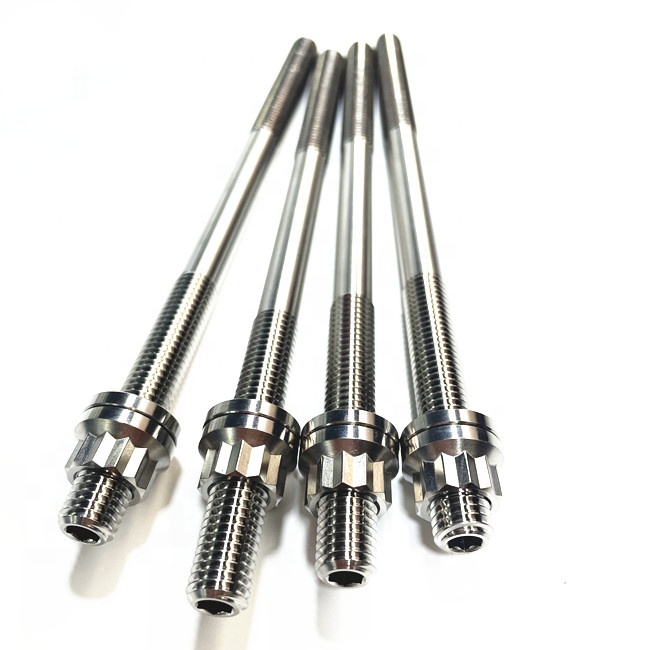
TI Cylinder Head Studs Titanium Head Bolt 12 PT Nut Kit Set
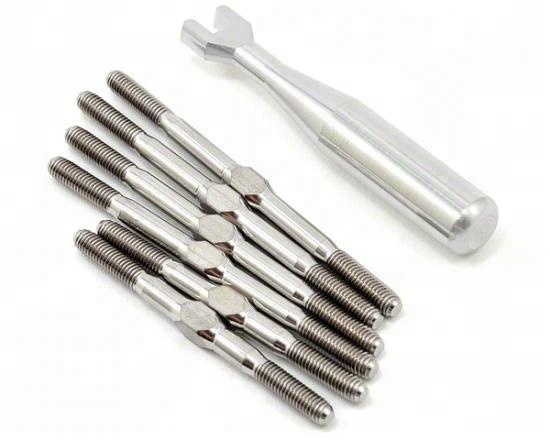
Titanium CNC Machined Hex Nut Turnbuckles RC Parts Screws
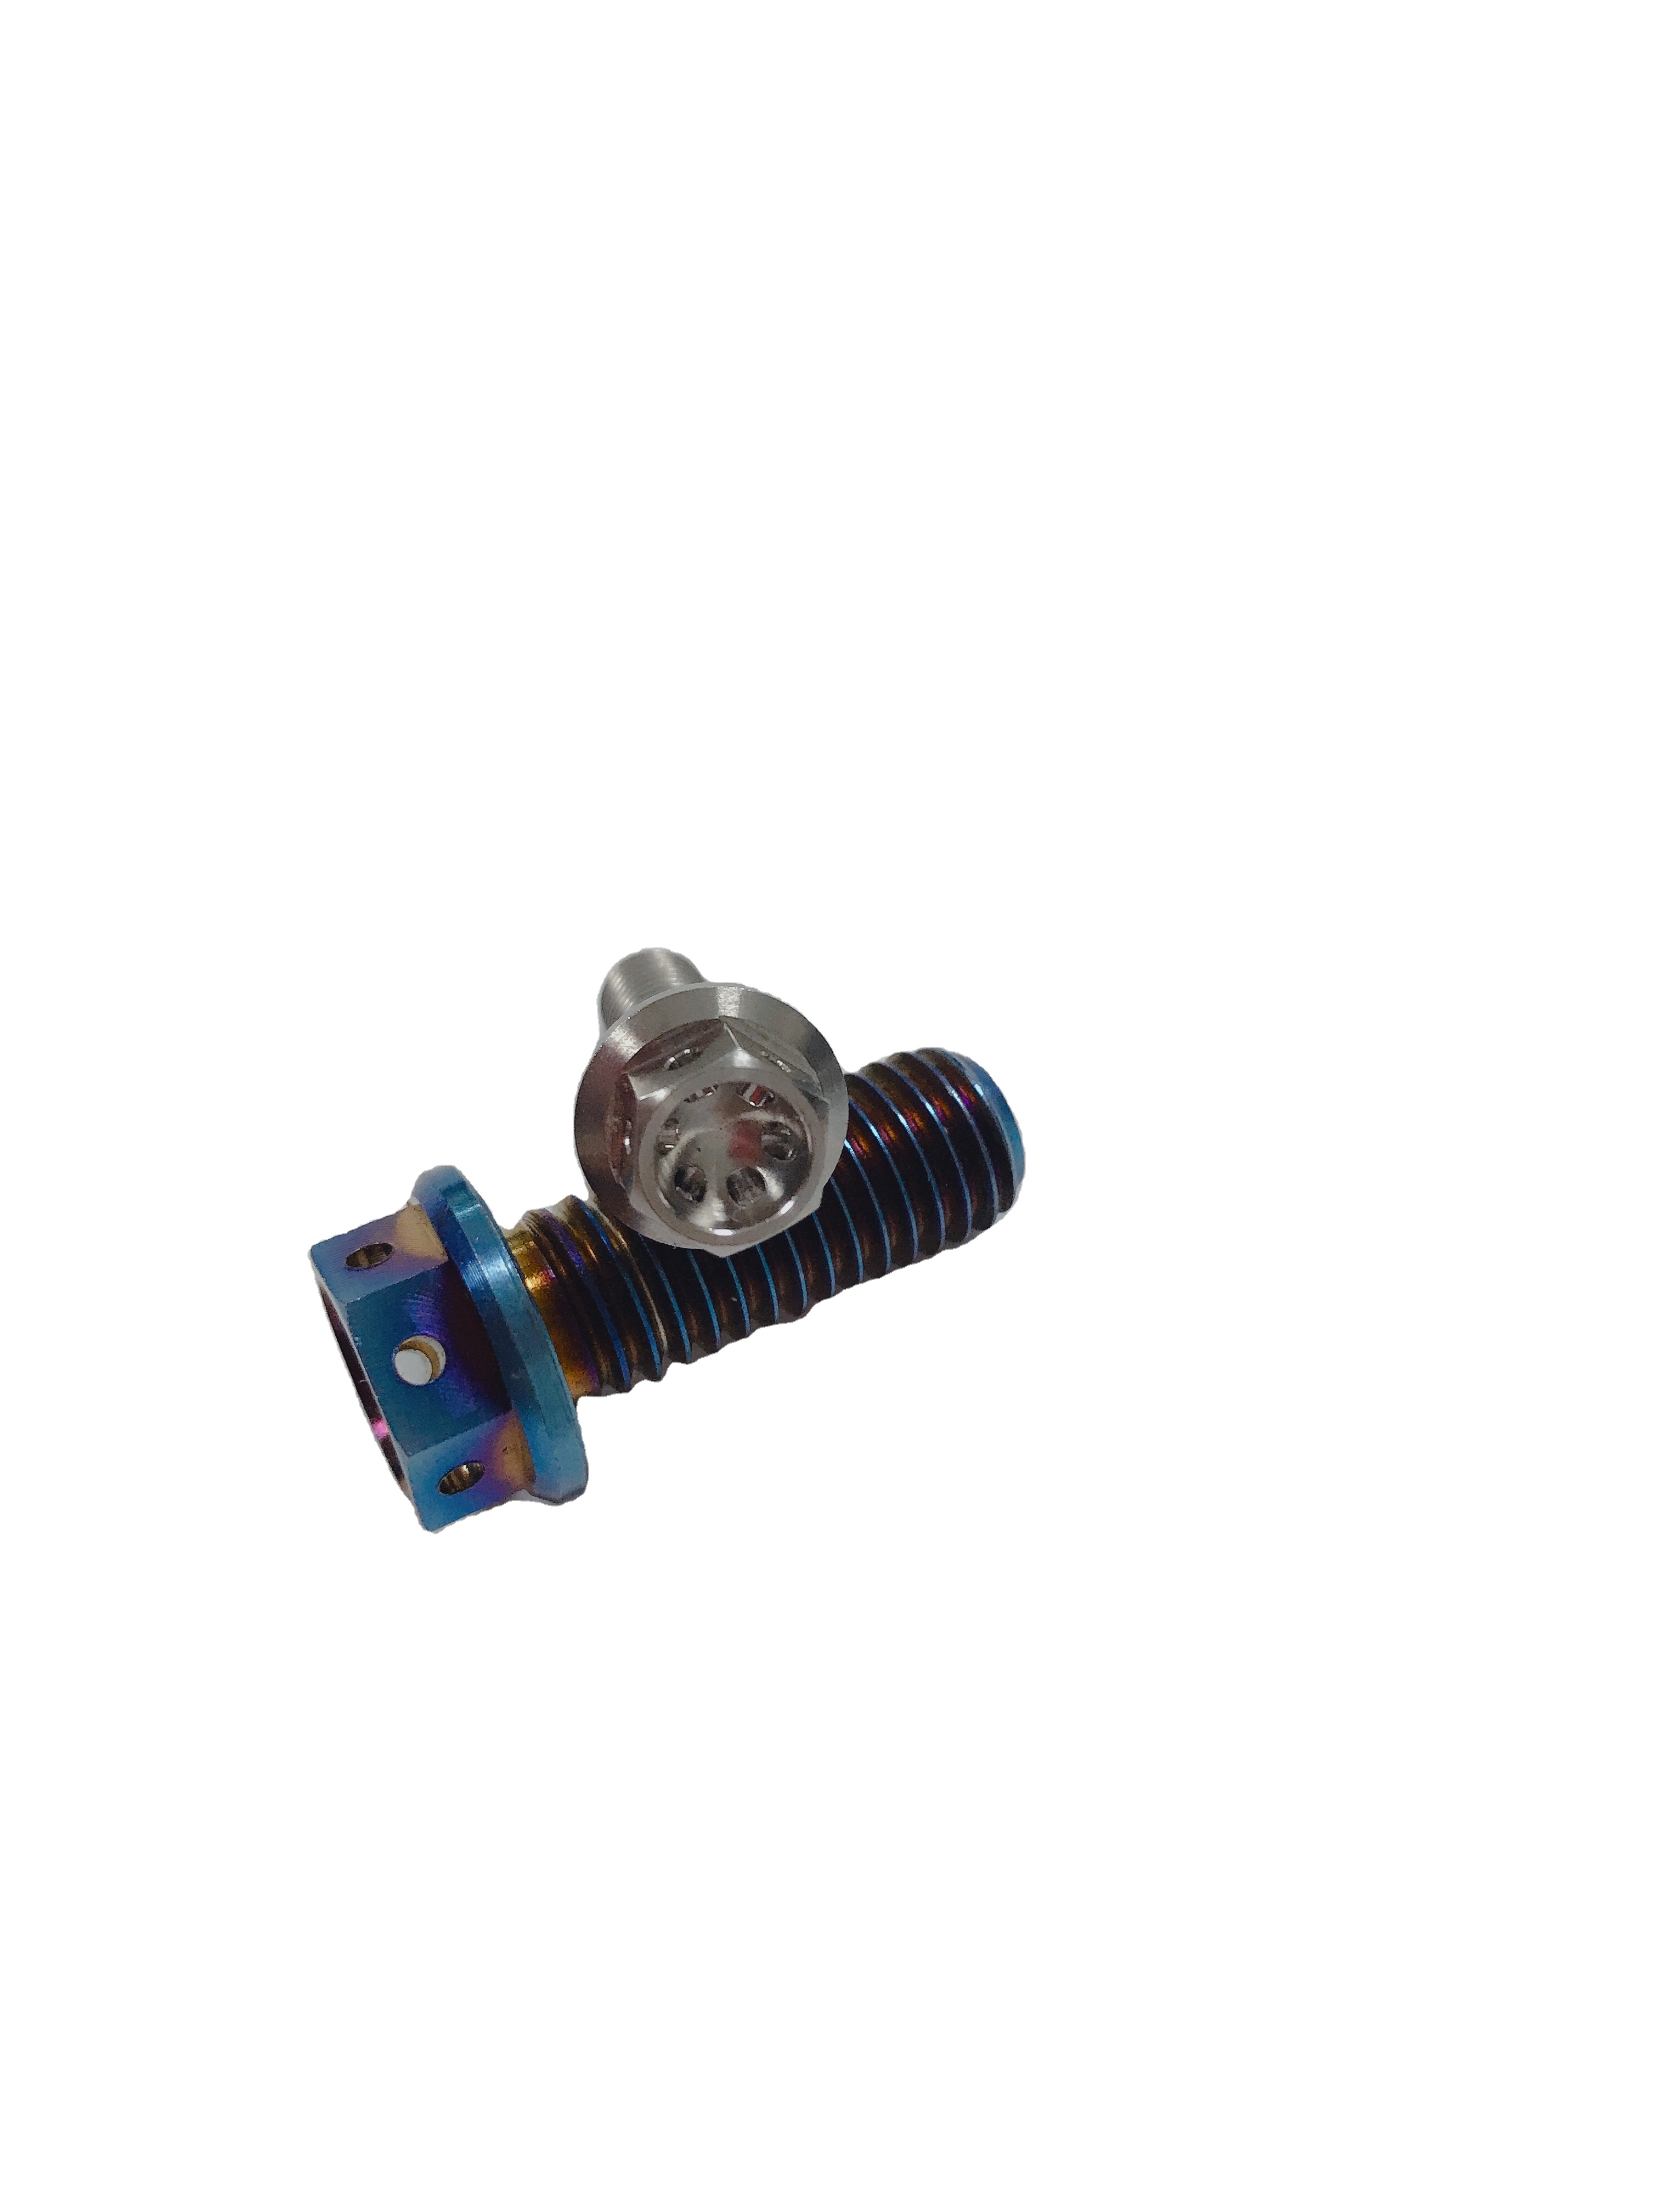
M6x30 M6x35 GR5 Grade Hex Head Titanium Wheel Flange Bolts
1. Technical White-Paper: Advanced Valvetrain Dynamics & Titanium Metallurgy for the London Motorsport Ecosystem
In high-rpm internal combustion engines—ranging from British Touring Car Championship (BTCC) engines to bespoke historic V12 and turbo-charged drag racing powerplants engineered across Greater London—the valvetrain represents the primary mechanical bottleneck limiting engine speed and power output. The dynamic inertia of the valve spring retainer directly influences valve float, harmonic resonance, and parasitic frictional losses. As London engine tuners and performance engineering firms located throughout Silverstone Valley and Kent push rev limits beyond 11,000 RPM, replacing conventional chromoly or tool-steel retainers with CE Certified Ti-6Al-4V Grade 5 Titanium Valve Retainers becomes a fundamental engineering imperative.
1.1 Metallurgical Properties & Material Comparison Matrix
Our titanium racing valve retainers are manufactured exclusively from virgin Grade 5 Ti-6Al-4V (UNS R56400) titanium alloy, sourced from verified billet in Baoji ("China Titanium Valley"). Below is a comprehensive engineering comparison against alternative valvetrain materials used in UK engine workshops:
| Material Specification | Ti-6Al-4V Gr5 Titanium | Ti-6Al-4V ELI (Gr23) | 4340 Chromoly Steel | 7075-T6 Aluminum |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 | 4.43 | 7.85 | 2.81 |
| Tensile Strength (MPa) | ≥ 895 - 1050 | ≥ 860 | ≥ 1100 | ≥ 570 |
| Yield Strength (MPa) | ≥ 828 | ≥ 795 | ≥ 980 | ≥ 505 |
| Fatigue Limit ($10^7$ Cycles) | 510 MPa | 490 MPa | 550 MPa | 160 MPa (Poor) |
| Operating Temp Limit | 400°C | 400°C | 500°C | 150°C (Unsuitable) |
| Corrosion Resistance | Immune to Fuel/Oil Acids | Immune | Requires Plating | Moderate Oxidation |
1.2 Precision CNC Manufacturing & Surface Engineering
Achieving the required structural fatigue threshold demands precision multi-axis Swiss CNC turning and 5-axis milling. Vunza Titanium Industry Co., Ltd. operates 34 state-of-the-art CNC machining centers equipped with live tooling, enabling one-setup machining of valve lock angles (7°, 10°, and Super 7°) to a geometric tolerance of ±0.005mm. This eliminates stress concentrations caused by micro-chattering or angular misalignment, ensuring 100% surface contact with valve keepers/locks.
To eliminate galling between the valve spring wire (typically chrome silicon or vanadium spring steel) and the titanium retainer step, our retainers undergo advanced surface treatments:
- Micro-Polishing & Shot Peening: Imparts compressive residual stress on the outer radius, elevating fatigue resistance by 22%.
- Physical Vapor Deposition (PVD) Titanium Nitride (TiN) / DLC Coating: Creates an ultra-hard surface layer (2500–3000 HV) with a coefficient of friction below 0.15, preventing spring fretting under high harmonic vibration.
- Anodized Finish Color Coding: Allows immediate visual inspection during engine assembly in fast-paced pit garages at Brands Hatch or Donington Park.
2. Localized Application Scenarios in London & the Broader UK Motorsport Industry
London serves as a global administrative, commercial, and engineering hub for high-performance automotive development. With major logistics networks connecting Heathrow Cargo Terminal and the Port of London directly to high-density tuning districts in Kent, Essex, Oxfordshire, and the Northamptonshire Motorsport Valley, our CE Certified Titanium Valve Retainers are deployed across diverse local applications:
BTCC & GT3 Circuit Racing Engines
High-revving 2.0L turbocharged inline-4 and naturally aspirated V8 engines require durable valvetrain hardware capable of sustaining continuous 9,500+ RPM over 45-minute sprint races. Our Ti-6Al-4V retainers prevent spring surge and keeper pull-through under sudden downshift over-revs.
London Historic & Classic Motorsport
Restoration workshops in Greater London servicing classic Jaguar XK, Aston Martin, and vintage Ferrari V12 race engines rely on custom-machined titanium retainers to protect irreplaceable original camshafts while safely increasing rev limits for Goodwood Revival events.
Drag Racing & High-BMEP Street Performance
Engineered for 1,500+ HP extreme boost applications tested at UK drag strips like Santa Pod Raceway. Grade 5 titanium retainers resist structural deformation under immense cylinder backpressures and aggressive valve opening velocities driven by high-lift cams.
3. Localized Market & Regulatory Development Trends in London
The UK automotive aftermarket and racing component sectors in Greater London are undergoing significant transformations governed by regulatory shifts, sustainability metrics, and digital supply chain integration:
3.1 CE & UKCA Marking Compliance Post-Brexit
Following updates to UK product safety compliance regulations, race parts imported into London and sold across European markets require verified quality management systems. Our valve retainers feature full CE Certification under Directive 2006/42/EC and ISO 9001:2015 certification, satisfying rigorous UKCA/CE harmonized standards. Each export shipment to London includes comprehensive EN 10204 3.1 Material Test Reports (MTRs) detailing chemical heat numbers and tensile test metrics.
3.2 ULEZ, Hybridization & Engine Downsizing Effects
With London’s Ultra Low Emission Zone (ULEZ) driving street tuning toward smaller-displacement, ultra-high-efficiency turbocharged engines, engine builders are achieving higher power-per-liter ratios than ever before. Lightweight titanium components are critical to reducing thermal losses and internal parasitic drag, directly aligning with modern low-emission, high-output powertrain designs.
4. Enterprise Manufacturing Superiority: Vunza Titanium Industry Co., Ltd.
Located in Gaoya Village Industrial Zone, Baoji, Shaanxi, China—adjacent to the Baoti Group Industrial Park—Vunza Titanium Industry Co., Ltd. operates at the core of world-class titanium refining and machining infrastructure. Established in 2008, our facility combines raw sponge processing oversight with advanced multi-axis CNC manufacturing.
In-House R&D & 13+ Years Expert Workforce
Over 50% of our production staff possess more than 13 years of dedicated hands-on titanium machining experience. Our engineering team conducts Finite Element Analysis (FEA) to optimize retainer wall thickness and stress distribution before turning a single piece of billet.
100% Raw Material & Part Traceability
From initial titanium sponge vacuum arc remelting (VAR) to finished optical inspection, every batch is recorded. We utilize Zeiss Coordinate Measuring Machines (CMM) and optical profilometers to guarantee concentricity within 0.003mm.
Direct Express Logistics to London Hubs
We provide rapid air freight service directly to London Heathrow (LHR) and sea container transport to the Port of London / Tilbury, complete with customs clearance paperwork, duty prepaid options, and dedicated local B2B support.
5. London Procurement FAQ: Sourcing Titanium Valve Retainers
What valve lock angles and spring dimensions do you stock or manufacture for UK engines?
How do CE Certification and ISO 9001 compliance benefit London importers?
What is the lead time for express air shipments to London workshops?
Will Grade 5 titanium retainers gall or wear against hardened steel valve springs?
What is the Minimum Order Quantity (MOQ) for custom racing components?
Request an Immediate Engineering Review & Direct B2B Quote
Partner with China's leading titanium CNC manufacturer. Upload your 2D/3D drawings, target quantities, and custom coating requirements for instant technical feedback from our engineering team in Baoji.
Get a Quote