Caliper Mount
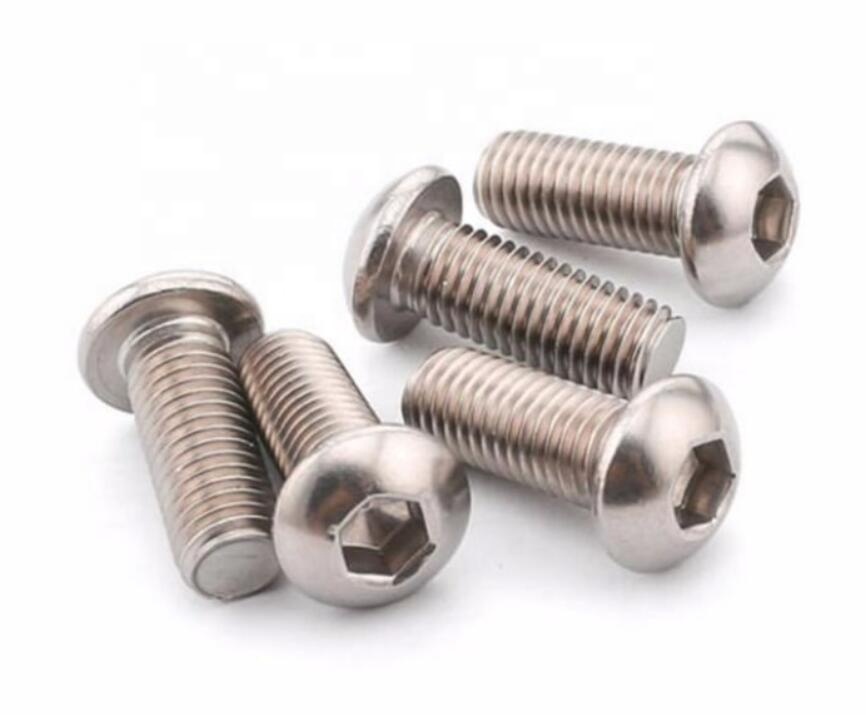
Precision-milled from certified aerospace Ti6Al4V Grade 5 alloy stock. Holding micron-level concentricity up to ±0.005 mm to satisfy Düsseldorf's rigorous engineering demands.
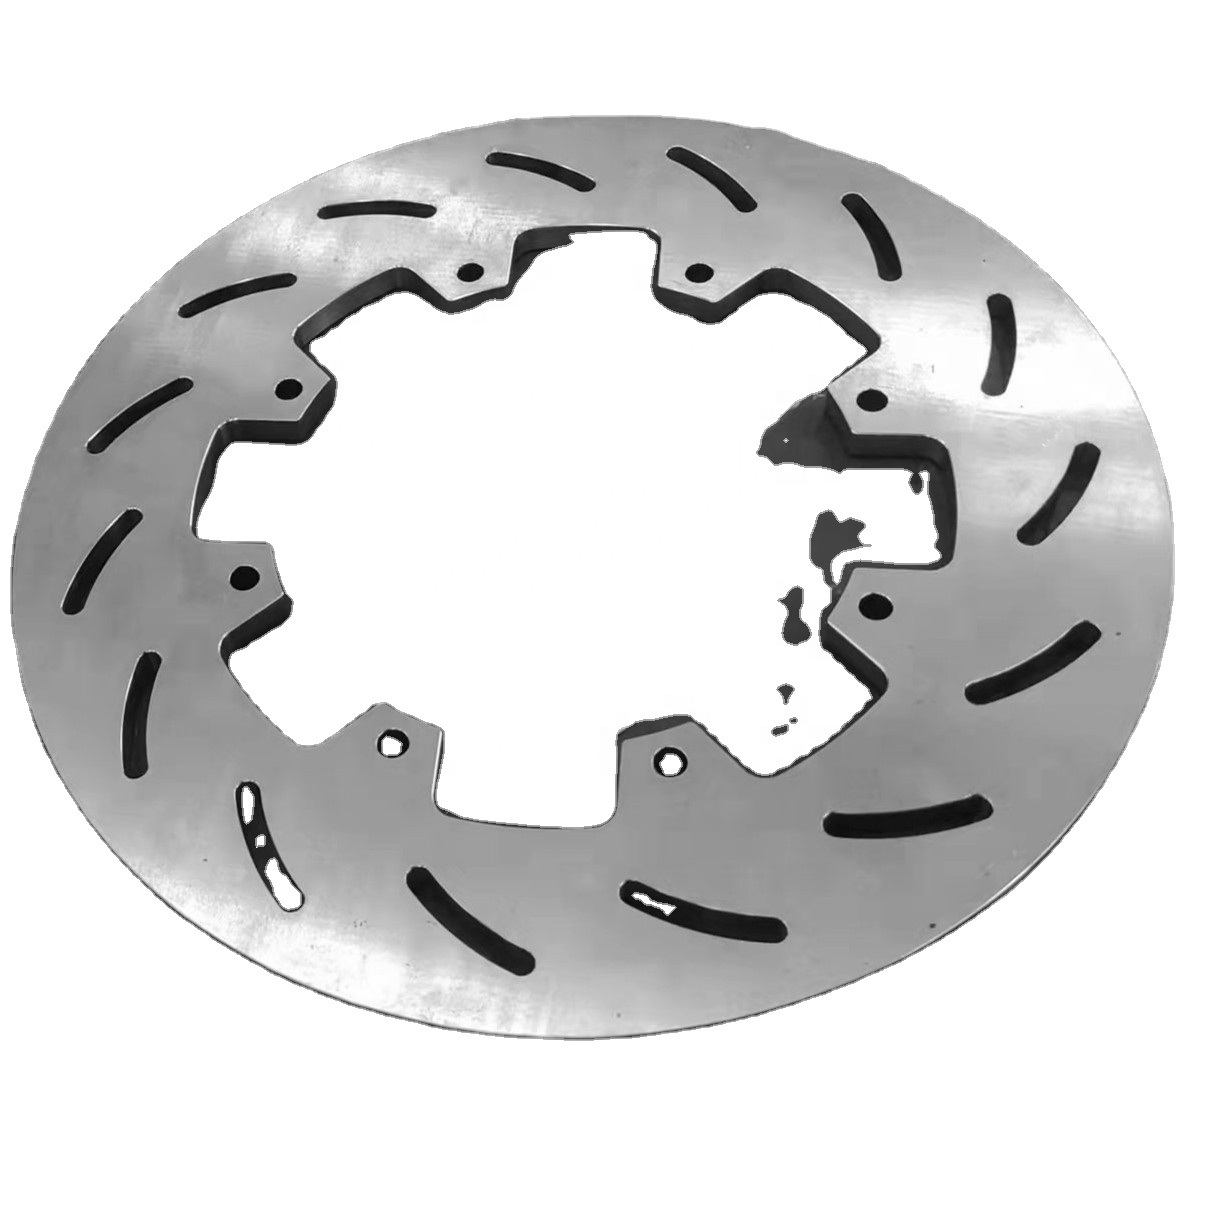
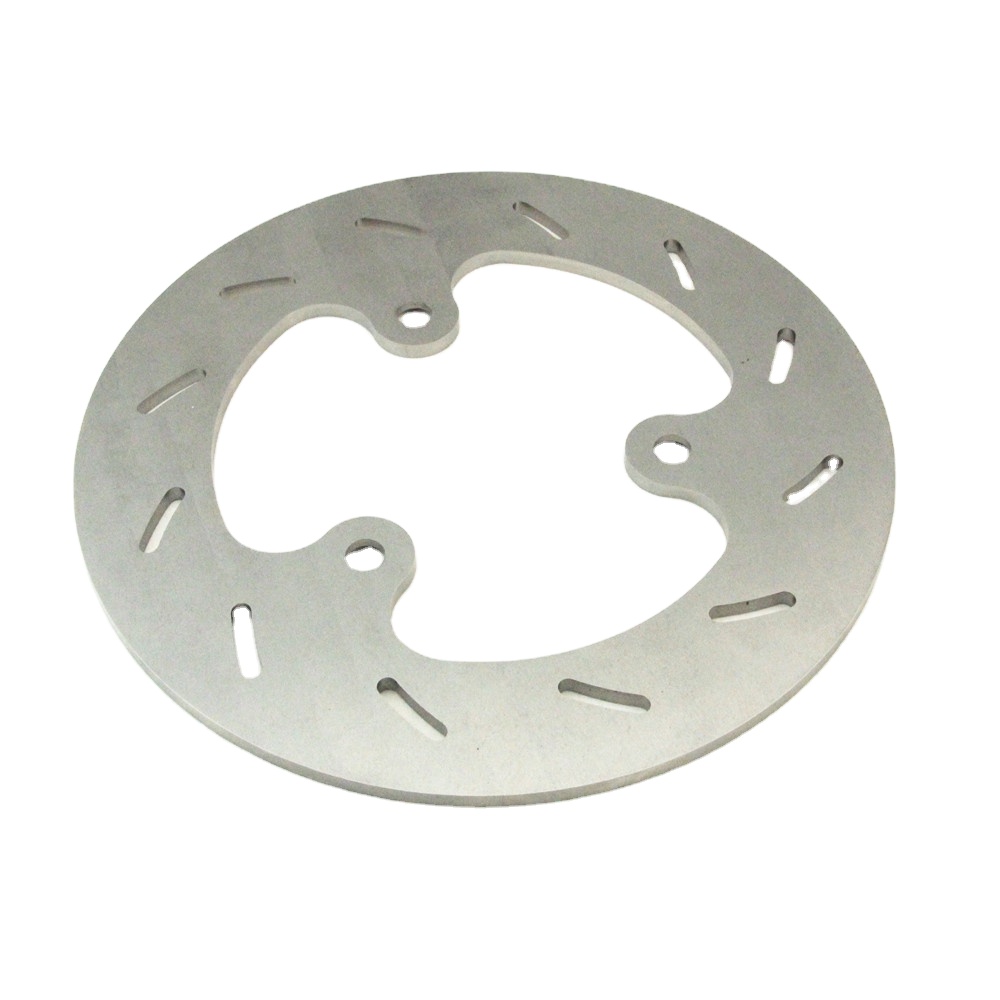
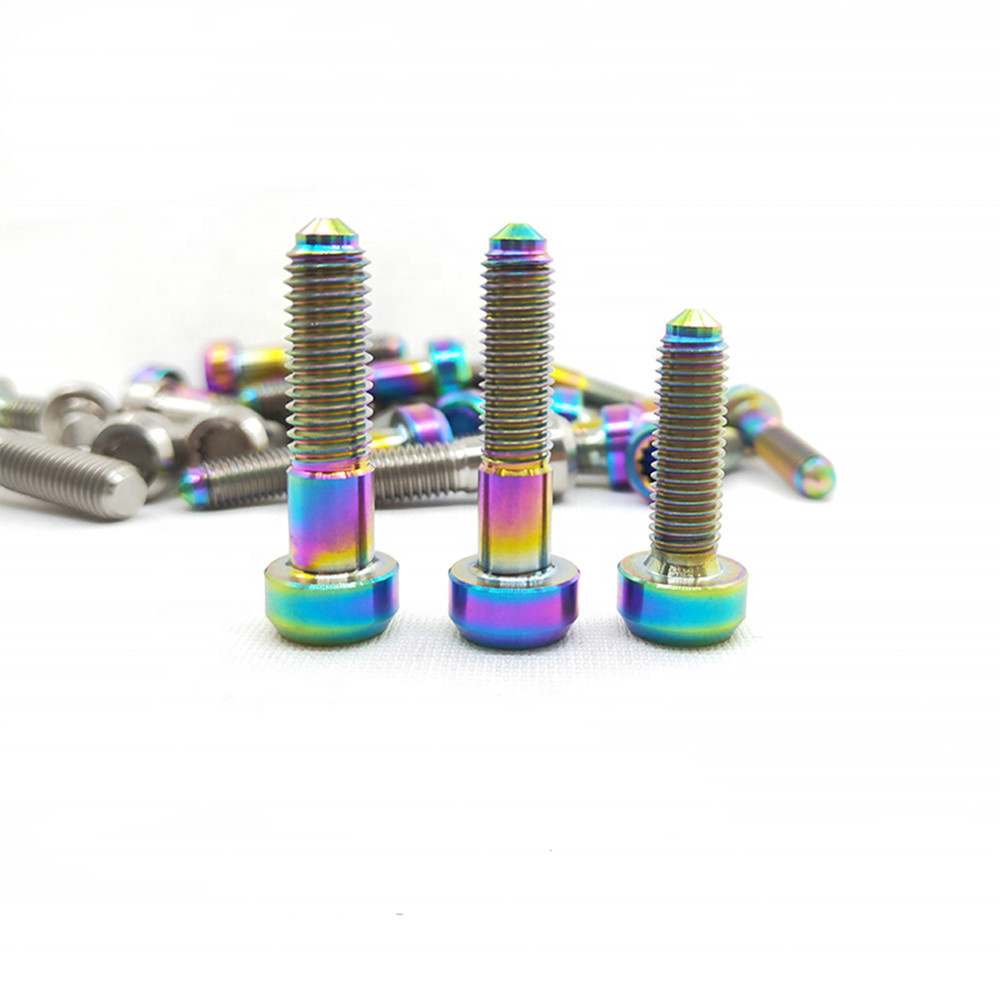
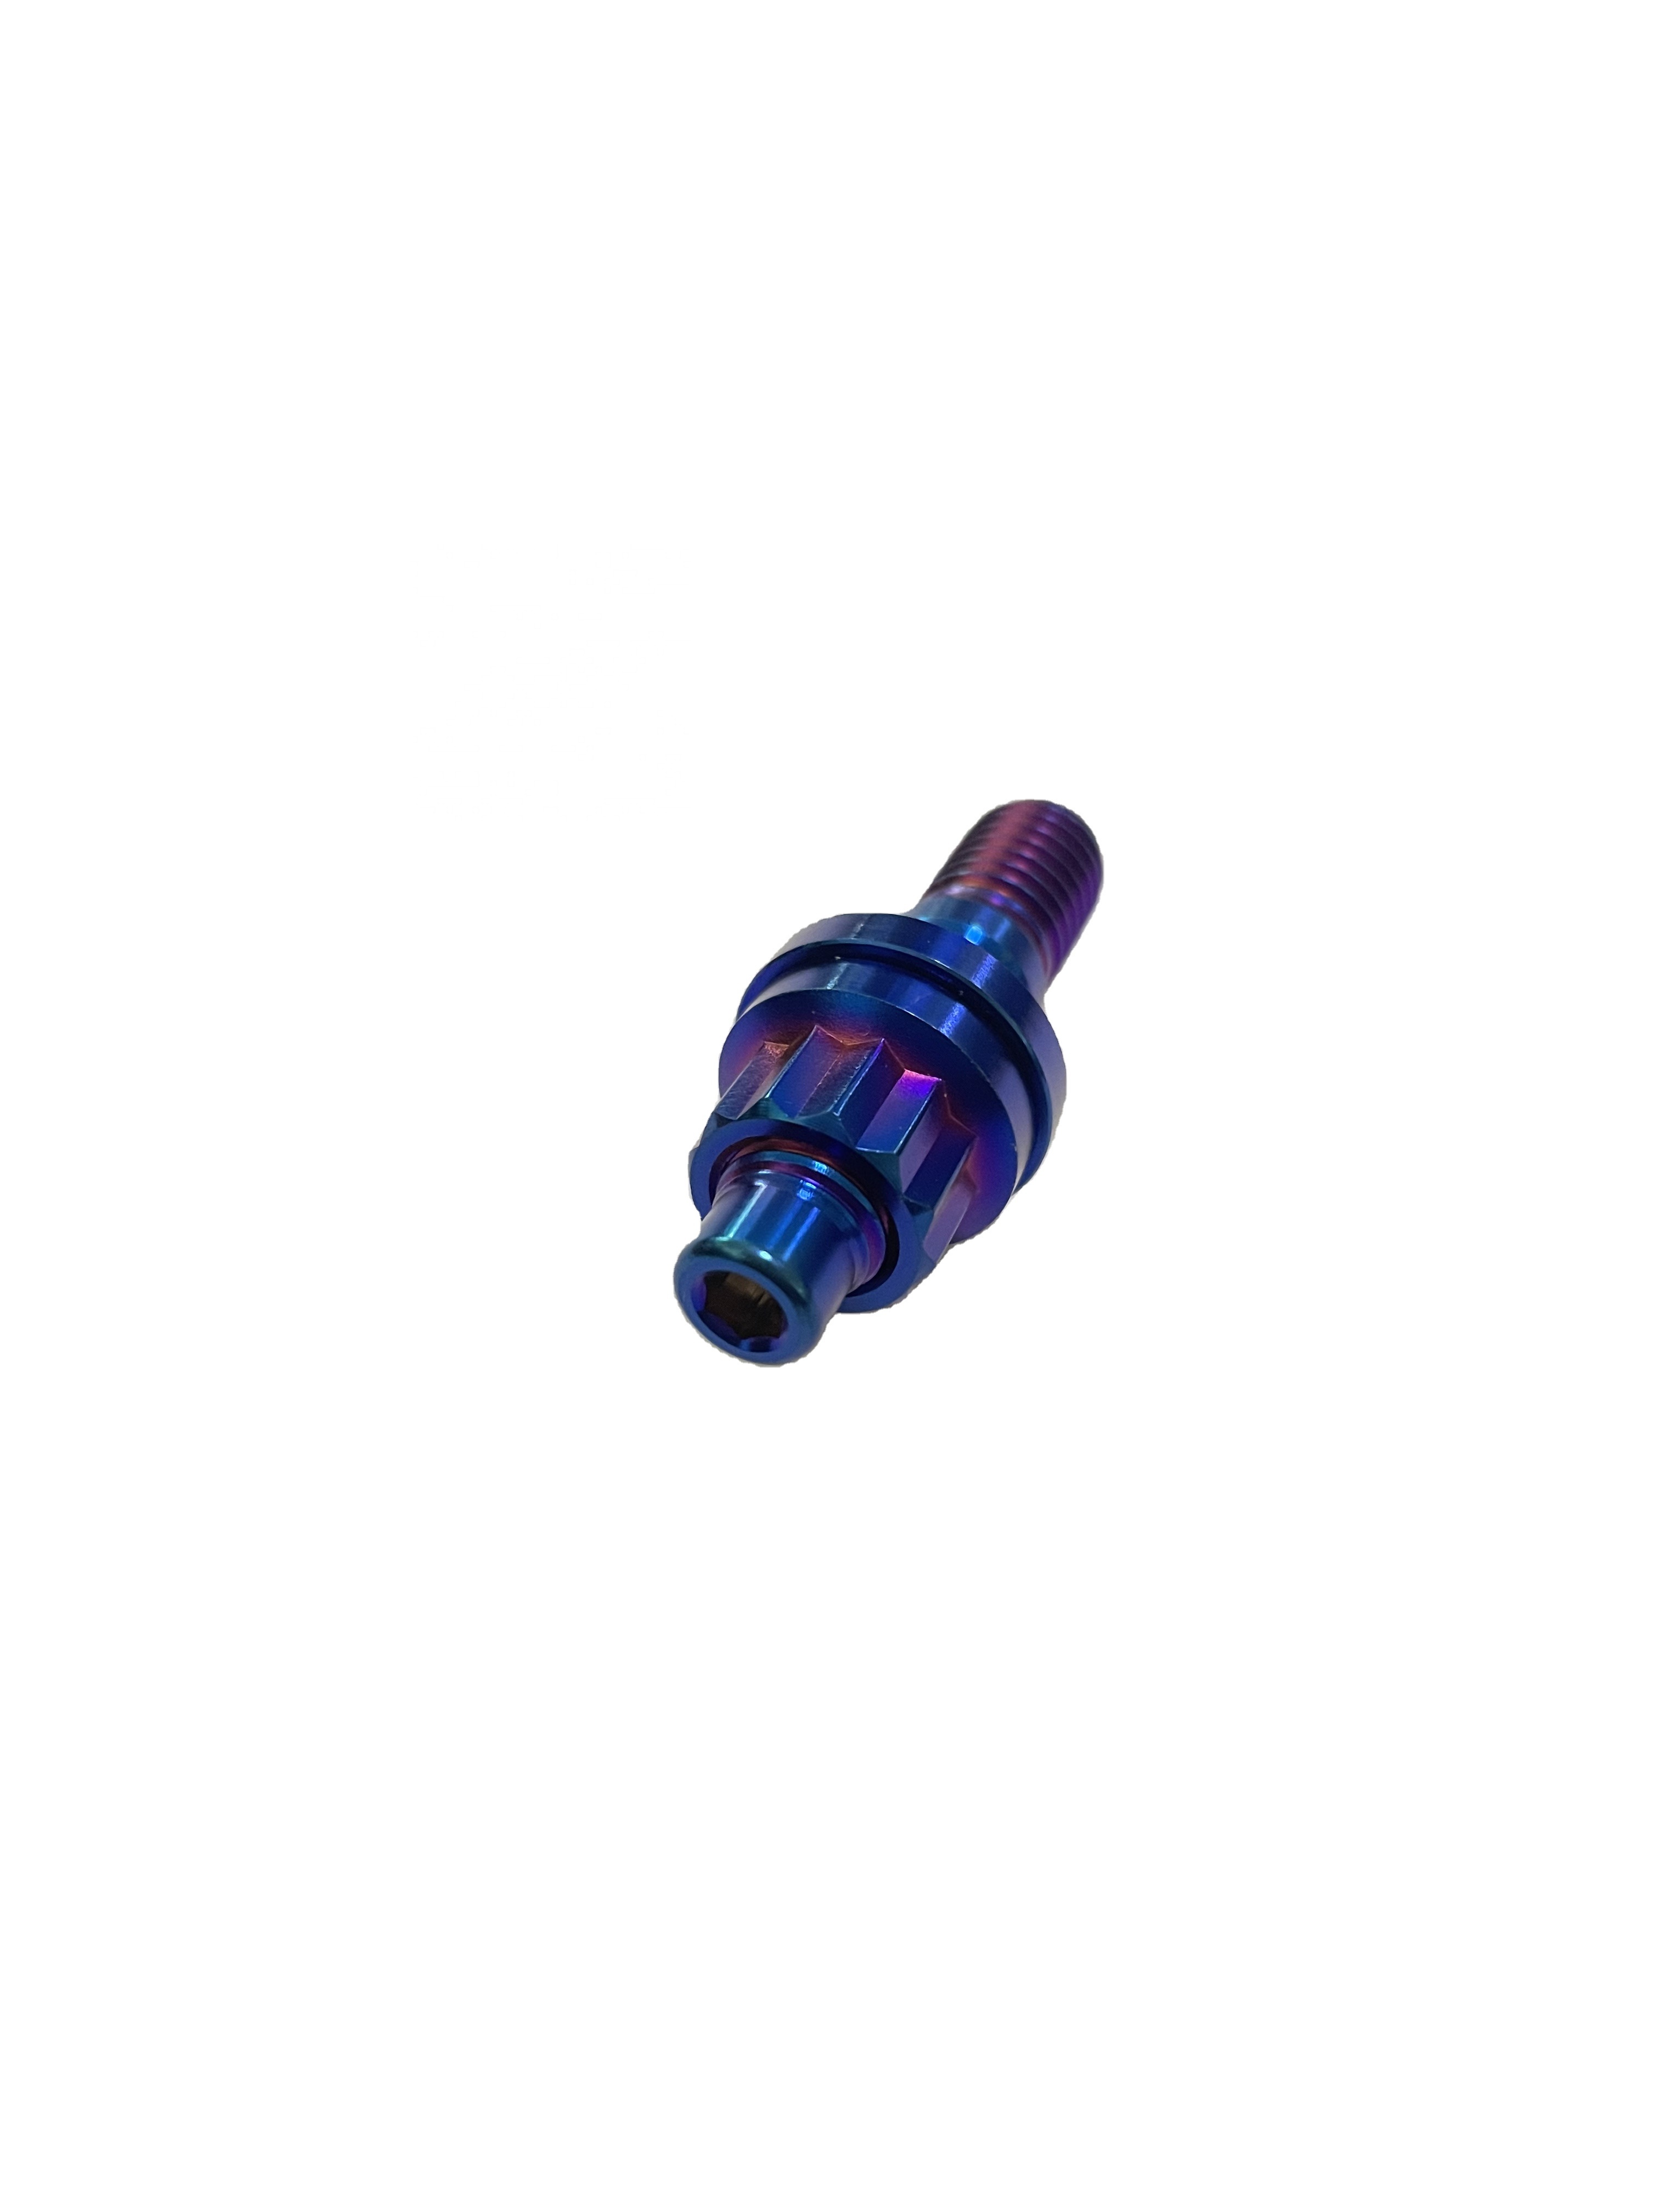
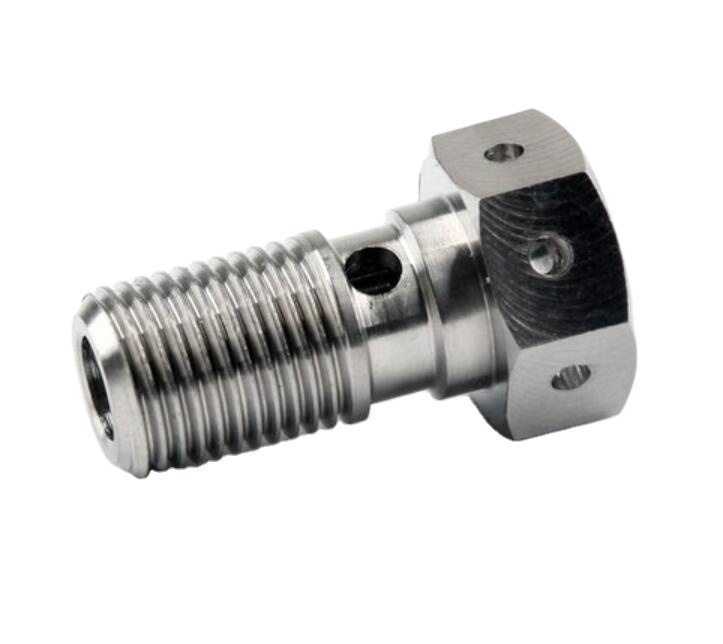
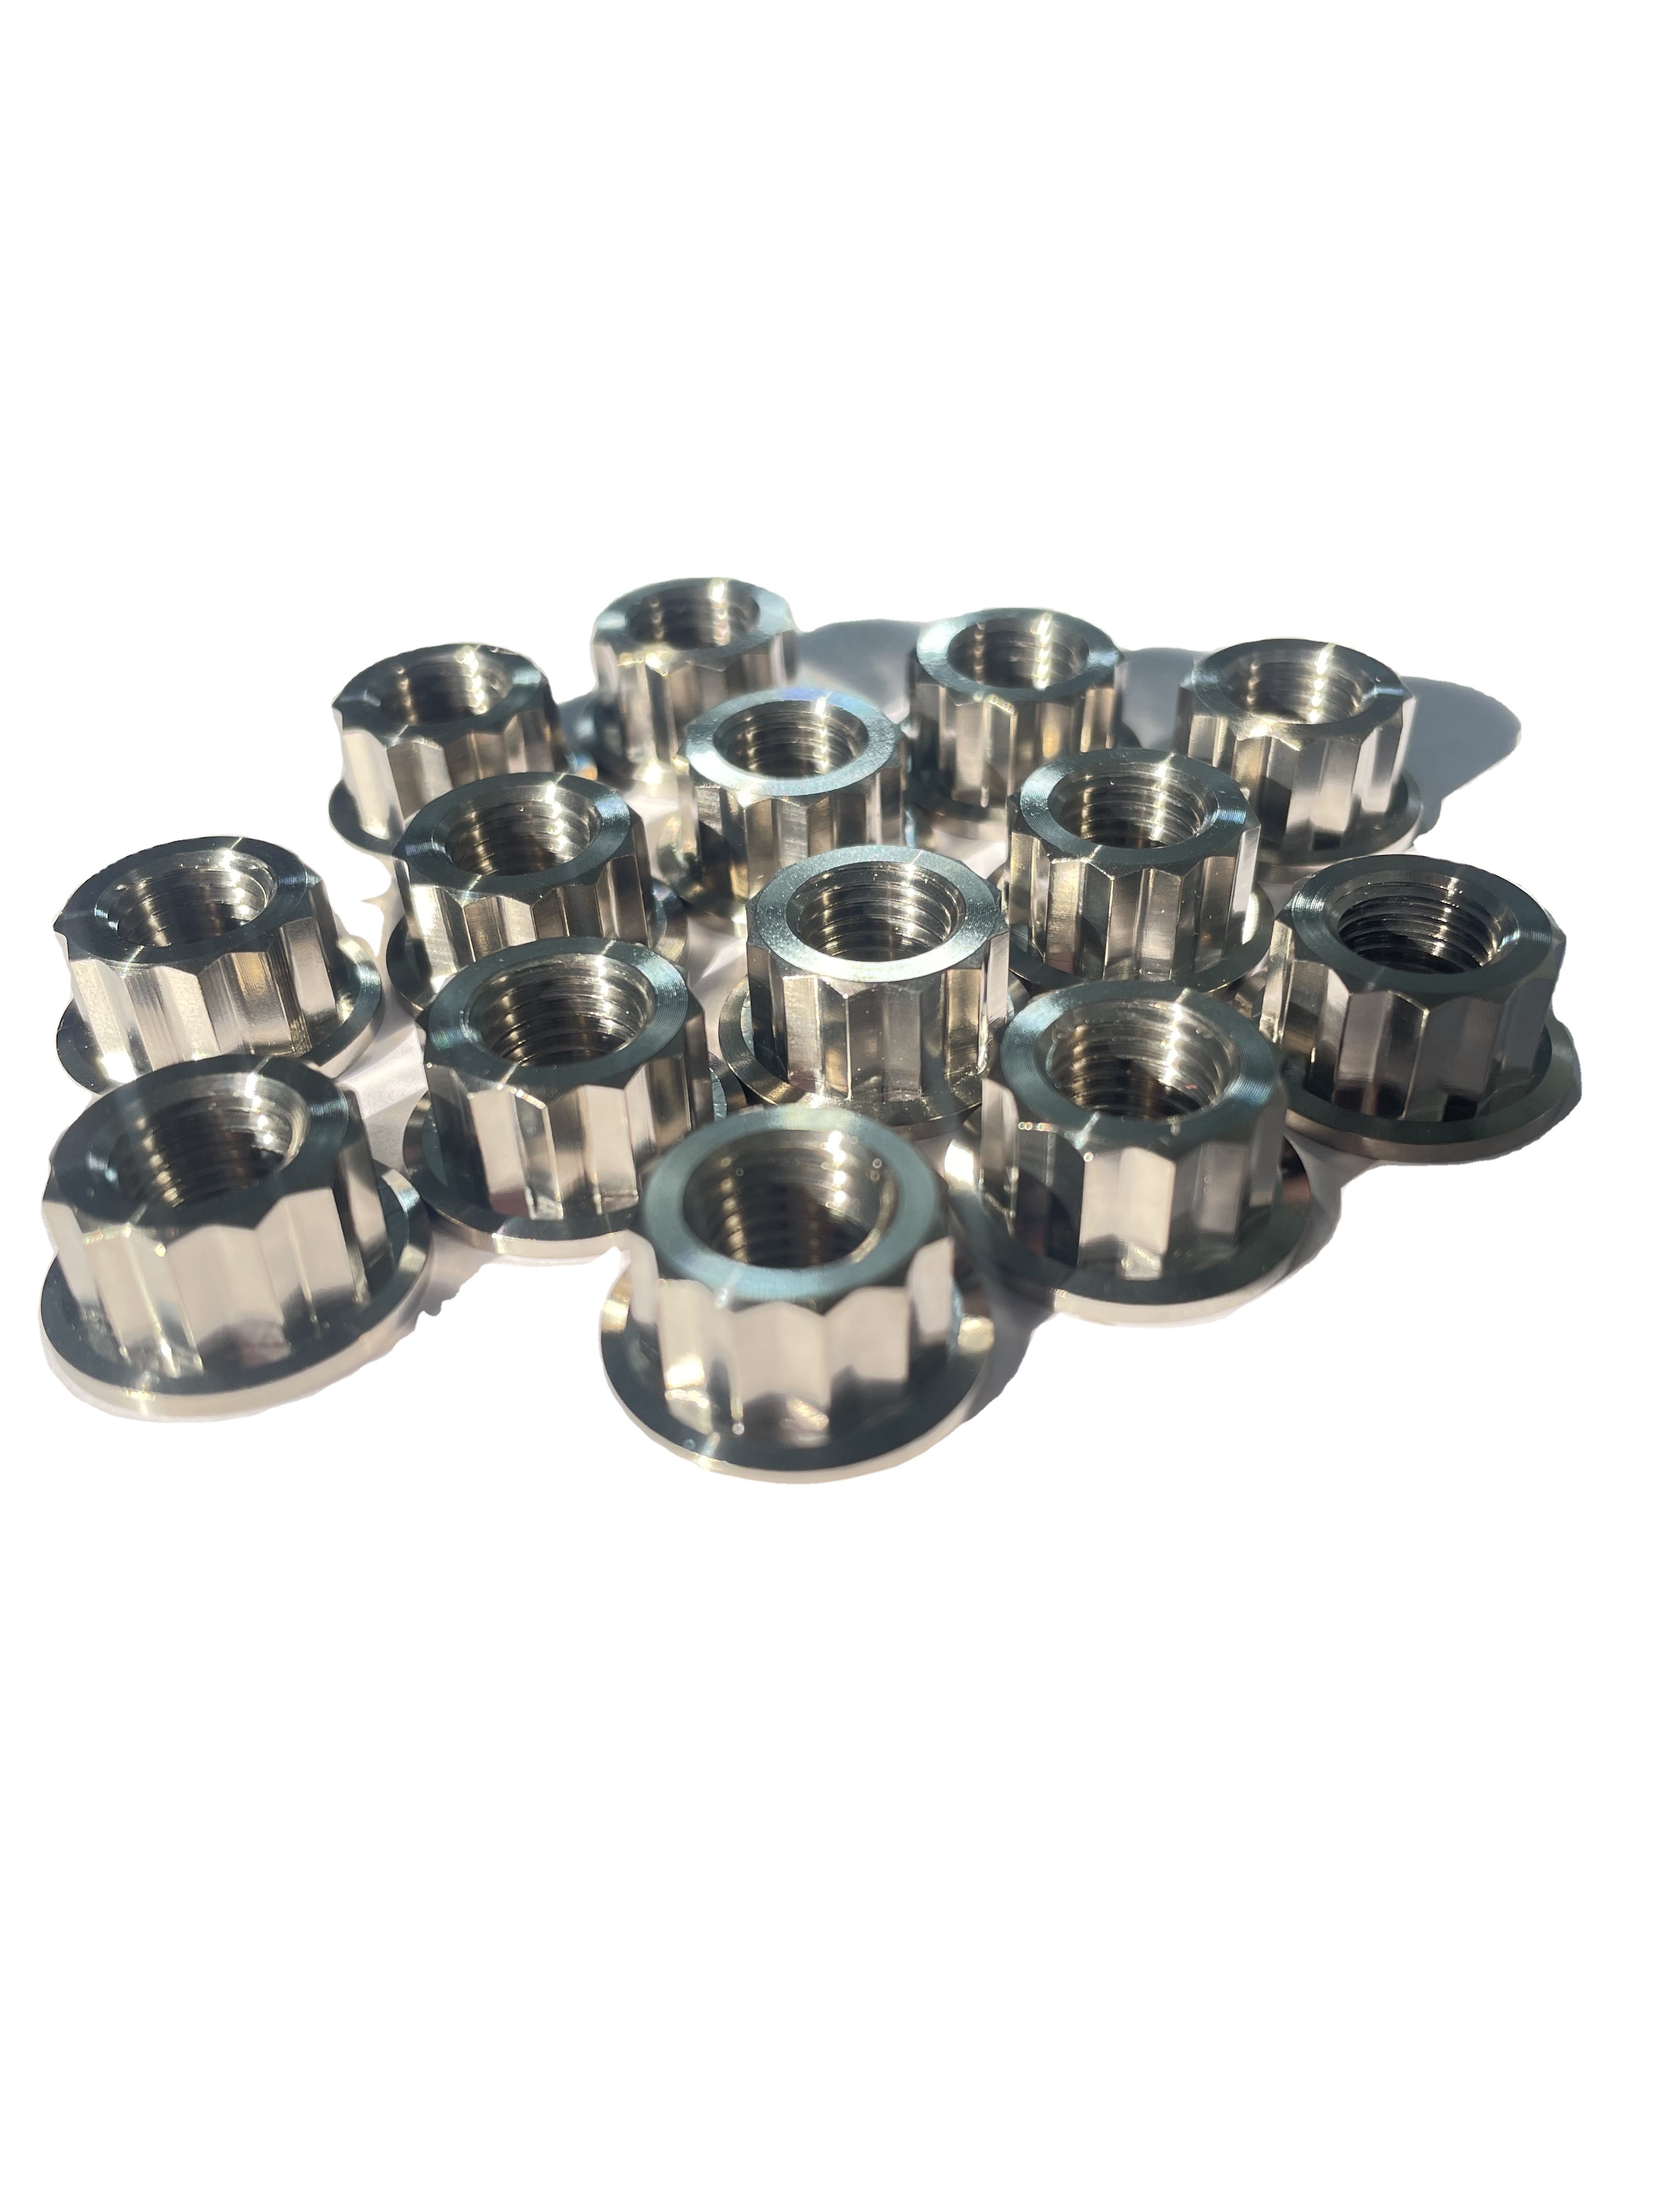
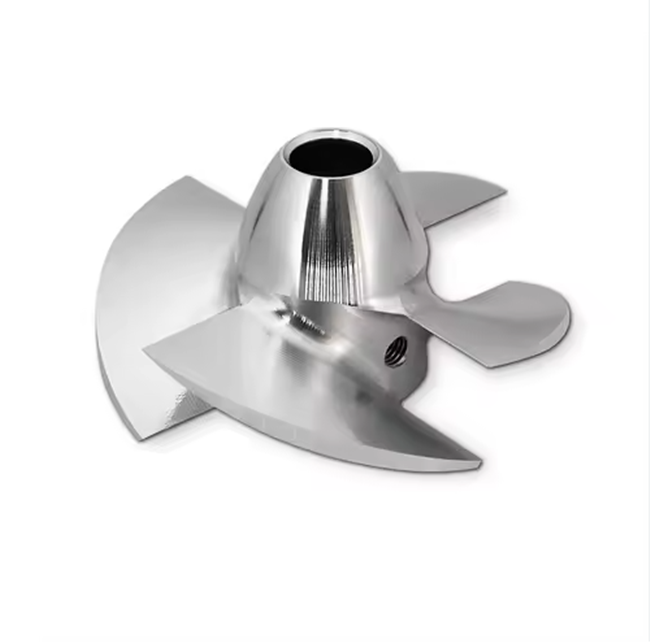
In internal combustion powertrains, high-performance engines, and reciprocating compression units, valve hardware operates under extreme cyclic mechanical stress and aggressive thermal environments. As the engine cycles past 8,500 RPM, standard martensitic or austenitic stainless steel valve retainers, spring keepers (cotters), and spring bases impose severe inertial mass penalties on the valvetrain architecture.
By migrating from steel to precision-machined Ti6Al4V (Grade 5, UNS R56400), engine design engineers achieve up to a 42% to 45% reduction in reciprocating valvetrain mass. This weight optimization is directly proportional to decreasing valve float, lowering parasitic friction, and enabling sharper camshaft profile lift rates without risking valvetrain bounce or catastrophic harmonic breakdown.
Unlike conventional subtractive mass-production shops, our production facility in Baoji—known globally as China's Titanium Valley—utilizes aerospace-grade vacuum arc remelted (VAR) titanium bars. This ensures a clean metallurgical microstructure free of interstitial oxygen or hydrogen inclusions, maintaining high cyclic fatigue limits required by the Nürburgring and regional German motorsport developers.
Düsseldorf, as the capital of North Rhine-Westphalia (NRW) and the heart of the industrial Rhine-Ruhr metropolitan region, commands an advanced manufacturing ecosystem. The demand for lightweight titanium hardware spans far beyond niche track builds into high-efficiency industrial machinery, specialized automotive Tier-1 engineering, and corrosive chemical flow management.
Düsseldorf's tuning ateliers and endurance racing teams rely heavily on custom 10° and 7° titanium valve retainers, lightweight spring bases, and exhaust studs. These components endure prolonged thermal cycles at the nearby Nordschleife endurance tracks without yielding or galling.
With Chempark hubs in close proximity to Düsseldorf (Leverkusen, Krefeld, Dormagen), chemical engineers specify titanium Grade 2 and Grade 5 flow-control valve components for high-pressure autoclaves, cryogenic valving, and acid handling networks that corrode duplex steels.
NRW-based precision aerospace manufacturers and hydrogen powertrain innovators procure custom 5-axis milled titanium impeller hardware, metering valves, and structural chassis fasteners that demand full EN 10204 3.1 chemical and mechanical traceability.
Selecting appropriate alloys for valvetrain hardware and critical fastener assemblies requires evaluating yield strength, operating temperature thresholds, and weight trade-offs against traditional steel and nickel-base superalloys:
| Material Specification | Density (g/cm³) | Tensile Strength (MPa) | Max Working Temp (°C) | Fatigue Endurance Limit | Ideal Application Scenario |
|---|---|---|---|---|---|
| Ti6Al4V (Grade 5 / TC4) | 4.43 | 950 – 1050 | 400°C | 510 MPa @ 10^7 cycles | High-RPM Valve Retainers, Caliper Mounts, Head Studs |
| Ti6Al4V ELI (Grade 23) | 4.43 | 860 – 920 | 380°C | 490 MPa @ 10^7 cycles | High-Ductility Valvetrain Keepers & Medical Grade Hardware |
| 4140 Chromoly Steel | 7.85 | 850 – 1000 | 420°C | 420 MPa @ 10^7 cycles | Standard Production Retainers (High Inertia Mass Penalty) |
| 7075-T6 Billet Aluminum | 2.81 | 570 | 120°C | 160 MPa (Poor Cyclic Life) | Low-Cost Budget Builds (Prone to Galling & Fatigue Failure) |
| Inconel 718 (Nickel Superalloy) | 8.19 | 1240 – 1400 | 700°C | 600 MPa @ 10^7 cycles | Turbo Exhaust Valves (Significant Mass Penalty for Retainers) |
*Data compiled from ASTM B348, ISO 5832-3, and certified factory laboratory spectrometer tests performed under ISO 9001 guidelines.
As German industrial manufacturers navigate energy transformation benchmarks and carbon-neutral production policies, several pivotal trends influence the procurement of titanium valve hardware across Düsseldorf and the Ruhr Valley:
1. Powertrain Downsizing and High-Boost Pressures: German OEMs and aftermarket tuning engineering firms are optimizing smaller internal combustion configurations utilizing high-pressure twin-scroll turbocharging. These engines experience increased valve seat temperatures and higher seating velocities, rendering conventional aluminum and steel valve spring retainers obsolete due to thermal fatigue and galling.
2. Adoption of Advanced PVD and DLC Friction Modifiers: German procurement specialists consistently demand modern surface modification technologies. We supply our Grade 5 titanium retainers and studs treated with Physical Vapor Deposition (PVD), Nitride passivated layers, or Diamond-Like Carbon (DLC) coatings. This reduces the friction coefficient down to μ ≤ 0.12, safeguarding titanium valve cotters from galling against hardened steel valve stems.
3. Resilient Sourcing Direct from Titanium Valley (Baoji): European procurement hubs are actively diversifying supply channels to avoid high intermediate markups. By establishing direct contracts with Baoji manufacturers, Düsseldorf enterprises secure factory-direct pricing, mill certificate transparency, and guaranteed lot-to-lot dimensional consistency.
Founded in 2008 and positioned adjacent to the Baoti Group Industrial Park in Baoji, China, Vunza Titanium Industry Co., Ltd. integrates metallurgy, CAD/CAM prototyping, mass CNC production, and global logistics under one rigorous quality management umbrella.
Equipped with simultaneous 3, 4, and 5-axis CNC machining stations, turning lathes, and automated thread-rolling machines capable of maintaining tolerances within 0.005 mm across large production runs.
Every batch begins with raw titanium sponge certification, followed by ultrasonic flaw detection, CMM dimensional checks, thread pitch projection, and optical surface roughness evaluation.
Over 50% of our frontline technicians boast more than 13 years of titanium-specific turning and milling expertise. Our bilingual engineering desk delivers DFM feedback within 9 hours on business days.
Direct answers addressing technical compliance, logistics, customs clearance, and quality verification for buyers across Germany:
Accelerate your project with aerospace-certified Ti6Al4V Grade 5 valve hardware and custom CNC components. Upload your CAD drawings or technical datasheets to receive comprehensive DFM analysis, volume quotation, and delivery lead times within 9 business hours.