Anodized Gr5
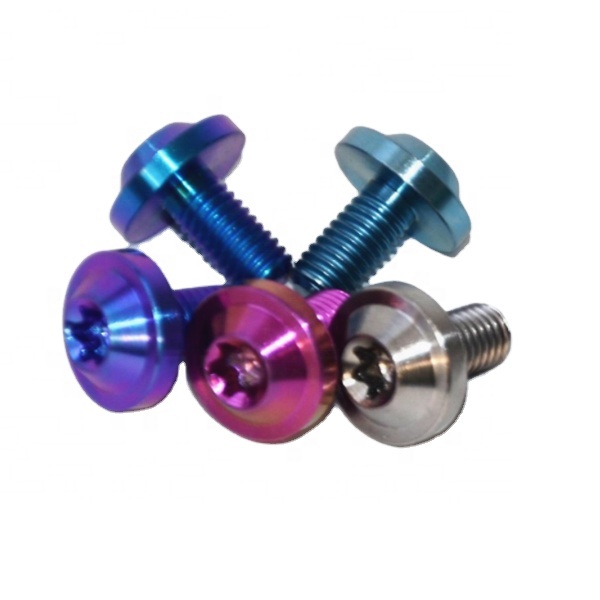
Constructed from certified aerospace-grade titanium alloy bar stock, each piece undergoes precision multi-axis CNC profiling, hot head forging, and cold rolled threading for zero-compromise fatigue resistance.
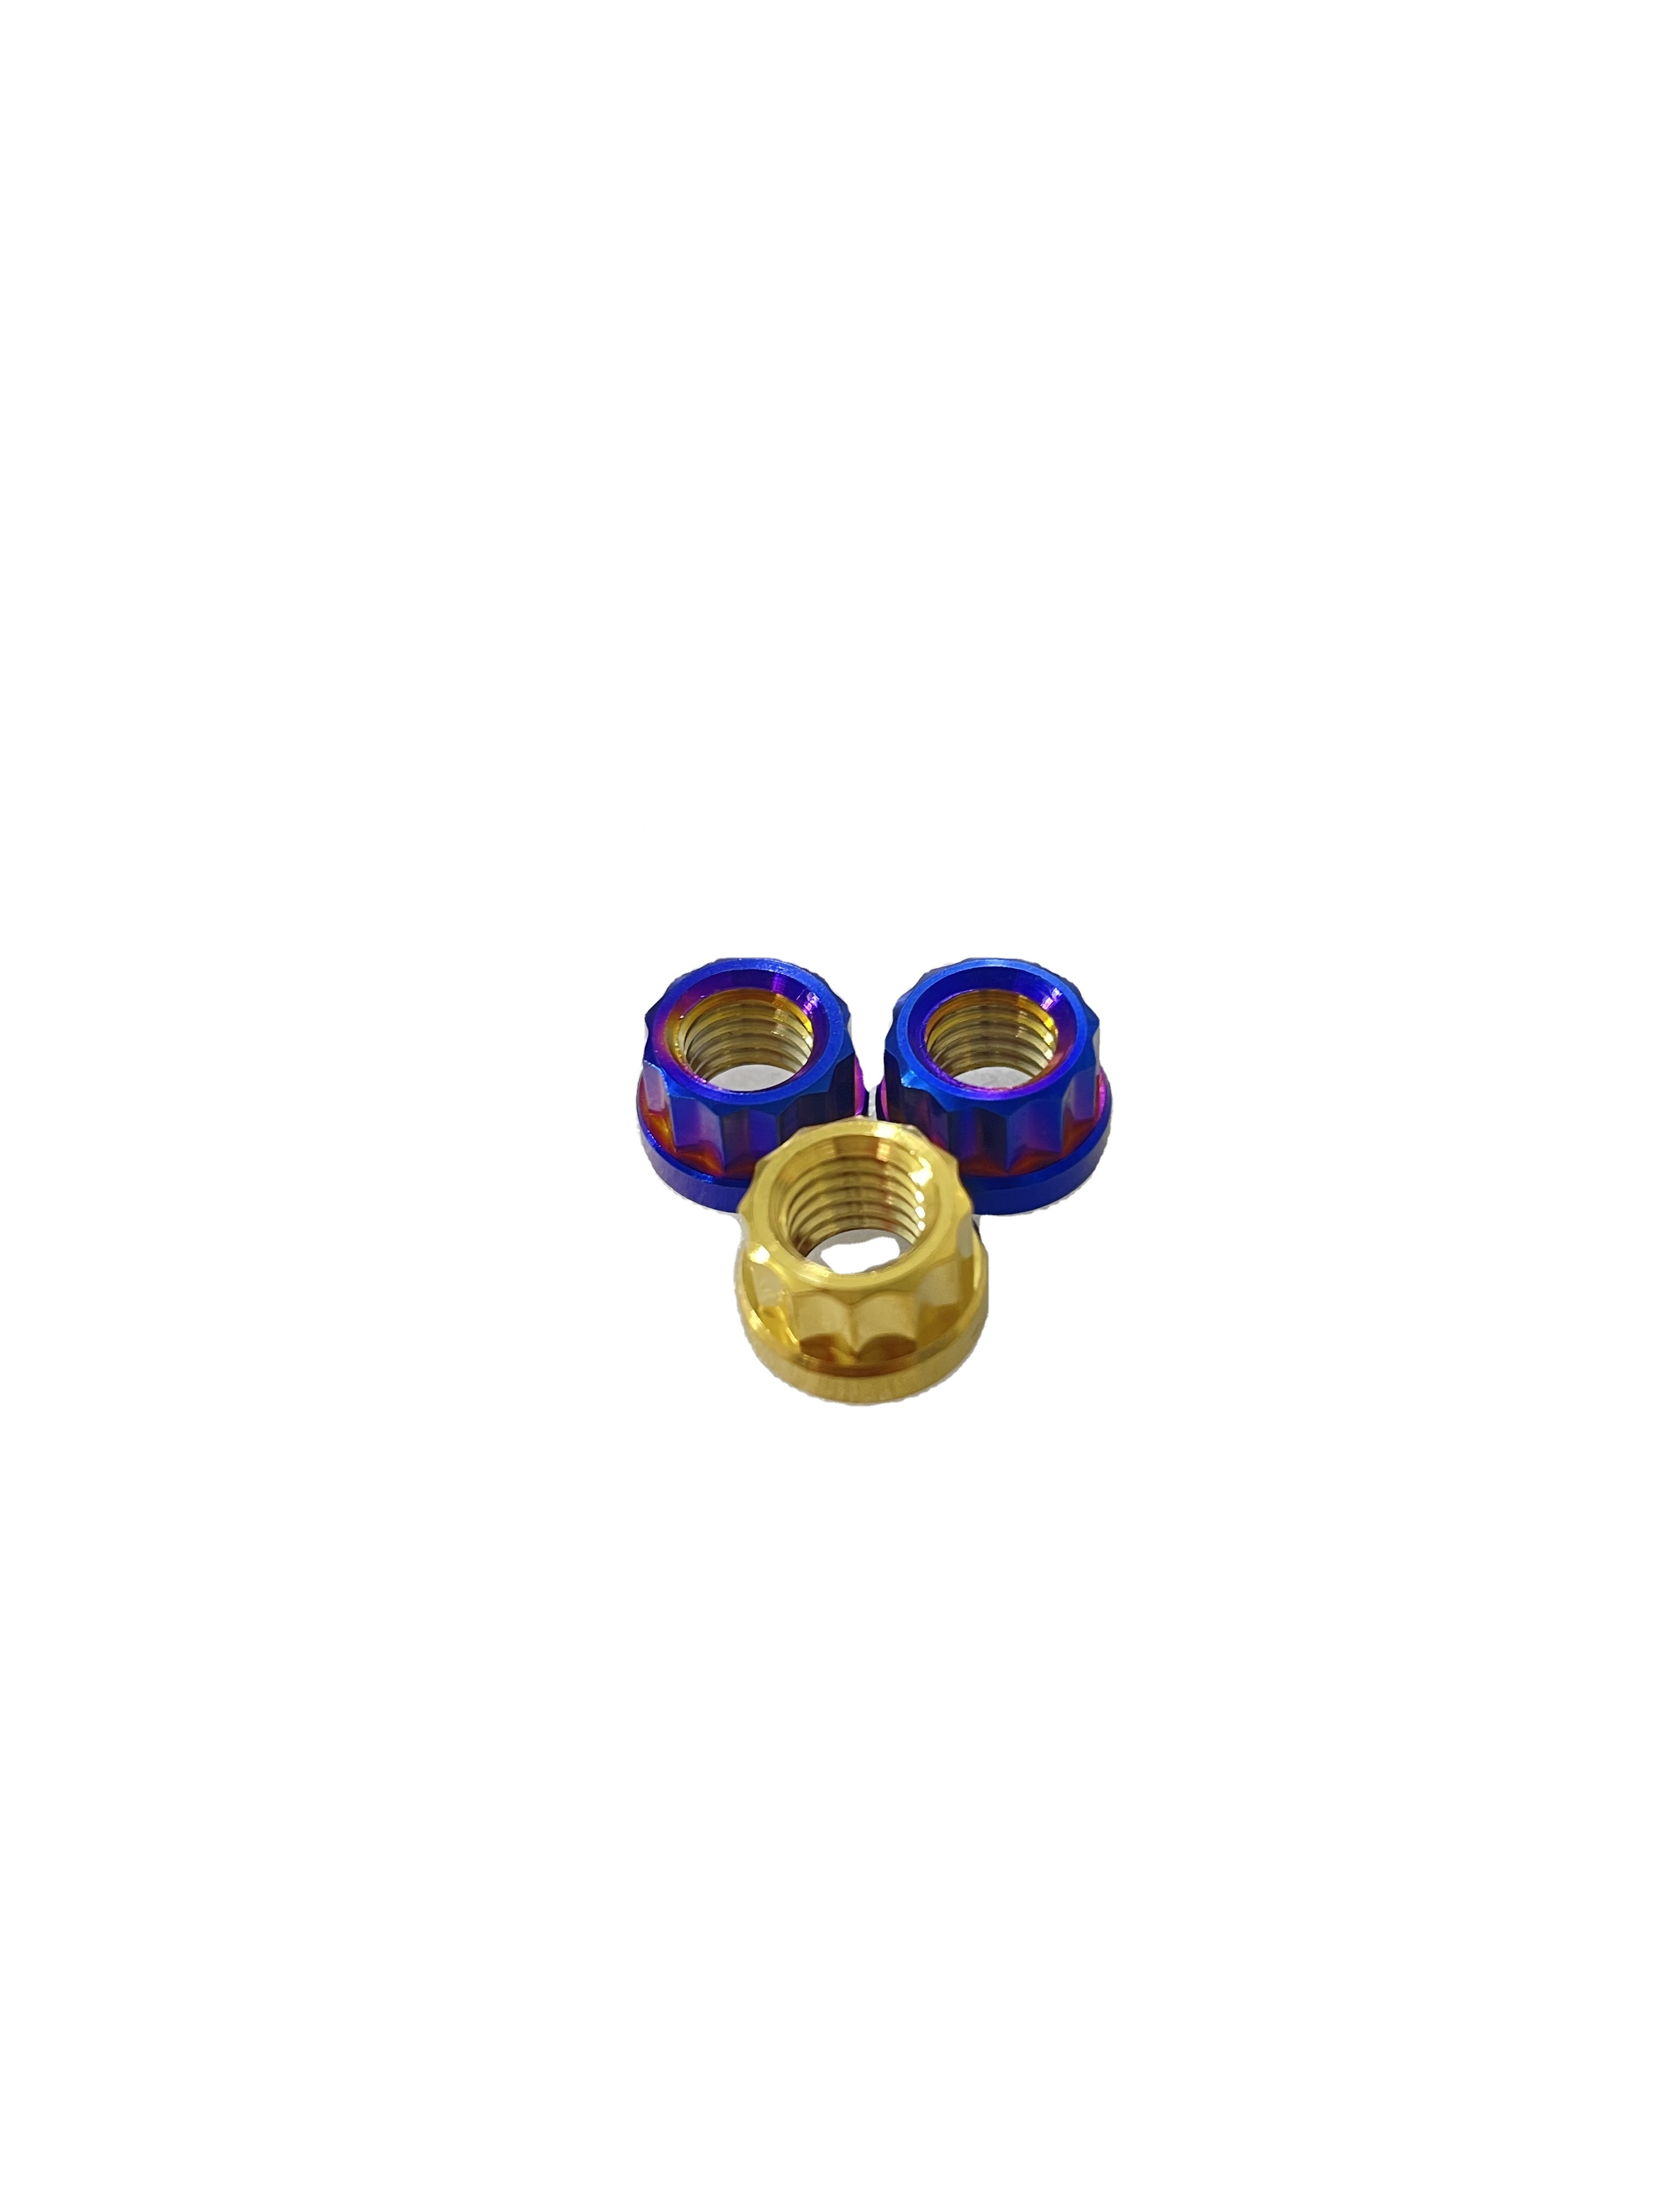
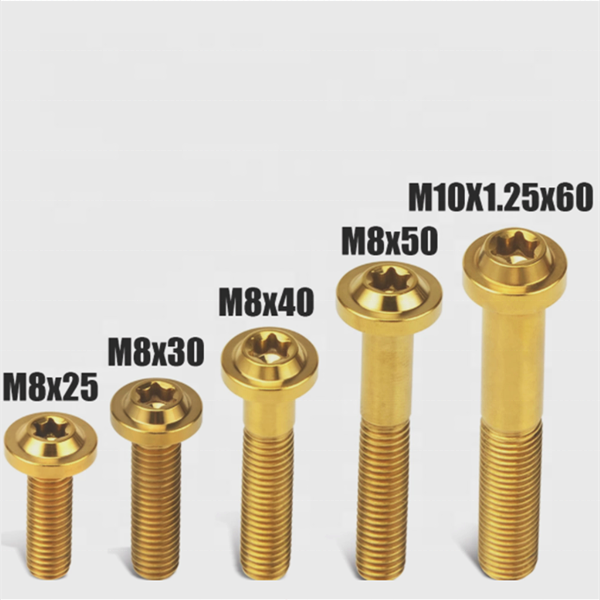
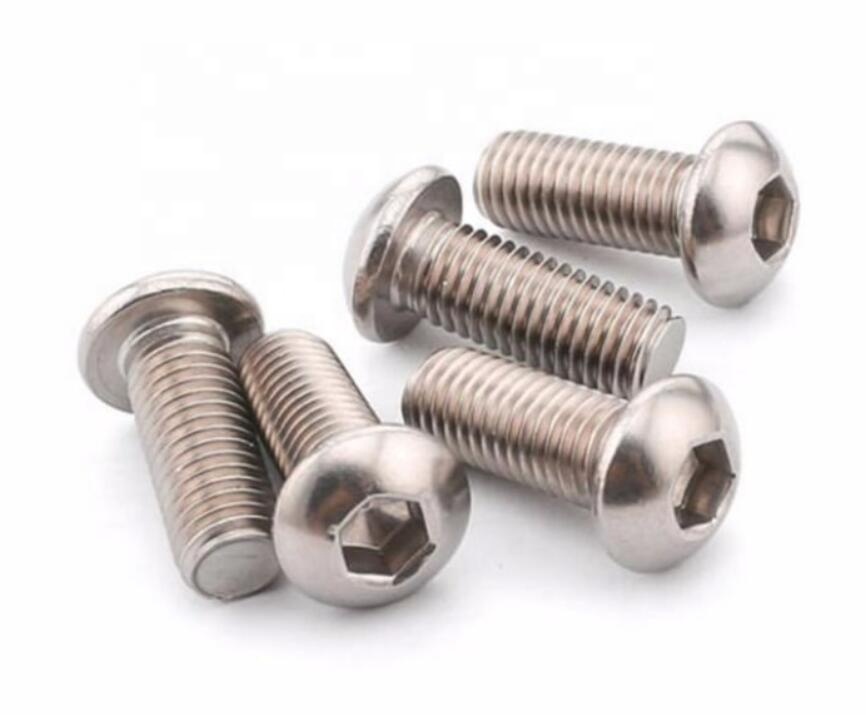
From the aggressive switchbacks of the Santa Cruz Mountains to high-speed fire roads in Saratoga Gap and Henry W. Coe State Park, disc brake rotor fasteners in Northern California face unrelenting thermomechanical cycling.
Braking on steep descents along Skyline Boulevard and Santa Clara County foothill trails generates localized rotor hub temperatures surpassing 350°C. Standard low-carbon steel fasteners experience bolt stretch and torque loss due to differential thermal expansion. Our Grade 5 (Ti-6Al-4V) titanium disc rotor bolts maintain consistent pre-load tension and structural integrity without embrittlement or micro-deformation under intense downhill thermal gradients.
In high-torque cross-country and competitive enduro racing, peripheral un-sprung rotational mass heavily impacts wheel acceleration and responsive steering damping. Grade 5 titanium boasts a low density of 4.43 g/cm³, offering 44% weight reduction compared to standard 10.9-grade steel fasteners while sustaining a tensile strength of over 895 MPa. This mass reduction at the wheel hub enables faster direction changes through technical rock gardens and root step-downs.
Moisture rolling off Monterey Bay into the South Bay region brings marine coastal chlorides and acidic dust loam that rapidly oxidize standard cadmium-plated steel bolts, causing galvanic corrosion with aluminum hubs. Titanium forms a dense, spontaneously repairing passive titanium oxide (TiO2) film that is chemically inert to chlorides, washing solvents, brake fluids, and winter mud, completely eliminating risk of seized fasteners during hub rebuilds.
| Fastener Material | Tensile Strength (MPa) | Yield Strength (MPa) | Density (g/cm³) | Corrosion Resistance | Weight Saving vs Steel |
|---|---|---|---|---|---|
| Ti6Al4V Grade 5 (Vunza Specification) | ≥ 895 – 1050 | ≥ 828 | 4.43 | Immune to Chlorides / Outdoor Acids | ~44% Lighter |
| Grade 10.9 High-Tensile Steel | 1040 | 940 | 7.85 | Moderate (Requires Zinc/Phosphate Plating) | Baseline (0%) |
| Commercial Pure Titanium (Grade 2) | 345 | 275 | 4.51 | Superior Chemical Resistance | ~42% (Insufficient Tensile for Disc Rotors) |
| 7075-T6 Billet Aluminum Alloy | 572 | 503 | 2.81 | Prone to Galvanic & Pitting Stress | Dangerous (Unacceptable Shear for Rotor Hubs) |
Detailed analysis of how boutique frame builders, aftermarket distributor brands, and high-performance electric mountain bike manufacturers across the Bay Area are evolving their hardware specifications.
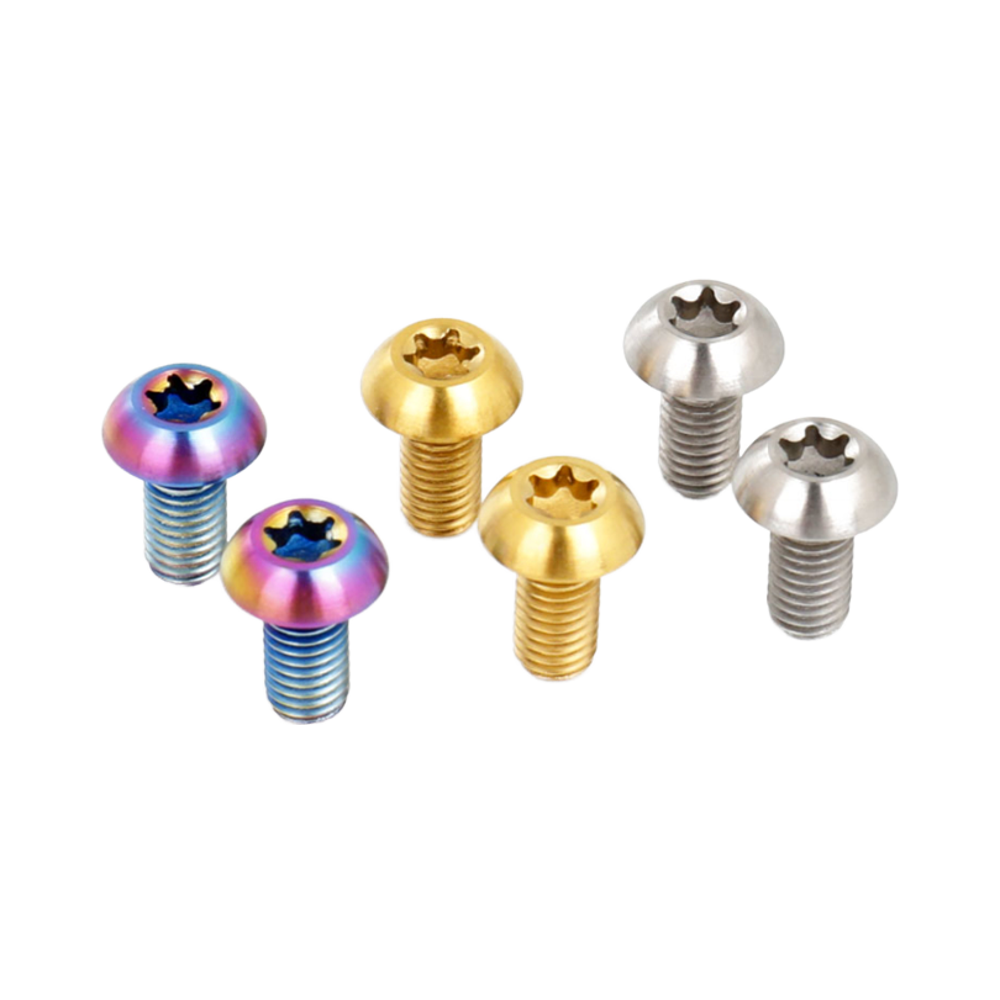
The explosive adoption of high-power Class 1 and Class 3 electric mountain bikes across Northern California trail networks has radically escalated brake torque demands. Electric mountain bikes weigh between 22 kg to 26 kg, generating tremendous shear force across 203mm and 220mm rotors during high-speed deceleration. Boutique assemblers in Santa Clara and San Jose are shifting from traditional M5 carbon steel screws to precision cold-forged Grade 5 titanium rotor bolts equipped with deep T25 Torx drive profiles that resist head rounding under higher pre-torquing thresholds.
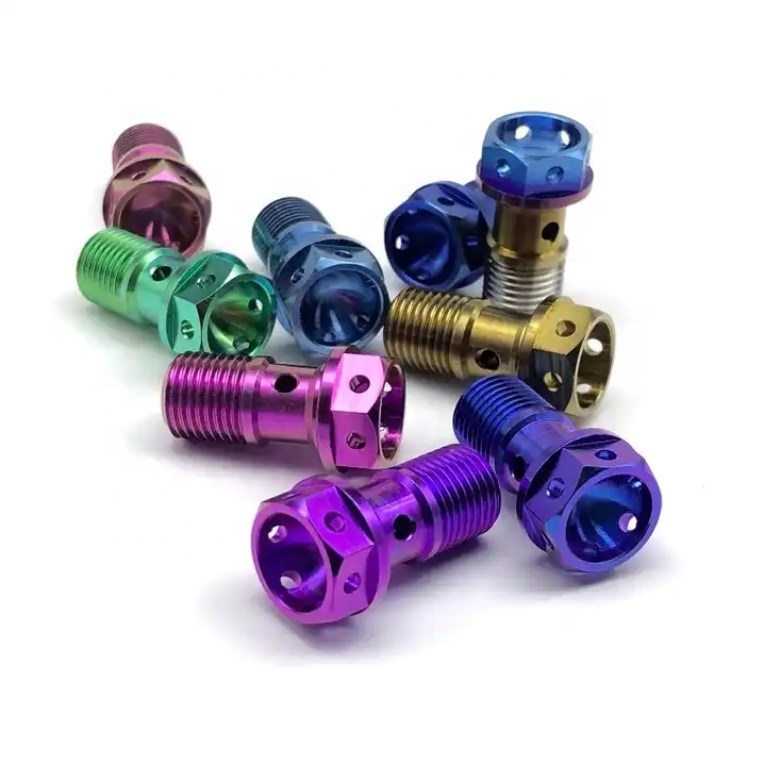
Santa Clara consumers demand bespoke visual aesthetics that integrate seamlessly with high-end anodized suspension fork crowns, dropper posts, and hub shells. Bicycle importers and aftermarket distributors actively commission customized Physical Vapor Deposition (PVD) rainbow, burnt blue, stealth matte black, and gold nitride finishes. These surface modifications not only provide striking optical color consistency but also increase surface micro-hardness above HV 2200, extending lifespan against wrench galling.
Tech-focused cycling startups and established component distributors in the Silicon Valley corridor are increasingly avoiding multi-tiered trading intermediaries. By executing direct OEM/ODM contracts with verified Baoji factories, procurement directors secure verified mill test certifications (MTC), customize packaging dimensions, apply laser-etched batch identifiers, and benefit from stable lead times with reliable door-to-door DDP logistics right to their Northern California distribution centers.
Operating from Gaoya Village Industrial Zone directly adjacent to the Baoti Group Industrial Park in China's Titanium Valley, we control every manufacturing phase from raw titanium sponge formulation to microscopic thread inspection.
Our workshop houses 34 units of Japanese and Taiwanese high-precision 3-axis, 4-axis, and simultaneous 5-axis CNC machining suites. We maintain continuous dimensional repeatability to within 0.005 mm, ensuring flange concentricity, perfect drive-socket depth, and uniform head profiles for seamless robotized and manual wheel assembly line installations.
Founded in 2008, over 50% of our production personnel possess more than 13 years of specialized non-ferrous metal machining experience. Our senior R&D engineering department works directly from customer CAD drawings (STEP, IGES, DXF) to optimize toolpaths, select grade-specific cutting fluid ratios, and eliminate tool chatter marks on all critical load-bearing shoulders.
Unlike budget factories that turn threads with single-point cutting bits (which shears metal grain lines and introduces micro-crack initiation points), all Vunza titanium brake rotor fasteners feature precision cold-rolled threads. This cold-forming process continuously aligns the titanium internal grain structure, improving fatigue strength by over 30% and eliminating thread binding.
Technical and logistics answers prepared by our export engineering team to streamline component prototyping and containerized purchasing.
A: We exclusively recommend Grade 5 Ti-6Al-4V (TC4) for all mountain bike rotor and caliper attachment hardware. Grade 2 pure titanium has exceptional chemical corrosion resistance but lacks the required shear and yield strength for safe braking torque. Grade 5 offers a minimum tensile strength of 895 MPa, guaranteeing reliable clamping torque under repeated emergency braking.
A: The standard industry specification for 6-bolt international standard (IS) disc rotor mounting is M5 x 10mm with a 0.8mm thread pitch. We engineer low-profile button heads or tapered flange heads with precision CNC-broached T25 Torx drive pockets. Custom lengths (e.g., M5 x 12mm, M5 x 15mm for fat bikes or specialty hub spacers) can be quickly fabricated to your technical drawings.
A: Yes. We routinely supply OEM rotor bolts pre-coated with medium-strength microencapsulated thread-locking adhesives (such as Loctite 242/243 equivalent). The adhesive remains dry to the touch during bulk shipping and instantly activates upon threading into the hub flange, saving valuable assembly minutes for bicycle brand assembly facilities in the US.
A: We provide comprehensive DDP (Delivered Duty Paid), DAP, and FOB air/sea freight services. For prototype batches and urgent replenishment, we dispatch via DHL Express, FedEx, or UPS with transit times of 4 to 6 business days directly to Santa Clara, San Jose, or Sunnyvale facilities, with all US customs declarations, tariffs, and clearance handled seamlessly.
A: Every production batch is accompanied by an authentic Mill Test Certificate (MTC) according to EN 10204 3.1 detailing chemical composition (Ti, Al, V, Fe, C, N, H, O) and mechanical tensile testing results. We also provide full dimensional First Article Inspection (FAI) reports and CMM coordinate inspection sheets upon request.
A: Standard polished titanium bolts have an MOQ starting at 300 pieces. For custom anodized colors (purple, gold, emerald green, rainbow) or laser-etched brand logos on the bolt perimeter or top face, our minimum order quantity is typically 500 to 1,000 pieces, with sample prototypes manufactured within 7 business days.
Whether you require standard M5x10mm T25 titanium rotor bolts or fully customized CNC lightweight components for high-stress bicycle, racing, or aerospace systems, Vunza Titanium delivers certified precision directly to your Santa Clara operations.