Racing Wheel
Explore our precision CNC-machined titanium hardware, engine architecture components, and direct-replacement motorsport assemblies designed for extreme thermal and mechanical endurance.
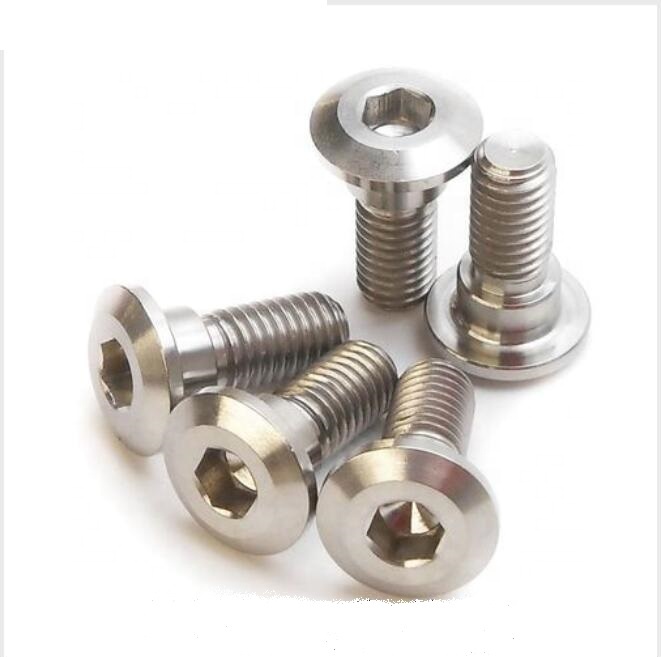

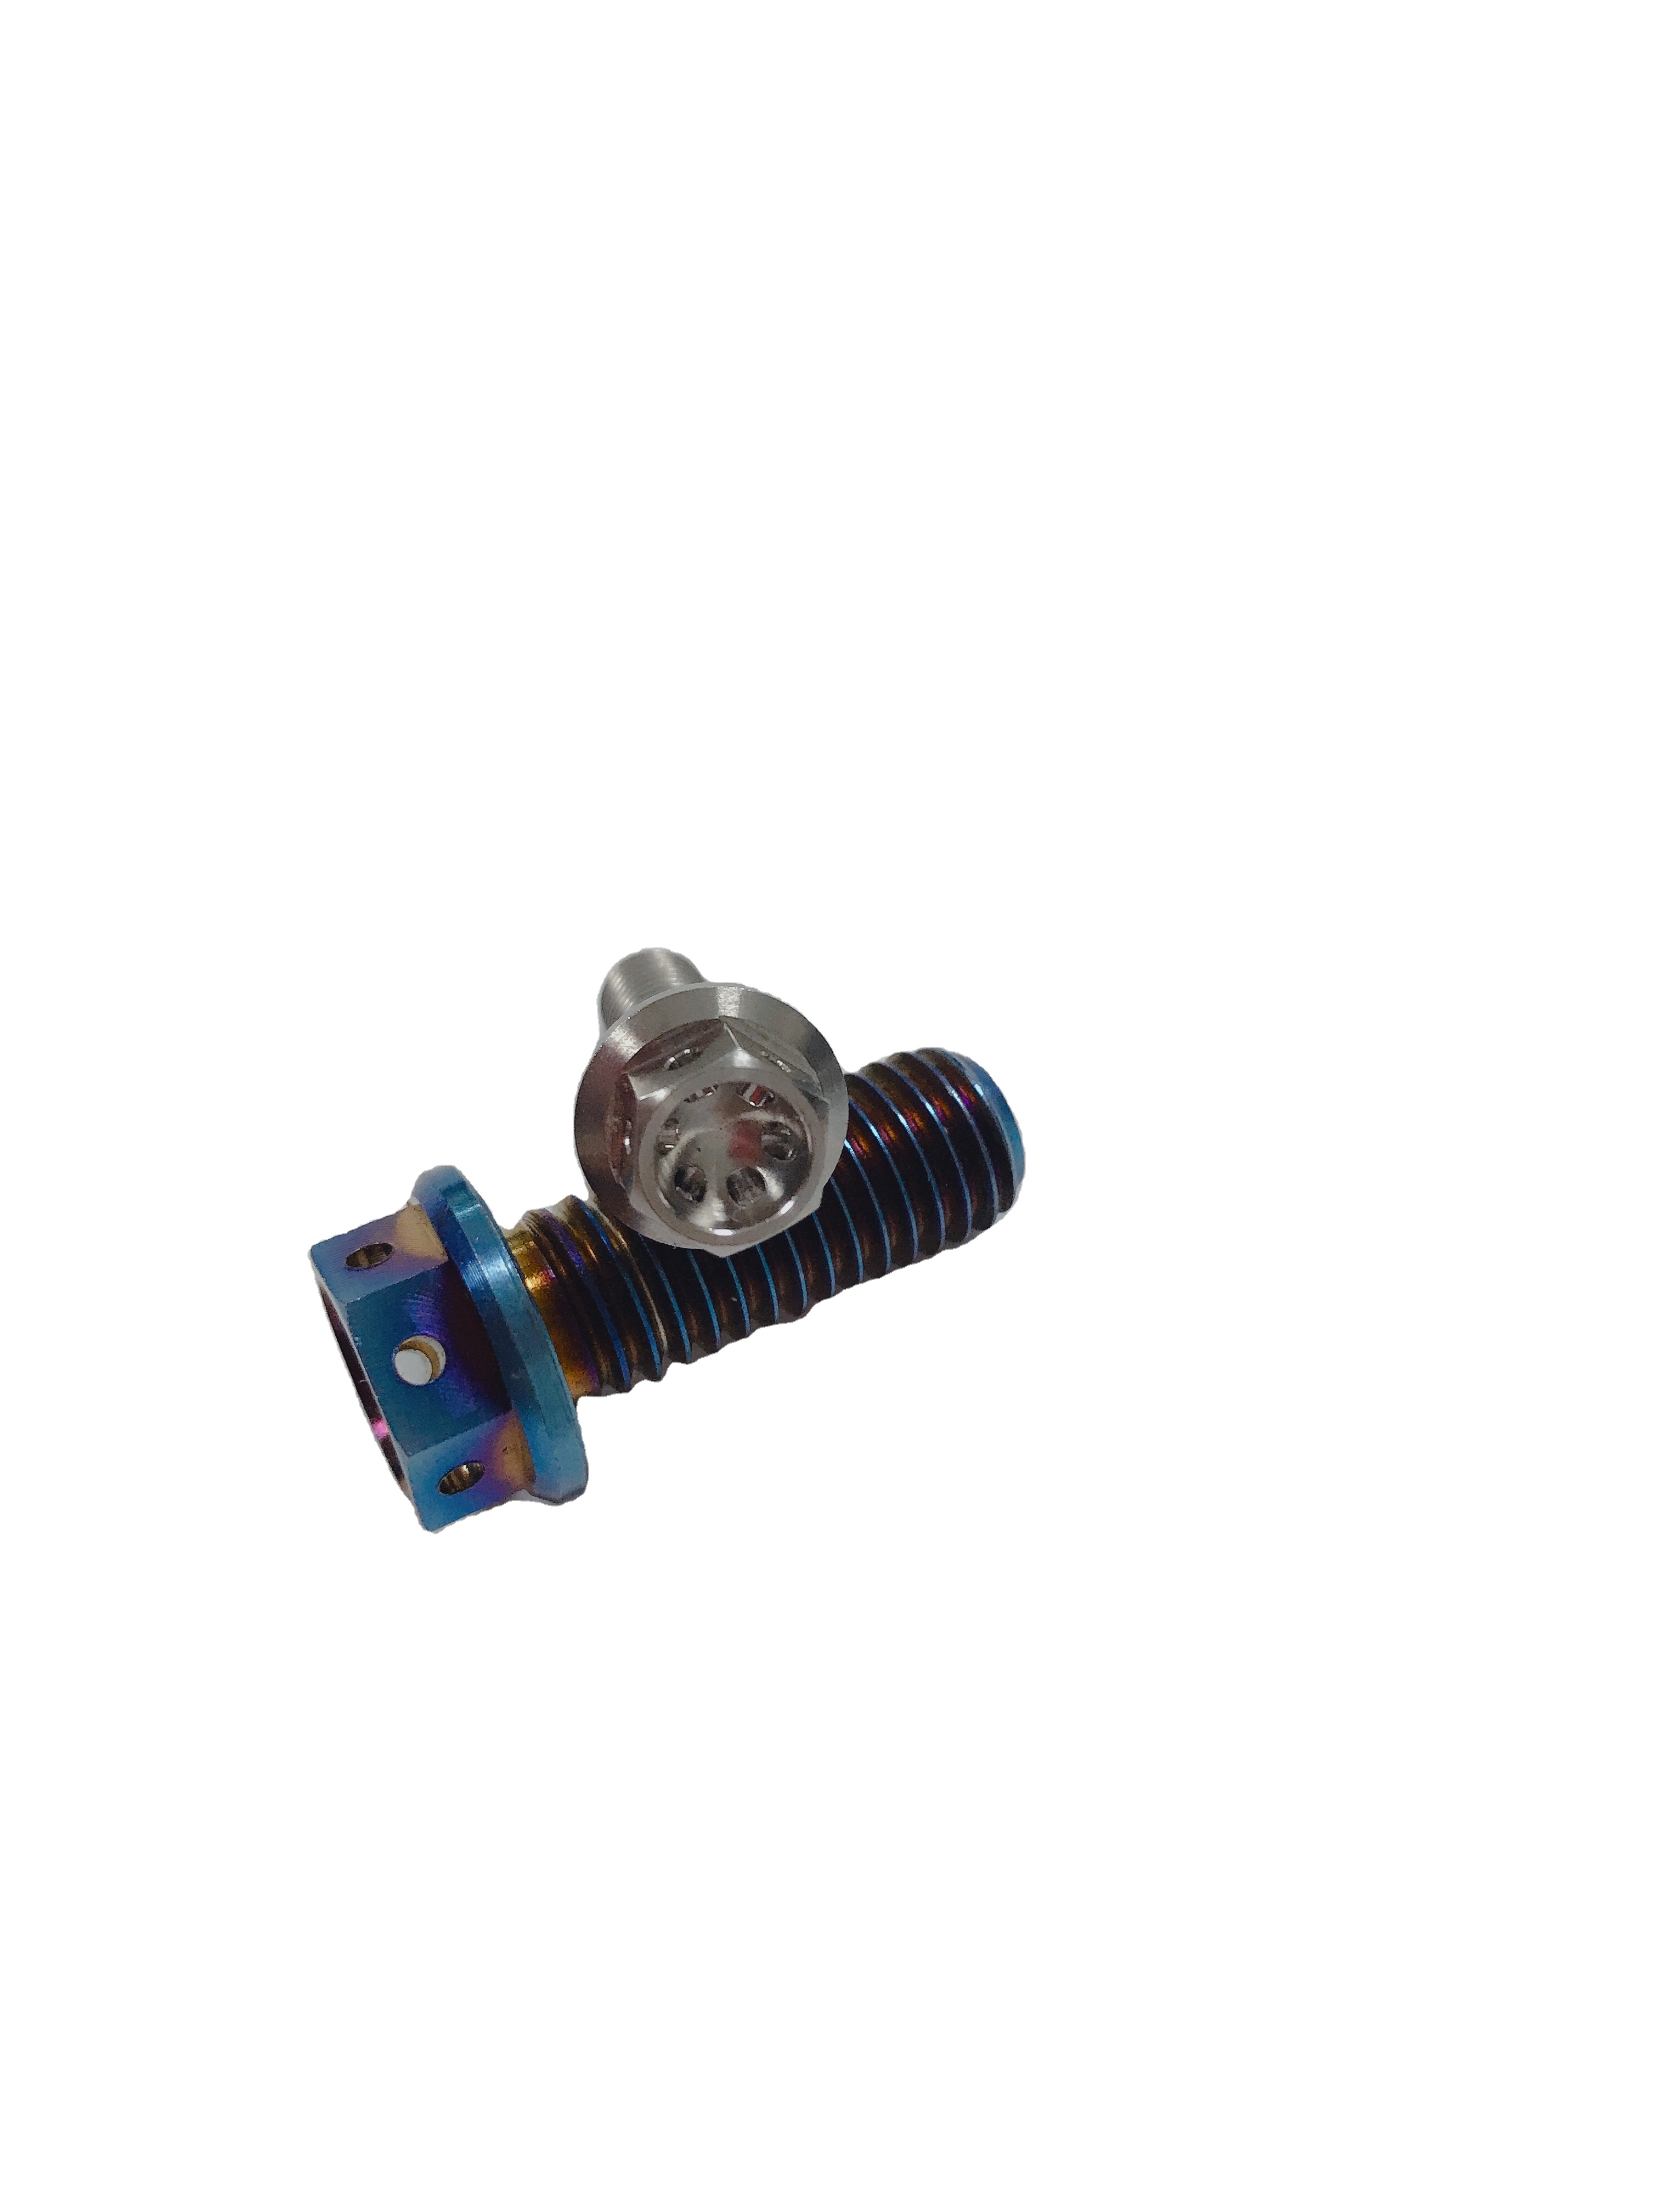
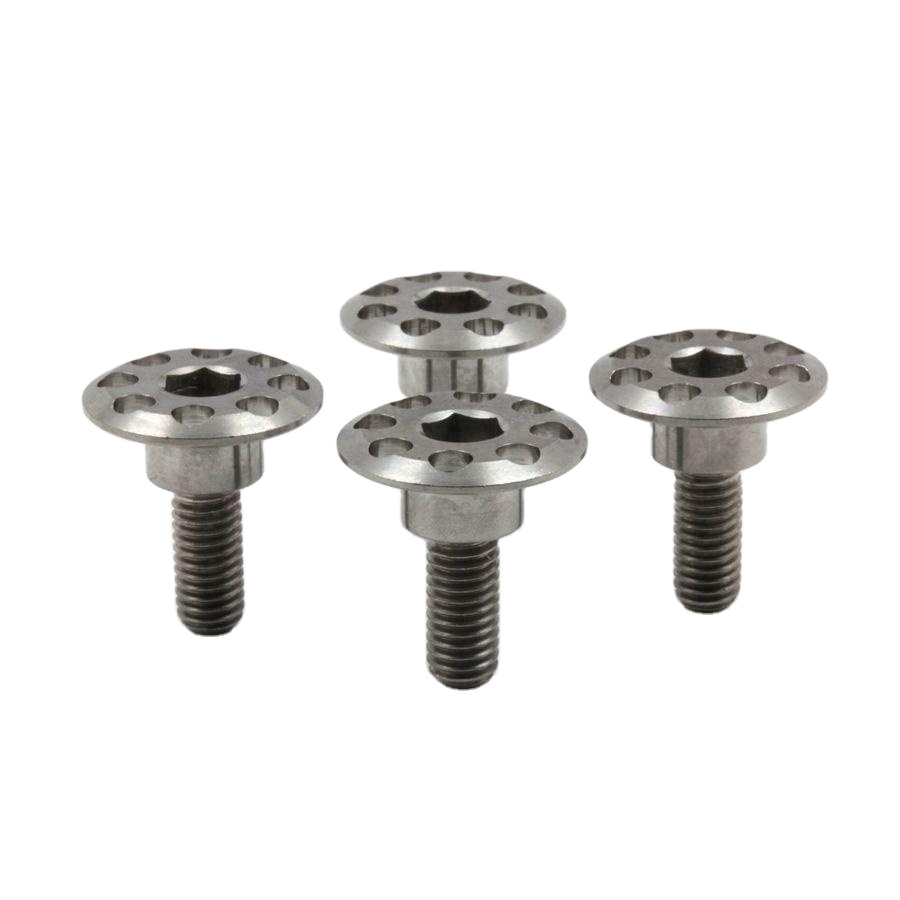
In modern motorsport engine calibration, valvetrain reciprocating mass is the primary barrier to achieving reliable engine speeds beyond 9,000 RPM. Vunza Titanium manufactures retainers tailored to eliminate harmonic float and reduce dynamic inertia.
Switching from tempered 4140 chromoly steel to aerospace-certified Ti6Al4V Grade 5 titanium delivers a direct mass reduction of roughly 40% to 44%. Lowering inertial weight on the spring side increases valvetrain natural frequency, pushing critical resonance thresholds outward and suppressing valve bounce without mandating punishing spring seat pressures.
Every titanium retainer is profiled on multi-axis Japanese CNC machine centers to hold concentricity tolerances under 0.005 mm across the keeper pocket and spring step. Perfectly balanced seat angles (7°, 8°, or 10° super-locks) ensure axial loading across the valve stem, eradicating local stress spikes and valve neck fatigue during high-lift events.
Titanium in raw contact with steel valve springs can be susceptible to microwelding and galling. Vunza provides optional PVD (Physical Vapor Deposition) Titanium Nitride (TiN), Diamond-Like Carbon (DLC), or deep thermal oxidation treatments. This process yields a micro-hardness exceeding 65 HRC on friction steps while maintaining ductile core fatigue strength.
| Characteristic / Parameter | Ti6Al4V Grade 5 (Baoji Vunza Spec) | Tempered Tool Steel (4140/4340) | 7075-T6 Billet Aluminum | Race Significance in Engine Valvetrain |
|---|---|---|---|---|
| Density (ρ) | 4.43 g/cm³ | 7.85 g/cm³ | 2.81 g/cm³ | Titanium drops mass by 44% vs steel; far higher fatigue resilience than aluminum. |
| Tensile Strength (σb) | ≥ 980 - 1050 MPa | 850 - 1000 MPa | 520 - 570 MPa | Guarantees retainer keeper walls do not deform or shear under 400+ lbs open valve load. |
| Yield Strength (σ0.2) | ≥ 895 - 920 MPa | 730 - 850 MPa | 430 - 500 MPa | Suppresses keeper groove yield deformation under violent high-cam deceleration pulses. |
| Thermal Expansion (α) | 8.6 × 10⁻⁶ / K | 12.2 × 10⁻⁶ / K | 23.4 × 10⁻⁶ / K | Superior dimensional stability inside cylinder heads where oil heats past 140°C. |
| Service Life Cycle | High Endurance (Full Season) | Infinite (Excessive Weight) | Extremely Short (Drag Only) | Optimal balance for circuit racing: lightweight safety margin without recurring failure risk. |
Madrid serves as the nerve center for Iberian motorsport development, combining elite engineering faculties, bespoke touring car skunkworks, and immediate proximity to historic testing tracks like Circuito del Jarama. Our racing titanium valve retainers satisfy the exacting requirements of distinct automotive racing sectors located across the Community of Madrid.
Race engineering ateliers across San Sebastián de los Reyes and Getafe rely on our valve retainers when upgrading 2.0 TSI and inline turbo platforms. High boost levels induce valve lift instability; lightening retainer weight ensures intake and exhaust valves accurately follow extreme cam lobes through heavy downshifts along Jarama's technical corners without catastrophic float.
Madrid hosts respected classic rally restoration hubs restoring legendary Group A, BDA Cosworth, and Alfa Romeo Busso powerplants. Sourcing obsolete original factory retainers is nearly impossible. Vunza reverse-engineers keeper geometry from worn samples or 2D technical drafts, supplying matched Grade 5 retainers that modernize valvetrain reliability while honoring period FIA specs.
Universities and technical workshops in Leganés and Madrid rely on single-cylinder and twin-cylinder supersport motorcycle blocks (e.g., CBR600RR, KTM 450 SX-F) for custom racing prototypes. Vunza manufactures ultra-miniaturized 4.5mm to 5.5mm valve stem titanium retainers that allow engine builders to run 14,000+ RPM redlines with zero harmonic flutter.

A clear operational shift is taking place across Spain's motorsport manufacturing sphere. Teams are leaving third-party domestic catalog middlemen to partner directly with primary titanium mills and specialized CNC production centers.
Engine preparation budgets in the Iberian peninsula face rising transport overheads and component markups. Madrid workshops now bypass multi-tier European distributors. Sourcing direct from China Titanium Valley (Baoji) allows racing outfits to cut retainer unit costs by 35% to 50% while securing verifiable mill certificates and dimensional inspection logs.
As touring car platforms integrate 48V mild hybrid motors and synthetic e-fuel combustion, cylinder head chamber pressures and thermal cycling loads have surged. Standard alloy retainers cannot withstand these thermal variations without galling. Grade 5 titanium, reinforced by micro-shot peening and specialized surface coating, has emerged as the baseline standard across Madrid's top engine programs.
Standard catalog retainers often force compromises in spring installed height and keeper lock angles. Spanish racing teams increasingly request custom CAD/CAM profile turnarounds within 7 to 10 days. Vunza's dedicated 34 multi-axis machine cells allow fast transitions from step-file review to prototype air-freight arriving at Madrid-Barajas Airport (MAD).
Headquartered in Gaoya Village Industrial Zone, Baoji, Shaanxi (China Titanium Valley), adjacent to the Baoti Group Industrial Park, Vunza Titanium Industry Co., Ltd. provides true sponge-to-part traceability for critical aerospace and motorsport systems.
Our workshop floor houses 34 dedicated 3-axis, 4-axis, and 5-axis high-speed CNC turning and milling centers capable of turning complex undercut keeper grooves, micro spring pockets, and featherweight hollow stems to 0.005 mm repeatability.
Quality begins at the melt. We source premium grade titanium sponge and traceable vacuum arc remelted (VAR) billets. Every valve retainer batch is accompanied by EN 10204 3.1 chemical composition analysis and physical mechanical tensile reports.
Over 50% of our production technicians have more than 13 years of specialized experience in cutting and tool-path engineering for reactive refractory alloys. We prevent thermal stress build-up and tool deflection during deep-groove retainer milling.
With an average enquiry turnaround of less than 9 hours, our export and engineering support teams seamlessly service Madrid time (CET/CEST), providing rapid DFM reviews, commercial invoicing, and express DDP air-freight logistics straight to your shop floor.
Clear technical answers addressing the real concerns of motorsport workshops, restoration garages, and precision procurement officers sourcing from our Baoji facility.
Submit your CAD drawing, keeper angle, spring OD/ID specs, or valve stem diameter. Our senior technical team in China Titanium Valley will return DFM feedback, dimensional verification, and factory-direct pricing within 9 hours.