ISO/Metric
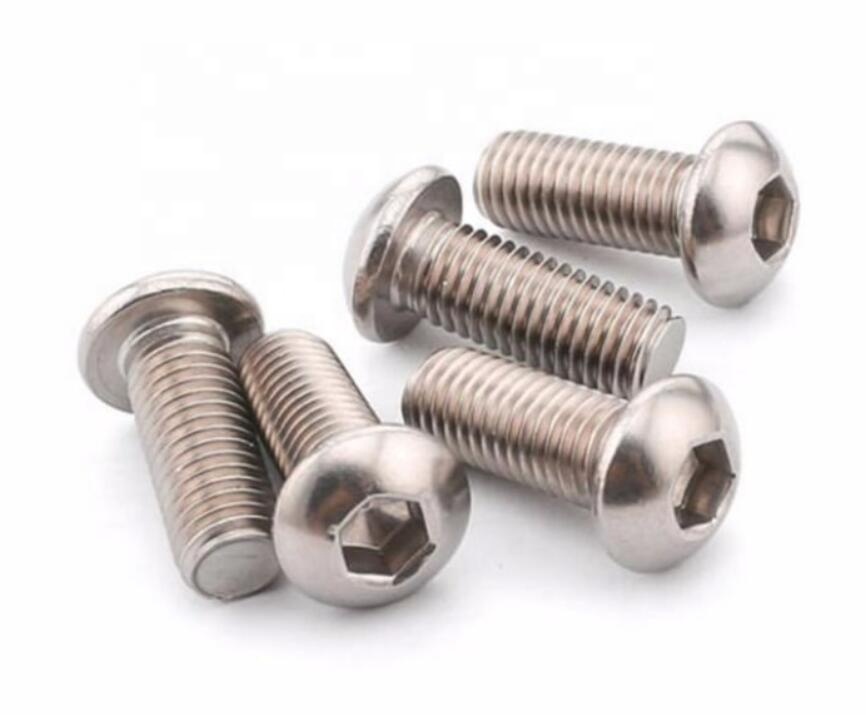
Direct-from-factory titanium fasteners, precision CNC multi-axis milled structural components, and high-performance hardware manufactured under rigorous quality systems from China's Titanium Valley to international delivery benchmarks.
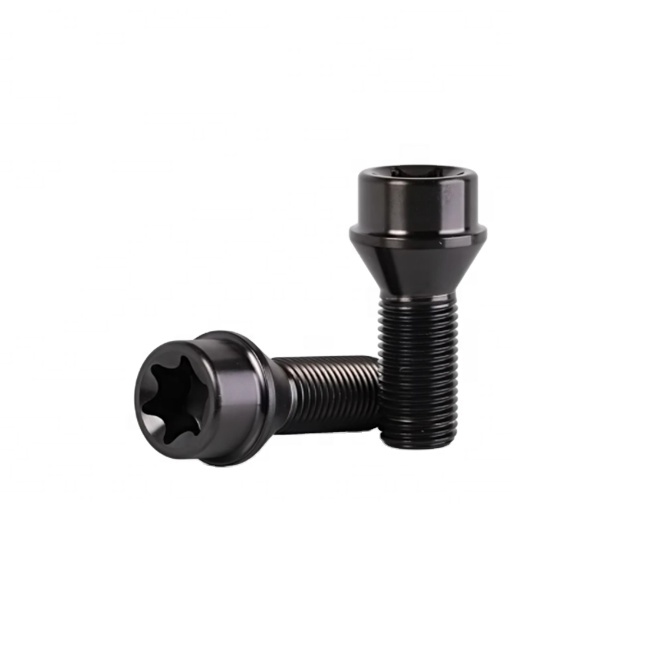
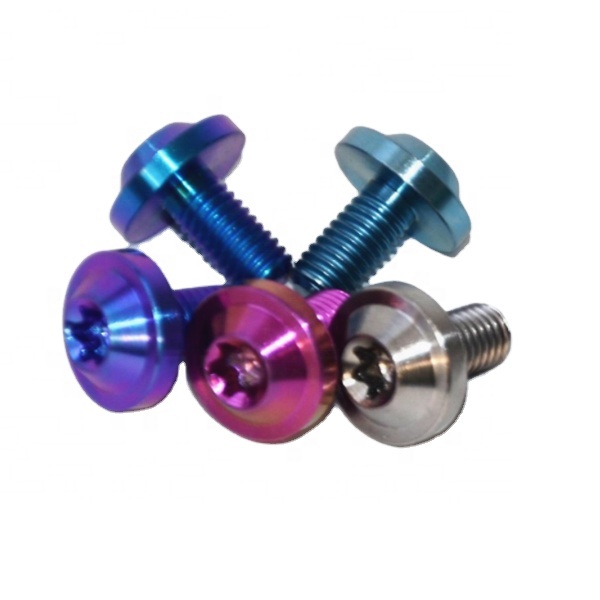
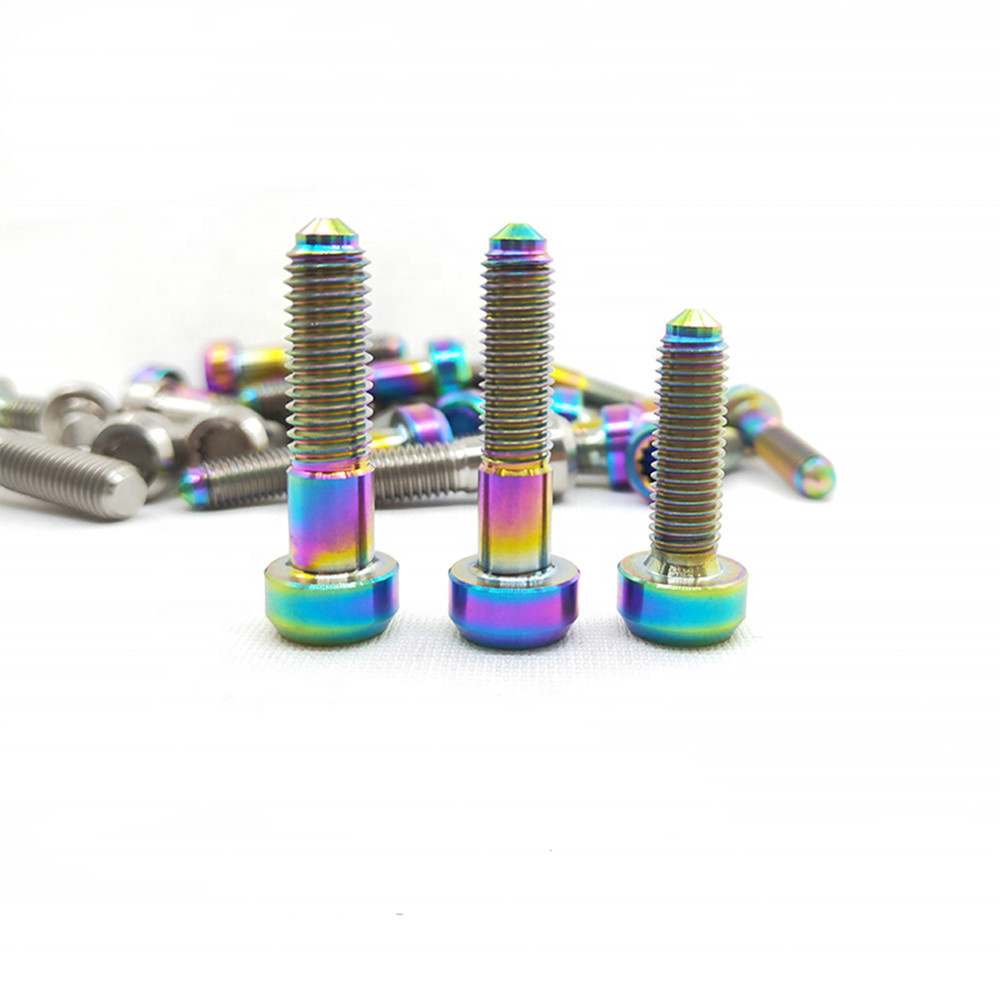
Titanium flat head screws—also known internationally as countersunk screws conforming to DIN 7991, ISO 10642, and ASME B18.6.3 standards—represent the pinnacle of flush-mount fastening technology. Machined primarily from Grade 5 Ti-6Al-4V (UNS R56400 / Werkstoff 3.7165) or commercially pure Grade 2 Titanium (UNS R50400 / Werkstoff 3.7035), these mechanical fasteners allow seamless coplanar assembly where physical clearance, zero aerodynamic disturbance, or uniform heat dissipation are strict operational constraints.
In high-precision manufacturing, especially within the specialized technological corridor encompassing Balzers, the Rhine Valley, and the broader Liechtenstein-Swiss micro-engineering cluster, fastening requirements consistently transcend the mechanical capacities of standard A2/A4 austenitic stainless steels or carbon alloy hardware. Flat head titanium screws manufactured by Vunza Titanium integrate cold-heading and multi-axis CNC secondary turning directly from high-purity sponge material, delivering exceptional tensile strengths (≥ 895 MPa for Ti-6Al-4V), an approximate 44% mass reduction compared to structural steel, zero ferromagnetic permeability, and unmatched passivity against aggressive processing media.
For applications where cleanroom protocol, high thermal cycling, or reactive chemical deposition are encountered, titanium countersunk screws provide natural immunity against stress corrosion cracking and pitting. The immediate spontaneous formation of a coherent, self-healing titanium dioxide (TiO₂) boundary layer prevents galling and corrosion even when subjected to vacuum chamber conditioning, baking cycles, and alternating plasma processing fields.
Balzers and the surrounding Rhine Valley industrial ecosystem are universally recognized as world-leading centers for surface engineering, high-vacuum equipment, photonics, and micro-electromechanical fabrication.
As the international benchmark for physical vapor deposition (PVD) and cathode arc evaporation, Balzers-based equipment builders require screws with extremely low outgassing and near-zero magnetic distortion. Our Grade 5 and Grade 2 flat head screws sit completely flush within shielding liners, target mounts, and vacuum turntables, eliminating particulate traps and avoiding virtual leaks inside high and ultra-high vacuum (HV/UHV) chambers.
The regional precision optics cluster relies on countersunk titanium hardware to lock mirror retainers, prism mounts, and beam splitters without thermal hysteresis. The low thermal expansion coefficient of Ti-6Al-4V (8.6×10⁻⁶/K) closely matches specialized optical glasses and ceramic substrates, preventing alignment drift during intensive industrial multi-kilowatt laser operations.
Surgical instrumentation manufacturers and analytical laboratory equipment integrators throughout the Rhine valley mandate non-toxic, biologically inert, and non-magnetic mechanical fasteners. With Grade 23 Ti-6Al-4V ELI (ASTM F136) availability and strictly degreased clean packaging, our flat head screws ensure complete compliance with demanding European medical device regulations.
Over the past decade, high-technology procurement across the Principality of Liechtenstein and Eastern Switzerland has shifted decisively away from legacy corrosion-resistant nickel alloys and austenitic stainless steels (such as 1.4404 / 316L) toward certified titanium alloys. Three market-driven imperatives are fueling this technological evolution:
1. Aggressive Miniaturization & Inertial Reduction in Multi-Axis Automation: High-speed pick-and-place equipment, wafer-handling end effectors, and dynamic vacuum arms require the highest possible power-to-weight ratio. By incorporating Ti-6Al-4V flat head screws (density: 4.43 g/cm³ versus steel's 7.9 g/cm³), automation designers substantially reduce mechanical inertia, enabling higher cycle rates and less motor wear without lowering fastening clamp force.
2. Vacuum Cleanliness Standards in Semiconductor & Hard Coating Tooling: In high-throughput PVD/CVD systems, outgassing and magnetic permeability in fasteners create unwanted micro-arcing and plasma deflection. Titanium flat head screws are naturally non-magnetic (magnetic permeability μr ≈ 1.00005) and exhibit virtually negligible vapor pressure under high vacuum up to elevated chamber operating temperatures. Fastener recessed drives (such as Torx/Hexalobular ISO 10664) are CNC cleared of tooling residue, preventing virtual outgassing volumes beneath screw heads.
3. Sustainability & Lifecycle Integrity in Harsh Chemical Processing: Across Swiss and Liechtenstein chemical synthesis, sensor manufacturing, and alpine environmental monitoring, total lifecycle cost has become a focal metric. The superior chemical resistance of titanium to chlorides, wet chlorine, organic acids, and sulfur compounds eliminates premature mechanical failure and rust discoloration, avoiding costly cleanroom shutdowns and premature maintenance overhauls.
Compare mechanical properties and engineering thresholds across our most sourced countersunk screw grades.
| Property / Characteristic | Titanium Gr5 (Ti-6Al-4V / TC4) | Titanium Gr2 (Commercial Pure) | Stainless Steel A4-80 (1.4404) | Aluminum 7075-T6 |
|---|---|---|---|---|
| Tensile Strength (Rm) | ≥ 895 - 1050 MPa | ≥ 345 - 480 MPa | ≥ 800 MPa | ≥ 570 MPa |
| Yield Strength (Rp 0.2) | ≥ 828 MPa | ≥ 275 MPa | ≥ 600 MPa | ≥ 500 MPa |
| Density | 4.43 g/cm³ | 4.51 g/cm³ | 8.00 g/cm³ | 2.81 g/cm³ |
| Modulus of Elasticity | 114 GPa | 105 GPa | 200 GPa | 72 GPa |
| Magnetic Permeability (μr) | 1.00005 (Non-magnetic) | 1.00005 (Non-magnetic) | ~ 1.005 - 1.050 (Trace Mag) | 1.00002 (Non-magnetic) |
| Thermal Expansion (20-100°C) | 8.6 × 10⁻⁶ / K | 8.6 × 10⁻⁶ / K | 16.0 × 10⁻⁶ / K | 23.4 × 10⁻⁶ / K |
| Vacuum Outgassing Integrity | Exceptional / Non-porous | Exceptional / Non-porous | High outgassing risk if plated | Prone to surface oxidation |
| Drive Style Options | Torx (T6-T55), Hex Socket, Slot | Torx, Hex Socket, Cross Slot | Standard Hex / Torx | Hex Socket |
Vunza Titanium Industry Co., Ltd. combines raw titanium supply chain control in Baoji with world-class CNC precision capabilities to ensure compliance with European industrial standards.
Situated in the Gaoya Village Industrial Zone adjacent to the Baoti Group Industrial Park in Baoji, we operate within the epicenter of global titanium refining. This proximity allows complete raw material traceability from premium titanium sponge to vacuum arc remelted (VAR) billet stock, ensuring stable grain structure, uniform chemical properties, and no internal voids in cold-headed or machined fasteners.
Our workshop houses 34 advanced multi-axis (3, 4, and 5-axis) CNC high-precision machining centers along with automated cold heading and thread rolling equipment. We reliably hold linear tolerances to ±0.005 mm and thread accuracy to 4h/6g DIN classifications, preventing thread galling and guaranteeing repeat fitment for automated production lines.
Over 50% of our production personnel possess more than 13 years of specialized experience in cutting, threading, and finishing reactive refractory alloys. Our in-house technical engineering team reviews complex 2D/3D technical drawings (STEP, IGES, DXF) to recommend design-for-manufacturability (DFM) adjustments, custom thread leads, and underhead relief geometries.
Quality control operates under a closed-loop system encompassing spectral chemical analysis, tensile testing, torque yield proofing, micro-hardness verification, and automated optical thread inspection. Each production lot is dispatched with documented EN 10204 Type 3.1 Mill Test Certificates and Dimensional Inspection Reports.
We maintain an average inquiry response turnaround under 9 hours. In conjunction with reliable air-freight corridors serving Zurich-Kloten (ZRH) and local customs clearance agents in Liechtenstein/St. Gallen, our lead times for custom CNC prototypes span just 7 to 10 working days, with scheduled batch deliveries to maintain your inventory buffers.
Beyond natural mechanical fine polishing, we offer medical-grade Type II anodizing, vibrant decorative color anodizing, micro-arc oxidation, dry-film lubricant coating, and vacuum PVD finishes (including DLC and Titanium Nitride). These treatments eliminate galling during repeated assembly cycles in cleanroom environments.
Clear, direct technical responses addressing common engineering and sourcing considerations for titanium flat head screws.
Connect with our technical engineering desk in China's Titanium Valley. Submit your 2D/3D drawings, bill of materials, or application specifications for rapid design-for-manufacturability feedback, material verification, and immediate competitive quotes.