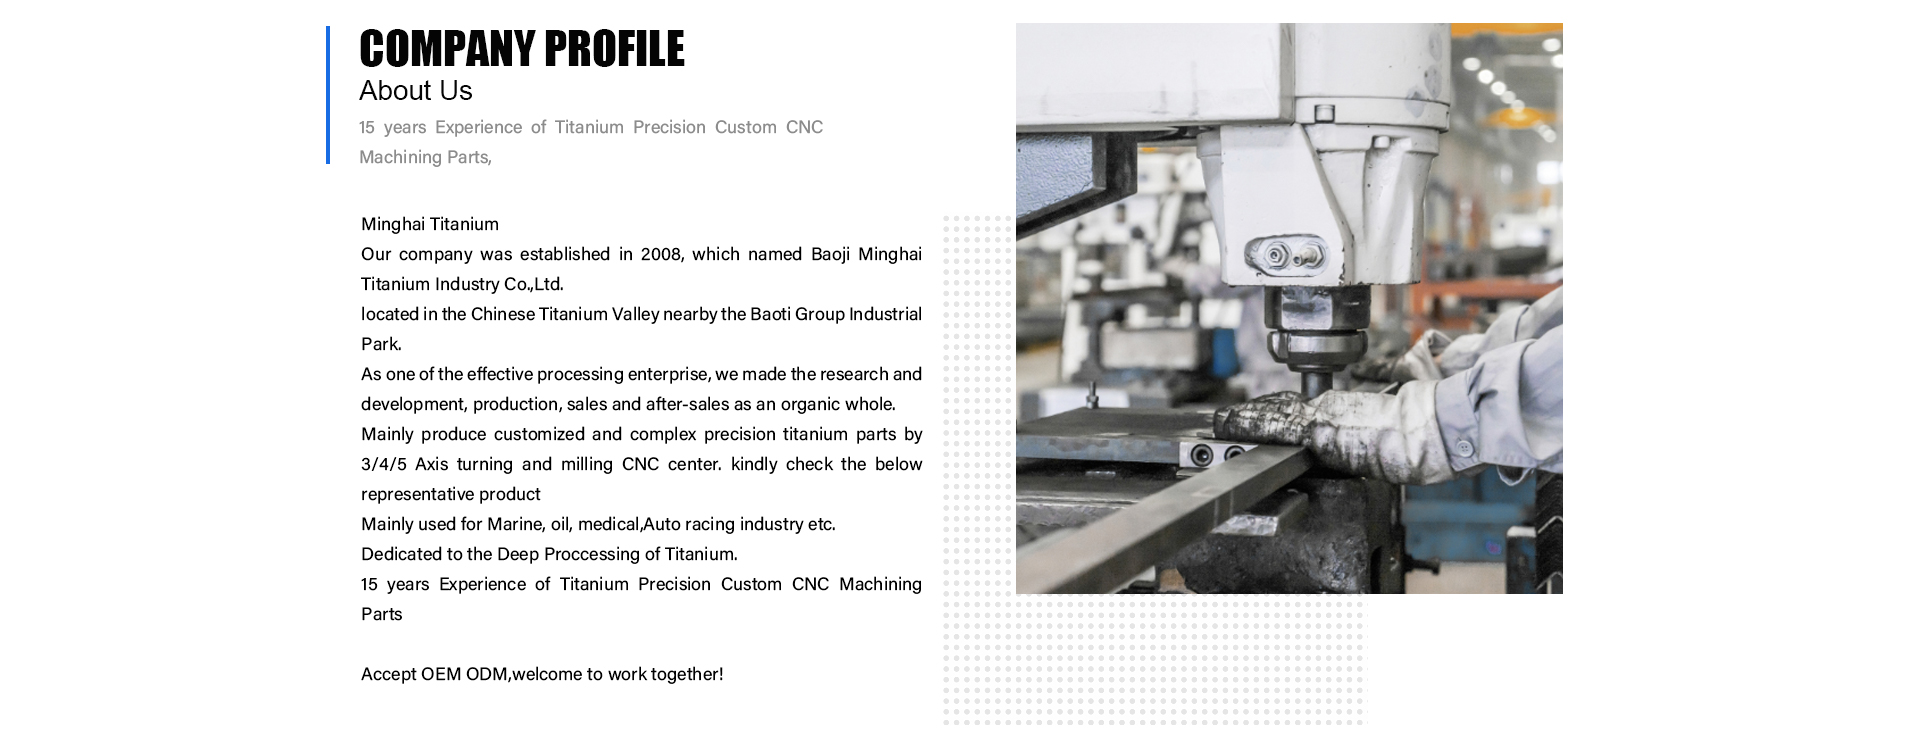
5-Axis CNC
Precision-turned Grade 5 (Ti-6Al-4V) components engineered for hyper-responsive reciprocating mass, extreme thermal resilience, and galvanic endurance in demanding performance atmospheres.
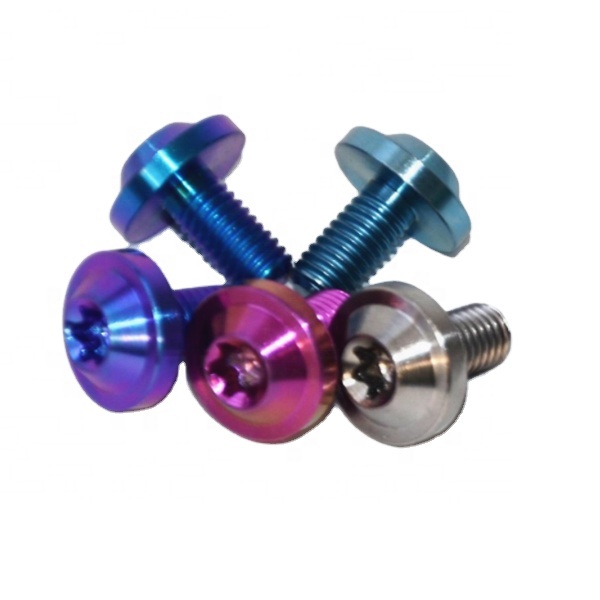
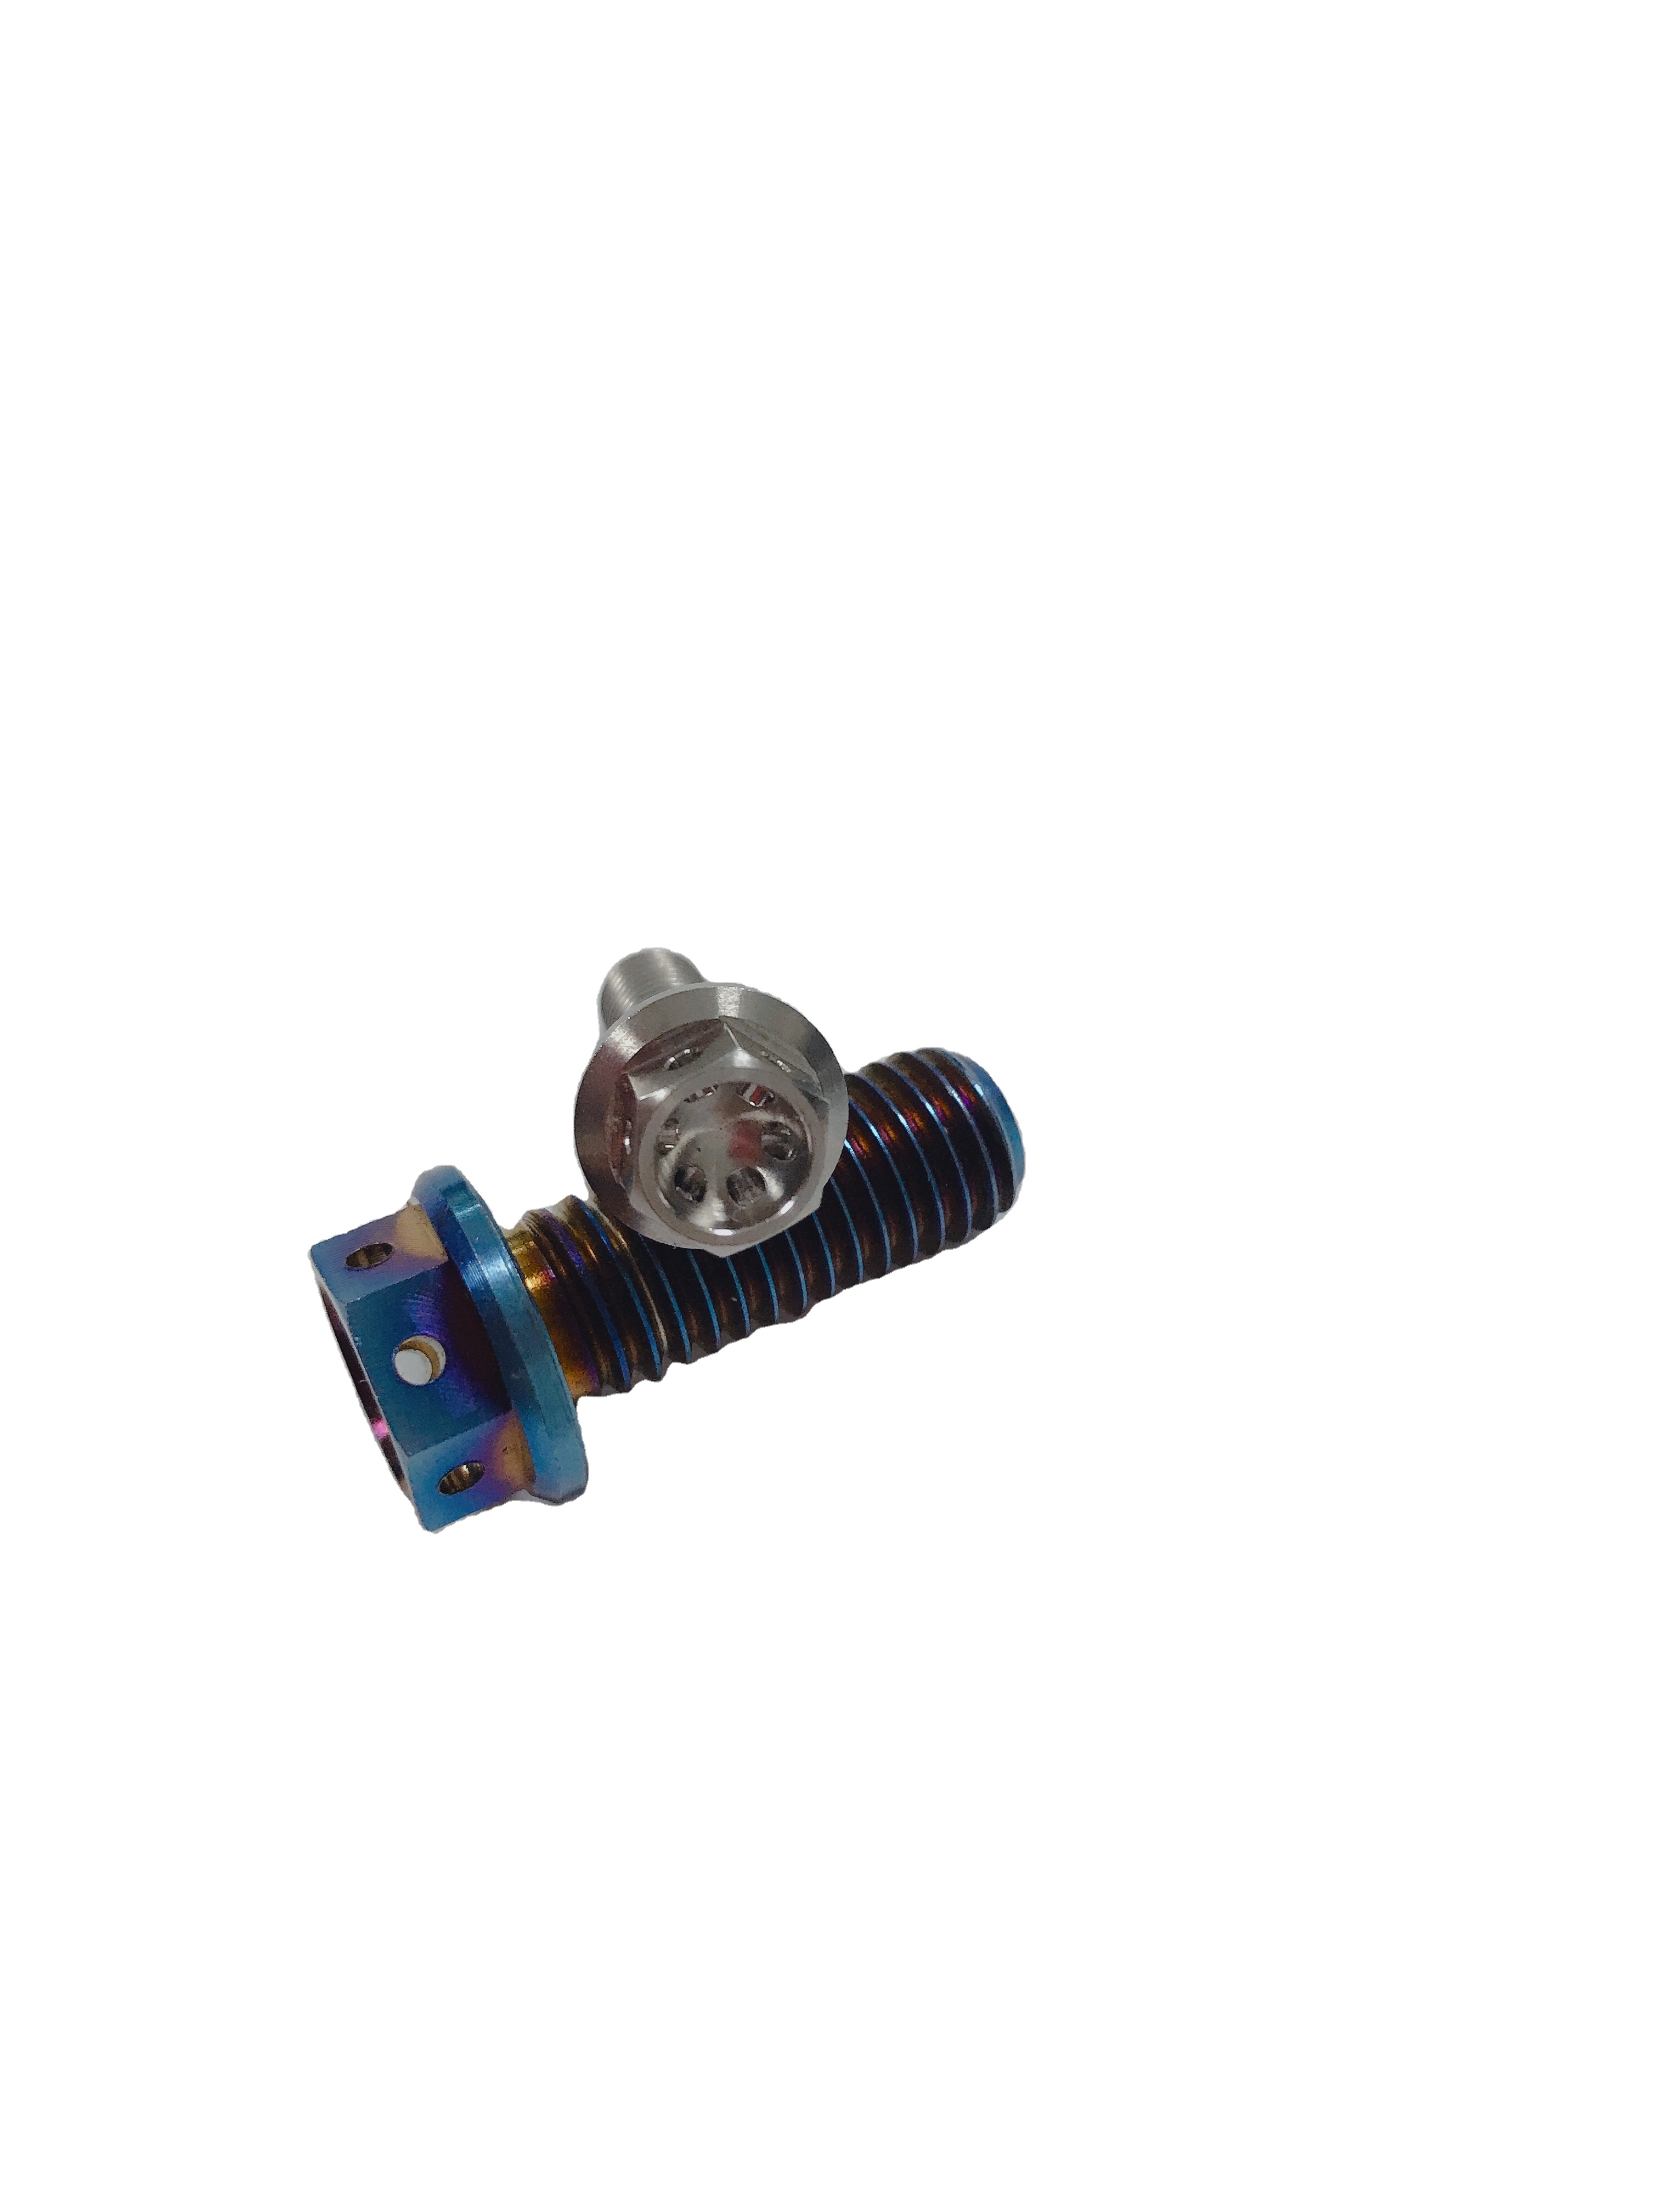
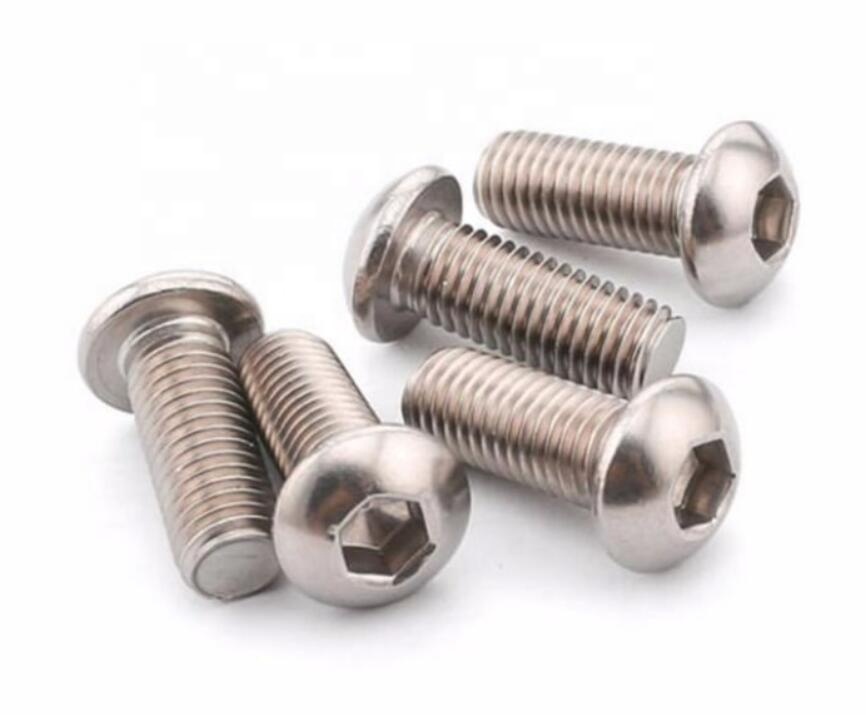

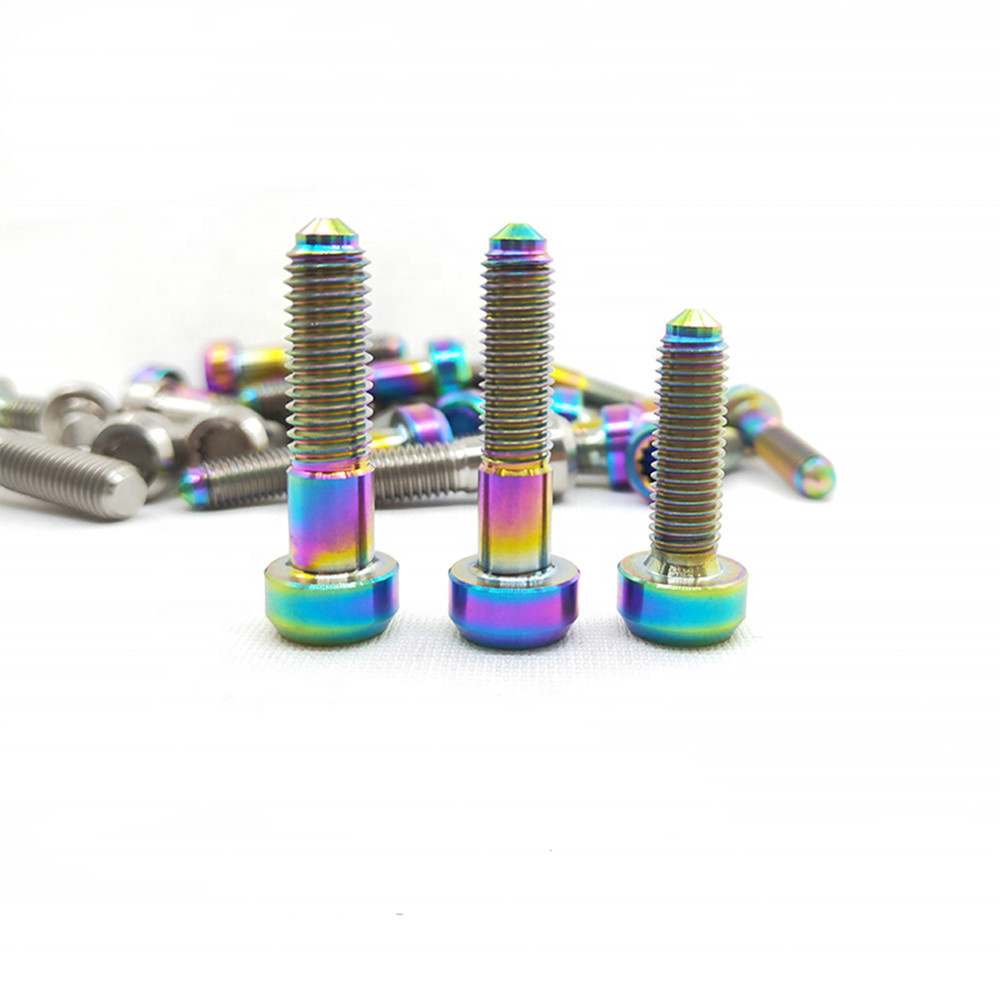
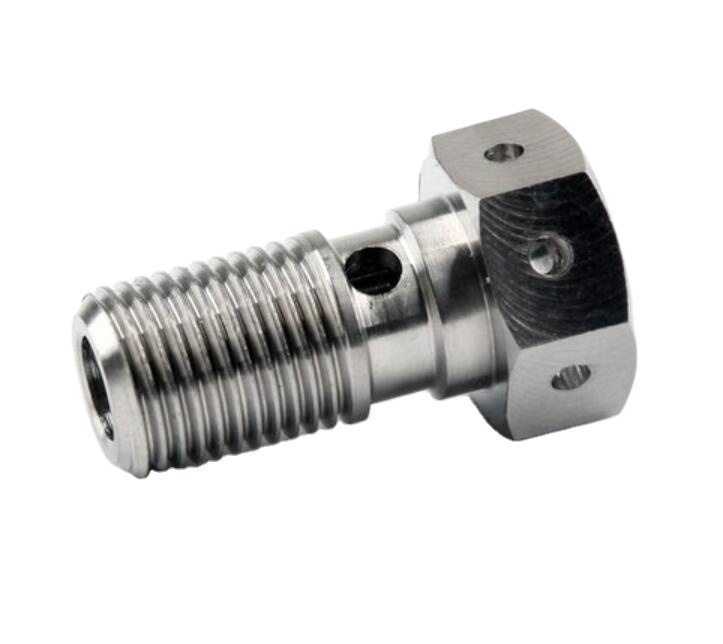
Modern internal combustion architecture, experimental aerospace thrusters, and hypersonic propellant valve assemblies designed across the South Bay corridor—from San Jose down to Santa Clara and Sunnyvale—face an identical physical bottleneck: valve float induced by inertial reciprocating mass. When valvetrain assemblies operate at speeds exceeding 9,000 RPM, the kinetic energy of standard chrome-moly or alloy steel spring retainers, cotters, and keepers creates inertia overshoots that cause erratic valve timing, parasitic seat bounce, and rapid seat recession.
By leveraging certified Ti-6Al-4V (Grade 5, AMS 4928) titanium alloy produced in Baoji—widely acknowledged as China’s Titanium Valley—system engineers achieve a dramatic 44% mass reduction compared to 4140 steel, while retaining a yield strength of ≥ 828 MPa. The mechanical resonance frequency shifts beyond standard vibration bands, virtually extinguishing harmonic resonance within the valve spring pocket.
Direct sourcing from our Gaoya Village facility allows OEM tier-1 builders in Northern California to bypass costly intermediary markups while maintaining 100% material traceability from certified sponge titanium to finished multi-axis turned hardware.

Deploying precision Grade 5 and Grade 2 titanium valve hardware across high-tech hardware testbeds, performance motorsports stables, and next-gen electric powertrain labs in Silicon Valley.
Silicon Valley's next-generation EV powertrain prototypes require ultra-lightweight, non-magnetic thermal management valves. Grade 5 titanium hardware withstands aggressive dielectric coolants and high thermal gradients without galvanic corrosion or embrittlement.
Engine builders around San Jose and Laguna Seca rely on custom 10-degree valve retainers, 12-point manifold studs, and lightweight titanium keepers to prevent valve drop during sustained high-rev runs across open-wheel circuit and drag events.
San Jose’s burgeoning aerospace startups demand low-mass fluid delivery components. Our CNC Grade 5 and ELI Grade 23 valve seats and retainers maintain ductility at cryogenic liquid nitrogen and methane handling temperatures down to -196°C.
Silicon Valley hardware engineering teams are migrating away from static domestic wholesale brokers toward agile, factory-direct manufacturing partnerships that deliver rapid precision iterations.
| Evaluation Parameter | Traditional Regional Broker (US Local) | Vunza Factory Direct (Baoji to San Jose) | Technical Impact for Bay Area OEMs |
|---|---|---|---|
| Lead Times (Custom DFM) | 12 to 16 Weeks (Multi-tier reselling) | 2 to 3 Weeks (First Article CNC Samples) | Accelerates prototype test cycles by 70% in agile labs. |
| Raw Material Traceability | Variable, fragmented documentation | 100% Vacuum Arc Remelt (VAR) Sponge to Part | Passes incoming metallurgical and AS9100 quality audits. |
| Machining Precision Range | Typically ±0.05 mm standard | Tight down to ±0.005 mm (5-Axis Multi-axis) | Eliminates micro-galling on valve guides and seating faces. |
| Surface Modification Options | Subcontracted / standard natural finish | In-house Micro-polish, PVD, Hard Anodizing | Reduces kinetic coefficient of friction (μ) to ≤ 0.15. |
| Total Procurement Cost | Includes 200–350% domestic distributor margin | Ex-Factory direct competitive volume pricing | Reduces bill-of-materials costs on performance runs. |
Headquartered adjacent to the legendary Baoti Industrial Park in Baoji, Shaanxi, our factory integrates advanced CNC engineering, rigorous material testing, and export-proven quality systems since 2008.
We source high-purity titanium sponge within Baoji's ecosystem, verifying chemistry and mechanical integrity through accredited mill test certificates with each production batch.
Our machining fleet includes 3-axis, 4-axis, and 5-axis centers that hold micro-tolerances down to 0.005 mm on complex valve retainers, split rim hardware, and high-flow impellers.
Over 50% of our production staff have more than 13 years of specialized titanium machining experience, effectively preventing work-hardening and tool chatter on demanding alloys.
Tailored to Pacific Time (PT) working hours, our direct engineering team reviews 2D/3D CAD models within 9 hours, giving fast DFM feedback to ensure production feasibility.
Practical insights addressing international logistics, custom machining specs, anti-galling coatings, and import compliance for California enterprises.