EDC Gear
Aerospace-grade Ti-6Al-4V Grade 5 fasteners, studs, and custom components manufactured in Baoji, China with direct B2B export solutions for Las Vegas race shops and performance distributors.
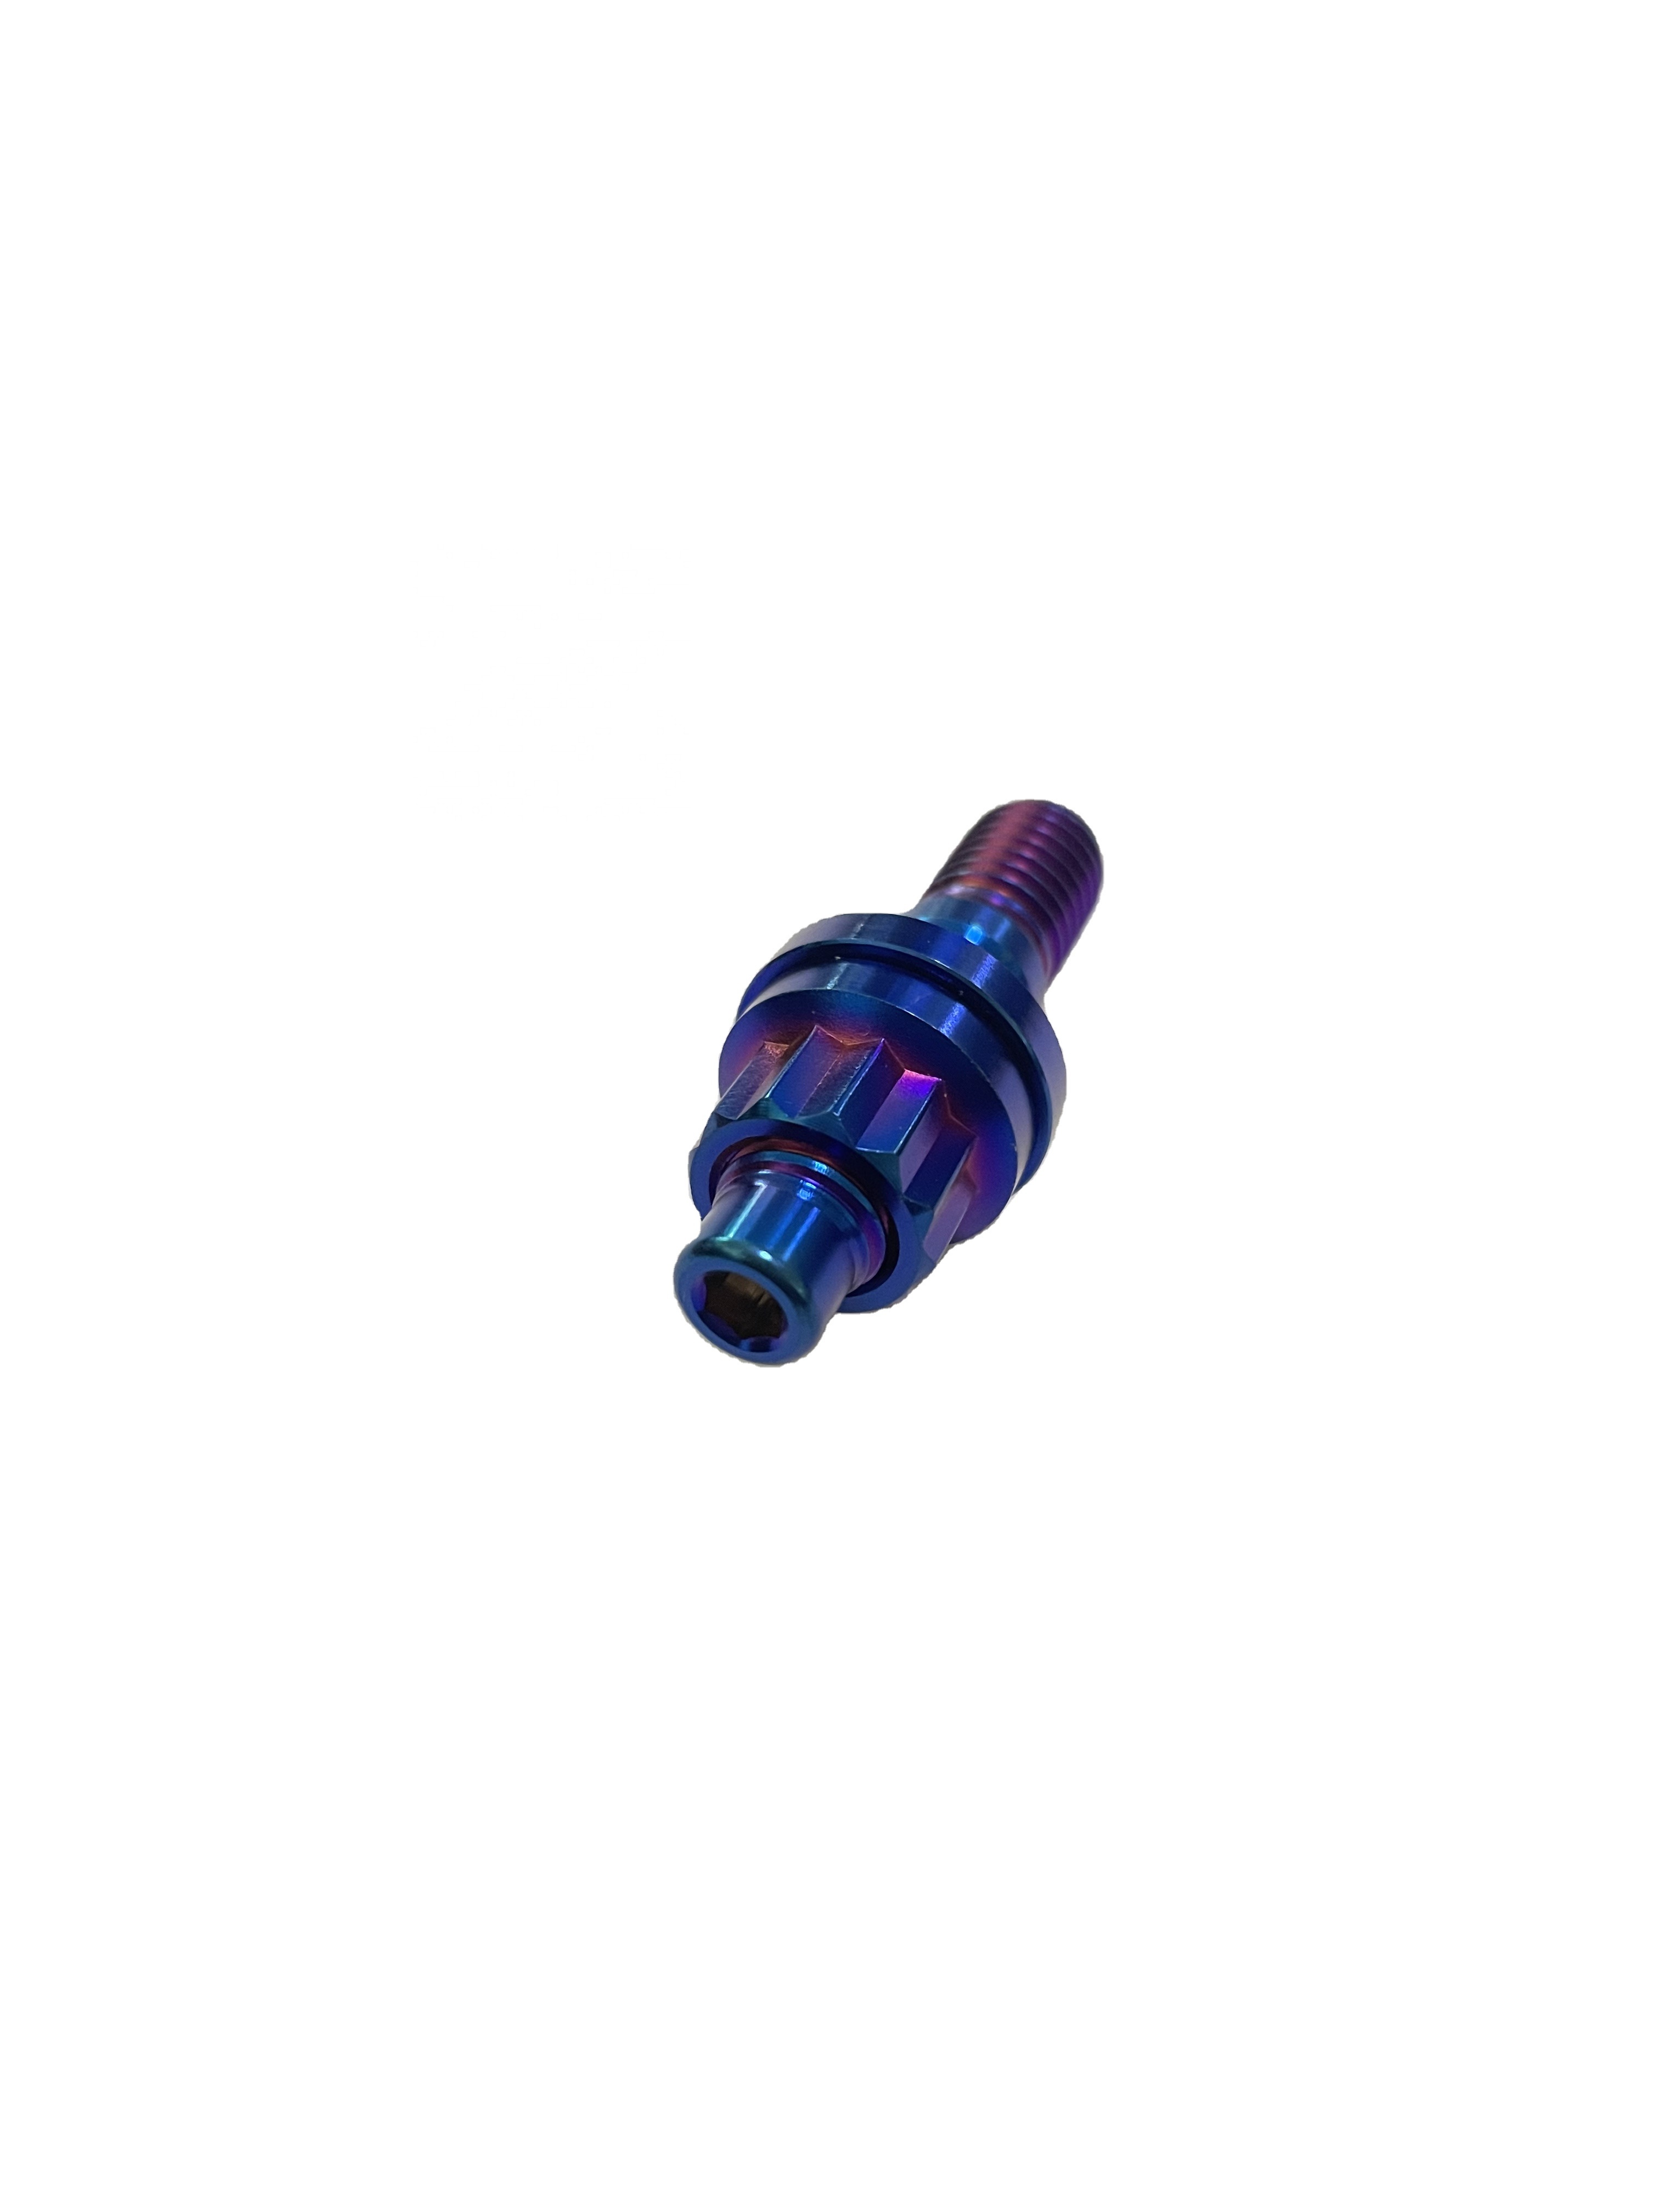
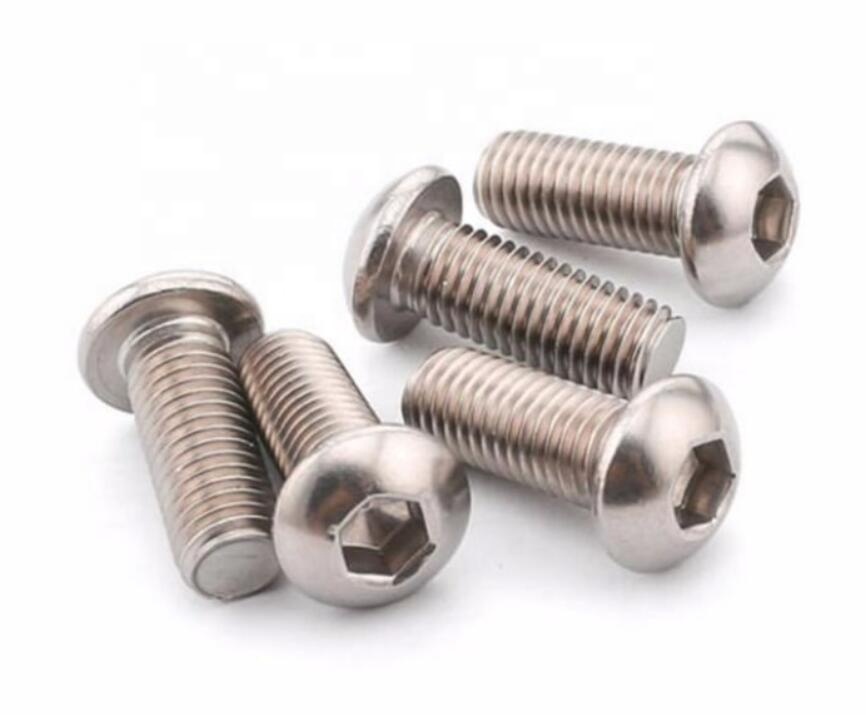
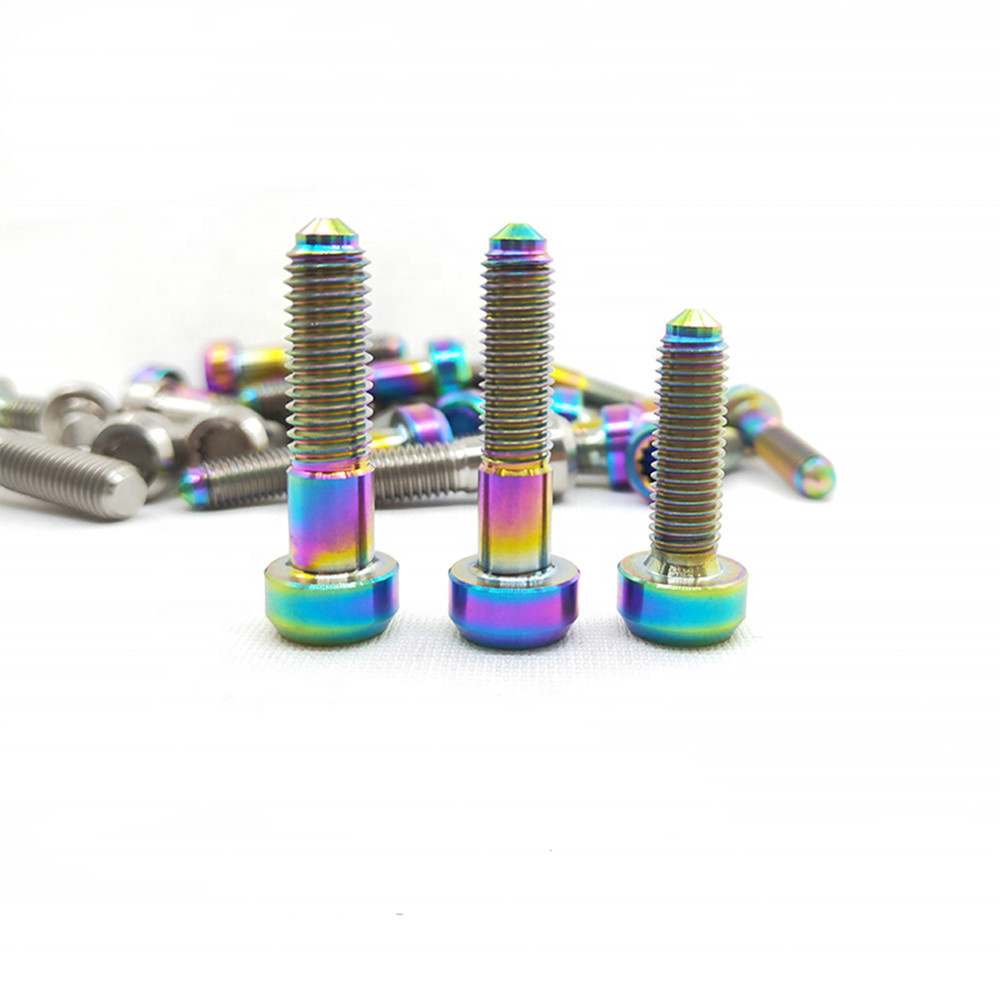
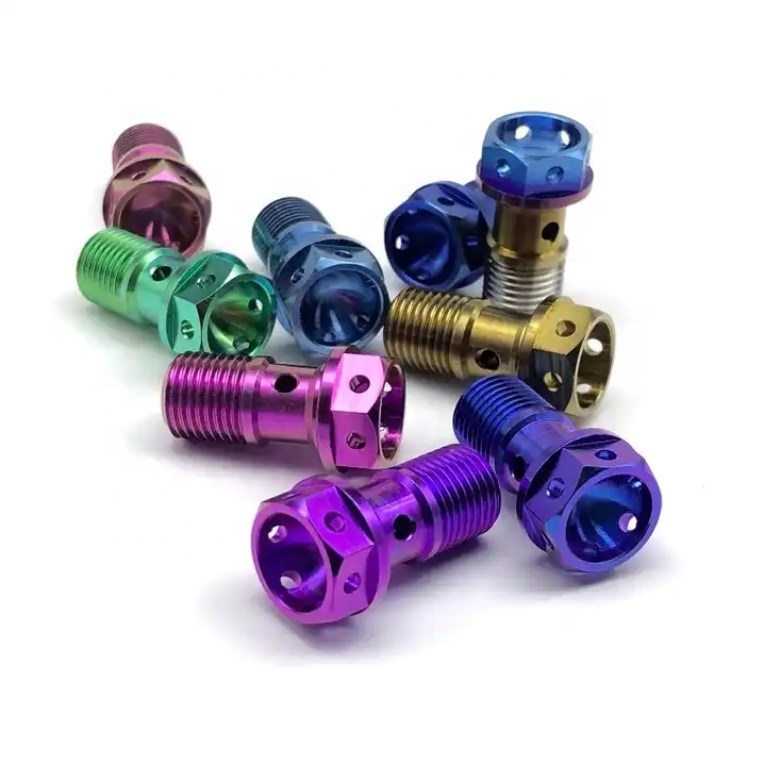
The greater Las Vegas metropolitan area, anchored by the internationally celebrated SEMA Show (Specialty Equipment Market Association) at the Las Vegas Convention Center, the roaring oval and drag strips of the Las Vegas Motor Speedway (LVMS), and the gruelling desert terrain of the Mint 400, represents one of North America's most demanding proving grounds for ultra-high-performance mechanical fasteners. While high-tensile 8740 chromoly and H-11 tool steels have historically dominated aftermarket wheel hubs, exhaust flanges, and cylinder head studs, the relentless search for unsprung rotating mass reduction coupled with elevated operating temperatures has accelerated the adoption of Grade 5 Titanium (Ti-6Al-4V, UNS R56400).
Operating in the arid, high-temperature Mojave Desert climate imposes extreme cyclic thermal loading upon internal combustion hardware. Forced-induction powertrains tuned for competitive drifting, drag racing, and desert Trophy Truck sprints generate exhaust gas temperatures (EGT) frequently surpassing 850°C (1,562°F). Under these intense thermal expansions, conventional steel studs exhibit unequal thermal growth relative to aluminum cylinder heads and turbocharger turbine housings, precipitating chronic flange warping, micro-galling, and fastener stretch failure. Our Baoji-manufactured titanium stud kits resolve this mechanical mismatch by providing a coefficient of thermal expansion (8.6 × 10⁻⁶/K) closely mirroring billet and cast aircraft aluminum, preventing clamping load loss and catastrophic blown manifold gaskets during grueling race conditions.
Engineered specifically for the exacting standards of professional motorsport teams, luxury customizers, and aerospace contractors based in Southern Nevada.
At LVMS's dirt track and paved tri-oval, un-sprung rotating weight is the single biggest enemy of throttle response and lateral tire grip. By replacing standard carbon steel hub wheel studs and bumper bolts with our forged 10-32 UNF & M12/M14 titanium wheel stud conversion systems, race engineers remove 44% of rotational fastener mass. The reduction directly decreases gyroscopic inertia, allowing sharper steering transitions, cooler brake rotor discs, and improved tire wear across multi-lap heat endurance cycles.
Motorsport & Short Track OvalThe southern Nevada desert subjects off-road suspensions to continuous high-G washboard vibrations, 115°F ambient heat, and abrasive silica dust. Our Gr5 titanium heim joint rod end bearings, caliper mount bolts, and suspension links undergo precision cold rolling of thread roots. This continuous grain flow eliminates the stress concentration micro-notches typical of cut threads, offering exceptional fatigue life that prevents suspension detachment across 400 miles of unforgiving desert terrain.
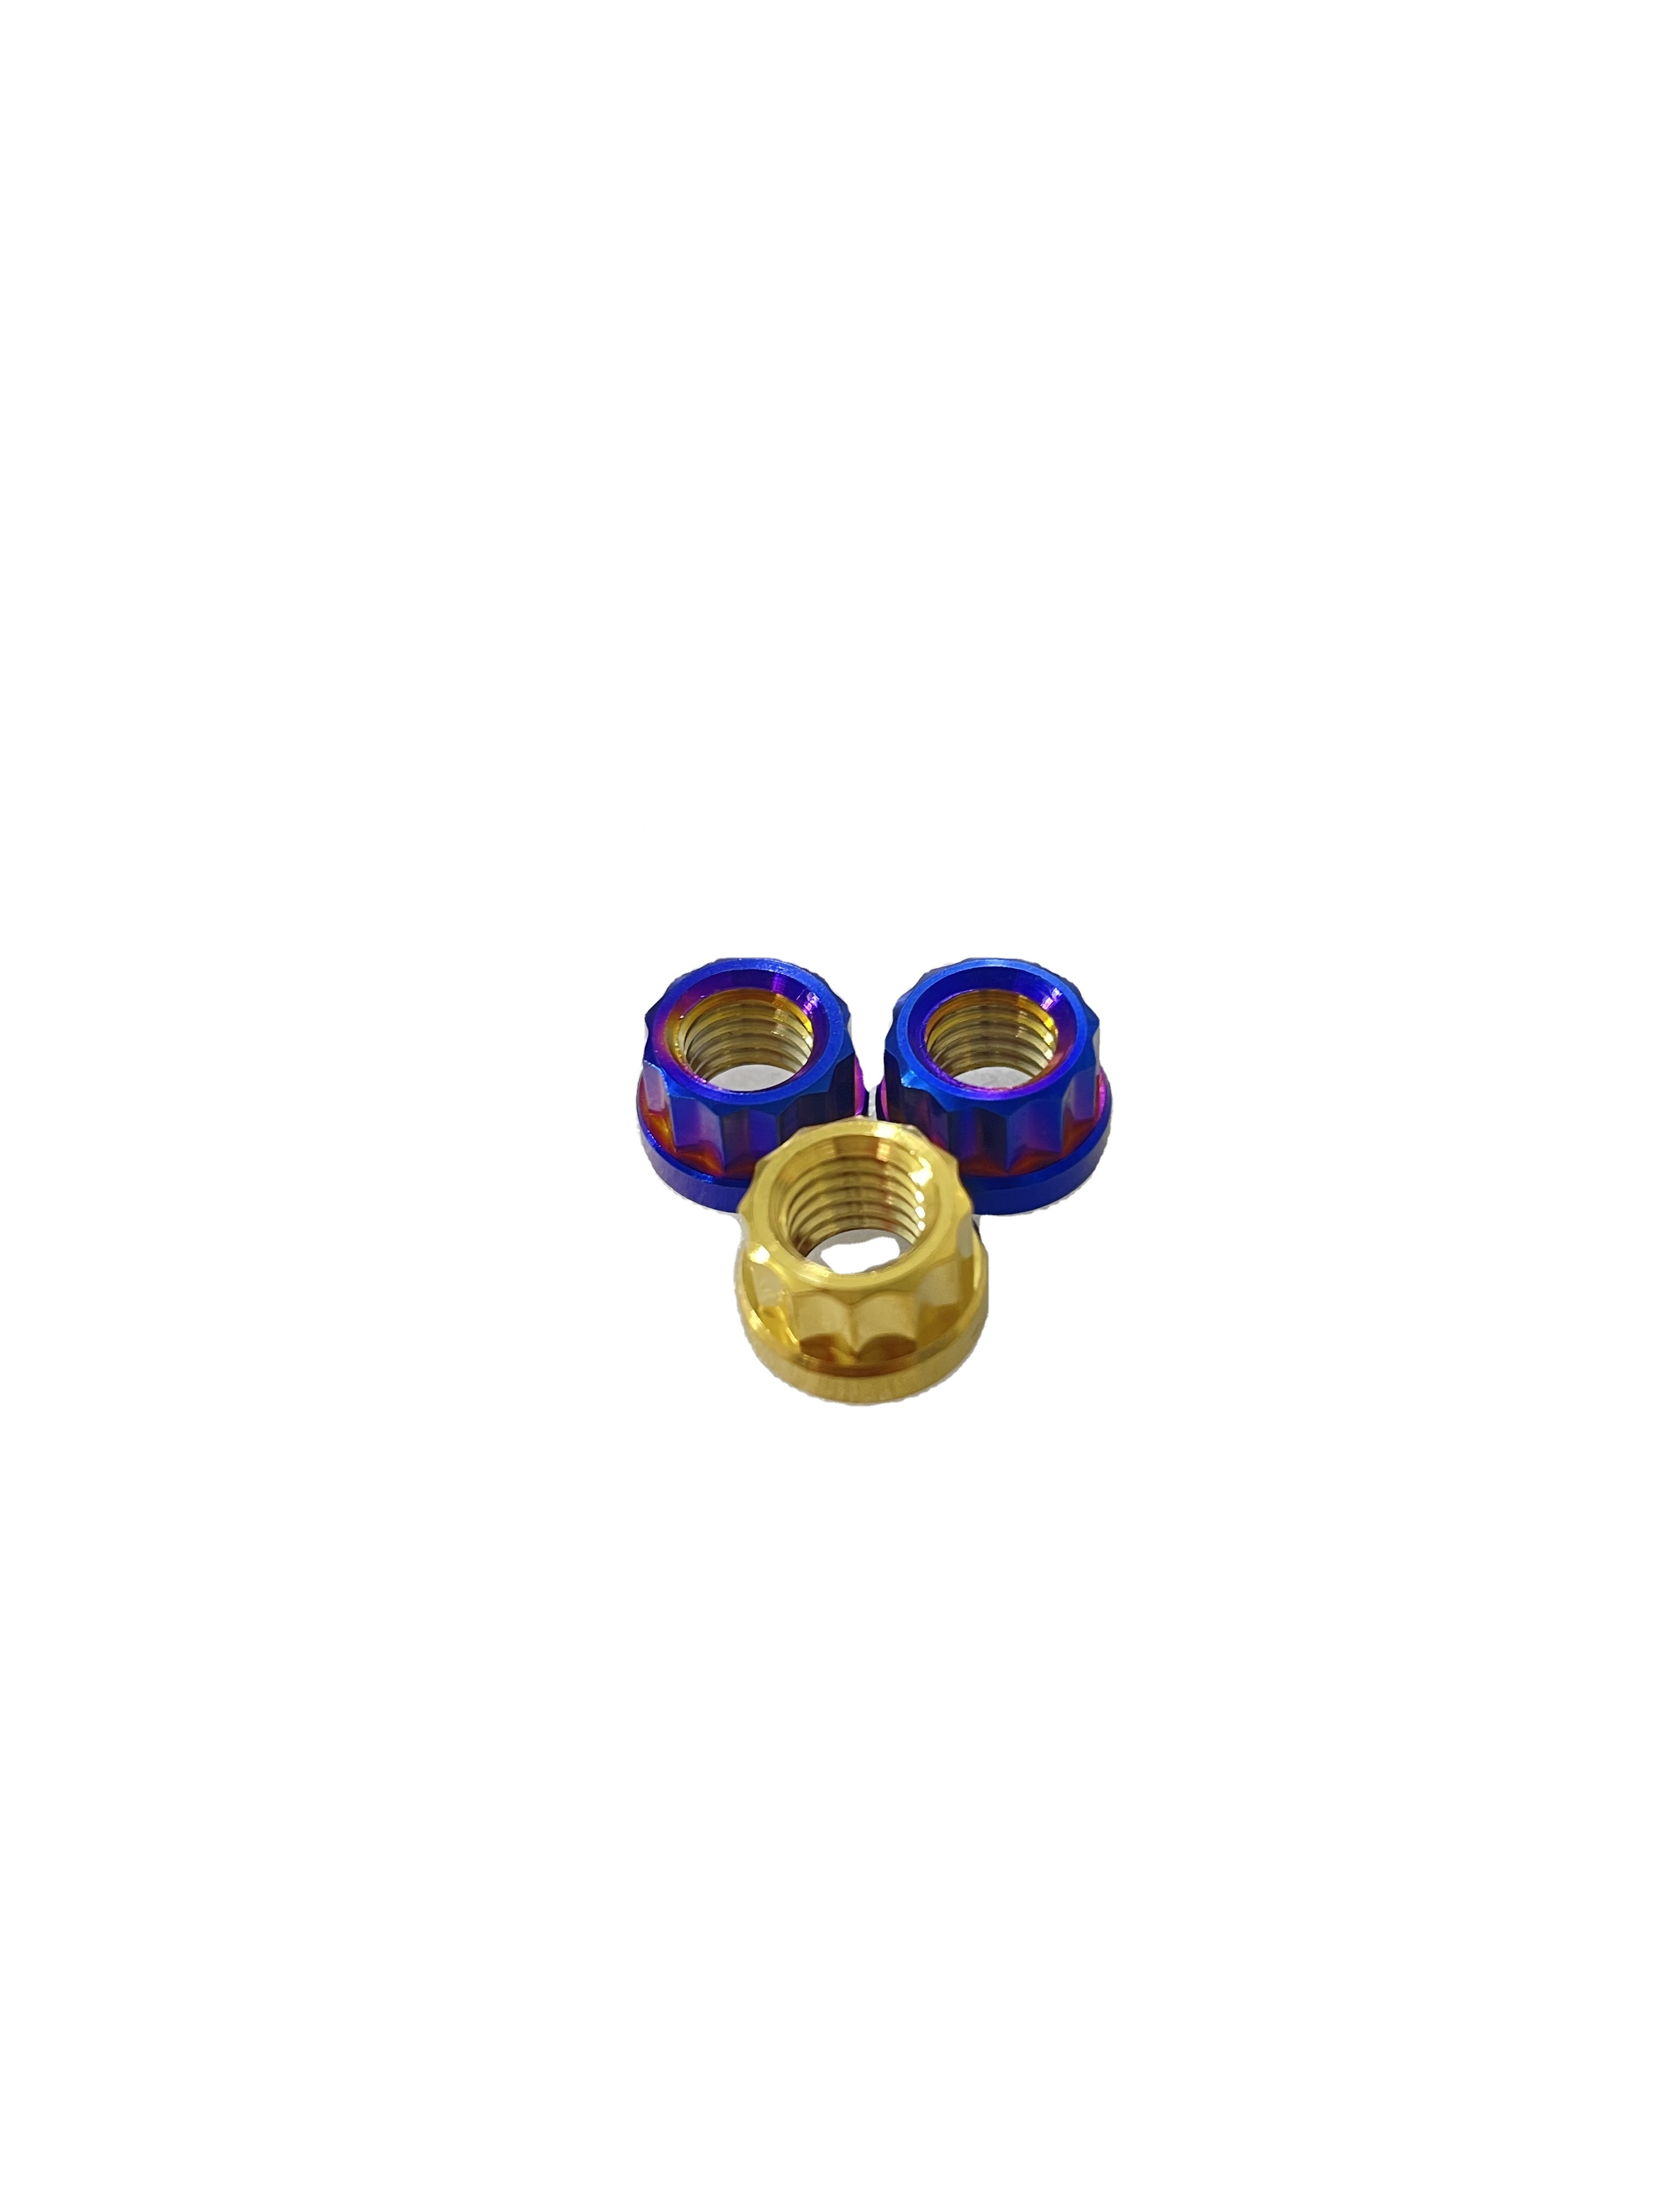
Off-Road EnduranceExotic European platforms (Porsche GT3, McLaren, Lamborghini Huracán) and high-end SEMA project builds demanding immaculate aesthetics without compromising track integrity rely on our PVD Nitride and Anodized 12-Point Titanium Lug Nuts & Split Rim Bolts. Resistant to road salt, brake dust wash acids, and extreme wheel hub temperatures, these fasteners retain their brilliant cosmetic finish and tensile integrity permanently without the pitting typical of chrome-plated steel.
Aesthetic Perfection & SEMA ShowValidated data for Nevada mechanical engineers comparing yield strengths, thermal tolerances, and density weight savings.
| Mechanical Property | Vunza Baoji Gr5 Ti-6Al-4V (TC4) | ARP 8740 Chrome Moly Steel | Grade 10.9 Carbon Steel | 316 Marine Stainless Steel |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 g/cm³ (-44% Mass) | 7.85 g/cm³ | 7.84 g/cm³ | 8.00 g/cm³ |
| Tensile Strength (MPa) | 950 – 1050 MPa | 1240 – 1380 MPa | 1000 – 1040 MPa | 580 – 620 MPa |
| Yield Strength (0.2% Offset) | 880 – 920 MPa | 1100 – 1250 MPa | 900 – 940 MPa | 240 – 290 MPa |
| Fatigue Endurance Limit | Superior (Smooth Root Radius) | High (Susceptible to H-embrittlement) | Moderate | Low |
| Thermal Expansion (×10⁻⁶/K) | 8.6 (Matches Aluminum Heads) | 12.2 | 11.7 | 16.0 |
| Corrosion & Oxidation Resistance | Permanent (TiO₂ Passive Layer) | Requires Plating (Prone to Rust) | Requires Zinc/Phosphate Coating | Moderate (Pitting in Chlorides) |
| Magnetic Permeability | Non-Magnetic (µr ≈ 1.00005) | Ferromagnetic | Ferromagnetic | Slightly Magnetic when Cold Worked |
Key procurement shifts shaping how Las Vegas distributors, aftermarket fabricators, and racing enterprises secure Asian supply chains.
With Nevada emerging as a national hub for battery gigafactories and electric hypercar tuning, non-magnetic titanium fasteners are replacing steel to avoid electromagnetic interference and provide fire-safe clamping for high-density battery racks.
EV Powertrain EvolutionLas Vegas racing speed shops are increasingly bypassing expensive domestic repackagers. Direct OEM partnership with certified Chinese manufacturing facilities reduces fastener procurement expenses by 35% to 50% while preserving identical aerospace MTR standards.
Supply Chain OptimizationFollowing high-profile fastener shear recalls in competitive drifting and drag competitions, regional builders now demand 3.1 Mill Test Certificates verifying sponge titanium provenance, low hydrogen/oxygen interstitial content, and zero porosity inclusions.
Quality VerificationDesert dust contains sharp microscopic quartz grains. Local fabricators insist on specialized PVD (Physical Vapor Deposition) Titanium Nitride (gold) and DLC (Diamond-Like Carbon) coatings, eliminating thread galling during rapid pneumatic pit-stop tire swaps.
Surface MetallurgyDeep industrial roots in China's Titanium Valley, combining virgin raw material metallurgy with multi-axis CNC micro-machining.
Situated in the Gaoya Village Industrial Zone, Baoji, Shaanxi, our facility operates in direct proximity to the Baoti Group industrial ecosystem. This geographical dominance gives us unhindered access to top-grade aerospace sponge titanium, cutting raw material delays and safeguarding structural purity from ingots to finished threaded fasteners.
Our workshop houses 34 sets of 3, 4, and 5-axis high-speed CNC turning and milling centers capable of holding tolerances down to ±0.005 mm. Rather than cutting external threads, we employ multi-ton hydraulic thread-rolling dies that compress and align grain structures for unmatched fatigue resistance under cyclical loads.
From spectrometry verification of incoming Grade 5 (Ti-6Al-4V) billets to final optical comparator profile measurement, each production run receives a comprehensive batch inspection dossier. Over 50% of our production team possesses more than 13 years of specialized precision machining experience in high-temperature titanium alloys.
Addressing commercial, engineering, and logistical queries regarding titanium fastener importation from China into Nevada.
Titanium and aluminum have a natural tendency toward friction welding or adhesive galling when mated dry under high torque, a phenomenon accelerated by the dry, 100°F+ temperatures of Las Vegas summers. To completely negate thread seizure, our titanium studs feature rolled, mirror-micro-finished threads (Ra < 0.4 µm). We advise using a molybdenum disulfide or nickel-based anti-seize lubricant during assembly. Furthermore, our PVD-coated studs (featuring Titanium Nitride or DLC) present a ceramic barrier that exhibits a friction coefficient under 0.15, guaranteeing accurate torque tension transfer and repeat serviceability without thread stripping.
Cut threads are machined using cutting inserts that sever the metal's internal grain lines, creating microscopic stress risers and sharp micro-notches at the thread roots where cyclic fatigue cracks initiate under boost. In contrast, our threads are hydraulically rolled under controlled pressure using hardened dies. This plastic deformation cold-works the root radius, burnishes the flanks, and curves the titanium grain lines continuously around the thread profile, boosting dynamic fatigue lifespan by over 300% compared to cut fasteners.
For standard catalog fasteners, orders ship within 48 to 72 hours. For custom CNC machining to print (e.g., custom step-down studs or proprietary 12-point heads), tooling setup, sample approval, and production run typically take 15 to 20 working days. We provide express door-to-door air freight (via DHL, FedEx, or UPS Priority) delivering directly to your Las Vegas, Henderson, or North Las Vegas warehouse within 4 to 6 business days. All shipments include commercial invoices, packing lists with correct HS codes (7318.15 / 8108.90), and formal 3.1 Material Test Reports to ensure effortless U.S. Customs clearance.
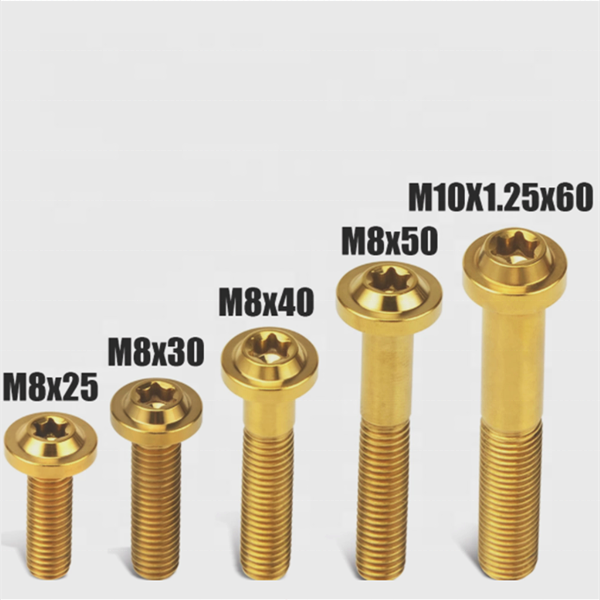
Yes. Although we produce thousands of metric items (M6, M8, M10, M12, M14) for imported platforms, our multi-axis CNC machines and rolling dies routinely manufacture American Unified threads, including 10-32 UNF, 1/4-20 UNC, 3/8-24 UNF, 1/2-20 UNF, and 5/8-18 wheel studs commonly found in sprint cars, NHRA dragsters, and domestic V8 muscle platforms. We can conform to standard ANSI/ASME B1.1 Class 2A/3A or execute bespoke pitch-diameter tolerances based on your 2D CAD/3D STEP drawings.
To support emerging race teams, boutique chassis builders, and SEMA project fabricators, we offer flexible MOQ tiers. Stocked titanium exhaust stud kits, 12-point nuts, and motorcycle bolts have low MOQs of 50 to 100 units. For fully bespoke CNC parts crafted from proprietary drawings, prototype sample batches start at only 10 to 20 units, scaling seamlessly up to multi-thousand piece production runs for wholesale distributors.
Every single heat of titanium bar stock undergoes rigorous chemical composition spectrometry and tensile mechanical testing in accordance with ASTM B348 (Grade 5 Ti-6Al-4V) standards. We verify low gas contents (Carbon ≤ 0.08%, Iron ≤ 0.25%, Oxygen ≤ 0.20%, Nitrogen ≤ 0.05%, Hydrogen ≤ 0.0125%). We supply mill certificates, hardness test records (32–38 HRC), and dimensional CMM inspection reports upon request with every batch shipment.
Send your 2D/3D component drawings, race-spec requirements, or annual supply forecasts. Our senior metallurgical engineers respond with design-for-manufacturing (DFM) feedback and competitive factory-direct pricing within 9 hours.