Precision-Machined Titanium Engine Hardware
Direct factory supply of certified Grade 5 (Ti-6Al-4V / TC4) fasteners, hot-forged and precision CNC-turned to standard metric and imperial thread profiles for high-temperature and extreme-vibration environments.
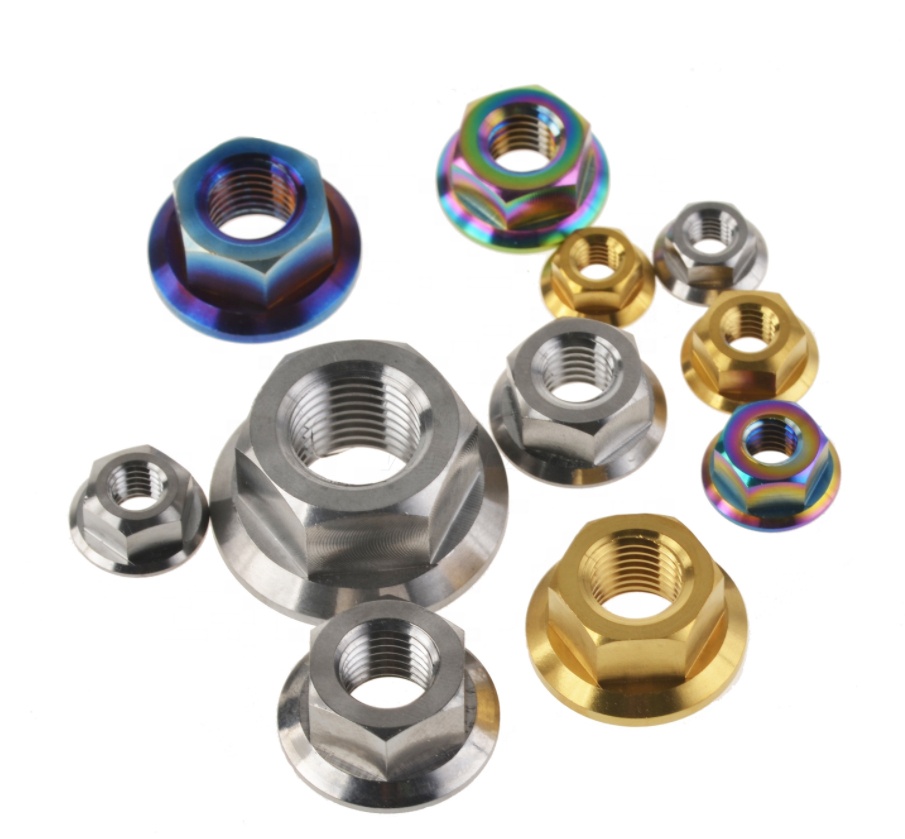
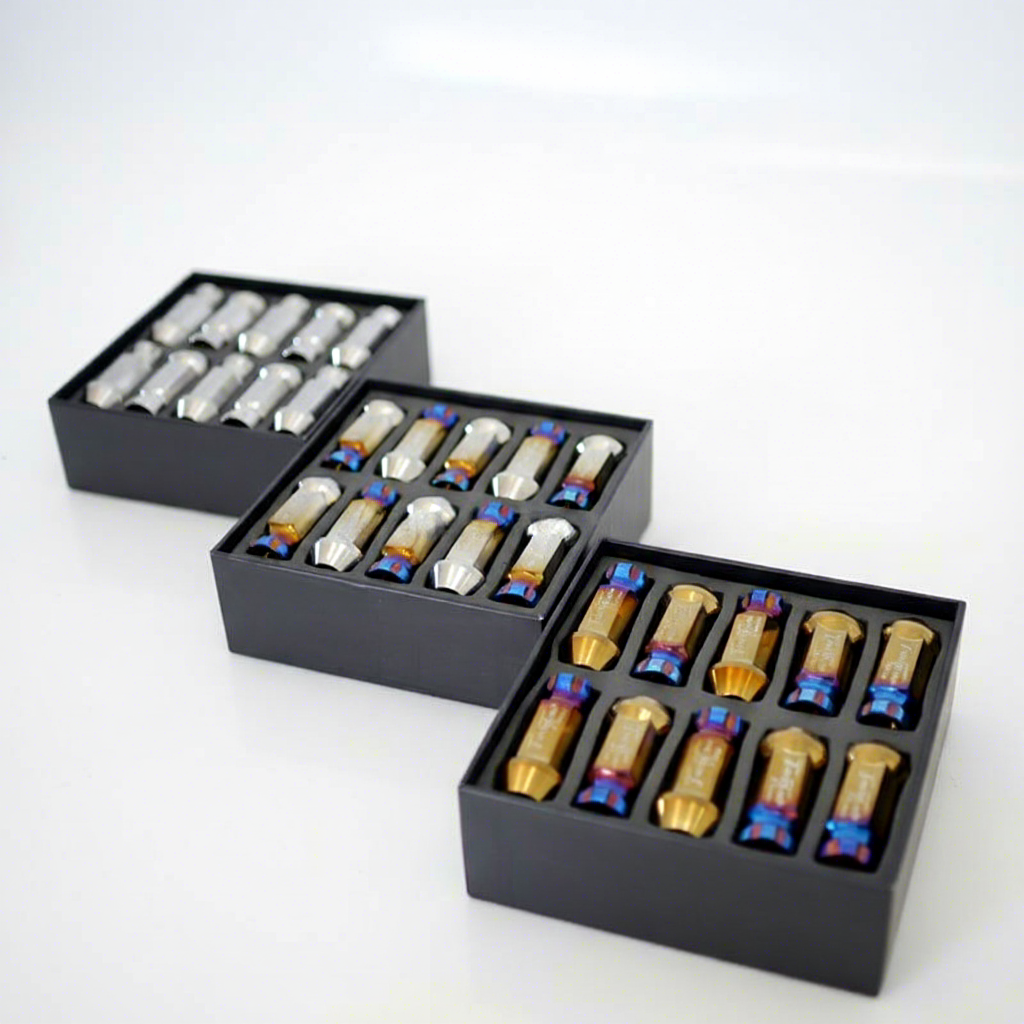
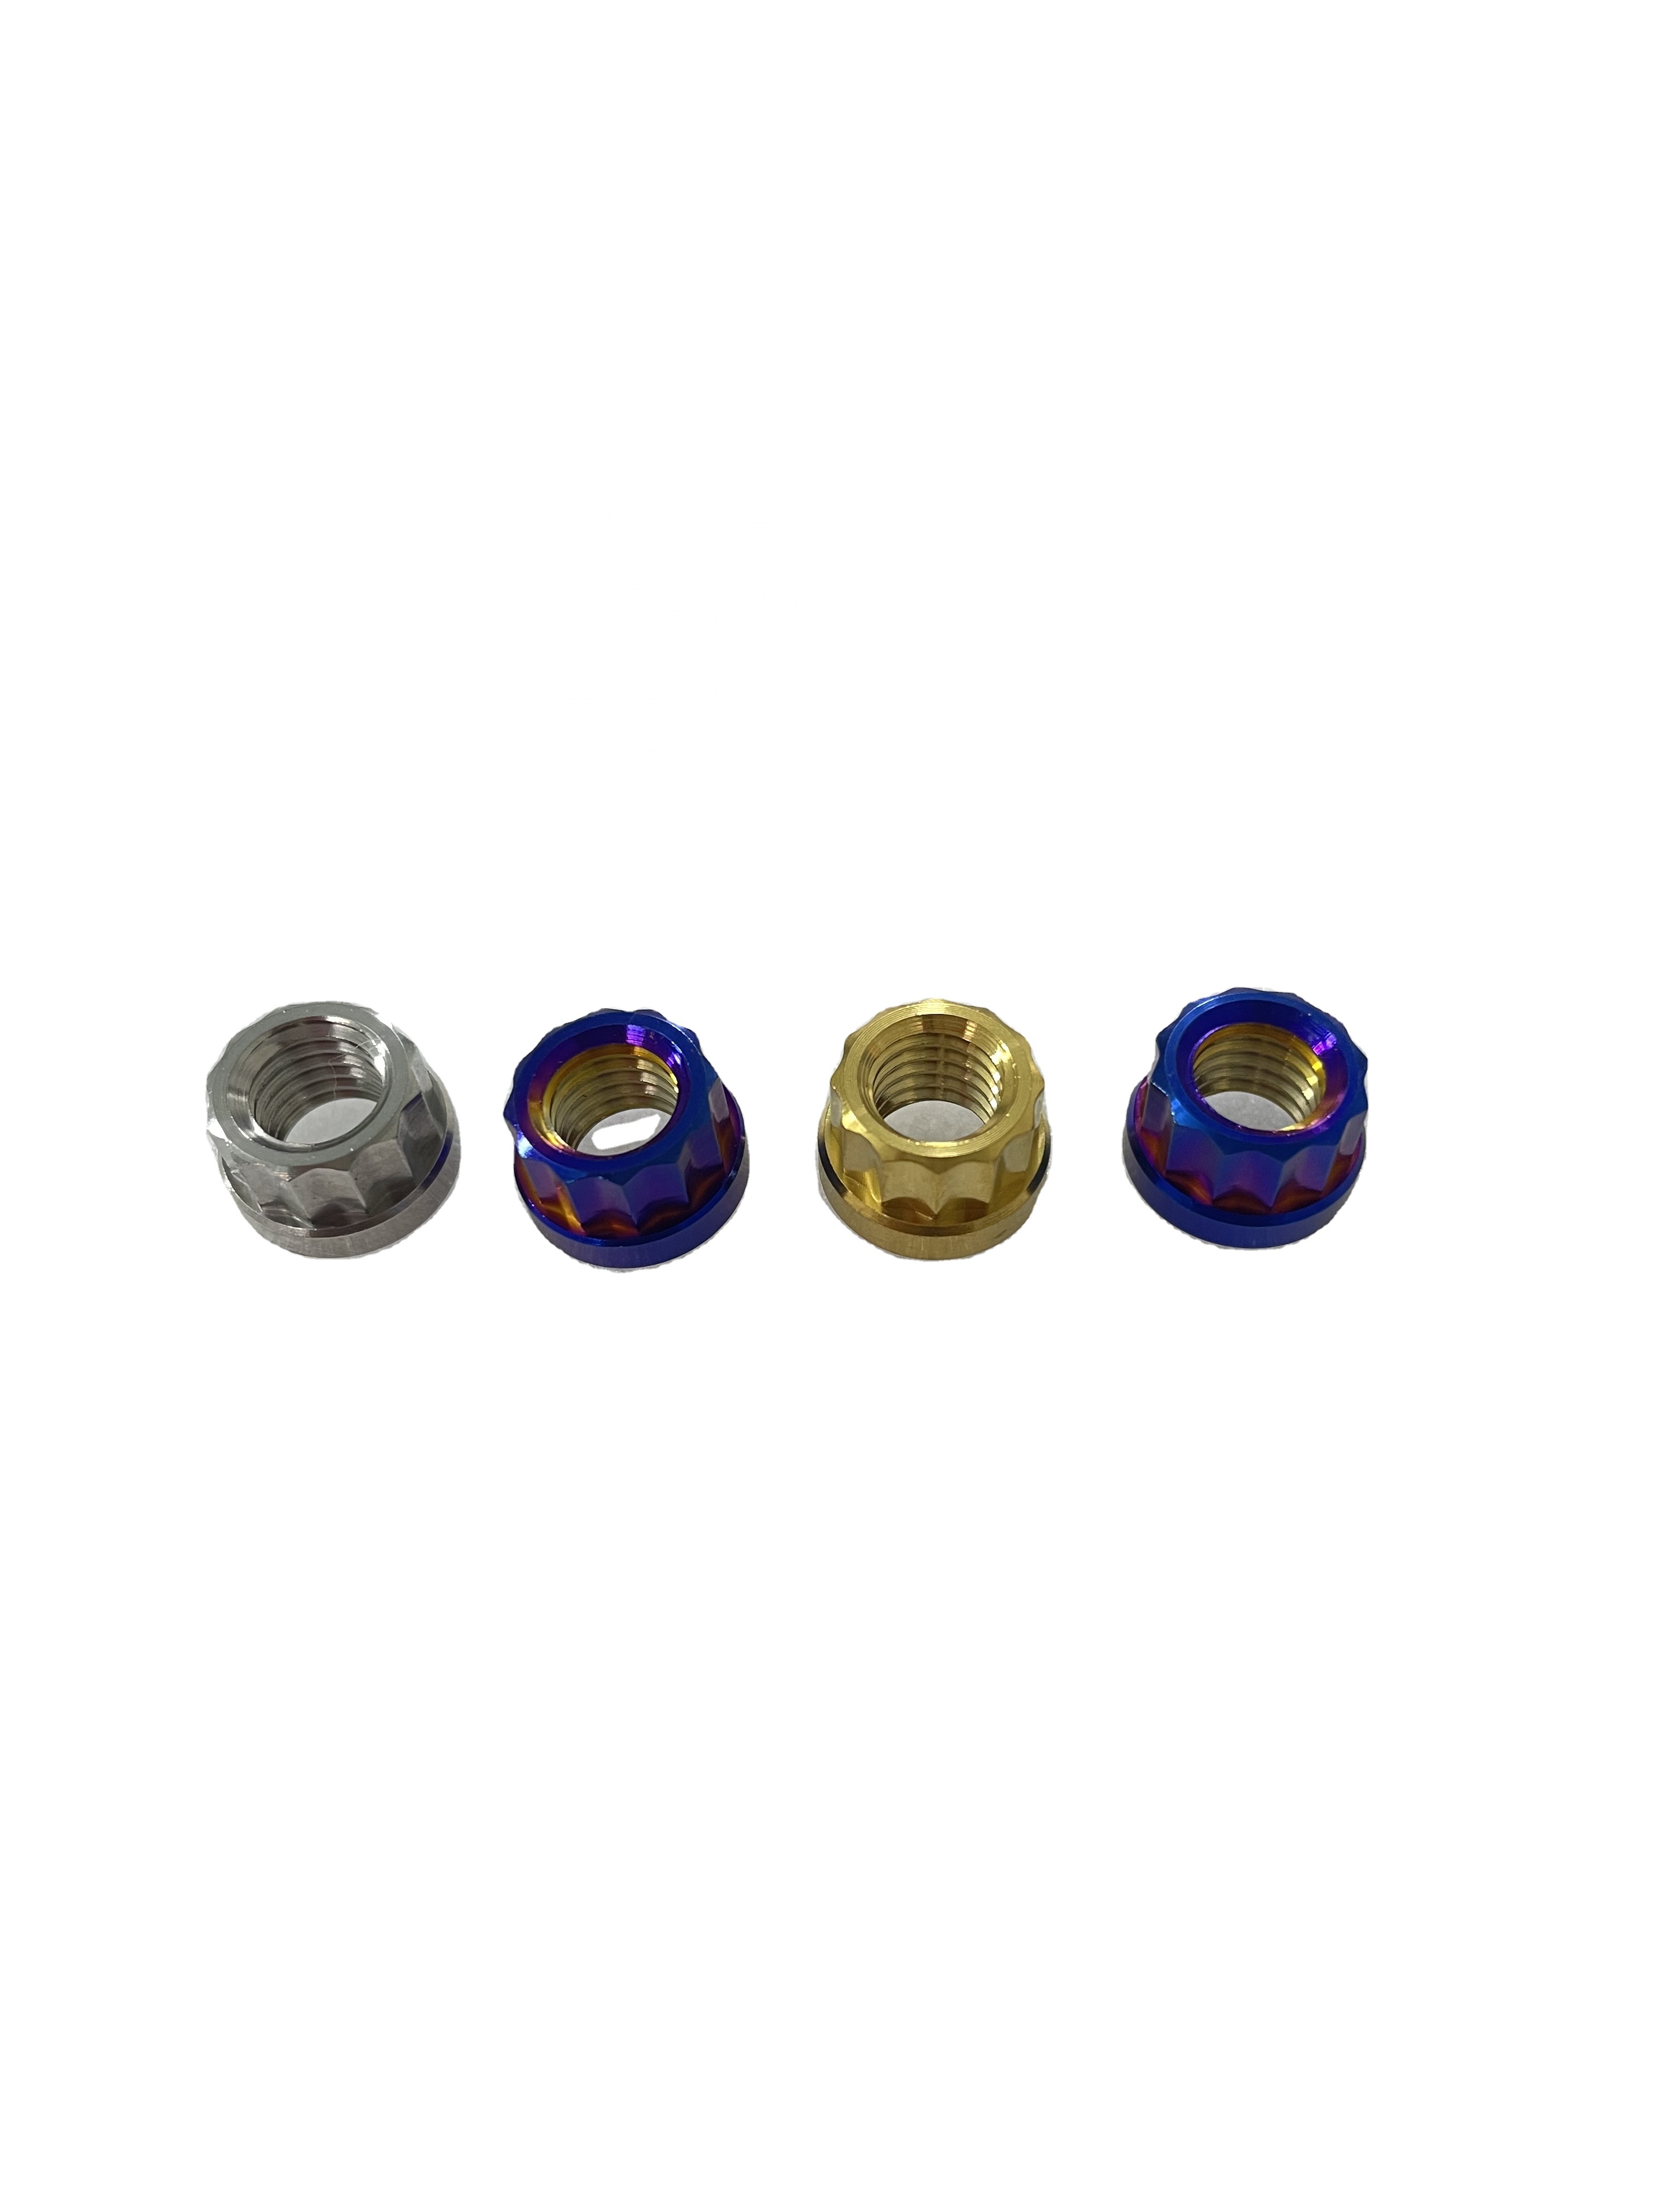
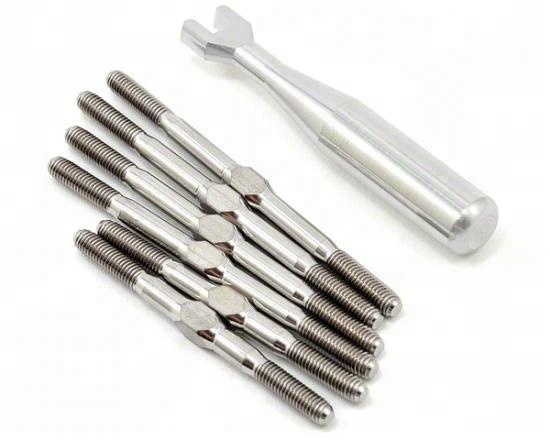
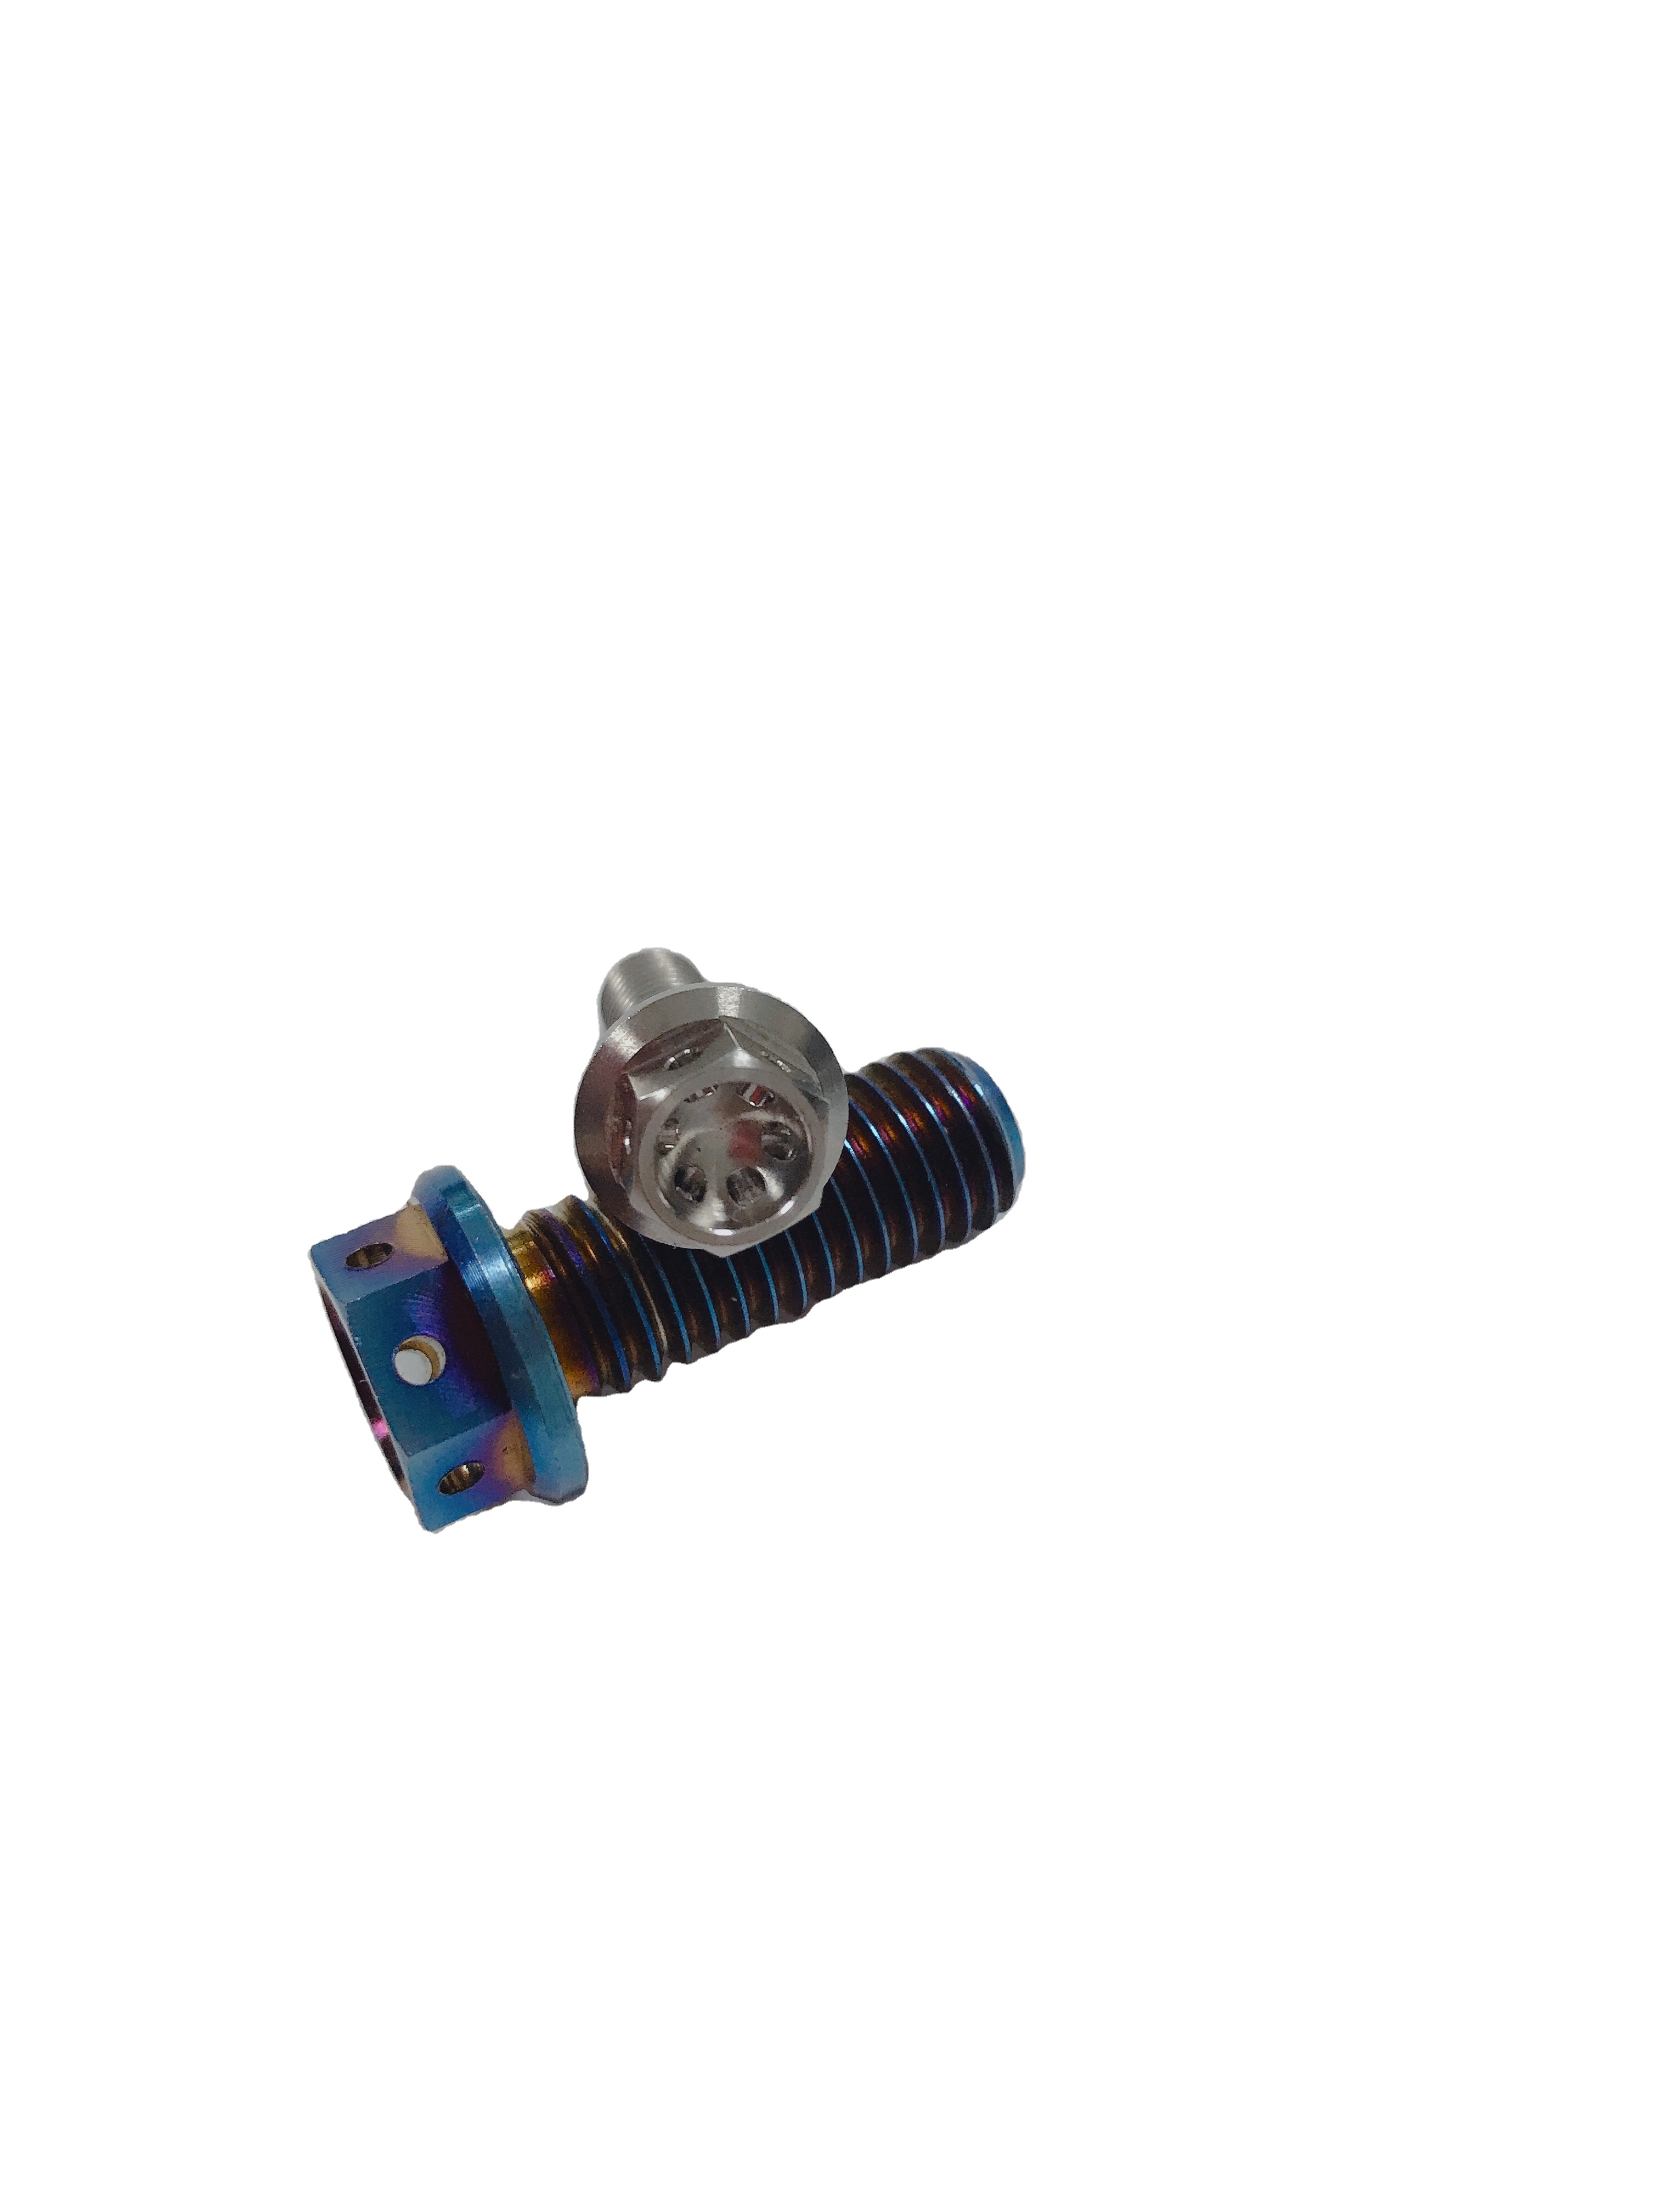
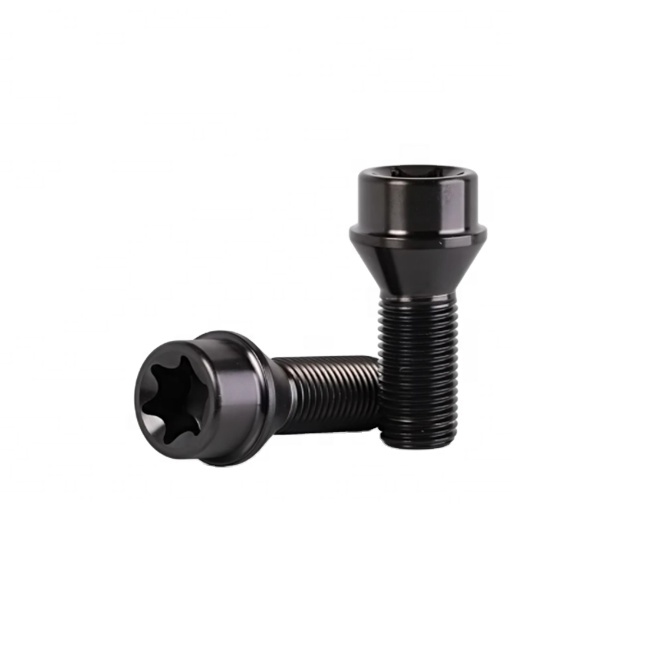
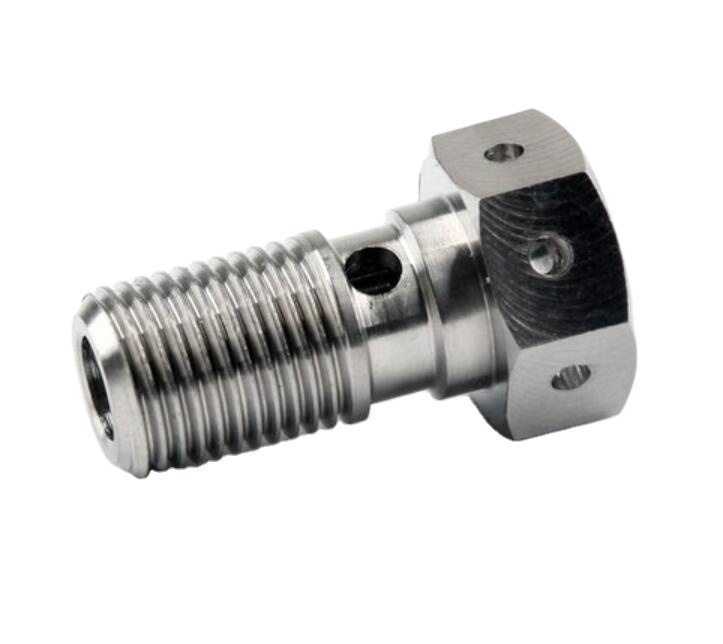
Engineering Grade 5 Titanium for Dudelange's Powertrain Ecosystem
A rigorous examination of titanium metallurgy, thermal dynamics, and mechanical performance under extreme internal combustion and turbomachinery stresses.
Strength-to-Weight Optimization
Grade 5 Titanium (Ti-6Al-4V) yields an ultimate tensile strength exceeding 895–1100 MPa while maintaining a density of merely 4.43 g/cm³. For Dudelange's specialized automotive racing and heavy industrial transport conversions, replacing Grade 10.9 or 12.9 carbon steel engine bolts with Ti-6Al-4V sheds approximately 44% of parasitic fastener weight without compromising yield point security.
This dynamic reduction lowers reciprocating mass in high-RPM valvetrains, flywheel attachments, and connecting rods, directly translating into faster throttle response, dampened rotational inertia, and suppressed vibrational harmonics across critical crankcase geometries.
Thermal Expansion Compatibility
Thermal cycling in high-output forced-induction engines induces severe clamp-load relaxation when disparate metals expand at mismatched rates. Ti-6Al-4V exhibits a coefficient of thermal expansion (CTE) of 8.6 × 10⁻⁶/K at 20°C to 100°C, significantly closer to high-performance cast iron and aluminum alloys than austenitic stainless steels.
This CTE proximity ensures that cylinder heads, turbocharger exhaust manifolds, and wastegate flange bolts retain stable preload torque through thermal excursions extending from cold ambient starts up to continuous operational temperatures of 450°C without yield stretching or catastrophic shear rupture.
Corrosion Immunity & PVD Nitriding
In the southern Luxembourg climate and salt-treated roadways of the Grand Duchy, exposed engine and chassis fasteners endure severe galvanic attack. The naturally forming, self-healing titanium dioxide (TiO2) passivation film renders Ti-6Al-4V fundamentally impervious to chloride pitting, acidic road splash, and industrial airborne sulfur compounds.
Our PVD (Physical Vapor Deposition) Titanium Nitride (TiN) and Chromium Nitride (CrN) vacuum coating processes increase fastener surface microhardness to >2000 HV, drastically curtailing thread galling risks during repeated pneumatic or torque-wrench servicing intervals.
| Material Specification | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Max Service Temp (°C) | Corrosion Resistance |
|---|---|---|---|---|---|
| Minghai Gr5 (Ti-6Al-4V) Fasteners | 4.43 | 950 – 1050 | 880 – 920 | 450 – 500 | Immune (Atmospheric/Chloride) |
| Class 10.9 High-Tensile Steel | 7.85 | 1040 | 940 | 300 | Low (Requires Zinc Flake/Plating) |
| Class 12.9 Alloy Steel (SCM435) | 7.85 | 1220 | 1100 | 320 | Vulnerable to Hydrogen Embrittlement |
| A4-80 Marine Stainless Steel | 8.00 | 800 | 600 | 400 | Moderate (Prone to Galling) |
| Commercially Pure Grade 2 Titanium | 4.51 | 345 – 485 | 275 – 380 | 300 | Exceptional (Chemical/Marine Only) |
High-Stress Application Environments Across Dudelange
Addressing the exact logistical, industrial, and automotive engineering demands of Dudelange's strategic multimodal and mechanical engineering hubs.
CFL Multimodal Logistics Corridor
Dudelange houses the critical CFL Multimodal rail-road interchange connecting Western Europe. Fleet operators running heavy transport tractor units and high-duty auxiliary power generators utilize our titanium engine studs and exhaust hardware to eliminate stud breakage caused by extreme low-frequency diesel harmonics and thermal shock.
Cross-Border GT & Track Day Tuning
Proximity to the Nürburgring Nordschleife (135 km) and Circuit de Spa-Francorchamps (140 km) makes Dudelange and the surrounding Minett region a premier nexus for specialized race engineering shops. Our 12-point cylinder head bolts and M14 Torx titanium wheel bolts endure cyclic brake rotor heat transfers up to 600°C without thread fatigue.
Industrial Turbomachinery Maintenance
Rooted in southern Luxembourg's metallurgical and industrial transformation, local manufacturing and energy plants employ our custom CNC-machined titanium tie rods, rotor retaining studs, and high-pressure steam valve fasteners to prevent hydrogen embrittlement common in standard high-strength steel bolts.
Specialized Prototype Automotive OEM
Automotive R&D centers in Luxembourg focused on electric vehicle (EV) battery enclosure mountings and lightweight hybrid combustion prototypes integrate our customized M6/M8 rolled-thread titanium fasteners to meet stringent non-magnetic, corrosion-immune, and crash-shear parameters.
Shaping the Future of Fastener Procurement in Luxembourg
How green mobility mandates, supply chain nearshoring resilience, and European metallurgical standards govern hardware selection in Dudelange.
The Decarbonization & Lightweighting Imperative
As the European Union intensifies Euro 7 emission thresholds and corporate fleet carbon accounting, every gram of unsprung and reciprocating mass in commercial and passenger vehicles undergoes scrutiny. Dudelange engineering firms are shifting from traditional zinc-nickel coated steel to titanium hardware, capturing an immediate 40–45% mass reduction on engine accessories, exhaust downpipes, and suspension linkages to fulfill fleet efficiency metrics.
Direct-from-Source Supply Chain Security
Mid-tier machine shops and performance garages in Dudelange historically relied on domestic distributors with steep markups and opaque supply lines. The emerging procurement paradigm favors direct relationships with verified primary manufacturers in Baoji (China's Titanium Valley) that can guarantee sponge-to-part metallurgical certificates (EN 10204 3.1) and transparent lead-time tracking via express air freight directly to Findel Airport.
Standardization Under DIN, ISO, and REACH
Procurement teams in the Grand Duchy require full compliance with EU REACH Regulation (EC No 1907/2006) and RoHS directives. Our factory produces fasteners strictly adhering to DIN 6923, DIN 933, DIN 912, and ISO 4161, entirely free from banned heavy metals, hexavalent chromium passivations, or conflict minerals, streamlining local customs clearance through the Luxembourg Customs and Excise Agency.
Why Dudelange Engineers Partner with Vunza Titanium
Combining the metallurgical supremacy of Baoji's Titanium Valley with world-class multi-axis machining tolerances to deliver unyielding hardware reliability.
Sponge-to-Part Quality Traceability
Situated adjacent to the Baoti Group Industrial Park, our plant commands direct access to premium aerospace-grade titanium sponge. We manage every phase in-house: vacuum arc remelting (VAR), precision bar extrusions, thread rolling, 5-axis CNC turning, ultrasonic flaw testing, and final optical dimensional sorting, eliminating sub-tier contamination.
Cold & Hot Thread Rolling Mastery
Unlike budget workshops that cut screw threads with lathe tooling (which severs grain structure and invites fatigue crack propagation), Vunza rolls every engine bolt thread. Thread rolling realigns the internal crystalline grain flow of Grade 5 titanium along the contour of each crest and root, increasing fatigue endurance life by more than 300% under high-vibration operational loads.
Rapid Prototype to Production Cadence
Whether you require a short run of 50 custom-engineered M11 head studs for a high-boost turbo modification project or recurring 10,000-piece container deliveries for industrial equipment assembly, our dual R&D and production engineering workflow responds within 9 hours with comprehensive DFM (Design for Manufacturability) analysis.
Frequently Asked Questions by Dudelange Buyers
Addressing common queries regarding international shipping, technical torque specifications, customs documentation, and metallurgical validation.
How does shipping and customs clearance operate for deliveries into Dudelange?
We provide full DDP (Delivered Duty Paid) and DAP (Delivered at Place) shipping options into Luxembourg via DHL Express, FedEx, and specialized air freight direct to Luxembourg Findel Airport (LUX). Typical transit times for stock and standard sizes are 4 to 6 business days. All commercial invoices are issued with accurate HS codes (typically 8108.90 for titanium articles) ensuring smooth clearance with the Luxembourg Administration des Douanes et Accises.
What torque adjustment factor is needed when replacing steel engine bolts with titanium?
Because Grade 5 Titanium possesses a lower elastic modulus (approximately 114 GPa compared to 210 GPa for structural steel) and distinct frictional characteristics, torque values generally require a 10% to 15% reduction when installed with high-temperature anti-seize lubricant (such as copper-paste, MoS2, or ceramic assembly compound). A full tightening torque chart and friction coefficient table are supplied with each custom shipment to prevent overtightening.
Do you supply EN 10204 3.1 Inspection Certificates with batch traceability?
Yes. Every production run is backed by comprehensive Mill Test Certificates (MTC) according to EN 10204 Type 3.1 standards. This dossier reports the quantitative chemical composition (Al, V, Fe, C, N, H, O contents verifying pure Grade 5 / TC4 chemistry) and mechanical test data, including yield strength, ultimate tensile strength, elongation percentage, and Rockwell hardness verification.
Can you machine non-standard custom engine bolts from client 2D/3D CAD drawings?
Absolutely. Over 40% of our production comprises custom components engineered to customer-supplied STEP, IGES, DXF, or PDF engineering prints. We routinely produce non-standard shank diameters, step-down studs, customized 12-point ARP-style flange heads, internal Torx recess drives, and specialized cross-drilled safety wire holes to tolerances within ±0.005 mm.
What surface treatments are recommended for engine manifold and turbo studs?
For exhaust manifolds, turbo downpipes, and wastegate housings exposed to continuous thermal loads ≥ 400°C, we recommend our specialized PVD Nitride Black or micro-polished finish paired with high-temperature silver plating. These coatings prevent atmospheric oxidation and galling between titanium threads and cylinder heads under high-temperature expansion.
What are your typical minimum order quantities (MOQ) and sample lead times?
Standard DIN-specification titanium bolts (e.g., M6, M8, M10 flange and hex screws) in stock maintain an MOQ as low as 50 to 100 units. For fully customized prototype development, sample batches of 10 to 20 pieces can be CNC-machined and shipped to Dudelange within 10 to 14 days following engineering drawing sign-off.
Ready to Engineer Custom Titanium Hardware for Dudelange?
Submit your 2D/3D CAD models, standard fastener part numbers, or material requirements. Our factory engineering department reviews DFM feasibility, tolerance fits, and quote breakdowns within 9 business hours.